Каталог Sumitomo фрезы со сменными пластинами - страница 95
Навигация
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo модульные системы для револьверных головок токарных станков
 Каталог Sumitomo токарные резцы (державки) для внутреннего точения
 Общий каталог Sumitomo 2018 - 2019
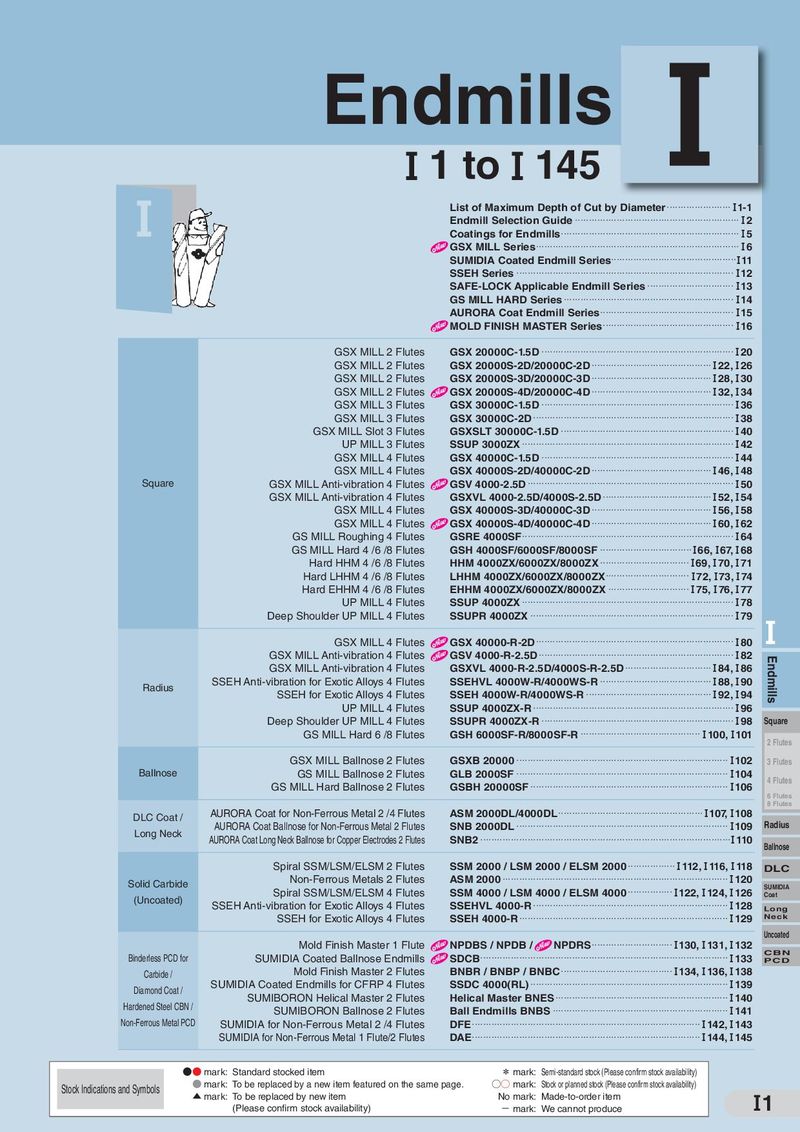 Каталог Sumitomo монолитные фрезы
- H001
- H002
- H003
- H004
- H005
- H006
- H007
- H008
- H009
- H010
- H011
- H012
- H013
- H014
- H015
- H016
- H017
- H018
- H019
- H020
- H021
- H022
- H023
- H024
- H025
- H026
- H027
- H028
- H029
- H030
- H031
- H032
- H033
- H034
- H035
- H036
- H037
- H038
- H039
- H040
- H041
- H042
- H043
- H044
- H045
- H046
- H047
- H048
- H049
- H050
- H051
- H052
- H053
- H054
- H055
- H056
- H057
- H058
- H059
- H060
- H061
- H062
- H063
- H064
- H065
- H066
- H067
- H068
- H069
- H070
- H071
- H072
- H073
- H074
- H075
- H076
- H077
- H078
- H079
- H080
- H081
- H082
- H083
- H084
- H085
- H086
- H087
- H088
- H089
- H090
- H091
- H092
- H093
- H094
- H095
- H096
- H097
- H098
- H099
- H100
- H101
- H102
- H103
- H104
- H105
- H106
- H107
- H108
- H109
- H110
- H111
- H112
- H113
- H114
- H115
- H116
- H117
- H118
- H119
- H120
- H121
- H122
- H123
- H124
- H125
- H126
- H127
- H128
- H129
- H130
- H131
- H132
- H133
- H134
- H135
- H136
- H137
- H138
- H139
- H140
- H141
- H142
- H143
- H144
- H145
- H146
- H147
- H148
- H149
- H150
- H151
- H152
- H153
- H154
- H155
- H156
- H157
- H158
- H159
- H160
- H161
- H162
- H163
- H164
- H165
- H166
- H167
- H168
- H169
- H170
- H171
- H172
- H173
- H174

- General Features SEC-WaveMill WFXH type is a high efficiency, multi-purpose cutter, that uses the WFX series inserts, for high-feed roughing and a variety of processes.
- Characteristics 1. Stable, high-efficiency milling with superior cutting edge sharpness. 2. Supports various types of processes (ramping and helical milling). 3. Able to use the selection of inserts from the WFX series.
Cutting Force : Stable milling with high cutting edge sharpness Chip : Small curls and low cutting temperature
2,000
WFXH(R1.6-G Chipbreaker)
1,500
1,000
500
WFXH Comp. A Comp. B
0 WFXH Comp. Work Material : S50C Work Material : S50C H
Tool : WFXH12063RS(5 flutes) Tool : WFXH12063RS, SOMT120416PDER-G(ACP200)
Cutting Conditions : c=200m/min, z=1.0mm/t, =0.5mm,
| p | Cutting Conditions : | =200m/min, | =1.0mm/t, | =1mm, | =35mm, Dry | |
| =44mm, Dry | c | z | p | e |
e
- Grade Selection
| Work Material Grade | Finishing to Light Cutting | Medium Cut | Rough to Heavy Cutting | Work Material Grade | Finishing to Light Cutting | Medium Cut | Rough to Heavy Cutting | |
| Face | ||||||||
| Milling |
| C ACP100 | C ACK200 Shoulder | |
| K | Milling | |
| P | ACP200 | High Feed |
| Cast Iron | ACK300 | |
| Steel | P | |
| P Radius | ||
| ACP300 | Multi- | |
| P | Purpose | |
| DL1000 R/ | ||
| Profiling | ||
| N | P | |
| M | C ACM200 | Groove/ |
| T-Slot | ||
| Non-Ferrous Metal | ||
| Stainless Steel | ACM300 | H1 Chamfering |
| P | Aluminum/ | |
| Light Alloys |
The letters "C" and "P" at either end of each grade indicate coating type. C:CVD :PVD Blank: Non-coated High-Speed
P Cast Iron
- Chipbreaker Selection
Work Material P Steel M Stainless Steel K Cast Iron N Aluminum
| L | L Type | G Type | H Type | S Type | ||
| General Purpose (Standard) | ||||||
| Light Cutting | Breaker | |||||
| G |
H Characteristic Low Cutting Force General Purpose Strong Edge Sharp Edge
Cutting Edge 20° 15° 10° 25°
Heavy Cutting Figure Edge Strength → High Light Cutting, Heavy Cut,
Main Chipbreaker
Application Low Rigidity Milling Heavy Interrupted Machining Non-Ferrous Metal
General - Interrupted Milling Low-Burr Design Hardened steel