Каталог Sumitomo фрезы со сменными пластинами - страница 17
Навигация
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo модульные системы для револьверных головок токарных станков
 Каталог Sumitomo токарные резцы (державки) для внутреннего точения
 Общий каталог Sumitomo 2018 - 2019
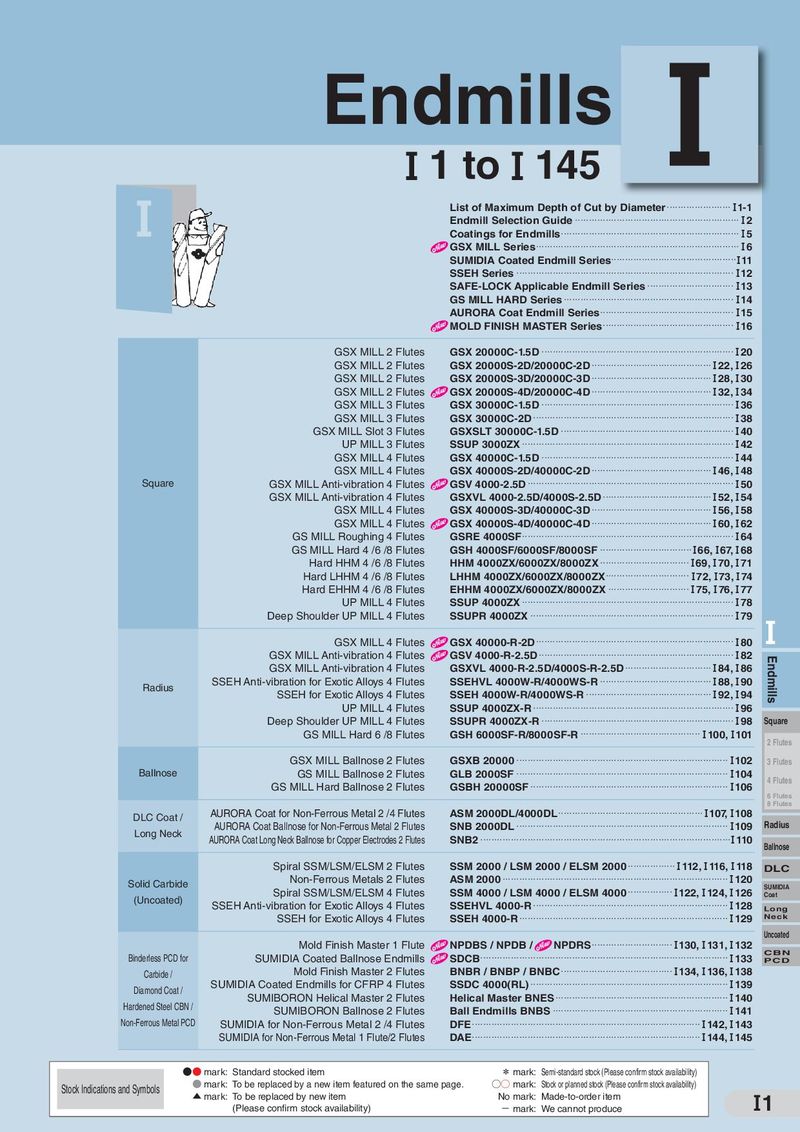 Каталог Sumitomo монолитные фрезы
- H001
- H002
- H003
- H004
- H005
- H006
- H007
- H008
- H009
- H010
- H011
- H012
- H013
- H014
- H015
- H016
- H017
- H018
- H019
- H020
- H021
- H022
- H023
- H024
- H025
- H026
- H027
- H028
- H029
- H030
- H031
- H032
- H033
- H034
- H035
- H036
- H037
- H038
- H039
- H040
- H041
- H042
- H043
- H044
- H045
- H046
- H047
- H048
- H049
- H050
- H051
- H052
- H053
- H054
- H055
- H056
- H057
- H058
- H059
- H060
- H061
- H062
- H063
- H064
- H065
- H066
- H067
- H068
- H069
- H070
- H071
- H072
- H073
- H074
- H075
- H076
- H077
- H078
- H079
- H080
- H081
- H082
- H083
- H084
- H085
- H086
- H087
- H088
- H089
- H090
- H091
- H092
- H093
- H094
- H095
- H096
- H097
- H098
- H099
- H100
- H101
- H102
- H103
- H104
- H105
- H106
- H107
- H108
- H109
- H110
- H111
- H112
- H113
- H114
- H115
- H116
- H117
- H118
- H119
- H120
- H121
- H122
- H123
- H124
- H125
- H126
- H127
- H128
- H129
- H130
- H131
- H132
- H133
- H134
- H135
- H136
- H137
- H138
- H139
- H140
- H141
- H142
- H143
- H144
- H145
- H146
- H147
- H148
- H149
- H150
- H151
- H152
- H153
- H154
- H155
- H156
- H157
- H158
- H159
- H160
- H161
- H162
- H163
- H164
- H165
- H166
- H167
- H168
- H169
- H170
- H171
- H172
- H173
- H174
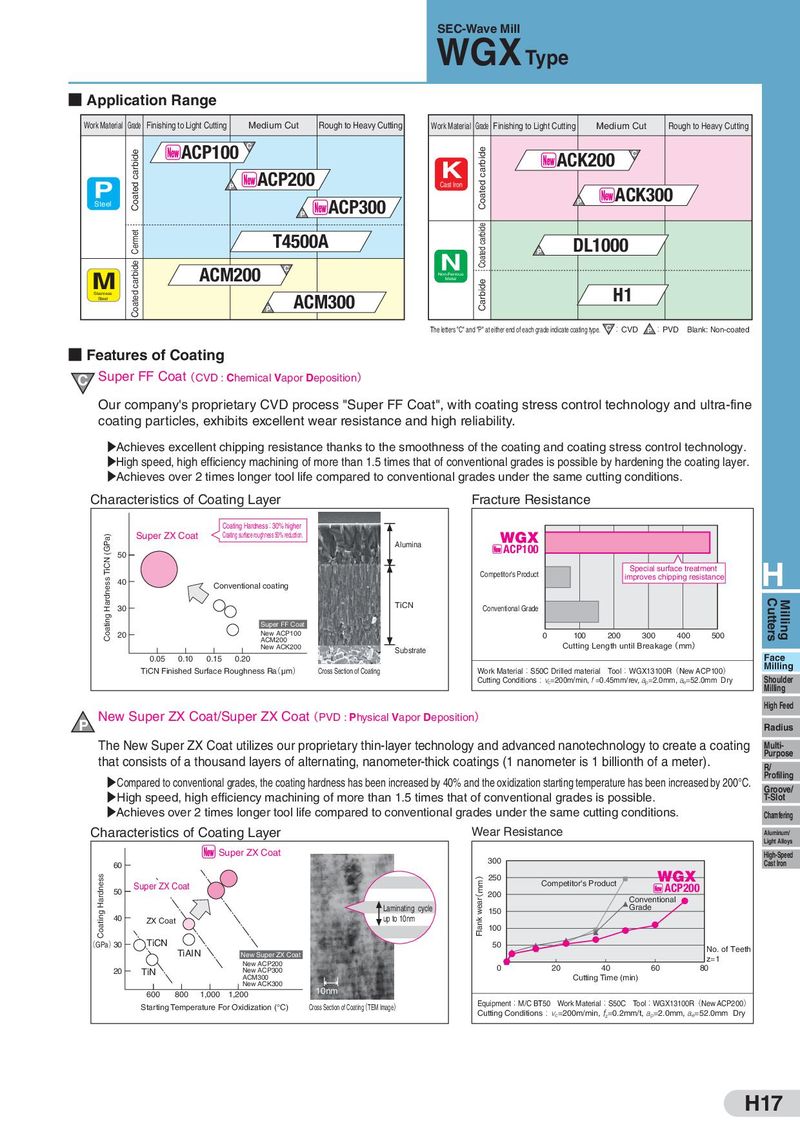
- Application Range
Work Material Grade Finishing to Light Cutting Medium Cut Rough to Heavy Cutting Work Material Grade Finishing to Light Cutting Medium Cut Rough to Heavy Cutting
ACP100 C ACK200 C K K ACP200
P P Cast Iron鋳鉄 P ACK300
Steel鋼 ACP300 P
P T4500A DL1000 N N P ACM200 C
M M 非鉄金属 Non-Ferrous Metal ステンレス鋼 H1 Stainless ACM300 Steel P The letters "C" and "P" at either end of each grade indicate coating type. :CCVD :PVD Blank: Non-coated P
- Features of Coating C Super FF Coat (CVD : Chemical Vapor Deposition) Our company's proprietary CVD process "Super FF Coat", with coating stress control technology and ultra-fine coating particles, exhibits excellent wear resistance and high reliability. Achieves excellent chipping resistance thanks to the smoothness of the coating and coating stress control technology. High speed, high efficiency machining of more than 1.5 times that of conventional grades is possible by hardening the coating layer. Achieves over 2 times longer tool life compared to conventional grades under the same cutting conditions. Characteristics of Coating Layer Fracture Resistance
Coating Hardness : 30% higher
Super ZX Coat Coating surface roughness 50% reduction. WGX
Alumina ACP100 50 H Special surface treatment Competitor's Product improves chipping resistance
40 Conventional coating
| 30 | TiCN | Conventional Grade | |
| Super FF Coat |
| 20 | New ACP100 | 0 | 100 | 200 | 300 | 400 | 500 | ||
| ACM200 | ( | ) | |||||||
| New ACK200 | Cutting Length until Breakage | mm | |||||||
| Substrate |
0.05 0.10 0.15 0.20 Face
| ( | ) | : | : | ( | ) | Milling | ||||
| TiCN Finished Surface Roughness Ra μm | Cross Section of Coating | Work Material | S50C Drilled material | Tool | WGX13100R | New ACP100 | ||||
| Cutting Conditions:v =200m/min, f =0.45mm/rev, a =2.0mm, a =52.0mm Dry | Shoulder |
c p e Milling
High Feed New Super ZX Coat/Super ZX Coat (PVD : Physical Vapor Deposition) P Radius
The New Super ZX Coat utilizes our proprietary thin-layer technology and advanced nanotechnology to create a coating Multi- Purpose that consists of a thousand layers of alternating, nanometer-thick coatings (1 nanometer is 1 billionth of a meter). R/ Profiling Compared to conventional grades, the coating hardness has been increased by 40% and the oxidization starting temperature has been increased by 200°C. Groove/
High speed, high efficiency machining of more than 1.5 times that of conventional grades is possible. T-Slot
Achieves over 2 times longer tool life compared to conventional grades under the same cutting conditions. Chamfering
Characteristics of Coating Layer Wear Resistance
Aluminum/ Light Alloys Super ZX Coat High-Speed 300 Cast Iron 60 250 WGX
| Super ZX Coat | Competitor's Product | ACP200 | |||
| 50 | 200 | ||||
| Conventional 従来品 D | |||||
| F |
Laminating cycle 150 Grade
| 40 | ZX Coat | up to 10nm | |
| D |
100 ■F D
| ( | ) | FD | D | |||
| GPa 30 | TiCN | 50 | F | ■ |
| F | D■ | No. of Teeth | ||
| TiAIN | D■ | |||
| New Super ZX Coat | z=1 | |||
| DF■ |
New ACP200 0 20 40 60 80
| 20 | TiN | New ACP300 | |
| ACM300 | Cutting Time (min) | ||
| New ACK300 |
600 800 1,000 1,200 10nm
| Equipment:M/C BT50 | Work Material:S50C | Tool:WGX13100R(New ACP200) | ||
| Starting Temperature For Oxidization (°C) | Cross Section of Coating (TEM Image) | |||
| Cutting Conditions:v =200m/min, f =0.2mm/t, a =2.0mm, a =52.0mm Dry |
c z p e