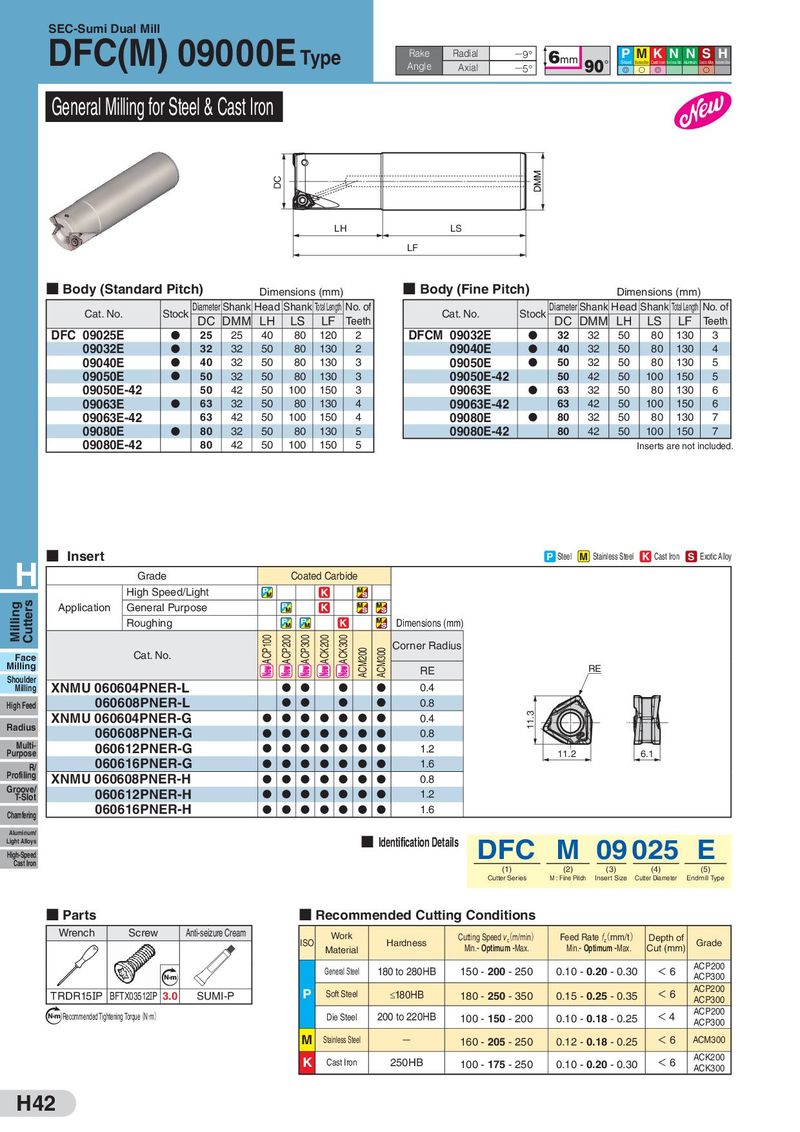
DFC(M) 09000ESEC-Sumi Dual Mill
General Milling for Steel & Cast Iron
LH LS LF
| ■ Body (Standard Cat No | Pitc Stock | h) Diameter | Shank | Head Dim | Shank ensions | Total Length (mm) | No. of |
| . . | | DC | DMM | LH | LS | LF | Teeth |
| DFC 09025E | D | 25 | 25 | 40 | 80 | 120 | 2 |
| 09032E | D | 32 | 32 | 50 | 80 | 130 | 2 |
| 09040E | D | 40 | 32 | 50 | 80 | 130 | 3 |
| 09050E | D | 50 | 32 | 50 | 80 | 130 | 3 |
| 09050E-42 | | 50 | 42 | 50 | 100 | 150 | 3 |
| 09063E | D | 63 | 32 | 50 | 80 | 130 | 4 |
| 09063E-42 | | 63 | 42 | 50 | 100 | 150 | 4 |
| 09080E | D | 80 | 32 | 50 | 80 | 130 | 5 |
| 09080E-42 | | 80 | 42 | 50 | 100 | 150 | 5 |
| ■ Body (Fine Pitc | h) | | | Dim | ensions | (mm) | |
| | Diameter | Shank | Head | Shank | Total Length | No. of |
| Cat. No. | Stock | DC | DMM | LH | LS | LF | Teeth |
| DFCM 09032E | D | 32 | 32 | 50 | 80 | 130 | 3 |
| 09040E | D | 40 | 32 | 50 | 80 | 130 | 4 |
| 09050E | D | 50 | 32 | 50 | 80 | 130 | 5 |
| 09050E-42 | | 50 | 42 | 50 | 100 | 150 | 5 |
| 09063E | D | 63 | 32 | 50 | 80 | 130 | 6 |
| 09063E-42 | | 63 | 42 | 50 | 100 | 150 | 6 |
| 09080E | D | 80 | 32 | 50 | 80 | 130 | 7 |
| 09080E-42 | | 80 | 42 | 50 | 100 | 150 | 7 |
| H | | | | P Steel | M Stainless Steel | K Cast Iron | S Exotic Alloy |
| Grade | Coated Carbide | | | | | |
| High Speed/Light | | K | | | | |
Application General Purpose K
| Roughing | K | Dimensions (mm) |
| | | Corner Radius |
| Face | Cat. No. | | |
Milling RE RE
Shoulder D D D D
Milling XNMU 060604PNER-L 0.4
| 060608PNER-L | D D | D | D | 0.8 |
| High Feed | | | | | |
XNMU 060604PNER-G DDDDDDD 0.4
| Radius | 060608PNER-G | DDDDDDD | |
| | | 0.8 |
| Multi- | 060612PNER-G | DDDDDDD | 1.2 |
Purpose 11.2 6.1
| 060616PNER-G | DDDDDDD | 1.6 |
| R/ | | |
| Profiling | XNMU 060608PNER-H | DDDDDDD | 0.8 |
| Groove/ | 060612PNER-H | DDDDDDD | |
| T-Slot | | | 1.2 |
| 060616PNER-H | DDDDDDD | 1.6 |
| Chamfering | | | |
| Aluminum/ | | | ■ Identification Details |
| Light Alloys | DFC | | | M | 09 025 | | | | E |
| High-Speed | | | | | | | | | |
| Cast Iron | | | | | | | | | |
| | (1) | | (2) | (3) | | (4) | | (5) |
| Cutter Series | | M : Fine Pitch | | Insert Size | Cutter Diameter | | Endmill Type | |
- Parts
- Recommended Cutting Conditions
| ISO | Work Material | Hardness | Cutting Speedvc(m/min) Min.-Optimum-Max. | Feed Ratefz(mm/t) Min.-Optimum-Max. | Depth of Cut (mm) | Grade |
| General Steel | 180 to 280HB | 150 -200- 250 | 0.10 -0.20- 0.30 | `<`6 | ACP200 ACP300 |
| P | Soft Steel | ≤180HB | 180 -250- 350 | 0.15 -0.25- 0.35 | `<`6 | ACP200 ACP300 |
| Die Steel | 200 to 220HB | 100 -150- 200 | 0.10 -0.18- 0.25 | `<`4 | ACP200 ACP300 |
| M | Stainless Steel | - | 160 -205- 250 | 0.12 -0.18- 0.25 | `<`6 | ACM300 |
| K | Cast Iron | 250HB | 100 -175- 250 | 0.10 -0.20- 0.30 | `<`6 | ACK200 ACK300 |
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo модульные системы для револьверных головок токарных станков
 Каталог Sumitomo токарные резцы (державки) для внутреннего точения
 Общий каталог Sumitomo 2018 - 2019
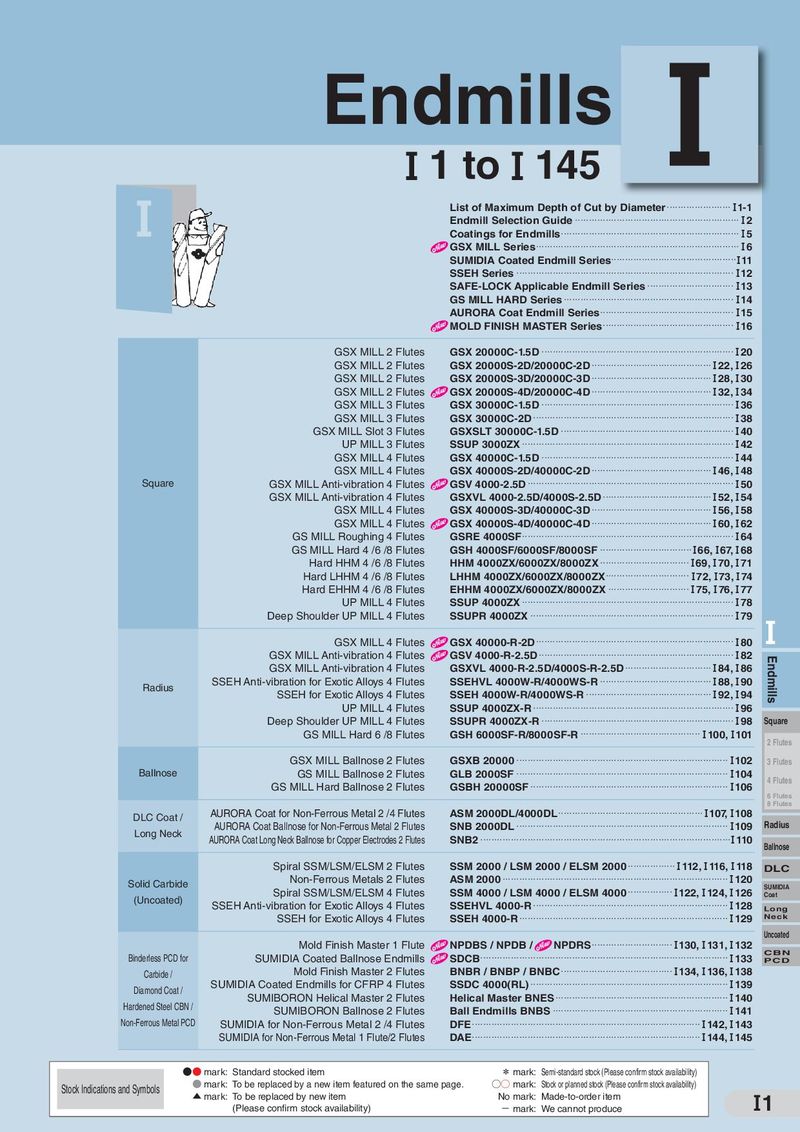 Каталог Sumitomo монолитные фрезы