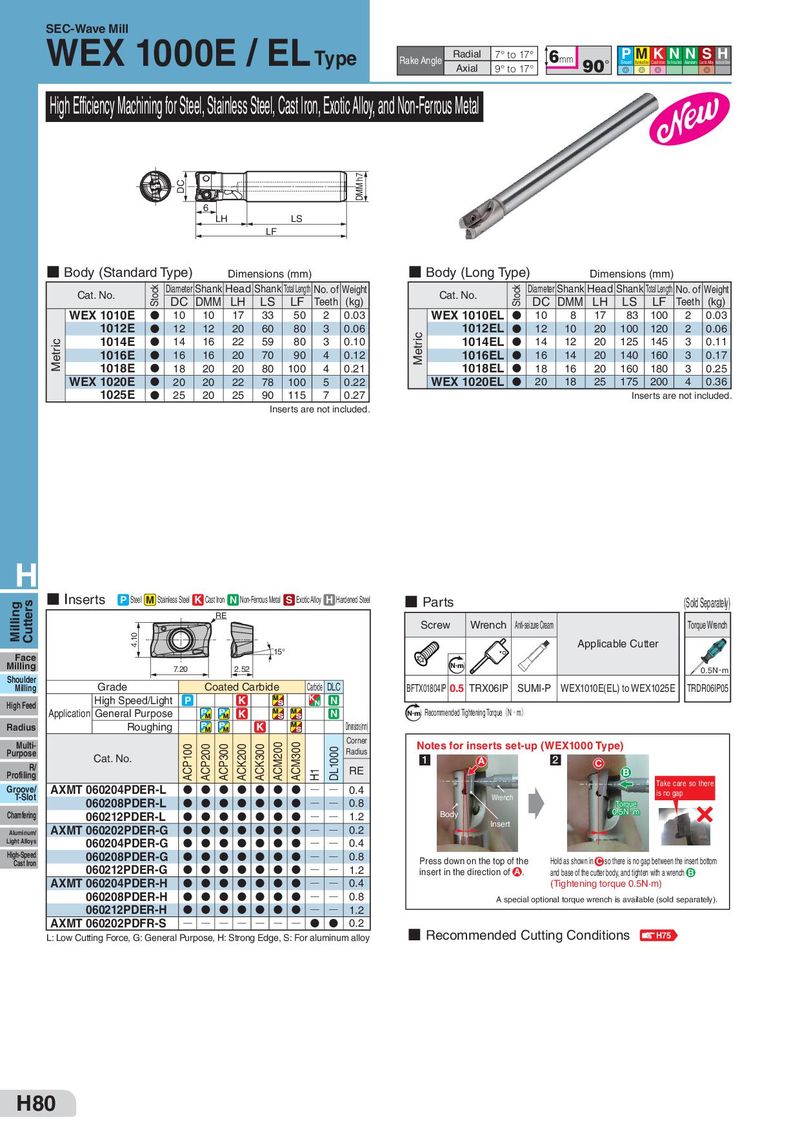
SEC-Wave MillWEX 1000E / EL
| Axial | 9° to 17° | Steel | Stainless Steel Cast Iron Non-Ferrous Metal Aluminum Exotic Alloy Hardened Steel | | |
| | G | G | G | G |
High Efficiency Machining for Steel, Stainless Steel, Cast Iron, Exotic Alloy, and Non-Ferrous Metal
6 LH LS LF
- Body (Standard Type)
- Body (Long Type)
Dimensions (mm) Dimensions (mm) k Diameter Shank Head Shank Total Length No. of Weight k Diameter Shank Head Shank Total Length No. of Weight Cat. No. Cat. No.
| | | DC DMM LH | | | LS | LF | Teeth | (kg) | | | | DC DMM LH | | | | LS | LF | Teeth | (kg) |
| WEX 1010E | | D | 10 | 10 | 17 | 33 | 50 | 2 | 0.03 | WEX 1010EL | | D | 10 | 8 | 17 | | 83 | 100 | 2 | 0.03 |
| 1012E | D | 12 | 12 | 20 | 60 | 80 | 3 | 0.06 | | 1012EL | D | 12 | 10 | 20 | 100 | | 120 | 2 | 0.06 |
| 1014E | D | 14 | 16 | 22 | 59 | 80 | 3 | 0.10 | | 1014EL | D | 14 | 12 | 20 | 125 | | 145 | 3 | 0.11 |
| 1016E | D | 16 | 16 | 20 | 70 | 90 | 4 | 0.12 | | 1016EL | D | 16 | 14 | 20 | 140 | | 160 | 3 | 0.17 |
| 1018E | D | 18 | 20 | 20 | 80 | 100 | 4 | 0.21 | | 1018EL | D | 18 | 16 | 20 | 160 | | 180 | 3 | 0.25 |
| WEX 1020E | | D | 20 | 20 | 22 | 78 | 100 | 5 | 0.22 | WEX 1020EL | | D | 20 | 18 | 25 | 175 | | 200 | 4 | 0.36 |
| 1025E | D | 25 | 20 | 25 | 90 | 115 | 7 | 0.27 | | | | | | | | Inserts are not included. | | | |
Inserts are not included.
H
| P Steel M Stainless Steel K Cast Iron N Non-Ferrous Metal S Exotic Alloy H Hardened Steel Parts | (Sold Separately) |
| RE | |
| Screw | Wrench Anti-seizure Cream Torque Wrench |
| Applicable Cutter |
| 15° | |
| Face | |
| Milling | 7.20 | 2.52 | N m | | ・ |
| | | | 0.5N m | |
| Shoulder | | | | | |
Milling Grade Coated Carbide Carbide DLC BFTX01804IP 0.5 TRX06IP SUMI-P WEX1010E(EL) to WEX1025E TRDR06IP05
| | High Speed/Light | P | K | N | | | |
| High Feed | | | | | | | ( ・ ) | |
| Application General Purpose | | | K | N | N m Recommended Tightening Torque N | | m |
| Radius | Roughing | K | Dimensions (mm) | |
| | | Corner | |
| Multi- | | | | Notes for inserts set-up (WEX1000 Type) |
| Purpose | | | Radius | |
| | Cat. No. | | | 1 | A | 2 | | | |
| R/ | | | | | | | C | | |
| | | | RE | | | | | B | |
| Profiling | | | | | | | | | | |
| | | DDDDDDDQQ | | | | | | | Take care so there |
| Groove/ | AXMT 060204PDER-L | 0.4 | |
| T-Slot | | | is no gap |
| 060208PDER-L | DDDDDDDQQ | 0.8 | Wrench | |
| | | | | TorqueTorque |
| | DDDDDDDQQ | | | 0.5N0.5N・・mm |
| Chamfering | 060212PDER-L | | 1.2 | Body | |
| AXMT 060202PDER-G | DDDDDDDQQ | 0.2 | Insert | |
| Aluminum/ | | DDDDDDDQQ | | | |
| Light Alloys | 060204PDER-G | | 0.4 | | |
| High-Speed | 060208PDER-G | DDDDDDDQQ | 0.8 | | |
Cast Iron Press down on the top of the Hold as shown in C so there is no gap between the insert bottom
| 060212PDER-G | DDDDDDDQQ | 1.2 | |
| | | | insert in the direction of .A and base of the cutter body, and tighten with a wrench B |
| AXMT 060204PDER-H | | DDDDDDDQQ | 0.4 | (Tightening torque 0.5N·m) |
| 060208PDER-H | DDDDDDDQQ | 0.8 | |
| | | | A special optional torque wrench is available (sold separately). |
| 060212PDER-H | DDDDDDDQQ | 1.2 | |
| AXMT 060202PDFR-S | | QQQQQQQDD | 0.2 | |
- Recommended Cutting Conditions
L: Low Cutting Force, G: General Purpose, H: Strong Edge, S: For aluminum alloy H75
H80H
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo модульные системы для револьверных головок токарных станков
 Каталог Sumitomo токарные резцы (державки) для внутреннего точения
 Общий каталог Sumitomo 2018 - 2019
 Каталог Sumitomo монолитные фрезы