Каталог Sumitomo фрезы со сменными пластинами - страница 124
Навигация
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo модульные системы для револьверных головок токарных станков
 Каталог Sumitomo токарные резцы (державки) для внутреннего точения
 Общий каталог Sumitomo 2018 - 2019
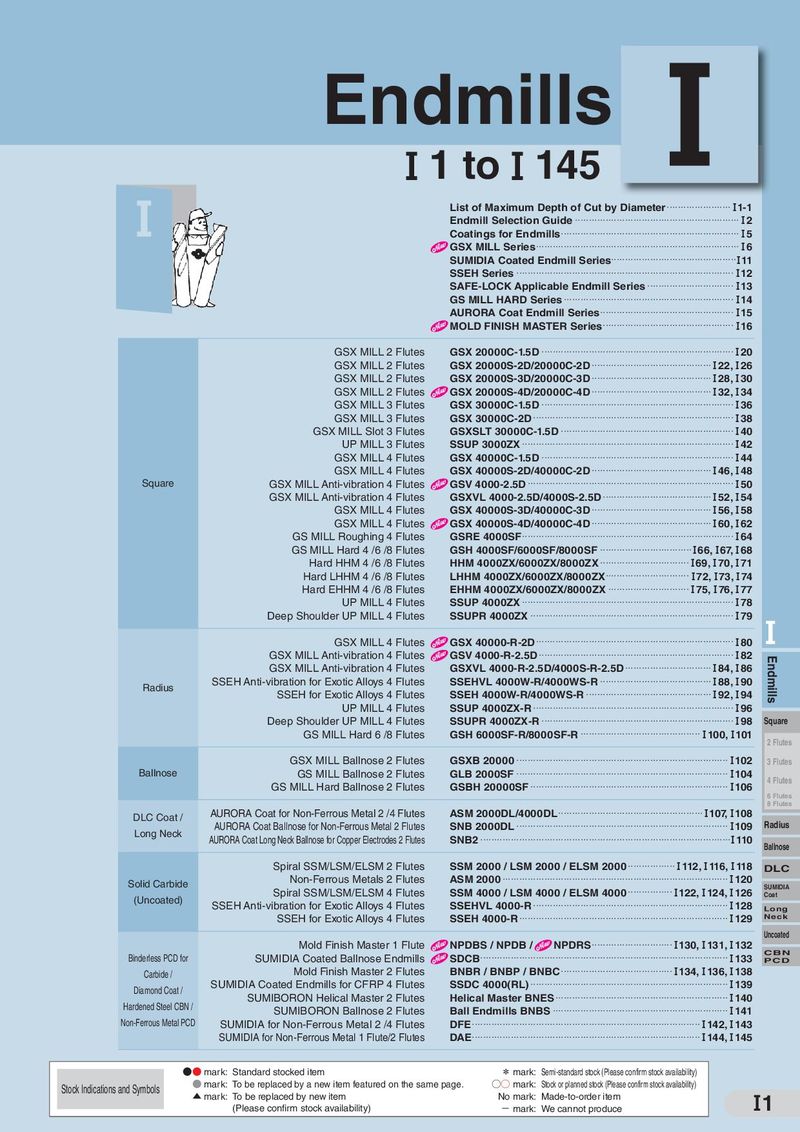 Каталог Sumitomo монолитные фрезы
- H001
- H002
- H003
- H004
- H005
- H006
- H007
- H008
- H009
- H010
- H011
- H012
- H013
- H014
- H015
- H016
- H017
- H018
- H019
- H020
- H021
- H022
- H023
- H024
- H025
- H026
- H027
- H028
- H029
- H030
- H031
- H032
- H033
- H034
- H035
- H036
- H037
- H038
- H039
- H040
- H041
- H042
- H043
- H044
- H045
- H046
- H047
- H048
- H049
- H050
- H051
- H052
- H053
- H054
- H055
- H056
- H057
- H058
- H059
- H060
- H061
- H062
- H063
- H064
- H065
- H066
- H067
- H068
- H069
- H070
- H071
- H072
- H073
- H074
- H075
- H076
- H077
- H078
- H079
- H080
- H081
- H082
- H083
- H084
- H085
- H086
- H087
- H088
- H089
- H090
- H091
- H092
- H093
- H094
- H095
- H096
- H097
- H098
- H099
- H100
- H101
- H102
- H103
- H104
- H105
- H106
- H107
- H108
- H109
- H110
- H111
- H112
- H113
- H114
- H115
- H116
- H117
- H118
- H119
- H120
- H121
- H122
- H123
- H124
- H125
- H126
- H127
- H128
- H129
- H130
- H131
- H132
- H133
- H134
- H135
- H136
- H137
- H138
- H139
- H140
- H141
- H142
- H143
- H144
- H145
- H146
- H147
- H148
- H149
- H150
- H151
- H152
- H153
- H154
- H155
- H156
- H157
- H158
- H159
- H160
- H161
- H162
- H163
- H164
- H165
- H166
- H167
- H168
- H169
- H170
- H171
- H172
- H173
- H174

WFXCSEC-Wave Mill
- General Features The SEC-Wave Mill WFXC type is a chamfering tool that uses inserts for the WFX series. This allows the WFXC type to support many types of work materials using a variety of grades.
- Application Range
Work Material Grade Finishing to Light Cutting Medium Cut Rough to Heavy Cutting Work Material Grade Finishing to Light Cutting Medium Cut Rough to Heavy Cutting
ACP100 C ACK200 C
K P ACP200 Cast Iron ACK300 Steel P
P
ACP300
P
DL1000
N P
| M | ACM200 | C | ||
| Non-Ferrous Metal | ||||
| Stainless Steel | ACM300 | H1 |
P The letters "C" and "P" at either end of each grade indicate coating type. :CCVD :PVD Blank: Non-coated H P
- CAUTION Since chamfering uses the straight cutting edge portion of the insert, the range that can be chamfered
will change depending on the corner radius (RE) of the insert that is attached to the body. Work diameter: Use in a range greater than or equal to DC1 and less than or equal to DC2. Depth: The workpiece can be chamfered from a, which is the distance from the tip of the tool to the straight cutting edge, at the depth indicated by b. Face Milling Shoulder Dimensions (mm) Milling
| Bd | Insert | Min. Work Dia. | Max. Work Dia. | Min. Depth | Max. Depth | Max. Diameter | ||||
| oy | ||||||||||
| Cat. No. | RE | DC1 | DC2 | a | b | DCX | ||||
| SOMT080304 | 0.4 | 7.5 | 15.8 | 0.1 | 4.1 | 17.8 | ||||
| WFXC08008E | SOMT080308 | 0.8 | 8.0 | 15.8 | 0.2 | 3.9 | 17.5 | |||
| SOMT080312 | 1.2 | 8.5 | 15.8 | 0.4 | 3.6 | 17.2 | ||||
| SOMT080304 | 0.4 | 15.5 | 23.8 | 0.1 | 4.1 | 25.8 | ||||
| WFXC08016E | SOMT080308 | 0.8 | 16.0 | 23.8 | 0.2 | 3.9 | 25.5 | 45° | ||
| SOMT080312 | 1.2 | 16.5 | 23.8 | 0.3 | 3.6 | 25.2 | b | |||
| SOMT120404 | 0.4 | 24.6 | 38.3 | 0.1 | 6.8 | 41.3 | ||||
| WFXC12025E | SOMT120408 | 0.8 | 25.0 | 38.3 | 0.2 | 6.6 | 41.0 | |||
| SOMT120412 | 1.2 | 25.6 | 38.3 | 0.4 | 6.3 | 40.7 | a | |||
| SOMT120416 | 1.6 | 26.1 | 38.3 | 0.5 | 6.1 | 40.4 | DC1 | |||
| SOMT120404 | 0.4 | 31.6 | 45.3 | 0.1 | 6.8 | 48.3 | DC2 | |||
| WFXC12032E | SOMT120408 | 0.8 | 32.0 | 45.3 | 0.2 | 6.6 | 48.0 | |||
| SOMT120412 | 1.2 | 32.6 | 45.3 | 0.4 | 6.3 | 47.7 | DCX | |||
| SOMT120416 | 1.6 | 33.1 | 45.3 | 0.5 | 6.1 | 47.4 |
R/
T-Slot
High-Speed