Каталог Sumitomo фрезы со сменными пластинами - страница 13
Навигация
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo модульные системы для револьверных головок токарных станков
 Каталог Sumitomo токарные резцы (державки) для внутреннего точения
 Общий каталог Sumitomo 2018 - 2019
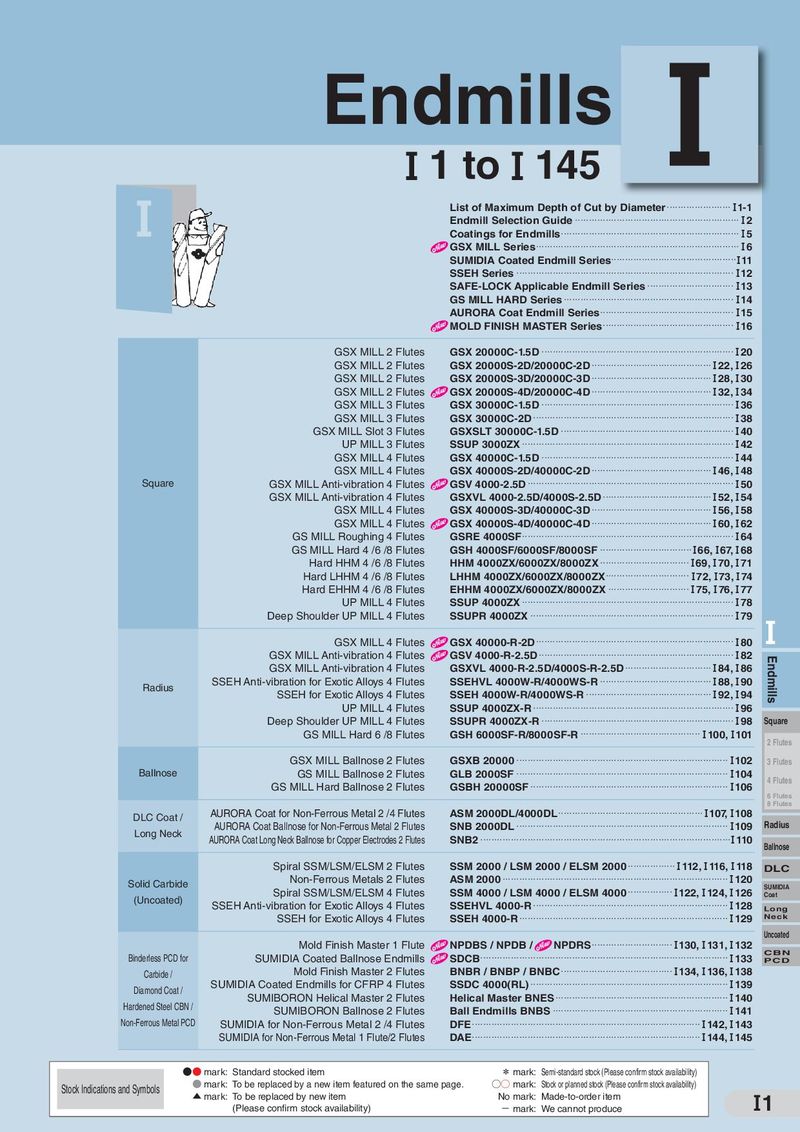 Каталог Sumitomo монолитные фрезы
- H001
- H002
- H003
- H004
- H005
- H006
- H007
- H008
- H009
- H010
- H011
- H012
- H013
- H014
- H015
- H016
- H017
- H018
- H019
- H020
- H021
- H022
- H023
- H024
- H025
- H026
- H027
- H028
- H029
- H030
- H031
- H032
- H033
- H034
- H035
- H036
- H037
- H038
- H039
- H040
- H041
- H042
- H043
- H044
- H045
- H046
- H047
- H048
- H049
- H050
- H051
- H052
- H053
- H054
- H055
- H056
- H057
- H058
- H059
- H060
- H061
- H062
- H063
- H064
- H065
- H066
- H067
- H068
- H069
- H070
- H071
- H072
- H073
- H074
- H075
- H076
- H077
- H078
- H079
- H080
- H081
- H082
- H083
- H084
- H085
- H086
- H087
- H088
- H089
- H090
- H091
- H092
- H093
- H094
- H095
- H096
- H097
- H098
- H099
- H100
- H101
- H102
- H103
- H104
- H105
- H106
- H107
- H108
- H109
- H110
- H111
- H112
- H113
- H114
- H115
- H116
- H117
- H118
- H119
- H120
- H121
- H122
- H123
- H124
- H125
- H126
- H127
- H128
- H129
- H130
- H131
- H132
- H133
- H134
- H135
- H136
- H137
- H138
- H139
- H140
- H141
- H142
- H143
- H144
- H145
- H146
- H147
- H148
- H149
- H150
- H151
- H152
- H153
- H154
- H155
- H156
- H157
- H158
- H159
- H160
- H161
- H162
- H163
- H164
- H165
- H166
- H167
- H168
- H169
- H170
- H171
- H172
- H173
- H174
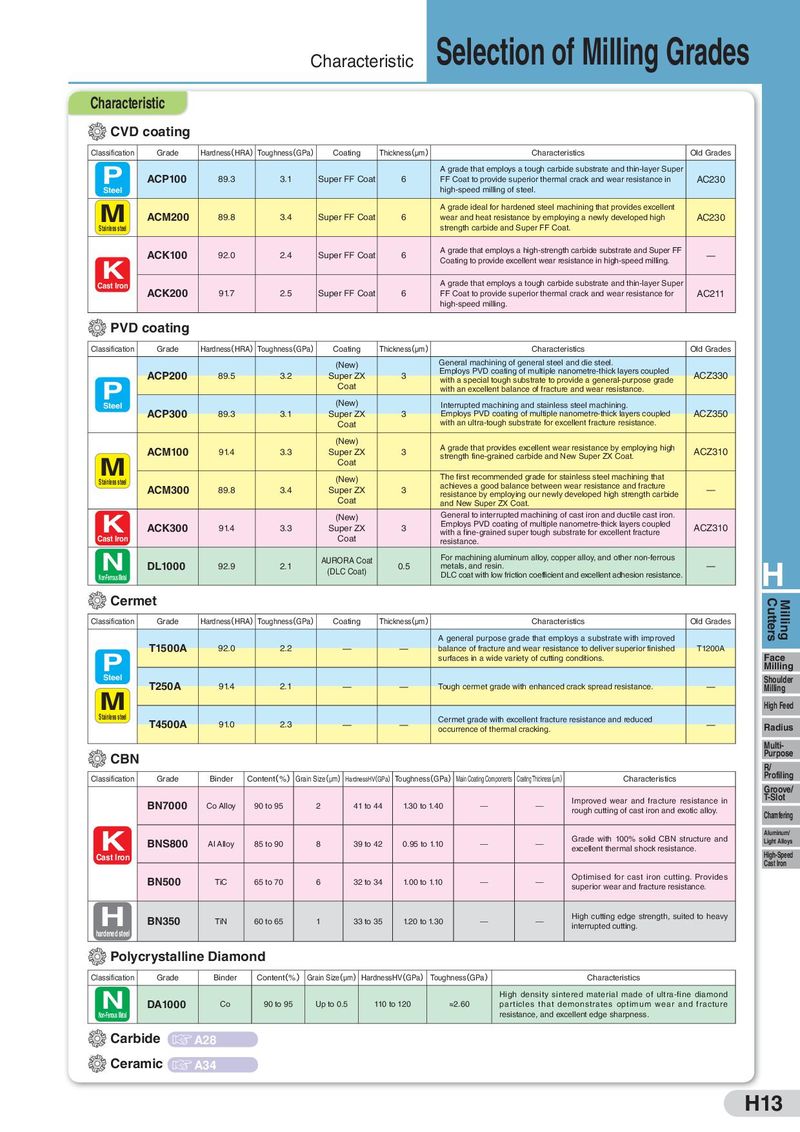
Characteristic
CVD coating
Selection of Milling Grades
Characteristic
| Classification | Grade | Hardness`(`HR | A`)`Toughness`(`GP | a`)` Coating Thi | ckness`(`μm | `)` Charac | teristics | Old Grades |
| P Steel | ACP100 | 89.3 | 3.1 | Super FF Coat | 6 | A grade that employs a tough car FF Coat to provide superior ther high-speed milling of steel. | bide substrate and thin-layer Super mal crack and wear resistance in | AC230 |
| M Stainless steel | ACM200 | 89.8 | 3.4 | Super FF Coat | 6 | A grade ideal for hardened steel wear and heat resistance by emp strength carbide and Super FF C | machining that provides excellent loying a newly developed high oat. | AC230 |
| K | ACK100 | 92.0 | 2.4 | Super FF Coat | 6 | A grade that employs a high-stren Coating to provide excellent wear | gth carbide substrate and Super FF resistance in high-speed milling. | |
| Cast Iron PVD | ACK200 coating | 91.7 | 2.5 | Super FF Coat | 6 | A grade that employs a tough car FF Coat to provide superior ther high-speed milling. | bide substrate and thin-layer Super mal crack and wear resistance for | AC211 |
| Classification | Grade | Hardness`(`HR | A`)`Toughness`(`GP | a`)` Coating Thi | ckness`(`μm | `)` Charac | teristics | Old Grades |
| P | ACP200 | 89.5 | 3.2 | (New) Super ZX Coat | 3 | General machining of general ste Employs PVD coating of multiple with a special tough substrate to with an excellent balance of fract | el and die steel. nanometre-thick layers coupled provide a general-purpose grade ure and wear resistance. | ACZ330 |
| Steel | ACP300 | 89.3 | 3.1 | (New) Super ZX Coat | 3 | Interrupted machining and stainl Employs PVD coating of multiple with an ultra-tough substrate for e | ess steel machining. nanometre-thick layers coupled xcellent fracture resistance. | ACZ350 |
| M | ACM100 | 91.4 | 3.3 | (New) Super ZX Coat | 3 | A grade that provides excellent w strength fine-grained carbide and | ear resistance by employing high New Super ZX Coat. | ACZ310 |
| Stainless steel | ACM300 | 89.8 | 3.4 | (New) Super ZX Coat | 3 | The first recommended grade for achieves a good balance betwee resistance by employing our new and New Super ZX Coat. | stainless steel machining that n wear resistance and fracture ly developed high strength carbide | |
| K Cast Iron | ACK300 | 91.4 | 3.3 | (New) Super ZX Coat | 3 | General to interrupted machining Employs PVD coating of multiple with a fine-grained super tough s resistance. | of cast iron and ductile cast iron. nanometre-thick layers coupled ubstrate for excellent fracture | ACZ310 |
| N | DL1000 | 92.9 | 2.1 | AURORA Coat (DLC Coat) | 0.5 | For machining aluminum alloy, co metals, and resin. DLC coat with low friction coefficie | pper alloy, and other non-ferrous t and excellent adhesion resistance | |
| Non-Ferrous Metal Cer | met | . | ||||||
| Classification | Grade | Hardness`(`HR | A`)`Toughness`(`GP | a`)` Coating Thi | ckness`(`μm | `)` Charac A general purpose grade that em | teristics ploys a substrate with improved | Old Grades |
| P | T1500A | 92.0 | 2.2 | balance of fracture and wear resis surfaces in a wide variety of cuttin | tance to deliver superior finished g conditions. | T1200A | ||
| Steel M | T250A | 91.4 | 2.1 | Tough cermet grade with enhance | d crack spread resistance. | |||
| Stainless steel CBN | T4500A | 91.0 | 2.3 | Cermet grade with excellent fract occurrence of thermal cracking. | ure resistance and reduced | |||
| Classification | Grade | Binder | Content`(`%`)`Gra | in Size`(`μm`)`HardnessHV`(`GPa | `)`Toughnes | s`(`GPa`)`Main Coating Components Coating Thickness`(`μ | m`)` Characteristics | |
| BN7000 | Co Alloy | 90 to 95 | 2 41 to 44 | 1.30 to | 1.40 | Improved wear and fracture re rough cutting of cast iron and ex | sistance in otic alloy. | |
| K Cast Iron | BNS800 | Al Alloy | 85 to 90 | 8 39 to 42 | 0.95 to | 1.10 | Grade with 100% solid CBN st excellent thermal shock resistan | ructure and ce. |
| BN500 | TiC | 65 to 70 | 6 32 to 34 | 1.00 to | 1.10 | Optimised for cast iron cuttin superior wear and fracture resis | g. Provides tance. | |
| H | BN350 | TiN | 60 to 65 | 1 33 to 35 | 1.20 to | 1.30 | High cutting edge strength, suit interrupted cutting. | ed to heavy |
| hardened steel Poly | crystallin | e Diamo | nd | |||||
| Classification | Grade | Binder | Content`(`%`)` | Grain Size`(`μm`)`Hardnes | sHV`(`GPa`)` | Toughness`(`GPa`)` | Characteristics | |
| N | DA1000 | Co | 90 to 95 | U to 05 110 | to 120 | ≈260 High density s articles that | ntered material made of ultra-fin demonstrates otimum wear a | e diamond d fracture |
| Non-Ferrous Metal | p . | . p resistance, and | p excellent edge sharpness. | |||||
| Cera Carb | mic ide A A | 28 34 |
Milling
High Feed
Multi- R/ Groove/ T-Slot
Cast Iron