Каталог Sumitomo фрезы со сменными пластинами - страница 134
Навигация
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo модульные системы для револьверных головок токарных станков
 Каталог Sumitomo токарные резцы (державки) для внутреннего точения
 Общий каталог Sumitomo 2018 - 2019
 Каталог Sumitomo монолитные фрезы
- H001
- H002
- H003
- H004
- H005
- H006
- H007
- H008
- H009
- H010
- H011
- H012
- H013
- H014
- H015
- H016
- H017
- H018
- H019
- H020
- H021
- H022
- H023
- H024
- H025
- H026
- H027
- H028
- H029
- H030
- H031
- H032
- H033
- H034
- H035
- H036
- H037
- H038
- H039
- H040
- H041
- H042
- H043
- H044
- H045
- H046
- H047
- H048
- H049
- H050
- H051
- H052
- H053
- H054
- H055
- H056
- H057
- H058
- H059
- H060
- H061
- H062
- H063
- H064
- H065
- H066
- H067
- H068
- H069
- H070
- H071
- H072
- H073
- H074
- H075
- H076
- H077
- H078
- H079
- H080
- H081
- H082
- H083
- H084
- H085
- H086
- H087
- H088
- H089
- H090
- H091
- H092
- H093
- H094
- H095
- H096
- H097
- H098
- H099
- H100
- H101
- H102
- H103
- H104
- H105
- H106
- H107
- H108
- H109
- H110
- H111
- H112
- H113
- H114
- H115
- H116
- H117
- H118
- H119
- H120
- H121
- H122
- H123
- H124
- H125
- H126
- H127
- H128
- H129
- H130
- H131
- H132
- H133
- H134
- H135
- H136
- H137
- H138
- H139
- H140
- H141
- H142
- H143
- H144
- H145
- H146
- H147
- H148
- H149
- H150
- H151
- H152
- H153
- H154
- H155
- H156
- H157
- H158
- H159
- H160
- H161
- H162
- H163
- H164
- H165
- H166
- H167
- H168
- H169
- H170
- H171
- H172
- H173
- H174
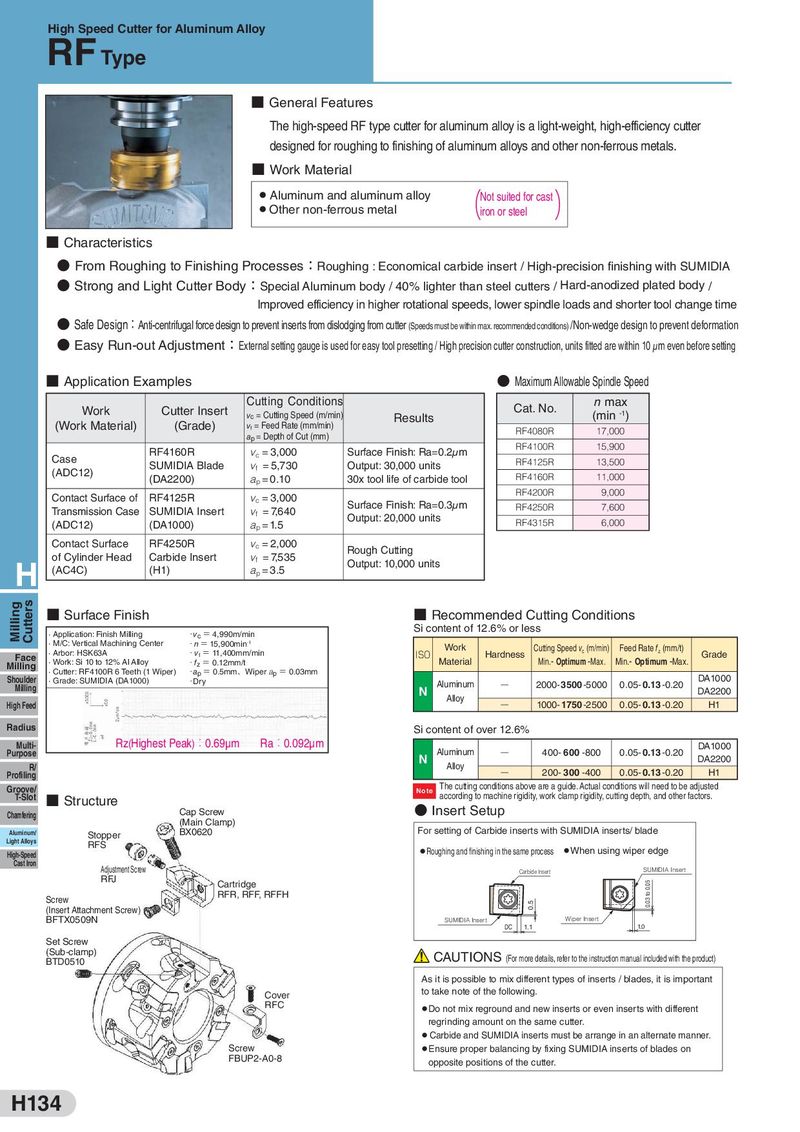
RFHigh Speed Cutter for Aluminum Alloy
- General Features The high-speed RF type cutter for aluminum alloy is a light-weight, high-efficiency cutter designed for roughing to finishing of aluminum alloys and other non-ferrous metals.
- Work Material
- Aluminum and aluminum alloy Not suited for cast
- Other non-ferrous metal iron or steel
- Characteristics
- From Roughing to Finishing Processes:Roughing : Economical carbide insert / High-precision finishing with SUMIDIA
- Strong and Light Cutter Body:
Special Aluminum body / 40% lighter than steel cutters / Hard-anodized plated body /
Improved efficiency in higher rotational speeds, lower spindle loads and shorter tool change time
- Safe Design: Anti-centrifugal force design to prevent inserts from dislodging from cutter /Non-wedge design to prevent deformation
(Speeds must be within max. recommended conditions)
- Easy Run-out Adjustment:
External setting gauge is used for easy tool presetting / High precision cutter construction, units fitted are within 10 μm even before setting
- Application Examples Maximum Allowable Spindle Speed
| Work (Work Material) | Cutter Insert (Grade) | Cutting Conditions vc= Cutting Speed (m/min) vf= Feed Rate (mm/min) ap= Depth of Cut(mm) | Results | Cat. No. RF4080R | nmax (min-1) 17,000 |
| Case (ADC12) | RF4160R SUMIDIA Blade | vc= 3,000 vf= 5,730 | Surface Finish: Ra=0.2μm Output: 30,000 units | RF4100R RF4125R | 15,900 13,500 |
| (DA2200) | ap= 0.10 | 30x tool life of carbide tool | RF4160R | 11,000 | |
| Contact Surface of Transmission Case | RF4125R SUMIDIA Insert | vc= 3,000 vf= 7,640 | Surface Finish: Ra=0.3μm O 2 i | RF4200R RF4250R | 9,000 7,600 |
| (ADC12) | (DA1000) | ap= 1.5 | utput: 0,000 unts | RF4315R | 6,000 |
| Contact Surface of Cylinder Head (AC4C) | RF4250R Carbide Insert (H1) | vc= 2,000 vf= 7,535 ap= 3.5 | Rough Cutting Output: 10,000 units |
- Surface Finish
- Recommended Cutting Conditions Si content of 12.6% or less
Application: Finish Milling ・v = 4,990m/min
c
- M/C: Vertical Machining Center ・n= 15,900min-1
・ = ISO Work Cutting Speed v (m/min) Feed Rate f (mm/t)
| · Arbor: HSK63A | v 11,400mm/min | Hardness | c | z Grade | ||||
| Face | ・ f = | - | - - | - | ||||
| · Work: Si 10 to 12% Al Alloy | f 0.12mm/t | Material | Min. Optimum | Min. Optimum Max. | Max. | |||
| Milling | z | |||||||
| · Cutter: RF4100R 6 Teeth (1 Wiper) | ・a = 0.5mm、Wiper a | = 0.03mm | ||||||
| p | p | |||||||
| Shoulder | · Grade: SUMIDIA (DA1000) | ・Dry | Q | DA1000 | ||||
| Milling | Aluminum | 2000-3500-5000 | 0.05-0.13 -0.20 | |||||
| N | DA2200 | |||||||
| Alloy | Q | |||||||
| High Feed | 1000-1750 -2500 | 0.05-0.13 -0.20 | H1 | |||||
| Radius | Si content of over 12.6% | |||||||
| Rz(Highest Peak):0.69μm | Ra:0.092μm | |||||||
| Multi- | Q | DA1000 | ||||||
| Purpose | Aluminum | 400- 600 -800 | 0.05-0.13 -0.20 | |||||
| N | DA2200 | |||||||
| R/ | Alloy | Q | ||||||
| Profiling | 200- 300 -400 | 0.05-0.13 -0.20 | H1 | |||||
| Groove/ | The cutting conditions above are a guide. Actual conditions will need to be adjusted | |||||||
| ■ | Note | according to machine rigidity, work clamp rigidity, cutting depth, and other factors. |
T-Slot Structure
- Insert Setup
Chamfering Cap Screw (Main Clamp) BX0620 For setting of Carbide inserts with SUMIDIA inserts/ blade Aluminum/ Stopper Light Alloys RFS
- Roughing and finishing in the same process
- When using wiper edge
High-Speed Cast Iron Adjustment Screw SUMIDIA Insert Carbide Insert RFJ Cartridge RFR, RFF, RFFH Screw (Insert Attachment Screw)
BFTX0509N SUMIDIA Insert Wiper Insert
DC 1.1 1.0
Set Screw (Sub-clamp) CAUTIONS BTD0510 (For more details, refer to the instruction manual included with the product) As it is possible to mix different types of inserts / blades, it is important
Cover to take note of the following. RFC
- Do not mix reground and new inserts or even inserts with different regrinding amount on the same cutter.
- Carbide and SUMIDIA inserts must be arrange in an alternate manner.
Screw Ensure proper balancing by fixing SUMIDIA inserts of blades on FBUP2-A0-8 opposite positions of the cutter.