Каталог Sumitomo фрезы со сменными пластинами - страница 108
Навигация
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo модульные системы для револьверных головок токарных станков
 Каталог Sumitomo токарные резцы (державки) для внутреннего точения
 Общий каталог Sumitomo 2018 - 2019
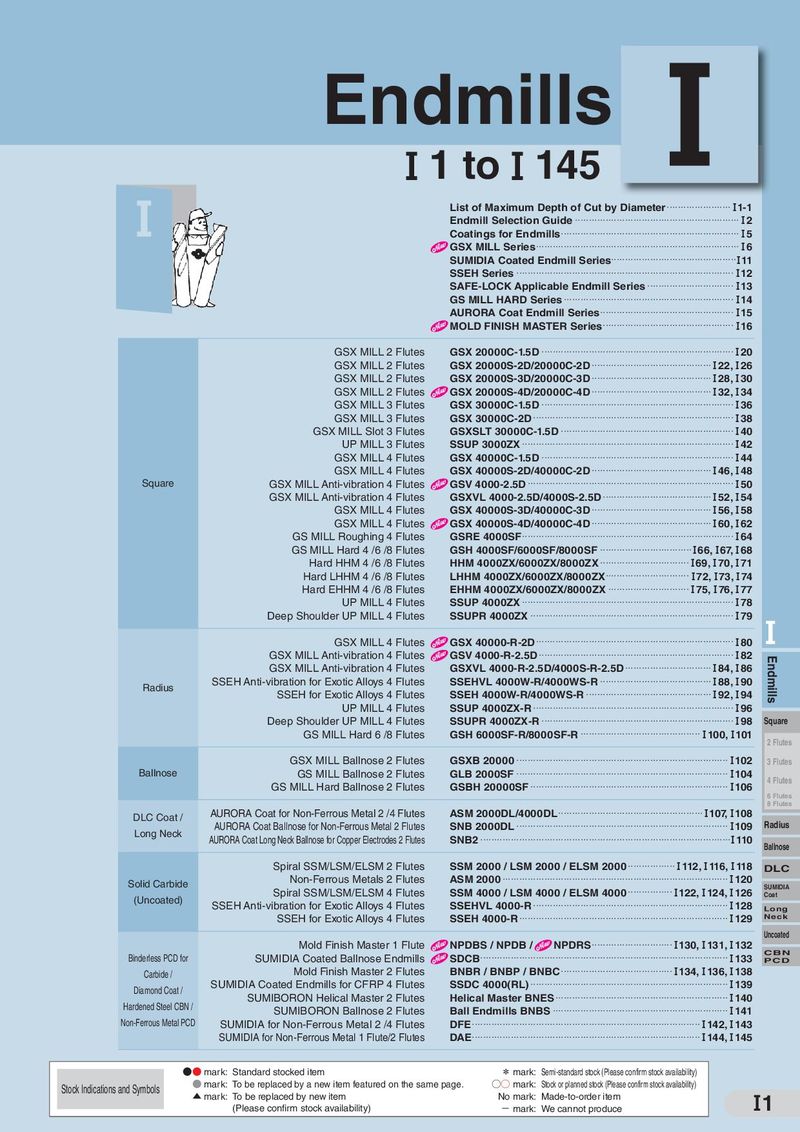 Каталог Sumitomo монолитные фрезы
- H001
- H002
- H003
- H004
- H005
- H006
- H007
- H008
- H009
- H010
- H011
- H012
- H013
- H014
- H015
- H016
- H017
- H018
- H019
- H020
- H021
- H022
- H023
- H024
- H025
- H026
- H027
- H028
- H029
- H030
- H031
- H032
- H033
- H034
- H035
- H036
- H037
- H038
- H039
- H040
- H041
- H042
- H043
- H044
- H045
- H046
- H047
- H048
- H049
- H050
- H051
- H052
- H053
- H054
- H055
- H056
- H057
- H058
- H059
- H060
- H061
- H062
- H063
- H064
- H065
- H066
- H067
- H068
- H069
- H070
- H071
- H072
- H073
- H074
- H075
- H076
- H077
- H078
- H079
- H080
- H081
- H082
- H083
- H084
- H085
- H086
- H087
- H088
- H089
- H090
- H091
- H092
- H093
- H094
- H095
- H096
- H097
- H098
- H099
- H100
- H101
- H102
- H103
- H104
- H105
- H106
- H107
- H108
- H109
- H110
- H111
- H112
- H113
- H114
- H115
- H116
- H117
- H118
- H119
- H120
- H121
- H122
- H123
- H124
- H125
- H126
- H127
- H128
- H129
- H130
- H131
- H132
- H133
- H134
- H135
- H136
- H137
- H138
- H139
- H140
- H141
- H142
- H143
- H144
- H145
- H146
- H147
- H148
- H149
- H150
- H151
- H152
- H153
- H154
- H155
- H156
- H157
- H158
- H159
- H160
- H161
- H162
- H163
- H164
- H165
- H166
- H167
- H168
- H169
- H170
- H171
- H172
- H173
- H174
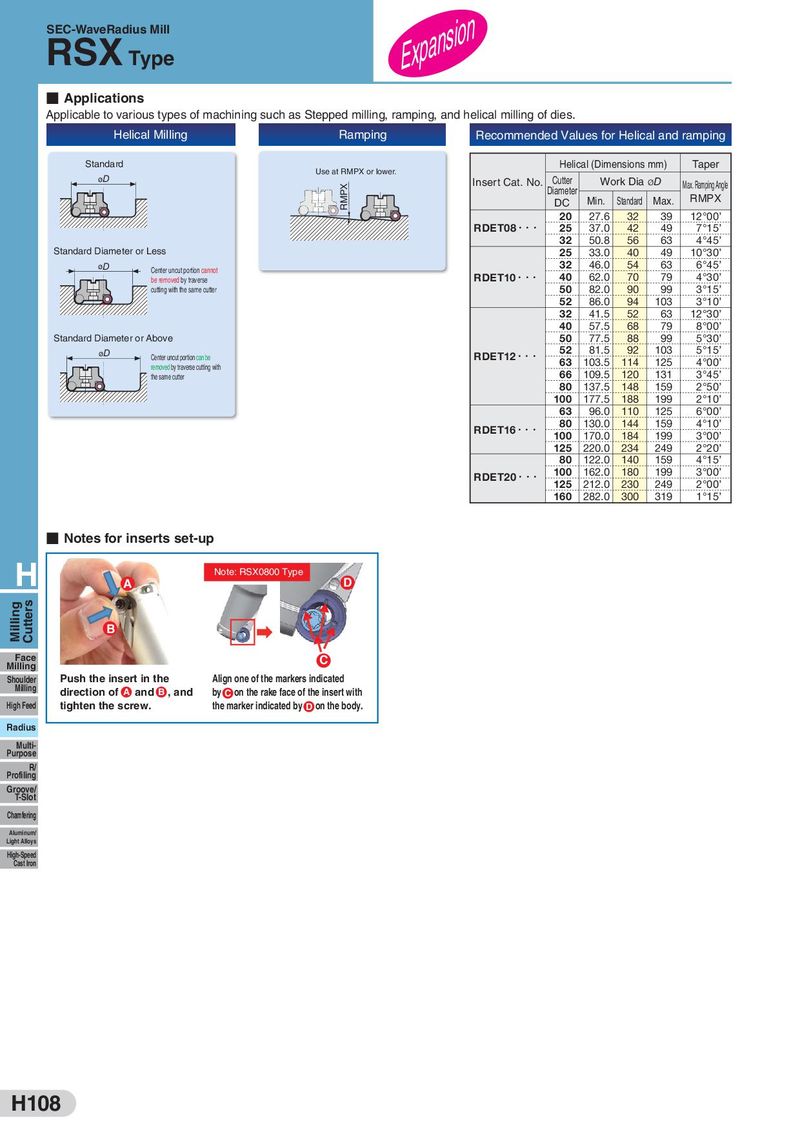
- Applications
Applicable to various types of machining such as Stepped milling, ramping, and helical milling of dies.
Helical Milling Ramping Recommended Values for Helical and ramping
| Helic | al(Dim | ensions | mm) | Taper | |
| Insert Cat. No. | Cutter Diameter | Wo | rk Dia | øD | Max. Ramping Angle |
| DC | Min. | Standard | Max. | RMPX | |
| 20 | 27.6 | 32 | 39 | 12°00’ | |
| RDET08`・・・` | 25 | 37.0 | 42 | 49 | 7°15’ |
| 32 | 50.8 | 56 | 63 | 4°45’ | |
| 25 | 33.0 | 40 | 49 | 10°30’ | |
| 32 | 46.0 | 54 | 63 | 6°45’ | |
| RDET10`・・・` | 40 | 62.0 | 70 | 79 | 4°30’ |
| 50 | 82.0 | 90 | 99 | 3°15’ | |
| 52 | 86.0 | 94 | 103 | 3°10’ | |
| 32 | 41.5 | 52 | 63 | 12°30’ | |
| 40 | 57.5 | 68 | 79 | 8°00’ | |
| 50 | 77.5 | 88 | 99 | 5°30’ | |
| RDET12`・・・` | 52 | 81.5 | 92 | 103 | 5°15’ |
| 63 | 103.5 | 114 | 125 | 4°00’ | |
| 66 | 109.5 | 120 | 131 | 3°45’ | |
| 80 | 137.5 | 148 | 159 | 2°50’ | |
| 100 | 177.5 | 188 | 199 | 2°10’ | |
| 63 | 96.0 | 110 | 125 | 6°00’ | |
| RDET16`・・・` | 80 | 130.0 | 144 | 159 | 4°10’ |
| 100 | 170.0 | 184 | 199 | 3°00’ | |
| 125 | 220.0 | 234 | 249 | 2°20’ | |
| 80 | 122.0 | 140 | 159 | 4°15’ | |
| RDET20`・・・` | 100 | 162.0 | 180 | 199 | 3°00’ |
| 125 | 212.0 | 230 | 249 | 2°00’ | |
| 160 | 282.0 | 300 | 319 | 1°15’ |
Use at RMPX or lower.
removed by traverse cutting with
- Notes for inserts set-up
H
Note: RSX0800 Type A D
B Face C Milling
| Shoulder | Push the insert in the | Align one of the markers indicated |
| Milling | ||
| direction of A and B , and | by C on the rake face of the insert with | |
| High Feed | tighten the screw. | the marker indicated by D on the body. |
Radius Multi- Purpose R/
Profiling Groove/ T-Slot Chamfering Aluminum/ Light Alloys High-Speed Cast Iron