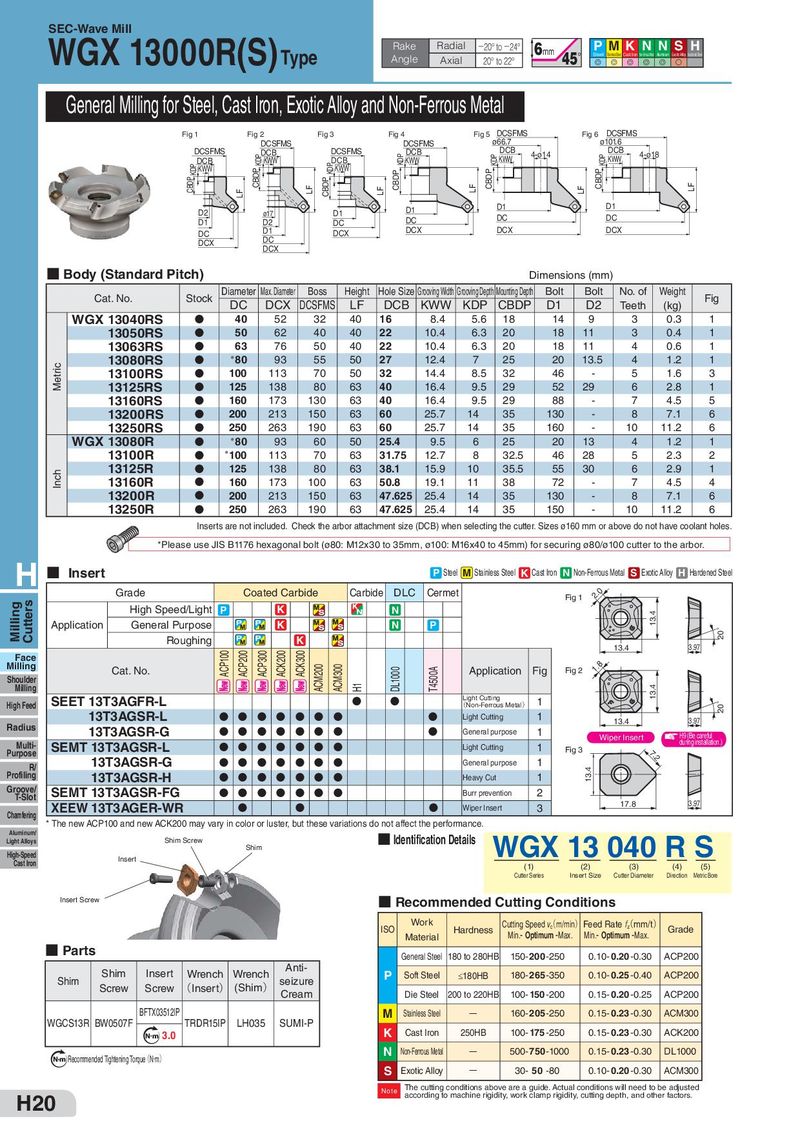
WGX 13000R(S)SEC-Wave Mill
Type mm 45°
| 20° to 22° | G | G | G | G | G | S |
| General Milling for Steel, Cast Iron, Exotic Alloy and Non-Ferrous Metal | | | | | | | |
| Fig 1 | | Fig 2 | | Fig 3 | | Fig 4 | | Fig 5 | DCSFMS | | Fig 6 | DCSFMS | |
| | | DCSFMS | | | | DCSFMS | | ø66.7 | | | ø101.6 | |
| DCSFMS | | DCB | | DCSFMS | | DCB | | DCB | | | DCB | |
| | | | | | | | | | 4-ø14 | | | 4-ø18 |
| DCB | | KWW | | DCB | | KDP KWW | | KWW | | | KWW | |
KWW KWW
DCX DC DCX
| ■ Body ( | Standard P | itch) | | | | | | | | D | imensio | ns(mm | ) | | |
| Ca | t No | Stock | Diameter | Max. Diameter | Boss | Height | Hole Size | GroovingWidth | GroovingDept | MountingDepth | Bolt | Bolt | No. of | Weight | Fi |
| . . | | DC | DCX | DCSFMS | LF | DCB | KWW | KDP | CBDP | D1 | D2 | Teeth | (kg) | g |
| WGX | 13040RS | D | 40 | 52 | 32 | 40 | 16 | 8.4 | 5.6 | 18 | 14 | 9 | 3 | 0.3 | 1 |
| 13050RS | D | 50 | 62 | 40 | 40 | 22 | 10.4 | 6.3 | 20 | 18 | 11 | 3 | 0.4 | 1 |
| 13063RS | D | 63 | 76 | 50 | 40 | 22 | 10.4 | 6.3 | 20 | 18 | 11 | 4 | 0.6 | 1 |
| c | 13080RS | D | `*`80 | 93 | 55 | 50 | 27 | 12.4 | 7 | 25 | 20 | 13.5 | 4 | 1.2 | 1 |
| etri | 13100RS | D | 100 | 113 | 70 | 50 | 32 | 14.4 | 8.5 | 32 | 46 | - | 5 | 1.6 | 3 |
| M | 13125RS | D | 125 | 138 | 80 | 63 | 40 | 16.4 | 9.5 | 29 | 52 | 29 | 6 | 2.8 | 1 |
| 13160RS | D | 160 | 173 | 130 | 63 | 40 | 16.4 | 9.5 | 29 | 88 | - | 7 | 4.5 | 5 |
| 13200RS | D | 200 | 213 | 150 | 63 | 60 | 25.7 | 14 | 35 | 130 | - | 8 | 7.1 | 6 |
| 13250RS | D | 250 | 263 | 190 | 63 | 60 | 25.7 | 14 | 35 | 160 | - | 10 | 11.2 | 6 |
| WGX | 13080R | D | `*`80 | 93 | 60 | 50 | 25.4 | 9.5 | 6 | 25 | 20 | 13 | 4 | 1.2 | 1 |
| 13100R | D | `*`100 | 113 | 70 | 63 | 31.75 | 12.7 | 8 | 32.5 | 46 | 28 | 5 | 2.3 | 2 |
| h | 13125R | D | 125 | 138 | 80 | 63 | 38.1 | 15.9 | 10 | 35.5 | 55 | 30 | 6 | 2.9 | 1 |
| Inc | 13160R | D | 160 | 173 | 100 | 63 | 50.8 | 19.1 | 11 | 38 | 72 | - | 7 | 4.5 | 4 |
| 13200R | D | 200 | 213 | 150 | 63 | 47.625 | 25.4 | 14 | 35 | 130 | - | 8 | 7.1 | 6 |
| 13250R | D | 250 | 263 | 190 | 63 | 47.625 | 25.4 | 14 | 35 | 150 | - | 10 | 11.2 | 6 |
| | Inser | ts are not i | ncluded. C | heck the ar | bor attac | hment size | (DCB) whe | n selectin | g the cutter. | Sizes ø1 | 60 mm or | above do n | ot have coo | lant holes. |
*Please use JIS B1176 hexagonal bolt (ø80: M12x30 to 35mm, ø100: M16x40 to 45mm) for securing ø80/ø100 cutter to the arbor.
| H | ■ | Insert | |
| | | P Steel M Stainless Steel K Cast Iron N Non-Ferrous Metal S Exotic Alloy H Hardened Steel |
| Grade | Coated Carbide | Carbide | DLC | Cermet | | |
| | | | | Fig 1 | 2.0 |
| High Speed/Light | P K | N |
| Application General Purpose | K | P N |
| | Roughing | K |
| | | 3.97 13.4 |
| Face | | | |
| Milling | | | |
| | Cat. No. | Application | 1.8 Fig 2 Fig |
| Shoulder | | | | |
| Milling | | | | |
| SEET 13T3AGFR-L | | D D Light Cutting | 1 |
| High Feed | | | (Non-Ferrous Metal) | |
| | 13T3AGSR-L DDDDDDD | D Light Cutting | 1 |
| | | | 3.97 13.4 |
| Radius | | 13T3AGSR-G DDDDDDD | D | 1 |
| | | General purpose | H9 (Be careful |
| | | | Wiper Insert |
| Multi- | SEMT 13T3AGSR-L | DDDDDDD | | during installation.) 1 |
| | | Light Cutting | 7.2 Fig 3 |
| Purpose | | DDDDDDD | | |
| | 13T3AGSR-G | General purpose | 1 |
| R/ | | | |
| Profiling | | 13T3AGSR-H DDDDDDD | Heavy Cut | 1 |
| Groove/ | SEMT 13T3AGSR-FG | DDDDDDD | | 2 |
| T-Slot | | | Burr prevention | |
| XEEW 13T3AGER-WR | | D D D | 3.97 17.8 3 |
| | | Wiper Insert | |
| Chamfering | | | | |
| * The new ACP100 and new ACK200 may vary in color or luster, but these variations do not affect the performance. | | | |
| Aluminum/ | | | | ■ Identification Details | WGX 13 040 R S |
| Light Alloys | | Shim Screw | | | |
| | | Shim | | |
| High-Speed | | | | | |
| Cast Iron | Insert | | | | |
| | | | | | (1) | | (2) | | (3) | (4) | (5) |
| | | | | | Cutter Series | | Insert Size | Cutter Diameter | | Direction | Metric Bore |
| Insert Screw | | Recommended Cutting Conditions | | | | | | | | | | |
| | | Work | | Cutting Speed v(m/min) Feed Rate f(mm/t) | | | | | | | |
| ISO | | | Hardness | | | c | | | z | Grade | |
Material Min.- Optimum -Max. Min.- Optimum -Max.
| | | | | | General Steel 180 to 280HB | | 150-200-250 | 0.10- 0.20 -0.30 | ACP200 |
| | | | Anti- | | | | | | |
| Shim | Insert | Wrench | Wrench | | P | Soft Steel | ≤180HB | 180-265-350 | 0.10- 0.25 -0.40 | ACP200 |
Shim ( ) ) seizure
Screw Screw Insert (Shim
| Cream | | Die Steel 200 to 220HB | | 100- 150-200 | 0.15-0.20 -0.25 | ACP200 |
| BFTX03512IP | | M | Stainless Steel | − | 160-205-250 | 0.15-0.23 -0.30 | ACM300 |
WGCS13R BW0507F TRDR15IP LH035 SUMI-P
| 3.0 | K | Cast Iron | 250HB | 100- 175-250 | 0.15-0.23 -0.30 | ACK200 |
| | N | Non-Ferrous Metal | − | 500-750-1000 | 0.15-0.23 -0.30 | DL1000 |
| N m Recommended Tightening Torque | | | | | | | |
| | S | Exotic Alloy | − | 30- 50 -80 | 0.10- 0.20 -0.30 | ACM300 |
H20H20 depth, and other factors.
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo модульные системы для револьверных головок токарных станков
 Каталог Sumitomo токарные резцы (державки) для внутреннего точения
 Общий каталог Sumitomo 2018 - 2019
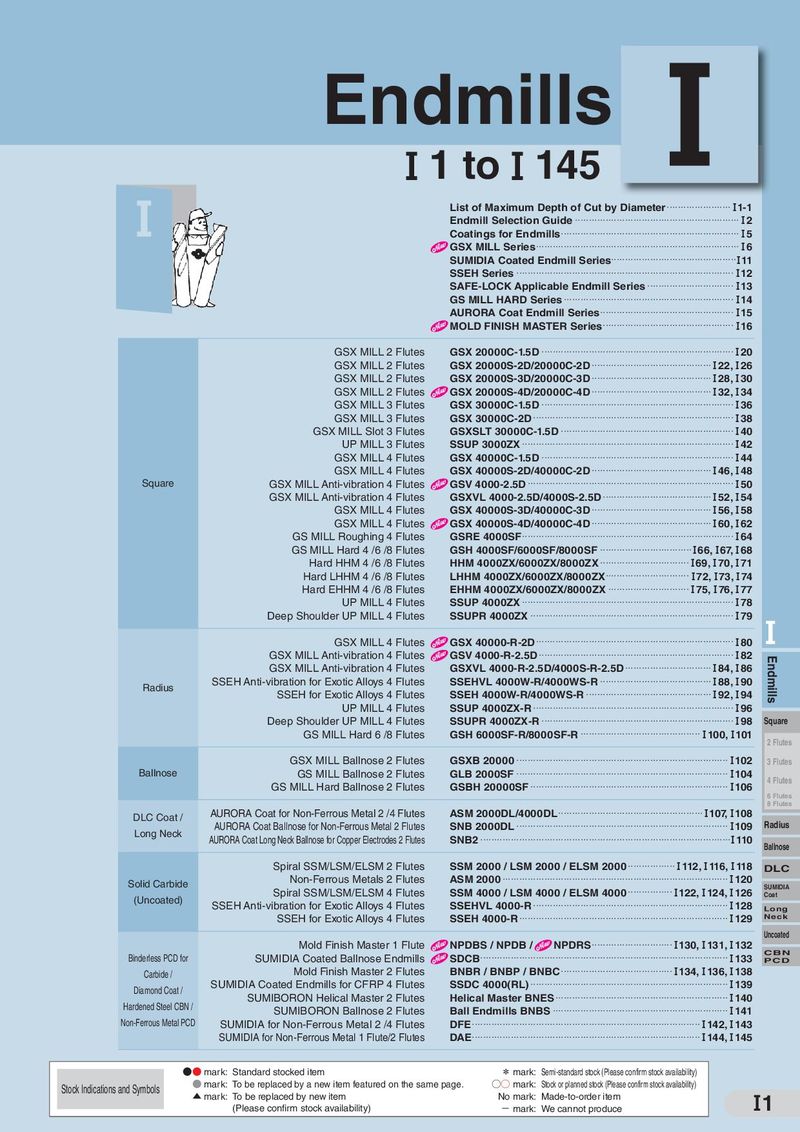 Каталог Sumitomo монолитные фрезы