| Type | Radial | −5° | 6 | P M K N N S H |
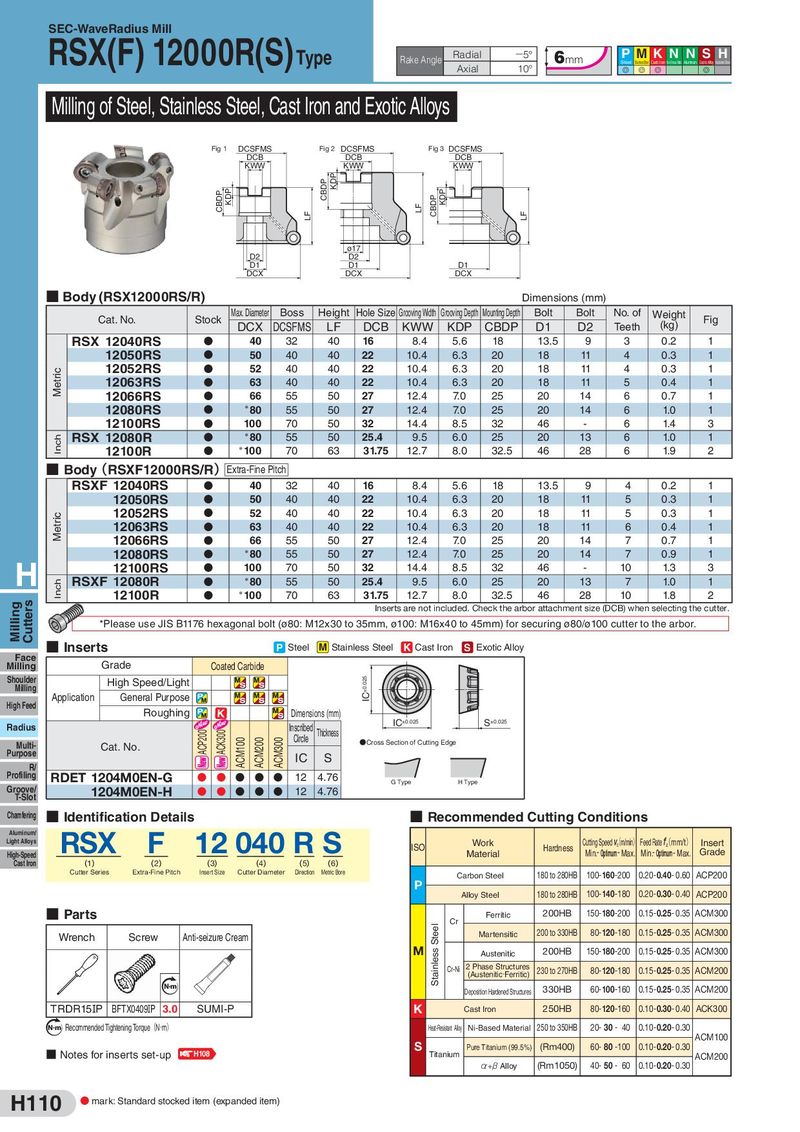
| Milling of Steel, Stainless Steel, Cast Iron and Exotic Alloys | | | | | |
| Fig 1 | DCSFMS | Fig 2 | DCSFMS | Fig 3 | DCSFMS |
| DCB | | DCB | | DCB |
| KWW | | KWW | | KWW |
ø17 D2 D2
| ■ Body (RSX12000R | /R) | | | | | | | | Dimensio | ns(mm | ) | | |
| Ct N | Stk | Max. Diameter | Boss | Height | Hole Size | GroovingWidth | GroovingDepth | MountingDepth | Bolt | Bolt | No. of | Weight | Fi |
| a. o. | oc | DCX | DCSFMS | LF | DCB | KWW | KDP | CBDP | D1 | D2 | Teeth | (kg) | g |
| RSX 12040RS | D | 40 | 32 | 40 | 16 | 8.4 | 5.6 | 18 | 13.5 | 9 | 3 | 0.2 | 1 |
| 12050RS | D | 50 | 40 | 40 | 22 | 10.4 | 6.3 | 20 | 18 | 11 | 4 | 0.3 | 1 |
| ic 12052RS | D | 52 | 40 | 40 | 22 | 10.4 | 6.3 | 20 | 18 | 11 | 4 | 0.3 | 1 |
| etr 12063RS | D | 63 | 40 | 40 | 22 | 10.4 | 6.3 | 20 | 18 | 11 | 5 | 0.4 | 1 |
| M 12066RS | D | 66 | 55 | 50 | 27 | 12.4 | 7.0 | 25 | 20 | 14 | 6 | 0.7 | 1 |
| 12080RS | D | `*`80 | 55 | 50 | 27 | 12.4 | 7.0 | 25 | 20 | 14 | 6 | 1.0 | 1 |
| 12100RS | D | 100 | 70 | 50 | 32 | 14.4 | 8.5 | 32 | 46 | - | 6 | 1.4 | 3 |
| ch RSX 12080R | D | `*`80 | 55 | 50 | 25.4 | 9.5 | 6.0 | 25 | 20 | 13 | 6 | 1.0 | 1 |
| In 12100R | D | `*`100 | 70 | 63 | 31.75 | 12.7 | 8.0 | 32.5 | 46 | 28 | 6 | 1.9 | 2 |
| ■ Body (RSXF12000 | RS/R) | Extra-Fine P | itch | | | | | | | | | | |
| RSXF 12040RS | D | 40 | 32 | 40 | 16 | 8.4 | 5.6 | 18 | 13.5 | 9 | 4 | 0.2 | 1 |
| 12050RS | D | 50 | 40 | 40 | 22 | 10.4 | 6.3 | 20 | 18 | 11 | 5 | 0.3 | 1 |
| ic 12052RS | D | 52 | 40 | 40 | 22 | 10.4 | 6.3 | 20 | 18 | 11 | 5 | 0.3 | 1 |
| etr 12063RS | D | 63 | 40 | 40 | 22 | 10.4 | 6.3 | 20 | 18 | 11 | 6 | 0.4 | 1 |
| M 12066RS | D | 66 | 55 | 50 | 27 | 12.4 | 7.0 | 25 | 20 | 14 | 7 | 0.7 | 1 |
| 12080RS | D | `*`80 | 55 | 50 | 27 | 12.4 | 7.0 | 25 | 20 | 14 | 7 | 0.9 | 1 |
| 12100RS | D | 100 | 70 | 50 | 32 | 14.4 | 8.5 | 32 | 46 | - | 10 | 1.3 | 3 |
| ch RSXF 12080R | D | `*`80 | 55 | 50 | 25.4 | 9.5 | 6.0 | 25 | 20 | 13 | 7 | 1.0 | 1 |
| In 12100R | D | `*`100 | 70 | 63 | 31.75 | 12.7 | 8.0 | 32.5 | 46 | 28 | 10 | 1.8 | 2 |
| | | | | Insert | s are not in | cluded. C | heck the arb | or attachm | ent size ( | DCB) whe | n selecting t | he cutter. |
| Please use JIS B | 1176 hex | agonal bo | lt (ø80: M | 12x30 to | 35mm, ø | 100: M16 | x40 to 4 | 5mm) for s | ecuring | ø80/ø10 | 0 cutter t | o the arbor | . |
| P Steel M Stainless Steel K Cast Iron | S | Exotic Alloy |
| Face | | | |
| Milling | | Grade | | Coated Carbide |
| Shoulder | | High Speed/Light | | |
| Milling | | | | |
| Application | | General Purpose | |
| High Feed | | | | |
Roughing K Dimensions (mm)
| Inscribed | | | IC±0.025 | S±0.025 |
| Radius | | Thickness | | | |
| Circle | | ● | | |
Multi- Cat. No. Cross Section of Cutting Edge
| Profiling | RDET 1204M0EN-G | | D | D | D | D | D | 12 | 4.76 | | | |
| | | D | D | D | D | D | | | G Type | | H Type |
| Groove/ | | 1204M0EN-H | | | | | | 12 | 4.76 | | | |
| T-Slot | | | | | | | | | | | | |
| Chamfering | ■ Identification Details | | | | | | | | | | ■ Recommended Cutting Conditions | |
| Aluminum/ | RSX | F | 12 040 R S | | | ( | ) | ( | ) | |
| Light Alloys | | | | Work | Cutting Speed m/min | | Feed Rate | mm/t | | Insert |
ISO Hardness - -c - z -
High-Speed Material Min. Optimum Max. Min. Optimum Max. Grade
Cast Iron (1) (2) (3) (4) (5) (6)
| Cutter Series | Extra-Fine Pitch | Insert Size | Cutter Diameter | Direction | Metric Bore | | Carbon Steel | 180 to 280HB | 100-160-200 | 0.20-0.40-0.60 | ACP200 |
| | | | | | P | | | | | |
| | | | | | | | 180 to 280HB | 100-140-180 | 0.20-0.30-0.40 | ACP200 |
| | | | | | | Alloy Steel | | | | |
Parts - - - -
| Ferritic | 200HB | 150 180 200 | 0.15 0.25 0.35 | ACM300 |
| Cr | | | | | |
| | 200 to 330HB | 80-120-180 | 0.15-0.25-0.35 | ACM300 |
Wrench Screw Anti-seizure Cream Martensitic
| | M | | 200HB | 150-180-200 | 0.15-0.25-0.35 | ACM300 |
| | | | Austenitic | | | |
| | | Cr-Ni 2 Phase Structures | 230 to 270HB | 80-120-180 | 0.15-0.25-0.35 | ACM200 |
| | | (Austenitic・Ferritic) | | | | |
| N m | | | 330HB | 60-100-160 | 0.15-0.25-0.35 | ACM200 |
| | | Deposition Hardened Structures | | | | |
| TRDR15IP BFTX0409IP | 3.0 | SUMI-P K | Cast Iron | 250HB | 80-120-160 | 0.10-0.30-0.40 | ACK300 |
| Recommended Tightening Torque(N・m) | | | 250 to 350HB | 20- 30 - 40 | 0.10-0.20-0.30 | |
| N m | | | Heat-Resistant Alloy Ni-Based Material | | | | |
Notes for inserts set-up H108 Titanium ACM200
H110 ● mark: Standard stocked item (expanded item)
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo модульные системы для револьверных головок токарных станков
 Каталог Sumitomo токарные резцы (державки) для внутреннего точения
 Общий каталог Sumitomo 2018 - 2019
 Каталог Sumitomo монолитные фрезы