Каталог Sumitomo фрезы со сменными пластинами - страница 45
Навигация
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo модульные системы для револьверных головок токарных станков
 Каталог Sumitomo токарные резцы (державки) для внутреннего точения
 Общий каталог Sumitomo 2018 - 2019
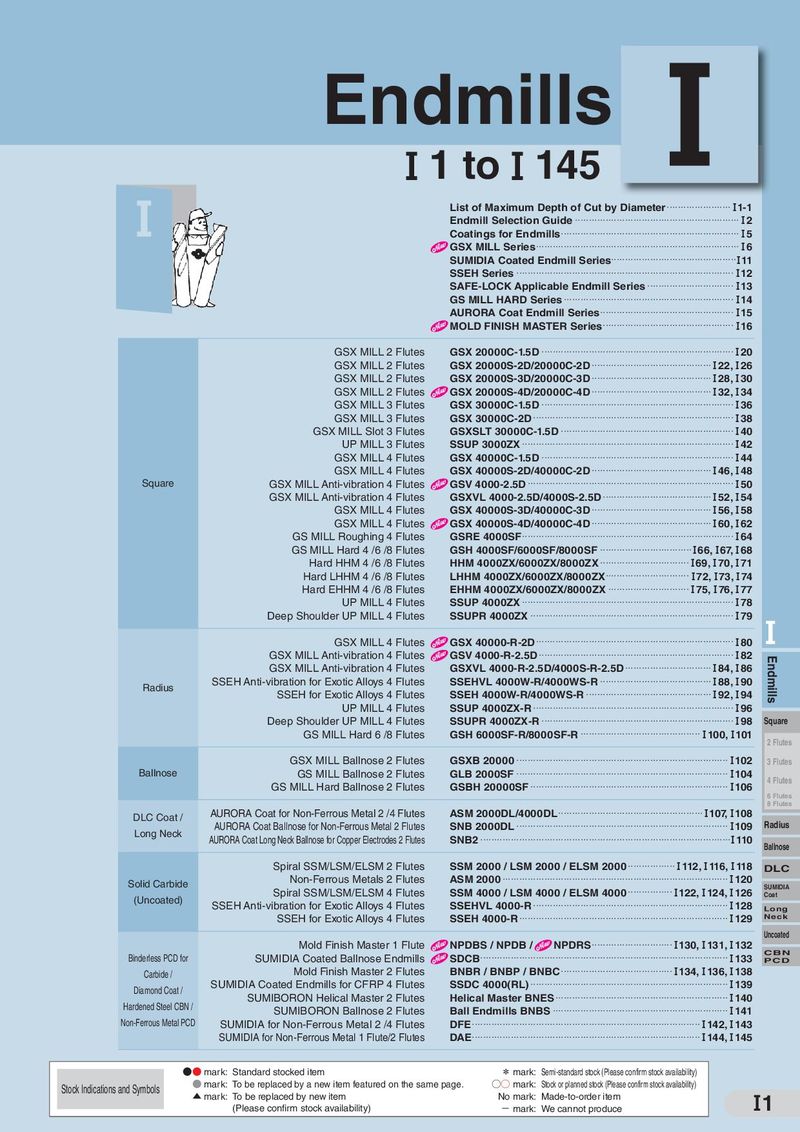 Каталог Sumitomo монолитные фрезы
- H001
- H002
- H003
- H004
- H005
- H006
- H007
- H008
- H009
- H010
- H011
- H012
- H013
- H014
- H015
- H016
- H017
- H018
- H019
- H020
- H021
- H022
- H023
- H024
- H025
- H026
- H027
- H028
- H029
- H030
- H031
- H032
- H033
- H034
- H035
- H036
- H037
- H038
- H039
- H040
- H041
- H042
- H043
- H044
- H045
- H046
- H047
- H048
- H049
- H050
- H051
- H052
- H053
- H054
- H055
- H056
- H057
- H058
- H059
- H060
- H061
- H062
- H063
- H064
- H065
- H066
- H067
- H068
- H069
- H070
- H071
- H072
- H073
- H074
- H075
- H076
- H077
- H078
- H079
- H080
- H081
- H082
- H083
- H084
- H085
- H086
- H087
- H088
- H089
- H090
- H091
- H092
- H093
- H094
- H095
- H096
- H097
- H098
- H099
- H100
- H101
- H102
- H103
- H104
- H105
- H106
- H107
- H108
- H109
- H110
- H111
- H112
- H113
- H114
- H115
- H116
- H117
- H118
- H119
- H120
- H121
- H122
- H123
- H124
- H125
- H126
- H127
- H128
- H129
- H130
- H131
- H132
- H133
- H134
- H135
- H136
- H137
- H138
- H139
- H140
- H141
- H142
- H143
- H144
- H145
- H146
- H147
- H148
- H149
- H150
- H151
- H152
- H153
- H154
- H155
- H156
- H157
- H158
- H159
- H160
- H161
- H162
- H163
- H164
- H165
- H166
- H167
- H168
- H169
- H170
- H171
- H172
- H173
- H174
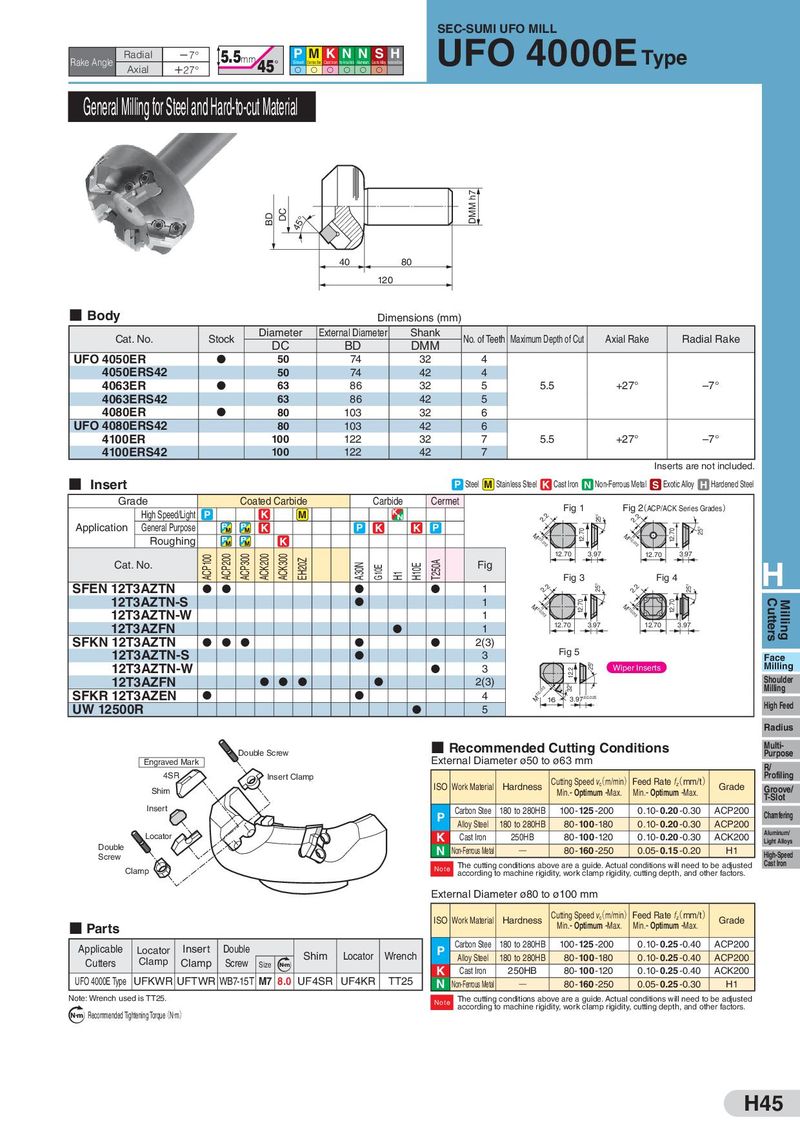
UFO 4000ESEC-SUMI UFO MILL
| Radial | 㸫7° | 5.5 | P M K N N S H | Type | ||
| Rake Angle | mm45° |
Axial 㸩27° S S S S S S
General Milling for Steel and Hard-to-cut Material
45°
40 80 120
| Body | Dim | ensions(m | m) | |||||
| Cat. No. | Stock | Diameter DC | External Diameter BD | Shank DMM | No. of Teeth | Maximum Depth of Cut | Axial Rake | Radial Rake |
| UFO 4050ER | D | 50 | 74 | 32 | 4 | |||
| 4050ERS42 | 50 | 74 | 42 | 4 | ||||
| 4063ER | D | 63 | 86 | 32 | 5 | 5.5 | +27° | –7° |
| 4063ERS42 | 63 | 86 | 42 | 5 | ||||
| 4080ER | D | 80 | 103 | 32 | 6 | |||
| UFO 4080ERS42 | 80 | 103 | 42 | 6 | ||||
| 4100ER | 100 | 122 | 32 | 7 | 5.5 | +27° | –7° | |
| 4100ERS42 | 100 | 122 | 42 | 7 | ||||
| Ins | erts are not included. |
- Insert
P Steel M Stainless Steel K Cast Iron N Non-Ferrous Metal S Exotic Alloy H Hardened Steel
| Grade | Coated Carbide | Carbide | Cermet | ||
| Fig 1 | Fig 2(ACP/ACK Series Grades) |
| High Speed/Light | P | K | M | ||
| 2.2 | 2.2 |
| Application | General Purpose | K | P | K | K | P | ||
| M ± | M ± |
| Roughing | K | 0.0 | 0.0 |
| 13 | 13 |
12.70 3.97 12.70 3.97
| Cat. No. | Fig | H | ||
| Fig 3 | Fig 4 |
| SFEN 12T3AZTN | D D | D | D | 1 | ||||
| 2.2 | 2.2 | |||||||
| 12T3AZTN-S | D | 1 | ||||||
| M ± | M ± | |||||||
| 12T3AZTN-W | 1 | 0.013 | 0.013 |
12T3AZFN D 1 12.70 3.97 12.70 3.97
| SFKN 12T3AZTN | DDD | D | D | 2(3) | |||
| 12T3AZTN-S | D | 3 | Fig 5 | ||||
| Face | |||||||
| 12T3AZTN-W | D | 3 | Wiper Inserts Milling | ||||
| 12T3AZFN | DDD | D | 2(3) | Shoulder | |||
| Milling | |||||||
| SFKR 12T3AZEN | D | D | 4 | 13 | |||
| ±0.0 | |||||||
| M 16 | 3.97±0.025 | ||||||
| UW 12500R | D | 5 | High Feed |
Radius
- Recommended Cutting Conditions Multi-
Double Screw Purpose Engraved Mark External Diameter ø50 to ø63 mm R/
| Insert Clamp 4SR | ( | ) | ( | ) | Profiling | |||
| Cutting Speed v | m/min | Feed Rate f | mm/t | |||||
| ISO Work Material Hardness | c | z | Grade Groove/ | |||||
| Shim | Min.- Optimum -Max. | Min.- Optimum -Max. | ||||||
| T-Slot | ||||||||
| Insert | Carbon Stee 180 to 280HB | 100- 125-200 | 0.10-0.20 -0.30 | ACP200 | ||||
| P | Chamfering | |||||||
| Alloy Steel | 180 to 280HB 80- 100-180 | 0.10-0.20 -0.30 | ACP200 | |||||
| Locator | K | Cast Iron | 250HB 80- 100-120 | 0.10-0.20 -0.30 | ACK200 | Aluminum/ | ||
| Light Alloys | ||||||||
| Double | N | Non-Ferrous Metal | Q 80- 160-250 | 0.05- 0.15-0.20 | H1 |
Screw High-Speed The cutting conditions above are a guide. Actual conditions will need to be adjusted Cast Iron Clamp Note according to machine rigidity, work clamp rigidity, cutting depth, and other factors.
External Diameter ø80 to ø100 mm Cutting Speed v(m/min) Feed Rate ( ) f mm/t
ISO Work Material Hardness c z Grade
| Parts | Min.- Optimum -Max. | Min.- Optimum -Max. | ||
| Carbon Stee 180 to 280HB | 100- 125-200 | 0.10-0.25 -0.40 | ACP200 |
Applicable Locator Insert Double P
Shim Locator Wrench Alloy Steel 180 to 280HB 80- 100-180 0.10-0.25 -0.40 ACP200
Cutters Clamp Clamp Screw
Size N m K
| Cast Iron | 250HB | 80- 100-120 | 0.10-0.25 -0.40 | ACK200 | |||||
| UFO 4000E Type UFKWR UFTWR WB7-15T M7 8.0 | UF4SR UF4KR | TT25 | N | Non-Ferrous Metal | Q | 80- 160-250 | 0.05-0.25 -0.30 | H1 |
Note: Wrench used is TT25. The cutting conditions above are a guide. Actual conditions will need to be adjusted Note ( ・ ) according to machine rigidity, work clamp rigidity, cutting depth, and other factors. N m Recommended Tightening Torque N m