Каталог Sumitomo фрезы со сменными пластинами - страница 83
Навигация
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo модульные системы для револьверных головок токарных станков
 Каталог Sumitomo токарные резцы (державки) для внутреннего точения
 Общий каталог Sumitomo 2018 - 2019
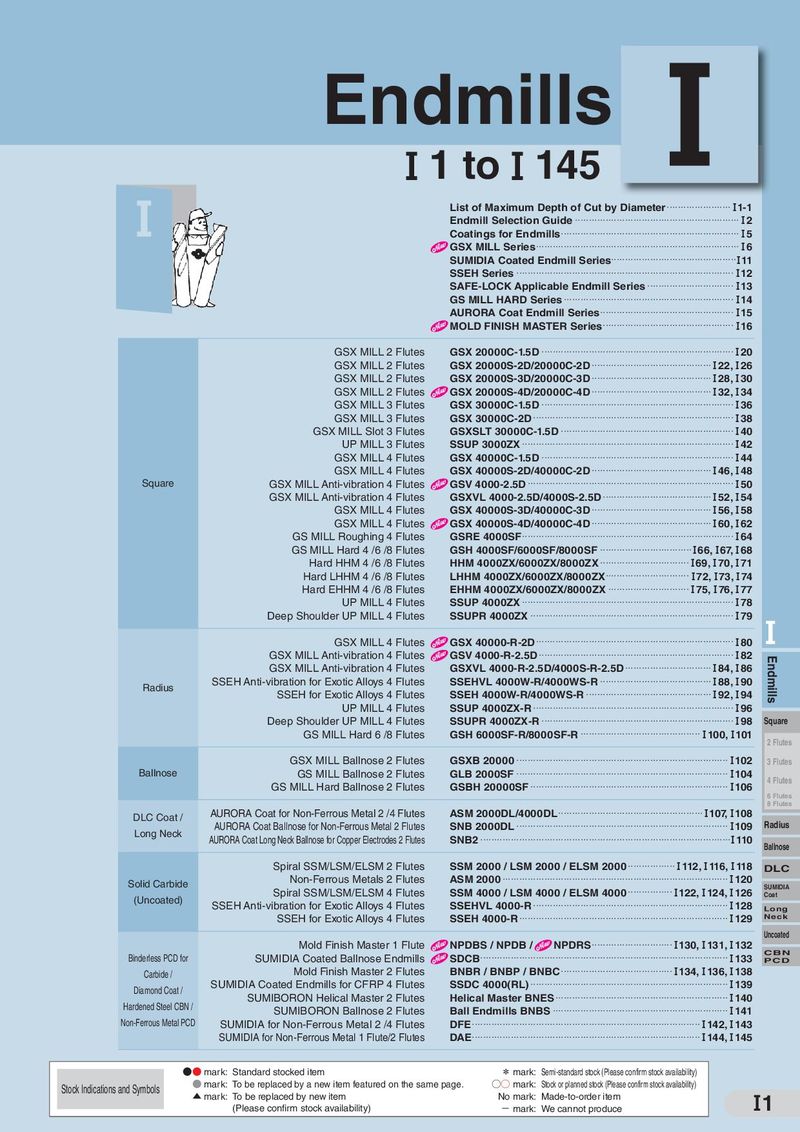 Каталог Sumitomo монолитные фрезы
- H001
- H002
- H003
- H004
- H005
- H006
- H007
- H008
- H009
- H010
- H011
- H012
- H013
- H014
- H015
- H016
- H017
- H018
- H019
- H020
- H021
- H022
- H023
- H024
- H025
- H026
- H027
- H028
- H029
- H030
- H031
- H032
- H033
- H034
- H035
- H036
- H037
- H038
- H039
- H040
- H041
- H042
- H043
- H044
- H045
- H046
- H047
- H048
- H049
- H050
- H051
- H052
- H053
- H054
- H055
- H056
- H057
- H058
- H059
- H060
- H061
- H062
- H063
- H064
- H065
- H066
- H067
- H068
- H069
- H070
- H071
- H072
- H073
- H074
- H075
- H076
- H077
- H078
- H079
- H080
- H081
- H082
- H083
- H084
- H085
- H086
- H087
- H088
- H089
- H090
- H091
- H092
- H093
- H094
- H095
- H096
- H097
- H098
- H099
- H100
- H101
- H102
- H103
- H104
- H105
- H106
- H107
- H108
- H109
- H110
- H111
- H112
- H113
- H114
- H115
- H116
- H117
- H118
- H119
- H120
- H121
- H122
- H123
- H124
- H125
- H126
- H127
- H128
- H129
- H130
- H131
- H132
- H133
- H134
- H135
- H136
- H137
- H138
- H139
- H140
- H141
- H142
- H143
- H144
- H145
- H146
- H147
- H148
- H149
- H150
- H151
- H152
- H153
- H154
- H155
- H156
- H157
- H158
- H159
- H160
- H161
- H162
- H163
- H164
- H165
- H166
- H167
- H168
- H169
- H170
- H171
- H172
- H173
- H174

■ Application Examples
Machine Component SUS304
| WEX1000 | Machine Component | SS400 | WEX1000 | ||
| The WEX type achieves 1.3x the tool life of | In spotface milling, the WEX type demonstrates | ||||
| the competitor's product in helical milling. | low cutting force and stable milling, unlike the |
| 60 | competitor's product with unstable power. | 150 | ||
| 1.5x the tool life of the competitor's product. | ||||
| 40 | 100 | |||
| 20 | 50 | |||
| 0 | WEX | WEX 0 | ||
| Competitor's Product | Competitor's Product | |||
| Tool: WEX1020E (ø20) | (Cutting Conditions) | Tool: WEX1010EL (ø10) | (Cutting Conditions) | |
| v =60m/min | v =160m/min | |||
| Insert: AXMT060204PDER-G | c | Insert: AXMT060204PDER-L | c | |
| f =0.18mm/t | f =0.08mm/t | |||
| Grade: ACM300 | Equipment:Vertical M/C BT30 | z | : z | |
| a =1.0mm | Grade: ACP200 Equipment | Vertical M/C BT40 a =5.0mm | ||
| p | p | |||
| Dry | Dry |
| ●Block Material | SUS316 | WEX2000 | ●Block Material | SCM440 | WEX3000 | ||
| 10% decrease in cutting force by using an E type breaker. | Compared to the competitor's tools, the WEX type | ||||||
| 1,600 | leaves a cleaner side milling surface, enabling it to | ||||||
| 1,400 | Principal Force |
1,200 Feed Force be used for finishing without changing tools.
1,000 800 Back Force (+) 600 Back Force (–) 400
200 0 -200 -400 E Type(ACM300) G Type(ACP300)
| Tool: WEX2050F (ø50) | (Cutting Conditions) | Tool: WEX3032E (ø32) | (Cutting Conditions) |
| v =180m/min | v =200m/min | ||
| Insert: AXMT123508PEER-E | c | Insert: AXMT170508PEER-G | c |
| f =0.15mm/t | f =0.15mm/t | ||
| Grade: ACM300 | z | Grade: ACP200 | z |
| a =20mm | a =5mm | ||
| e | e | ||
| a =3mm Dry | Dry a =10mm×3 times | ||
| p | p | ||
| ●Die Parts | Low Carbon Steel | ● |
WEX3000 Injection Molds SKT4 WEX3000
The WEX type doubles the tool Compared to the competitor's product, the WEX life of previous tools by performing type allows for stable milling with cutting longer without breakage. conditions increased 200% while achieving low cutting noise and good chip control. Additionally,
it leaves a good, glossy machined surface.
| Tool: WEX3032E (ø32) | (Cutting Conditions) | Tool: WEX3080F (ø80) | (Cutting Conditions) |
| v =151m/min | v =75m/min | ||
| Insert: AXMT170508PEER-G | c | Insert: AXMT170508PEER-G | c |
| f =0.2mm/t | f =0.19mm/t | ||
| Grade: ACP100 | z | z | |
| a =25mm | Grade: ACP200 | =80mm | |
| a | |||
| e | e | ||
| a =5mm Wet | a =5mm Dry | ||
| p | p |
Machine Component SUS304 WEX3000 Tool: WEX3032E (ø32)
Insert: AXMT170508PEER-E Cutting Distance:4,500mm Cutting Distance:1,650mm Grade: ACM300
(Cutting Conditions) v =150m/min c f =0.15mm/t z a =10mm e a =3.0mm p
WEX WEX Dry
Comp. A Comp. B The highly fracture-resistant substrate and hardened coating allows stable milling without breakage.
H
Face Milling Shoulder Milling High Feed Radius Multi- Purpose R/ Profiling Groove/ T-Slot Chamfering Aluminum/ Light Alloys High-Speed Cast Iron