Каталог Sumitomo фрезы со сменными пластинами - страница 107
Навигация
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo модульные системы для револьверных головок токарных станков
 Каталог Sumitomo токарные резцы (державки) для внутреннего точения
 Общий каталог Sumitomo 2018 - 2019
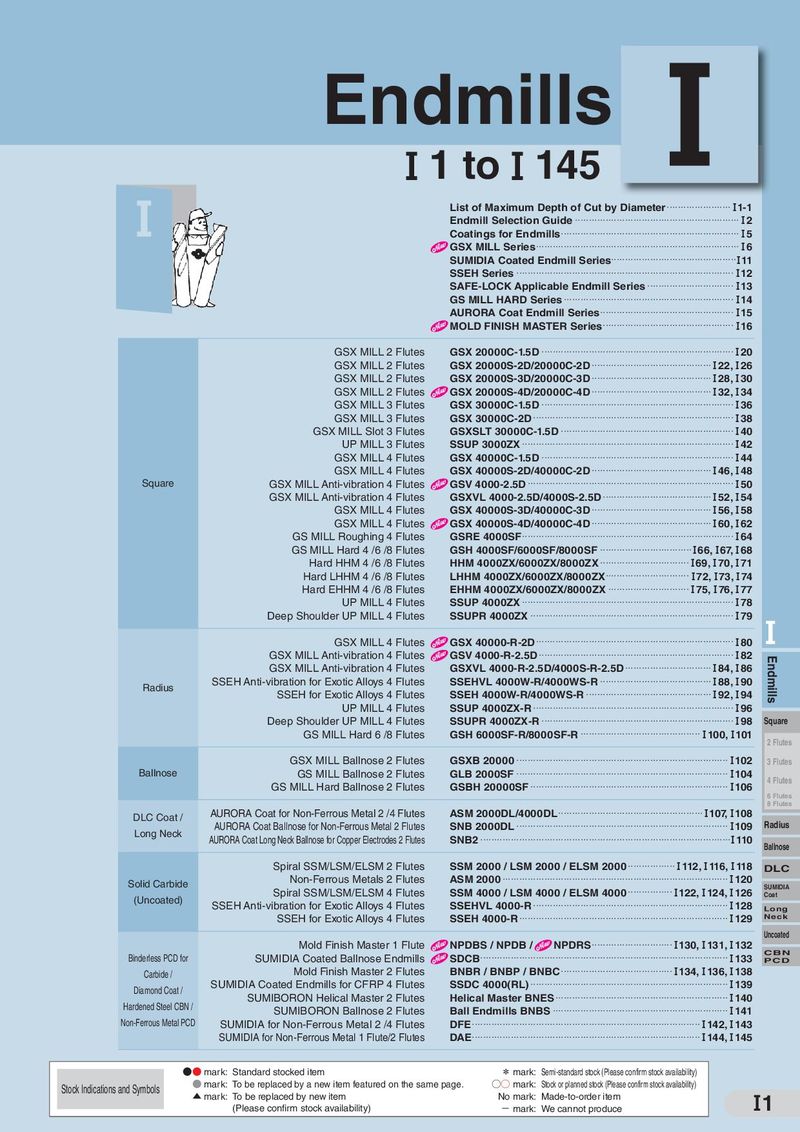 Каталог Sumitomo монолитные фрезы
- H001
- H002
- H003
- H004
- H005
- H006
- H007
- H008
- H009
- H010
- H011
- H012
- H013
- H014
- H015
- H016
- H017
- H018
- H019
- H020
- H021
- H022
- H023
- H024
- H025
- H026
- H027
- H028
- H029
- H030
- H031
- H032
- H033
- H034
- H035
- H036
- H037
- H038
- H039
- H040
- H041
- H042
- H043
- H044
- H045
- H046
- H047
- H048
- H049
- H050
- H051
- H052
- H053
- H054
- H055
- H056
- H057
- H058
- H059
- H060
- H061
- H062
- H063
- H064
- H065
- H066
- H067
- H068
- H069
- H070
- H071
- H072
- H073
- H074
- H075
- H076
- H077
- H078
- H079
- H080
- H081
- H082
- H083
- H084
- H085
- H086
- H087
- H088
- H089
- H090
- H091
- H092
- H093
- H094
- H095
- H096
- H097
- H098
- H099
- H100
- H101
- H102
- H103
- H104
- H105
- H106
- H107
- H108
- H109
- H110
- H111
- H112
- H113
- H114
- H115
- H116
- H117
- H118
- H119
- H120
- H121
- H122
- H123
- H124
- H125
- H126
- H127
- H128
- H129
- H130
- H131
- H132
- H133
- H134
- H135
- H136
- H137
- H138
- H139
- H140
- H141
- H142
- H143
- H144
- H145
- H146
- H147
- H148
- H149
- H150
- H151
- H152
- H153
- H154
- H155
- H156
- H157
- H158
- H159
- H160
- H161
- H162
- H163
- H164
- H165
- H166
- H167
- H168
- H169
- H170
- H171
- H172
- H173
- H174
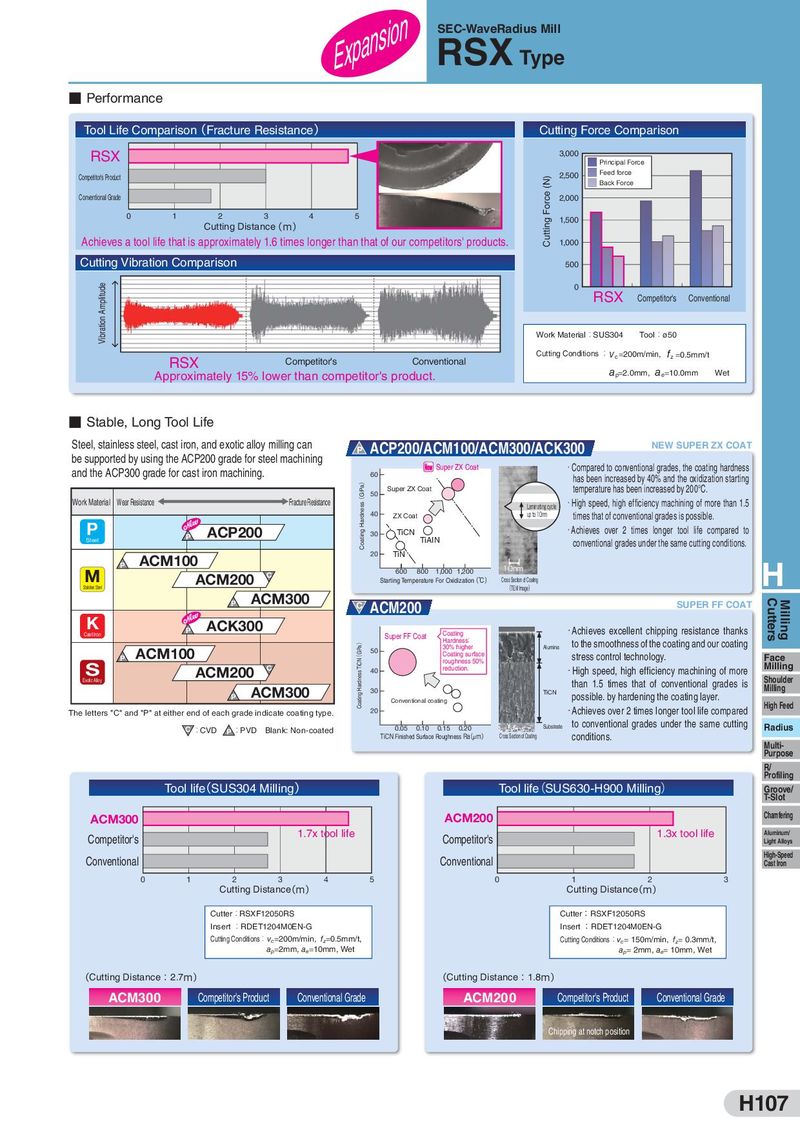
- Performance Tool Life Comparison (Fracture Resistance) Cutting Force Comparison RSX 3,000
Principal Force 2,500 Feed force Competitor's Product Back Force Conventional Grade 2,000
0 1 2 3 4 5
(m) 1,500 Cutting Distance Achieves a tool life that is approximately 1.6 times longer than that of our competitors' products. 1,000 Cutting Vibration Comparison 500
0
RSX Competitor's Conventional
Work Material:SUS304 Tool:ø50
| Cutting Conditions : | = 200m/min, f | = 0.5mm/t | |||
| RSX | V c | z | |||
| Competitor's | Conventional |
Approximately 15% lower than competitor's product. a = 2.0mm, a = 10.0mm Wet
p e
- Stable, Long Tool Life
| Steel, stainless steel, cast iron, and exotic alloy milling can | ACP200/ACM100/ACM300/ACK300 | NEW SUPER ZX COAT |
| P | ||
| be supported by using the ACP200 grade for steel machining | ||
| Super ZX Coat ・Compared to conventional grades, the coating hardness | ||
| and the ACP300 grade for cast iron machining. | ||
| 60 | has been increased by 40% and the oxidization starting | |
| Super ZX Coat temperature has been increased by 200°C. | ||
| 50 | ・ |
| Work Material Wear Resistance | Fracture Resistance | Laminating cycle | High speed, high efficiency machining of more than 1.5 | ||
| 40 | up to 10nm | times that of conventional grades is possible. | |||
| ZX Coat |
| P | ACP200 | ・Achieves over 2 times longer tool life compared to | ||||
| 30 | TiCN | |||||
| P | TiAIN | |||||
| Steel | conventional grades under the same cutting conditions. |
ACM100 20 TiN
P 10nm H
M 600 800 1,000 1,200
| ACM200 | C | (℃) | ||||
| Starting Temperature For Oxidization | Cross Section of Coating | |||||
| Stainless Steel | (TEM Image ) | |||||
| ACM300 |
| P | C ACM200 | SUPER FF COAT | ||||
| K | ACK300 | |||||
| ・Achieves excellent chipping resistance thanks | ||||||
| P |
| Cast Iron | Super FF Coat | Coating | |
| Hardness: | to the smoothness of the coating and our coating |
ACM100 30% higher Alumina
| 50 | Coating surface | stress control technology. | |
| P | Face | ||
| S | roughness 50% | ・ | Milling |
| C ACM200 | reduction. | High speed, high efficiency machining of more | |
| 40 | |||
| Exotic Alloy | than 1.5 times that of conventional grades is | Shoulder | |
| ACM300 | Milling | ||
| 30 | TiCN possible. by hardening the coating layer. | ||
| P | |||
| Conventional coating | ・ | High Feed | |
| The letters "C" and "P" at either end of each grade indicate coating type. 20 | Achieves over 2 times longer tool life compared | ||
| to conventional grades under the same cutting | |||
| Blank: Non-coated :CCVD :PVD | 0.10 0.05 0.15 | Substrate 0.20 | Radius |
| P TiCN | Ra( m) conditions. |
Finished Surface Roughness μ Cross Section of Coating
Multi- Purpose R/ Profiling
Tool life(SUS304 Milling) Tool life(SUS630-H900 Milling)
Groove/ T-Slot
ACM300 ACM200 Chamfering
| 1.7x tool life | 1.3x tool life | Aluminum/ | ||
| Competitor's | Competitor's | |||
| Light Alloys |
| Conventional | Conventional | High-Speed |
| Cast Iron |
| 0 | 1 | 2 | 3 | 4 | 5 | 0 | 1 | 2 | 3 | ||
| Cutting Distance(m) | Cutting Distance(m) | ||||||||||
| Cutter:RSXF12050RS | Cutter:RSXF12050RS | ||||||||||
| Insert :RDET1204M0EN-G | Insert :RDET1204M0EN-G |
Cutting Conditions:v = 200m/min, f = 0.5mm/t, Cutting Conditions: = 150m/min,
| c | z | vc | f = 0.3mm/t, | ||||
| z | |||||||
| a = 2mm, a = 10mm, Wet | a = 2mm, a = 10mm, Wet | ||||||
| p | e | p | e | ||||
| (Cutting Distance : 2.7m) | (Cutting Distance : 1.8m) |
ACM300 Competitor's Product Conventional Grade ACM200 Competitor's Product Conventional Grade
Chipping at notch position