Общий каталог Tungaloy 2020 - 2021 - страница 854
Навигация
 Брошюра Tungaloy новая продукция
 Каталог Tungaloy глубокое сверление 1
 Каталог Tungaloy инструмент для автоматов швейцарского типа
 Каталог Tungaloy зубофрезерование
 Каталог Tungaloy глубокое сверление 2
- A Grade
- Grade contents
- CVD - Coated Grade
- PVD - Coated Grade
- Ceramic
- Cermet
- CBN
- PCD (T-DIA)
- Uncoated Cemented Carbide
- Grade - Comparison Chart
- CVD Coated Grades for Turning
- PVD Coated Grade for Turning
- Cermet for Turning
- Cemented Carbide for Turning
- PCBN and PCD for Turning
- Ceramics for Turning
- CVD Coated Grade for Milling
- PVD Coated Grade for Milling
- Cermet for Milling
- Cemented Carbide for Milling
- PCBN and PCD for Milling
- Ceramics for Milling
- Chipbreaker Comparison Chart
- Negative insert type
- Positive insert type
- B Insert
- Insert - Content structure
- Insert Contents
- General insert for Turning
- Designation system for Insert
- Chipbreaker Guide
- Negative - Steel
- Negative - Stainless Steel
- Negative - Cast Iron
- Negative - Non-ferrous Metal
- Negative - Superalloys and titanium
- Negative - Hard Materials
- Positive - Steel
- Positive - Stainless Steel
- Positive - Cast Iron
- Positive - Non-ferrous Metal
- Positive- Superalloys and titanium
- Positive - Hard Materials
- Chipbreaker Overview
- Negative type with hole
- Negative type without hole
- Positive 7° with hole
- Positive 11° with hole
- Positive 7° with hole
- Positive 5° with hole
- Positive 11° without hole
- Double-sided positive type with hole
- Positive 7° without hole
- Negative
- CN
- DN
- RN
- SN
- TN
- VN
- WN
- YN
- KN
- HN
- Positive
- CC
- CP
- DC
- DP
- DX
- EP
- RC
- RT
- SC
- SP
- TC
- TP
- VB
- VC
- VP
- WP
- VX
- WB
- WX
- YW
- JXF
- JXR
- JXB
- JTB
- J10E
- 10E
- CBN
- Features
- BXA20
- WavyJoint
- GNGA type CBN
- HP Chipbreaker
- Designation System for T-CBN (PCBN) Inserts
- Negative type
- Positive type
- PCD
- Negative type
- Positive type
- Technical Guide
- T-CBN series for hardened steel and hard material
- T-CBN series for sintered metal
- T-CBN series for grey cast iron and ductile cast iron
- T-CBN Series - Honing specifications
- Features - PCD grade, T-DIA series
- C External Toolholder
- External Toolholder - Content structure
- Main products
- Designation system for Toolholders
- Quick Guide
- Negative type
- Positive type
- Features
- TurnTen-Feed
- ISO-EcoTurn
- Cutting edge
- L
- J
- N
- V
- P
- A
- G
- B
- R
- X
- D
- S
- K
- F
- Q
- H
- Special
- Technical Guide
- Parts for coolant hose
- FixRTurn - Standard cutting conditions
- MiniForce-Turn - Standard cutting conditions
- TurnTen-Feed - Standard cutting conditions
- TurnFeed - Standard cutting conditions
- TurnTec - Standard cutting conditions
- DimpleFX - Standard cutting conditions
- D Internal Toolholder
- Internal Toolholder - Content structure
- Main products
- Designation system for Toolholders
- Quick Guide
- Positive type
- Negative type
- Features
- BoreMeister
- StreamJetBar
- Cutting edge
- L
- X
- J
- K
- F
- U
- Q
- Z
- Others
- Technical Guide
- Sleeves for StreamJetBar
- MiniForce-Turn - Standard cutting conditions
- TurnTec - Standard cutting conditions
- E Threading tool
- Threading Tool - Content structure
- Main products
- Quick Guide - Applicable tool
- External threading
- Internal threading
- Features
- TetraMini-Cut
- DuoJust-Cut
- Insert for threading
- For Energy
- API Round
- API Round (For tool-rotating machines)
- API Buttress
- API Buttress (For tool-rotating machines)
- General
- 60° thread angle
- 55° thread angle (General purpose)
- ISO metric (General purpose)
- Unified (General purpose)
- For Pipe
- Whitworth, Parallel pipe thread
- BSPT (for Pipe)
- NPT (for Pipe)
- NPTF
- For Machine parts
- 30° Trapezoidal / DIN103
- Round / DIN405
- For Aerospace industry
- UNJ
- MJ
- For Machine parts, Pipe
- 29° Trapezoidal / ACME
- 29° Trapezoidal/ STUB ACME
- Toolholder for threading
- Technical Guide
- Designation system for TT-type insert
- Designation system for ST-type insert
- TungThread - Standard cutting conditions
- TungT-Clamp - Standard cutting conditions
- TetraMini-Cut - Standard cutting conditions
- DuoJust-Cut - Standard cutting conditions
- TinyMini-Turn - Standard cutting conditions
- Replacement of shim
- F Parting, Grooving
- Parting, Grooving - Content structure
- Par ting, Grooving - Machining Overview
- Quick Guide
- Features
- TungCut
- External grooving
- TungCut
- TetraMini-Cut
- TetraForce-Cut
- My-T Series
- Toolholder for 2 corner insert
- Toolholder for 1 corner insert
- 2 corner insert
- Standard cutting conditions
- Chipbreaker Guide
- 1 corner insert
- Chipbreaker Guide
- Standard cutting contions
- TungT-Clamp
- Standard cutting conditions
- Insert
- Applicable toolhoder for GTGN type insert
- GTGN type insert
- Standard cutting conditions
- TungHeavyGroove
- Chipbreaker Guide
- Insert
- Standard cutting conditions
- Others
- Internal grooving
- TungCut
- Insert
- Chipbreaker Guide
- Standard cutting conditions
- My-T Series
- Insert
- Chipbreaker Guide
- Standard cutting conditions
- TungT-Clamp
- Insert
- Standard cutting conditons
- Applicable toolhoder for GTGN type insert
- GTGN type insert
- Standard cutting conditions
- Others
- Face grooving
- EasyMulti-Cut
- Chipbreaker Guide
- Insert
- Standard cutting conditions
- TungCut
- Insert
- Chipbreaker Guide
- Standard cutting conditions
- My-T Series
- Insert
- Chipbreaker Guide
- Standard cutting conditions
- Others
- Grooving and parting
- TungCut
- Insert
- Chipbreaker Guide
- Standard cutting conditions
- My-T Series
- Toolholder for 2 corner insert
- Insert
- Standard cutting conditions
- Chipbreaker Guide
- Toolhoder for 1 corner insert
- Insert
- Chipbreaker Guide
- Standard cutting conditions
- Undercutting, profiling
- TungCut
- Insert
- Standard cutting conditions
- Chipbreaker Guide
- Technical guide
- Parts for coolant hose
- G Miniature Machining
- Miniature Machining - Content structure
- Main products
- Quick Guide
- Miniature External Turning
- Miniature Internal Turning
- Miniature Grooving
- Miniature Parting
- Miniature Threading
- Miniature Internal Turning - TinyMini-Turn
- Features
- TungTurn-Jet
- DirectTung-Jet system
- MiniForce-Turn
- External turning
- L
- J, U
- N
- P
- A
- G
- D
- F
- X
- Others
- Technical Guide
- MiniForce-Turn - Standard cutting conditions
- J-Seires - Standard cutting conditions
- TinyMini-Turn
- Internal turning
- Internal thrading
- Internal grooving
- Face grooving
- Standard cutting conditions
- Grooving
- TetraMini-Cut
- Insert
- Standard cutting conditions
- TetraForce-Cut
- Insert
- Standard cutting coditions
- J-Series
- Applicable toolholder for JTG insert
- Insert - JTG
- Standard cutting conditions
- Applicatble toolholder for JXG insert
- Insert - JXG
- Applicable toolholder for JVG insert
- Insert - JVG
- JXG, JVG - Standard cutting conditions
- TungHeavyGroove
- Insert
- Standard cutting conditions
- Threading
- TungThread
- J-Series
- Insert - JXT
- Insert - JTT
- Standard cutting conditions
- Parting
- DuoJust-Cut
- Insert
- Standard cutting conditions
- TungCut
- Chipbreaker Guide
- Insert
- Standard cutting conditions
- H Milling Cutter
- Milling Cutter - Content structure
- Designation system
- Designation system for Inser t
- Application Overview
- Quick Guide
- High-Feed Milling
- Face Milling
- Shoulder milling
- Slot milling
- Profile milling
- Thread milling
- High FeedMilling
- Features
- DoFeed
- TungForce-Feed
- TungForce-Feed
- Insert
- Standard cutting conditions
- DoFeed 03
- Insert
- Standard cutting conditions
- DoFeed 06
- Insert
- Standard cutting conditions
- DoTwistBall
- Insert
- Standard cutting conditions
- DoFeedQuad
- Insert
- Standard cutting conditions
- MillQuadFeed
- Insert
- Standard cutiing conditions
- MillFeed
- Insert
- Standard cutting conditions
- Face Milling
- Features
- TungSpeed-Mill
- DoTriple-Mill
- Insert
- Standard cittiong conditions
- DoOcto
- Insert
- Standard cittiong conditions
- DoQuad-Mill
- Insert
- Standard cittiong conditions
- DoPent
- Insert
- Standard cittiong conditions
- TungMill - TAW/EAW
- Insert
- Standard cittiong conditions
- TungSpeed-Mill - TPYP/EPYP
- Insert
- Standard cittiong conditions
- TungSpeed-Mill - TPYD/EPYD
- Insert
- Standard cittiong conditions
- TungMill - TFE/EFE
- Insert
- Standard cittiong conditions
- TungMill - DPD/EDPD
- Insert
- Standard cutting conditions
- Other tools
- S-TAQ system
- QC system for TAC Mills
- Shoulder milling
- Features
- DoForce-Tri
- Tung-Tri
- DoForce-Tri
- Insert
- Standard cutting conditions
- Tung-Tri
- Insert
- Standard cutting conditions
- TungTri-Shred
- Insert
- Standard cutting conditions
- TungForce-Rec
- Insert
- Standard cutting conditions
- TungRec 07
- Insert
- Standard cutting conditions
- TungRec 11
- Insert
- Standard cutting conditions
- TungRec 18
- Insert
- Standard cutting conditions
- TungQuad
- Insert
- Standard cutting conditions
- TungMill - TPW-EPW
- Insert
- Standard cutting conditions
- DoRec
- Insert
- Standard cutting conditions
- TecMill
- Insert
- Standard cutting conditions
- TungAlu-Mill
- Insert
- Standard cutting conditions
- Other tools
- Slot Milling
- Features
- TungUniversalSlot
- Insert
- Standard cutting conditions
- TungThinSlit
- Insert
- Standard cutting conditions
- TungUniversalSlot
- Insert
- Standard cutting conditions
- TecTangentialSlot
- Insert
- Standard cutting conditions
- Profile Milling
- Features
- ProfileMill series
- BallFinishNose
- BallRoughNose
- Insert
- Standard cutting conditions
- BallFinishNose
- Insert
- Standard cutting conditions
- DoMini-Mill
- Insert
- Standard cutting conditions
- FixRMill
- Insert
- Standard cutting conditions
- RoundSplit
- Insert
- Standard cutting conditions
- Other tools
- I Endmill
- EndMill - Content structure
- Main products
- Solid Endmill
- Quick Guide
- Designation system
- Features
- Square
- VariableMeister
- Standard cuting conditions
- FinishMeistrer / ShredMeister
- Standard cutting conditions
- SolidMeister
- Standard cutting conditions
- Continuation of SolidMeister
- Standard cutting conditions
- High feed
- FeedMiester
- Standard cutting conditions
- Ball
- Standard cutting conditions
- Exchangeable Endmill
- TungMeister
- Quick Guide
- Features
- Designation system
- Square
- Standard cutting conditions
- Radius
- VRB, VRC, VRD
- Standard cutting conditions
- VFX
- Standard cutting conditions
- Ball
- Standard cutting conditions
- Spot drilling
- Standard cutting conditions
- Counterboring
- Standard cutting conditions
- Chamfering
- Staandard cutting conditions
- Slotting
- Standard cutting conditions
- Shank
- Other tools
- Threading endmill
- Features
- Solid carbide endmill - SolidThread
- Designation System
- ISO metric
- Unified
- Whitworth
- BSPT
- NPT
- NPTF
- MJ
- UNJ
- Standard cutting conditions
- TungMeister
- Designation System
- ISO metric
- Unified
- Whitwor th
- 60° par tial profile
- 55° par tial profile
- Standard cutting conditions
- ETTL
- Standard cutting conditions
- Other tools
- Milling insert
- J Drilling Tool
- Drilling Tool - Content structure
- Main product
- Basic Selection of Drilling Tools
- Quick Guide
- General drilling
- Deep drilling
- 2 Effective Drill
- DrillMeister
- Features
- TID L/D=1.5
- TID L/D=3
- TID L/D=5
- TID L/D=8
- TID L/D=12
- TIDC L/D=3
- TIDC L/D=5
- Chamfering adapter
- Drill head
- DMP General purpose
- DMC High precision machining
- Standard cutting conditions
- DrillForce-Meister
- Drill head
- Standard cutting coditions
- Regrinding holder
- SolidDrill
- Quick Guide
- DSW
- DSW-DE3 L/D=3
- DSW-DE5 L/D=5
- DSW-DI5 L/D=5
- DSW-DI8 L/D=8
- Designation system
- Standard cutting coditions
- DSX
- DSX-F03 L/D=3
- DSX-F05 L/D=5
- DSX-F08 L/D=8
- Standard cutting conditions
- DSE
- DSE-F02 L/D=2
- DSE-F03 L/D=3
- Standard cutting conditions
- DSM
- Standard cutting conditions
- DSM-CP
- Standard cutting conditions
- FDC-S
- L/D=5
- L/D=8
- Standard cutting conditions
- CDS
- Standard cutting cnditions
- Indexable drill
- TungSix-Drill
- Features
- L/D=2
- L/D=3
- L/D=4
- Standard cutting conditions
- Insert
- Chamfering tool
- TungDrillTwisted
- L/D=2
- L/D=3
- L/D=4
- L/D=5
- Insert
- Standard cutting conditions
- Chamfering tool
- EZ sleeve
- TundDrillBig
- TDB, TDS cartridge set
- Insert
- Standard cutting conditions
- TDB, TDX cartridge set
- Insert
- Standard cutting conditions
- TDP
- Insert
- Standard cutting conditions
- Drilling Insert
- Deep Hole Drill
- Indexable Gundrill guide
- DeepTri-Drill
- Features
- MCTR L/D=10
- MCTR L/D=15
- MCTR L/D=20
- MCTR L/D=25
- MCTRCH L/D=25
- MCTR L/D=8
- MCTR L/D=10
- MCTR L/D=15
- MCTR L/D=25
- TRLG
- TRLGCH
- TRLG-F
- Insert
- Guide pad
- Standard cutting conditions
- SLJ
- Standard cutting conditions
- BTA tool
- Drill Head Category
- Drill Tube Category
- Tri-Fine
- Insert
- Guide pad
- Fine-Beam
- Insert
- Guide pad
- Unidex
- Insert
- Standard cutting conditions
- Brazed drill head
- Standard cutting conditions
- Drill tube
- HF drill
- K Tooling System
- Tooling System - Content structure
- Main products
- TungCap
- Features
- TungCap tooling system
- External turning
- L
- J
- N
- V
- Internal turning
- L
- U
- X
- Q
- Treading
- Grooving
- Drilling
- Milling
- Adapter
- Side-lock holder
- SwissBore
- Features
- Boring head / Boring bar
- Digital display unit
- Clamping units
- Nomenclature for clamping units
- Clamping units & tools for CNC lathes
- Clamping torque
- TungHold
- DIN69871
- DIN 69893 HSK
- BT MAS 403
- DIN2080
- Other holders
- TungFit adapter
- ER Collet Chucking System
- ER collet
- TungShrink, ER collet type
- TungShrink - Induction heating unit for shrink tool chucking
- TungShrink - Quick change type
- Tapping attachment for ER collet chuck holders
- Pull stud with JIN/ANSI retention knob (BT), for MAZAK machines
- Parts
- Easy Lock - Electrical nut-clamp torque control device
- SpinJet
- Wireless RPM speed display
- Collet
- BeamWrench
- SwissBore
- Wide range of variation quick change system
- Digital display unit
- Boring head / boring bar
- Adapter
- PINZBOHR®
- Features
- System
- Designation System
- Boring head
- Arbor
- Adapter
- Parts
- Cartridge
- List of ISO Standard Cartridges by Application
- A-type (Positive rake, compact type)
- Top-Borer Tool
- Boring bar tool
- L User’s Guide
- User´s guide - contents
- Parts for Tools
- Screws
- Shims
- Clamps
- Clamp Sets
- Levers
- Pins
- Chipbreaker Pieces
- Springs (Springs for Shims)
- Coolant Supply Attachment
- Sizing Plates
- Washers
- Locators
- Insert locking wedges
- Locator adjusting wedges
- Fine adjusting screws
- Cover
- Technical Reference
- Turning Tools
- Grooving and Parting Tools
- Threading Tools
- Thread Milling CNC Program for Internal Thread
- Milling Tools
- Endmills
- Drilling Tools
- Symbols of Metals
- Approximate Conversion Table of Hardness
- Surface Roughness
- GC_2020-2021_G_M_Index
- Numeric
- A
- B
- C
- D
- E
- F
- G
- H
- I
- J
- K
- L
- M
- N
- O
- P
- Q
- R
- S
- T
- U
- V
- W
- X
- Y
- Z
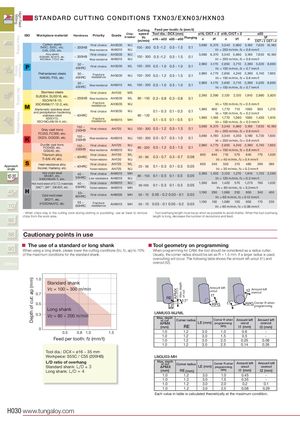
STANDARD CUTTING CONDITIONS T X N 0 3 / E X N 0 3 / H X N 0 3
| Cutting | Feedpe | r tooth:fz ( | mm/t) | |||||||||||
| ISO Workpiece material | Hardness | Priority | Grade | Chip- breaker | speed | Tool dia.: | DCX(mm) | ø16, C | ICT = 2 | ø18, C | ICT = 2 | ø20 | ||
| Vc (m/min) | ø16 ~ ø22 | ø25 ~ ø50 | Plunging | n | Vf | n | Vf | n CICT = | Vf 3 CICT = 4 | |||||
| Carbon steels S45C, S55C, etc. C45, C55, etc. | ~ 300HB | First choice Wear resistance | AH3035 AH8015 | MJ MJ | 100 - 300 | 0.5 -1.2 | 0.5 - 1.5 | 0.1 | 3,980 | 6,370 Vc | 3,540 =200 m | 5,660 /min,fz | 3,180 7,630 = 0.8 mm/t | 10,180 |
| Alloy steels SCM440, SCr415, etc. 42CrMo4, 17Cr3, etc. | ~ 300HB | First choice Wear resistance | AH3035 AH8015 | MJ MJ | 100 - 300 | 0.5 -1.2 | 0.5 - 1.5 | 0.1 | 3,980 | 6,370 Vc | 3,540 =200 m | 5,660 /min,fz | 3,180 7,630 = 0.8 mm/t | 10,180 |
| 30 ~ 40HRC | First choice | AH3035 | ML | 100 - 200 | 0.5 - 1.0 | 0.5 - 1.0 | 0.1 | 2,980 | 4,170 Vc | 2,650 =150 m | 3,710 /min,fz | 2,390 5,020 = 0.7 mm/t | 6,690 | |
| Prehardened steels NAK80, PX5, etc. | 30 ~ 40HRC | Fracture resistance | AH3035 | MJ | 100 - 200 | 0.5 - 1.2 | 0.5 - 1.5 | 0.1 | 2,980 | 4,770 Vc | 2,650 =150 m | 4,240 /min,fz | 2,390 5,740 = 0.8 mm/t | 7,650 |
| 30 ~ 40HRC | Wear resistance | AH8015 | ML | 100 - 200 | 0.5 - 1.0 | 0.5 - 1.0 | 0.1 | 2,980 | 4,170 Vc | 2,650 =150 m | 3,710 /min,fz | 2,390 5,020 = 0.7 mm/t | 6,690 | |
| Stainless steels SUS304, SUS316, etc. X5CrNi18-10 | ~ 200HB | First choice Wear resistance | AH130 AH3035 | MS ML | 80 - 150 | 0.3 - 0.8 | 0.3 - 0.8 | 0.1 | 2,390 | 2,390 | 2,120 | 2,120 | 1,910 2,860 | 3,820 |
| , X5CrNiMo17-12-2, etc. | Fracture resistance | AH3035 | MJ | Vc | =120 m | /min,fz | = 0.5 mm/t | |||||||
| Martensitic stainless steel and precipitation hardening il l | 40HRC | First choice | AH3035 | MJ | 80 120 | 0.1 - 0.3 | 0.1 - 0.3 | 0.1 | 1,990 | 800 Vc | 1,770 =100 m | 710 /min,fz | 1590 950 = 0.2 mm/t | 1,270 |
| staness stee X20Cr13, X5CrNiCuNb16-4 ,etc. | ~ | Fracture resistance | AH8015 | MH | - | 0.1 - 0.5 | 0.1 - 0.5 | 0.1 | 1,990 | 1,190 Vc | 1,770 =100 m | 1,060 /min,fz | 1590 1,430 = 0.3 mm/t | 1,910 |
| Gray cast irons FC250 FC300 t | 150 ~ 250HB | First choice | AH725 | MJ | 100 - 300 | 0.5 - 1.2 | 0.5 - 1.5 | 0.1 | 3,980 | 6,370 Vc | 3,540 =200 m | 5,660 /min,fz | 3,180 7,630 = 0.8 mm/t | 10,180 |
| , , ec. GG25, GGG30, etc. | 150 ~ 250HB | Wear resistance | AH8015 | MJ | 100 - 300 | 0.5 - 0.7 | 0.5 - 1.0 | 0.1 | 3,980 | 4,780 Vc | 3,540 =200 m | 4,250 /min,fz | 3,180 5,720 = 0.6 mm/t | 7,630 |
| Ductile cast irons FCD400, etc. GGG40, etc. | 150 ~ 250HB | First choice Wear resistance | AH725 AH8015 | MJ MJ | 80 - 200 | 0.5 - 1.2 | 0.5 - 1.5 | 0.1 | 2,980 | 4,770 Vc | 2,650 =150 m | 4,240 /min,fz | 2,390 5,740 = 0.8 mm/t | 7,650 |
| Titanium alloy | ~ 40HRC | First choice | AH130 | ML | 30 - 60 | 03 - 07 | 03 - 07 | 008 | 800 | 640 | 710 | 570 | 640 770 | 1,020 |
| Ti-6Al-4V, etc. | Fracture resistance | AH130 | MJ | . . | . . | . | Vc | =40 m | /min,fz | = 0.4 mm/t | ||||
| Heat-resistance alloy Inconel, Hasteroy, etc. | ~ 40HRC | First choice Fracture resistance | AH725 AH725 | ML MJ | 20 - 50 | 0.1 - 0.3 | 0.1 - 0.3 | 0.05 | 600 | 240 Vc | 530 =30 m | 210 /min,fz | 480 290 = 0.2 mm/t | 380 |
| Hot mold steel SKD61, etc. X40CrMoV5-1, etc. | 40 ~ 55HRC | First choice Low resistance | AH8015 AH8015 | MH MJ | 80 - 150 | 0.1 - 0.5 | 0.1 - 0.5 | 0.05 | 2,390 | 1,430 Vc | 2,120 =120 m | 1,270 /min,fz | 1,910 1,720 = 0.3 mm/t | 2,290 |
| Hot mold steel of D.T.C materials DAC, DH, DIEVER, etc. | 40 ~ 55HRC | First choice Fracture resistance | AH8015 AH8015 | MJ MH | 50-100 | 0.1 - 0.3 | 0.1 - 0.3 | 0.05 | 1,590 | 640 Vc | 1,420 = 80 m | 570 /min,fz | 1,270 760 = 0.2mm/t | 1,020 |
| Cold mold steel SKD11 t | 55~ 60HRC | First choice | AH8005 | MH | 50 - 70 | 0.05 - 0.2 | 0.03 - 0.1 | 0.03 | 1,190 | 290 Vc | 1,060 =60 m/ | 250 min,fz = | 950 340 0.12 mm/t | 450 |
| , ec. X153CrMoV12, etc. | 55 ~ 60HRC | Fracture resistance | AH8015 | MH | 50 - 70 | 0.03 - 0.1 | 0.05 - 0.2 | 0.03 | 1,190 | 150 Vc | 1,060 =60 m/ | 130 min,fz = | 950 170 0.06 mm/t | 230 |
45°
- When chips stay in the cutting zone during slotting or pocketing, use air blast to remove - Tool overhang length must be as short as possible to avoid chatter. When the tool overhang
| 85 | chips from the work area. | length is long, decrease the number of revolutions and feed. | |
| 88° | Cautionary points in use | ||
| 90 | The use of a standard or long shank | Tool geometry on programming |
When using a long shank, please lower the cutting conditions (Vc, fz, ap) to 70% When programming for CAM, the tool should be considered as a radius cutter. of the maximum conditions for the standard shank. Usually, the corner radius should be set as R = 1.5 mm. If a larger radius is used, overcutting will occur. The following table shows the amount left uncut (t1) and Others overcut (t2).
1.0 Standard shank
Vc = 100 300 m/min Amount left Amount left
uncut t2 overcut 0.7 t1 Max. depth of cut RE
17°
t1 RPG Corner R when
| 0.5 | LE | RPG | programming | |
| Long shank |
| 0.3 | V | LNMU03-MJ/ML |
| c = 80 ~ 200 m/min | ||
| Max. depth |
| of cut | Corner radius | Corner R when | Amount left | Amount left | ||||
| APMX | LE (mm) | programming: | uncut | overcut | ||||
| (mm) | RE | RPG | t1 (mm) | t2 (mm) | ||||
| 0 |
| 1.5 0.5 0.8 1.0 | 1.0 | 1.2 | 3.0 | 1.0 | 0.6 | - | |
| Feed per tooth: fz (mm/t) | 1.0 | 1.2 | 3.0 | 1.5 | 0.5 | - | |
| 1.0 | 1.2 | 3.0 | 2.0 | 0.25 | 0.08 | ||
| 1.0 | 1.2 | 3.0 | 2.5 | 0.14 | 0.26 | ||
| Tool dia.: DCX = ø16 ~ 35 mm | |||||||
| Workpeice: S55C / C55 (200HB) | LNGU03-MH | ||||||
| L/D ratio of overhang | Max. depth |
| of cut | Corner radius | Corner R when | Amount left | Amount left | ||||
| Standard shank: L/D ) 3 | APMX | LE (mm) | uncut | overcut | ||||
| programming: | ||||||||
| Long shank: L/D = 4 | (mm) | RE (mm) | RPG | t1 (mm) | t2 (mm) | |||
| 1.0 | 1.2 | 3.0 | 1.0 | 0.45 | - | |||
| 1.0 | 1.2 | 3.0 | 1.5 | 0.35 | - |
Each value in table is calculated theoretically at the maximum condition.