Техническая информация Sumitomo - страница 6
Навигация
 Каталог Sumitomo пластины с алмазными вставками Sumidia
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo токарные резцы (державки) для наружного точения
 Каталог Sumitomo твердосплавные пластины
 Каталог Sumitomo фрезы со сменными пластинами
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
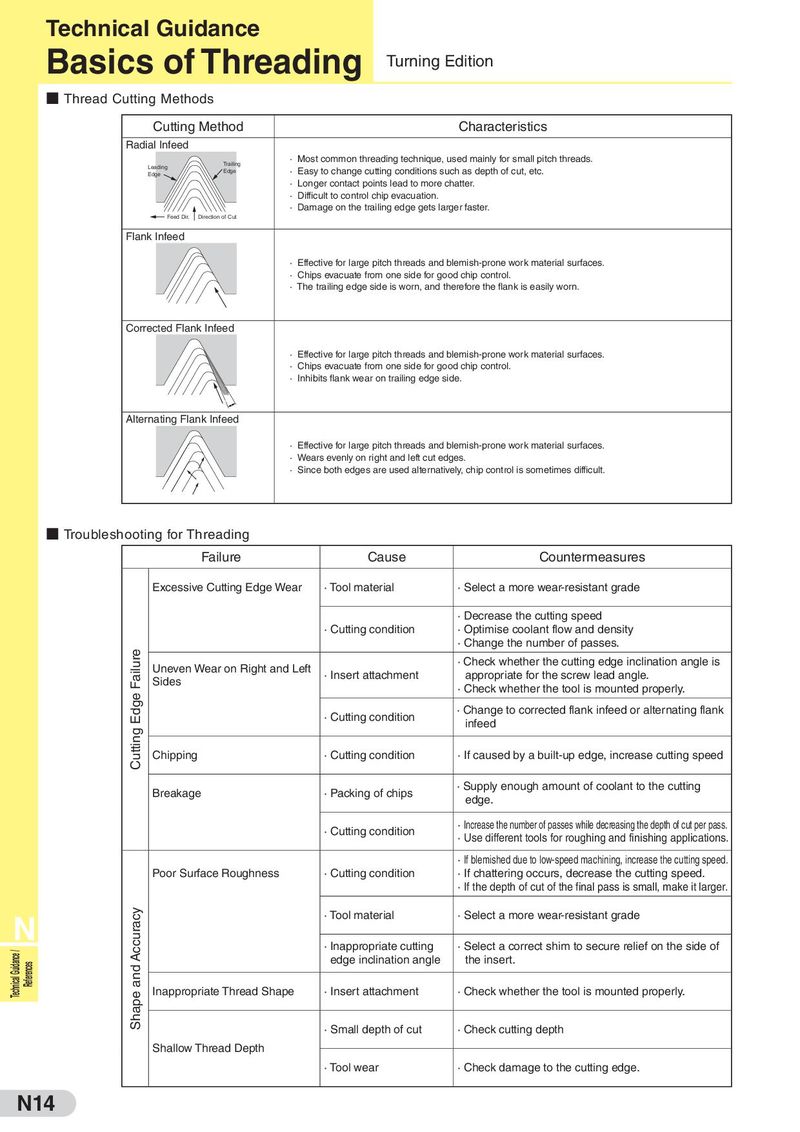
Basics of Threading
- Thread Cutting Methods
Cutting Method Characteristics
Radial Infeed
- Most common threading technique, used mainly for small pitch threads.
Leading Trailing Edge Easy to change cutting conditions such as depth of cut, etc. Edge
- Longer contact points lead to more chatter.
- Difficult to control chip evacuation.
- Damage on the trailing edge gets larger faster.
Feed Dir. Direction of Cut Flank Infeed
- Effective for large pitch threads and blemish-prone work material surfaces.
- Chips evacuate from one side for good chip control.
- The trailing edge side is worn, and therefore the flank is easily worn.
Corrected Flank Infeed
- Effective for large pitch threads and blemish-prone work material surfaces.
- Chips evacuate from one side for good chip control.
- Inhibits flank wear on trailing edge side.
Alternating Flank Infeed
- Effective for large pitch threads and blemish-prone work material surfaces.
- Wears evenly on right and left cut edges.
- Since both edges are used alternatively, chip control is sometimes difficult.
- Troubleshooting for Threading
| Failure | Cause | Countermeasures | |
| Excessive Cutting Edge Wear | · Tool material | · Select a more wear-resistant grade | |
| · Cutting condition | · Decrease the cutting speed · Optimise coolant flow and density · Change the number of passes. | ||
| e Failure | Uneven Wear on Right and Left Sides | · Insert attachment | · Check whether the cutting edge inclination angle is appropriate for the screw lead angle. · Check whether the tool is mounted properly. |
| g Edg | · Cutting condition | · Change to corrected flank infeed or alternating flank infeed | |
| Cuttin | Chipping | · Cutting condition | · If caused by a built-up edge, increase cutting speed |
| Breakage | · Packing of chips | · Supply enough amount of coolant to the cutting edge. | |
| · Cutting condition | ·Increase the number of passes while decreasing the depth of cut per pass. ·Use different tools for roughing and finishing applications. | ||
| Poor Surface Roughness | · Cutting condition | ·If blemished due to low-speed machining, increase the cutting speed. · If chattering occurs, decrease the cutting speed. ·If the depth of cut of the final pass is small, make it larger. | |
| racy | · Tool material | · Select a more wear-resistant grade | |
| d Accu | · Inappropriate cutting edge inclination angle | · Select a correct shim to secure relief on the side of the insert. | |
| pe an | Inappropriate Thread Shape | · Insert attachment | · Check whether the tool is mounted properly. |
| Sha | · Small depth of cut | · Check cutting depth | |
| Shallow Thread Depth | |||
| · Tool wear | · Check damage to the cutting edge. |