Техническая информация Sumitomo - страница 16
Навигация
 Каталог Sumitomo пластины с алмазными вставками Sumidia
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo токарные резцы (державки) для наружного точения
 Каталог Sumitomo твердосплавные пластины
 Каталог Sumitomo фрезы со сменными пластинами
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
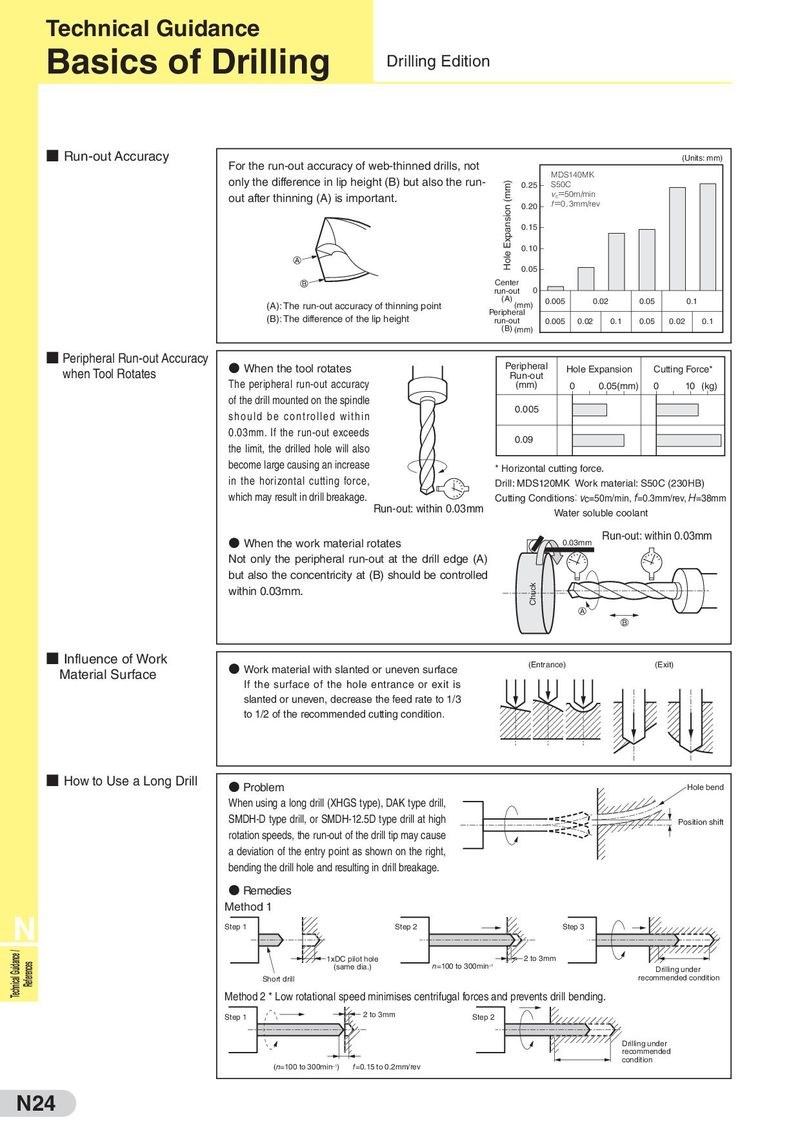
Basics of Drilling
- Run-out Accuracy
- Peripheral Run-out Accuracy when Tool Rotates
(Units: mm)
For the run-out accuracy of web-thinned drills, not
MDS140MK
only the difference in lip height (B) but also the run-
0.25 S50C v =50m/min out after thinning (A) is important. c f=0.3mm/rev 0.20 0.15 0.10 0.05 Center run-out 0
| (A) | 0.005 | 0.02 | 0.05 | 0.1 | |||
| (A): The run-out accuracy of thinning point | (mm) | ||||||
| Peripheral |
(B): The difference of the lip height run-out 0.005 0.02 0.1 0.05 0.02 0.1
(B) (mm)
- When the tool rotates Peripheral
Hole Expansion Cutting Force* Run-out
The peripheral run-out accuracy (mm) 0 0.05(mm) 0 10 (kg)
of the drill mounted on the spindle 0.005 should b e controlled within 0.03mm. If the run-out exceeds
0.09
the limit, the drilled hole will also
become large causing an increase
* Horizontal cutting force.
in the horizontal cutting force, Drill: MDS120MK Work material: S50C (230HB)
which may result in drill breakage. Cutting Conditions: c=50m/min, =0.3mm/rev, =38mm
Run-out: within 0.03mm
Water soluble coolant
- Run-out: within 0.03mm
When the work material rotates 0.03mm
Not only the peripheral run-out at the drill edge (A)
but also the concentricity at (B) should be controlled
within 0.03mm.
- Influence of Work Material Surface
Work material with slanted or uneven surface (Entrance) (Exit)
If the surface of the hole entrance or exit is slanted or uneven, decrease the feed rate to 1/3 to 1/2 of the recommended cutting condition.
- How to Use a Long Drill
N
- Problem
When using a long drill (XHGS type), DAK type drill,
SMDH-D type drill, or SMDH-12.5D type drill at high
rotation speeds, the run-out of the drill tip may cause
a deviation of the entry point as shown on the right, bending the drill hole and resulting in drill breakage.
- Remedies
Method 1
Step 1 Step 2 Step 3
1xDC pilot hole 2 to 3mm (same dia.) n=100 to 300min –1 Short drill Method 2 * Low rotational speed minimises centrifugal forces and prevents drill bending.
Step 1 2 to 3mm Step 2
(n=100 to 300min–1) f =0.15 to 0.2mm/rev
Hole bend
Position shift
Drilling under recommended condition
Drilling under recommended condition