Техническая информация Sumitomo - страница 15
Навигация
 Каталог Sumitomo пластины с алмазными вставками Sumidia
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo токарные резцы (державки) для наружного точения
 Каталог Sumitomo твердосплавные пластины
 Каталог Sumitomo фрезы со сменными пластинами
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
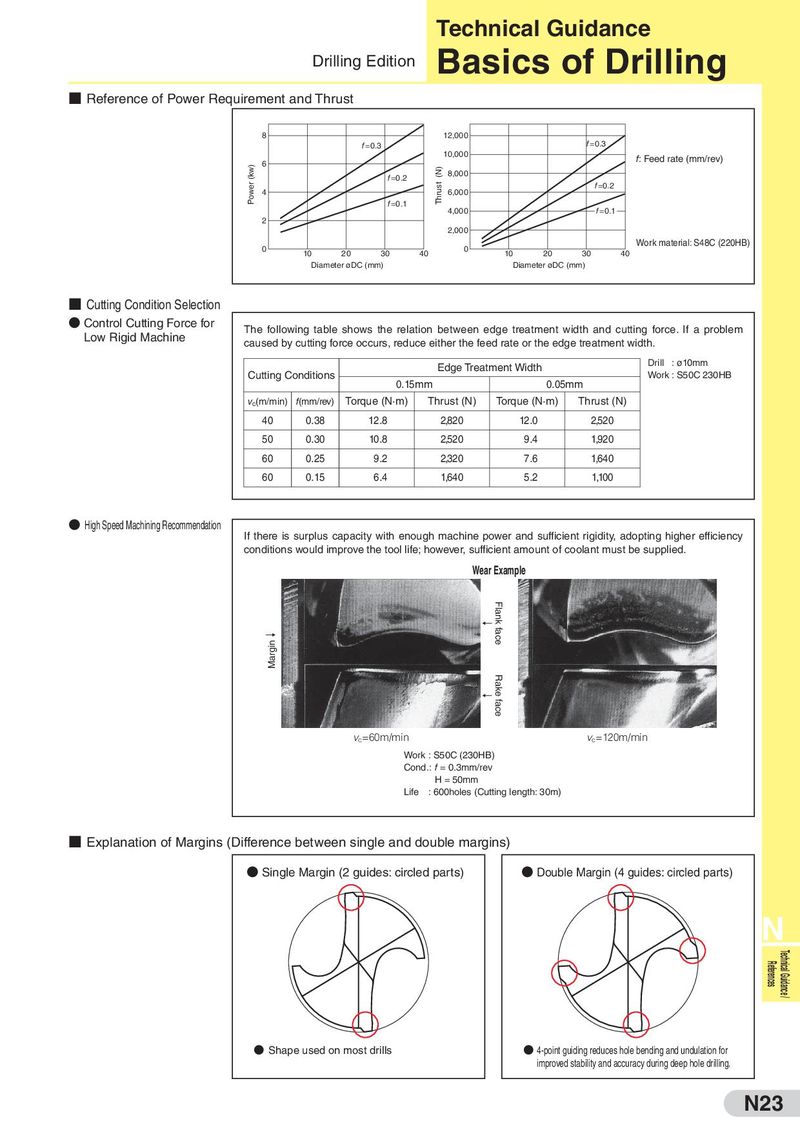
Basics of Drilling
- Reference of Power Requirement and Thrust
| 10 20 30 0 2 4 6 8 f=0.3 f=0.2 f=0.1 Diameter øDC (mm) Power (kw) | 40 10 20 30 40 0 12,000 10,000 8,000 6,000 4,000 2,000 f=0.3 f=0.2 f=0.1 Diameter øDC (mm) Thrust (N) | f: Feed rate (mm/rev) Work material: S48C (220HB) |
| he following table shows the relati aused by cutting force occurs, reduc Cutting Conditions 0.15m | on between edge treatment width and cutt e either the feed rate or the edge treatment w Edge Treatment Width m 0.05mm | ing force. If a problem idth. Drill : ø10mm Work : S50C 230HB |
| vc(m/min) f(mm/rev) Torque (N·m) | Thrust (N) Torque (N·m) Thrust (N) | |
| 40 0.38 12.8 | 2,820 12.0 2,520 | |
| 50 0.30 10.8 | 2,520 9.4 1,920 | |
| 60 0.25 9.2 | 2,320 7.6 1,640 | |
| 60 0.15 6.4 | 1,640 5.2 1,100 |
- Cutting Condition Selection
- Control Cutting Force for Low Rigid Machine
- High Speed Machining Recommendation
If there is surplus capacity with enough machine power and sufficient rigidity, adopting higher efficiency conditions would improve the tool life; however, sufficient amount of coolant must be supplied. Wear Example
v =60m/min v =120m/min c c Work : S50C (230HB) Cond.: f = 0.3mm/rev H = 50mm Life : 600holes (Cutting length: 30m)
- Explanation of Margins (Difference between single and double margins)
- Single Margin (2 guides: circled parts)
- Double Margin (4 guides: circled parts)
N
- Shape used on most drills
- 4-point guiding reduces hole bending and undulation for
improved stability and accuracy during deep hole drilling.