Техническая информация Sumitomo - страница 21
Навигация
 Каталог Sumitomo пластины с алмазными вставками Sumidia
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo токарные резцы (державки) для наружного точения
 Каталог Sumitomo твердосплавные пластины
 Каталог Sumitomo фрезы со сменными пластинами
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
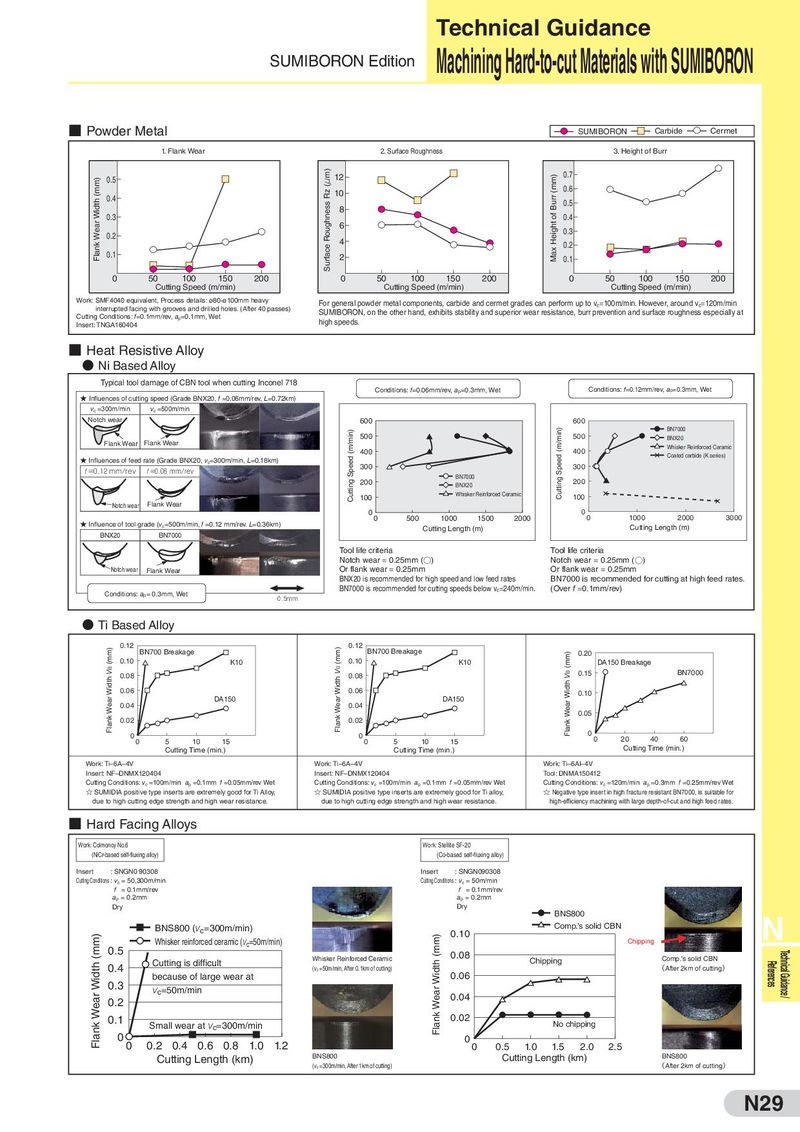
Machining Hard-to-cut Materials with SUMIBORON
- Powder Metal D
- D
SUMIBORON Carbide Cermet
1. Flank Wear 2. Surface Roughness 3. Height of Burr
D
- 0.7
0.5 12
| 0.6 | D | D | |
| 10 |
| 0.4 | ■ | D | |||
| 0.5 | |||||
| 8 | D | ||||
| 0.3 | D | 0.4 |
6 D D
| D | D | 0.3 | ||
| 0.2 | ■ |
D 4 D D D D
D D D 0.2 ■D
0.1 D 2 0.1
- D D
D D
| 0 | 50 | 100 | 150 | 200 | 0 | 50 | 100 | 150 | 200 | 0 | 50 | 100 | 150 | 200 | ||
| Cutting Speed (m/min) | Cutting Speed (m/min) | Cutting Speed (m/min) | ||||||||||||||
| Work: SMF4040 equivalent, Process details: ø80-ø100mm heavy | For general powder metal components, carbide and cermet grades can perform up to v =100m/min. However, around v =120m/min |
interrupted facing with grooves and drilled holes. (After 40 passes) c c
SUMIBORON, on the other hand, exhibits stability and superior wear resistance, burr prevention and surface roughness especially at Cutting Conditions: f=0.1mm/rev, ap=0.1mm, Wet Insert: TNGA160404 high speeds.
- Heat Resistive Alloy
- Ni Based Alloy Typical tool damage of CBN tool when cutting Inconel 718
Conditions: f=0.06mm/rev, ap=0.3mm, Wet Conditions: f=0.12mm/rev, ap=0.3mm, Wet
- Influences of cutting speed (Grade BNX20, f =0.06mm/rev, L=0.72km) vc =300m/min vc =500m/min
| Notch wear | 600 | 600 | |
| BN7000 | |||
| 500 | 500 | BNX20 |
Flank Wear Flank Wear Whisker Reinforced Ceramic 400 400
- Coated carbide (K series)
Influences of feed rate (Grade BNX20, vc=300m/min, L=0.18km)
| =0.12 mm/rev | =0.06 mm/rev | 300 | 300 | |
| f | f | |||
| BN7000 | ||||
| 200 | 200 | |||
| BNX20 | ||||
| 100 | Whisker Reinforced Ceramic | 100 | ||
| Notch wear Flank Wear | ||||
| 0 | 0 |
0 500 1000 1500 2000 0 1000 2000 3000
- Influence of tool grade (v =500m/min, f =0.12 mm/rev. L=0.36km)
| c | Cutting Length (m) | Cutting Length (m) | |||
| BNX20 | BN7000 | ||||
| Tool life criteria | Tool life criteria | ||||
| Notch wear = 0.25mm (○) | Notch wear = 0.25mm (○) |
Notch wear Flank Wear Or flank wear = 0.25mm Or flank wear = 0.25mm
BNX20 is recommended for high speed and low feed rates BN7000 is recommended for cutting at high feed rates. BN7000 is recommended for cutting speeds below v c=240m/min. (Over f =0.1mm/rev) Conditions: ap= 0.3mm, Wet 0.5mm
- Ti Based Alloy 0.12 0.12
BN700 Breakage BN700 Breakage 0.20
| 0.10 | K10 0.10 | K10 | DA150 Breakage |
| 0.15 | BN7000 | ||
| 0.08 | 0.08 | ||
| 0.06 | 0.06 | 0.10 | |
| DA150 | DA150 | ||
| 0.04 | 0.04 | ||
| 0.05 | |||
| 0.02 | 0.02 | ||
| 0 | 0 | 0 |
| 0 | 5 | 10 | 15 | 0 | 5 | 10 | 15 | 0 | 20 | 40 | 60 |
| Cutting Time (min.) | Cutting Time (min.) | Cutting Time (min.) |
| Work: Ti–6A–4V | Work: Ti–6A–4V | Work: Ti–6AI–4V |
| Insert: NF–DNMX120404 | Insert: NF–DNMX120404 | Tool: DNMA150412 |
| Cutting Conditions: vc =100m/min ap =0.1mm f =0.05mm/rev Wet | Cutting Conditions: vc =100m/min ap =0.1mm f =0.05mm/rev Wet | Cutting Conditions: vc =120m/min ap =0.3mm f =0.25mm/rev Wet |
| ☆ SUMIDIA positive type inserts are extremely good for Ti Alloy, | ☆ SUMIDIA positive type inserts are extremely good for Ti alloy, | ☆ Negative type insert in high fracture resistant BN7000, is suitable for |
| due to high cutting edge strength and high wear resistance. | due to high cutting edge strength and high wear resistance. | high-efficiency machining with large depth-of-cut and high feed rates. |
- Hard Facing Alloys Work: Colmonoy No.6 Work: Stellite SF-20 (NiCr-based self-fluxing alloy) (Co-based self-fluxing alloy)
| Insert | : SNGN0 90308 | Insert : SNGN090308 | |
| Cutting Conditions : vc = 50,300m/min | Cutting Conditions : vc = 50m/min | ||
| f = 0.1mm/rev | f = 0.1mm/rev | ||
| ap = 0.2mm | ap = 0.2mm | ||
| Dry | Dry | ||
| N BNS800 |
| BNS800 ( | =300m/min) | Comp.’s solid CBN | |
| c | 0.10 |
| Whisker reinforced ceramic ( | c=50m/min) | Chipping | ||
| 0.5 | ||||
| 0.08 |
| Cutting is difficult | Whisker Reinforced Ceramic | Chipping | Comp.'s solid CBN | |
| 0.4 | (v =50m/min, After 0.1km of cutting) | (After 2km of cutting ) |
c because of large wear at 0.06 0.3 =50m/min
c 0.04
0.2
0.1 0.02
| Small wear at | =300m/min | No chipping |
| c |
Cutting Length (km) BNS800 Cutting Length (km) BNS800
(v =300m/min, After 1km of cutting) (After 2km of cutting) c