Техническая информация Sumitomo - страница 5
Навигация
 Каталог Sumitomo пластины с алмазными вставками Sumidia
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo токарные резцы (державки) для наружного точения
 Каталог Sumitomo твердосплавные пластины
 Каталог Sumitomo фрезы со сменными пластинами
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
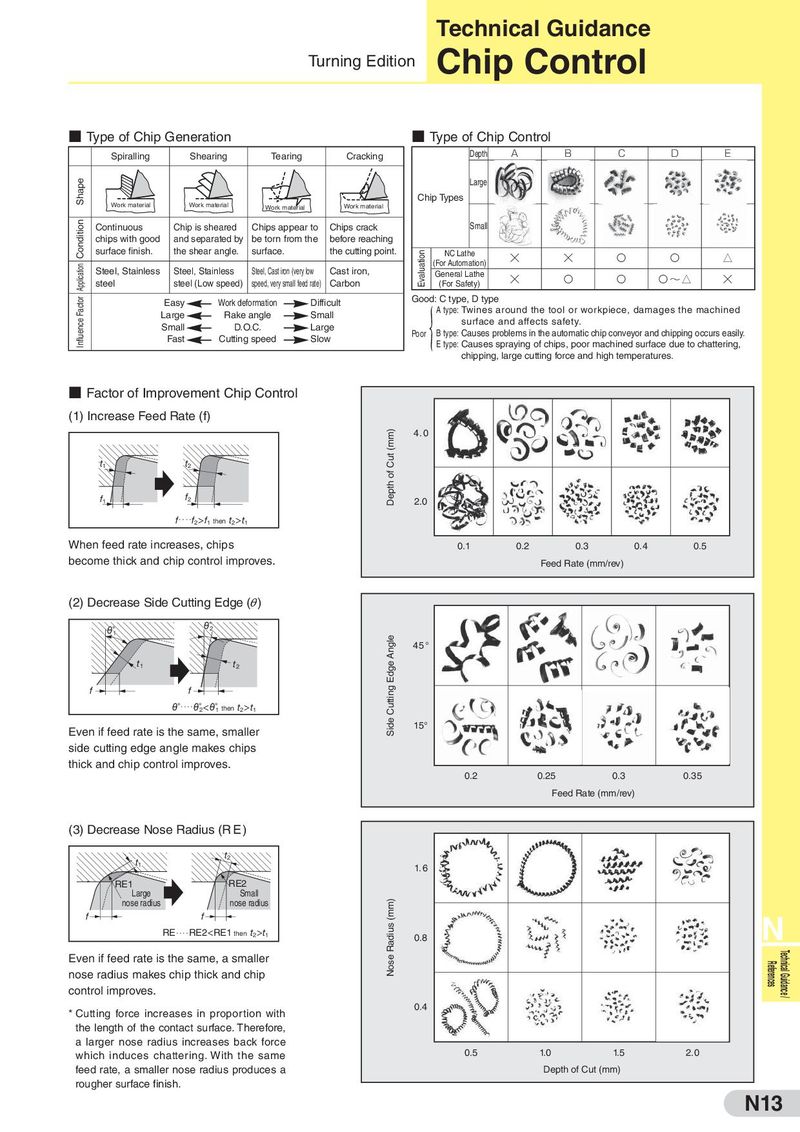
Chip Control
- Type of Chip Generation
- Type of Chip Control
| Depth | A | B | C | D | E | |
| Chip Types | Large | |||||
| Small | ||||||
| ation NC Lat (For Autom | he ation) | H | H | S | S | J |
| Evalu General L (For Saf | athe ety) | H | S | S | S~J | H |
Spiralling Shearing Tearing Cracking
Work material Work material Work material Work material
chips with good and separated by be torn from the before reaching
| Easy | Work deformation | Difficult | |
| Large | Rake angle | Small | |
| Small | D.O.C. | Large | |
| Fast | Cutting speed | Slow |
- Factor of Improvement Chip Control
(1) Increase Feed Rate (f)
| t | t | |
| 11 | 22 | |
| f | f | |
| 1 | 2 | |
| f‥‥f >f | then t >t | |
| 2 | 1 2 1 |
When feed rate increases, chips become thick and chip control improves. (2) Decrease Side Cutting Edge (θ ) θ: θ:
22 11
t t 1 2
f f :‥‥: <: t >t
2 1 then 2 1
Even if feed rate is the same, smaller side cutting edge angle makes chips thick and chip control improves.
(3) Decrease Nose Radius (R E )
t 22 t 11 RE1 RE2 Large Small nose radius nose radius f f RE‥‥RE2<RE1 then t >t 2 1
Even if feed rate is the same, a smaller
nose radius makes chip thick and chip
control improves.
* Cutting force increases in proportion with
the length of the contact surface. Therefore,
a larger nose radius increases back force
which induces chattering. With the same
feed rate, a smaller nose radius produces a
rougher surface finish.
{Good: C type, D type
A type: Twines around the tool or workpiece, damages the machined surface and affects safety. Poor B type: Causes problems in the automatic chip conveyor and chipping occurs easily. E type: Causes spraying of chips, poor machined surface due to chattering, chipping, large cutting force and high temperatures.
4 . 0
2.0
0.1 0.2 0.3 0.4 0.5
Feed Rate (mm/rev)
4 5 °
15°
0.2 0.25 0.3 0.35
Feed Rate (mm/rev)
1. 6
N
0.8
0.4
0.5 1.0 1.5 2.0
Depth of Cut (mm)