Техническая информация Sumitomo - страница 12
Навигация
 Каталог Sumitomo пластины с алмазными вставками Sumidia
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo токарные резцы (державки) для наружного точения
 Каталог Sumitomo твердосплавные пластины
 Каталог Sumitomo фрезы со сменными пластинами
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
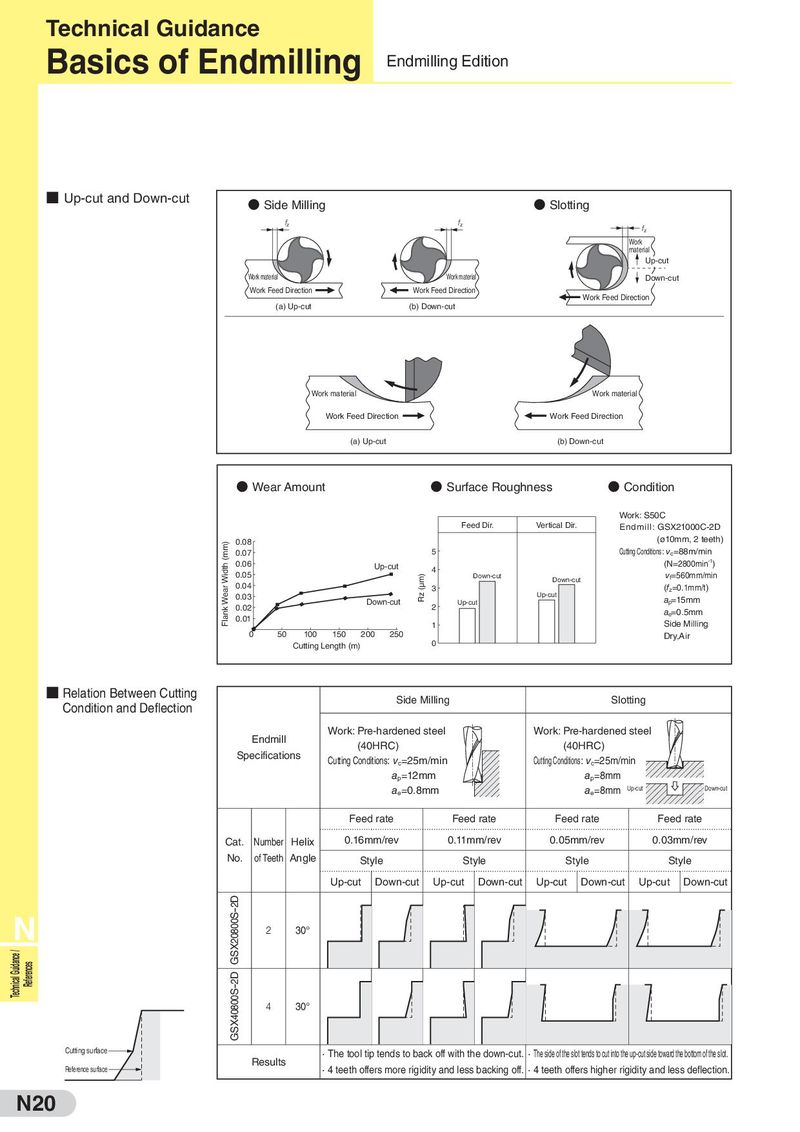
Basics of Endmilling
- Up-cut and Down-cut
- Side Milling fz fz
Work material Work material Work Feed Direction Work Feed Direction (a) Up-cut (b) Down-cut
- Slotting
f z Work material Up-cutUp-cut Down-cutDown-cut Work Feed Direction
- Relation Between Cutting Condition and Deflection
N
Work material Work material Work Feed Direction Work Feed Direction
(a) Up-cut (b) Down-cut
- Wear Amount
- Surface Roughness
- Condition
Work: S50C
| Feed Dir. | Vertical Dir. | Endmill: GSX21000C-2D | ||
| 0.08 | (ø10mm, 2 teeth) |
| 0.07 | 5 | Cutting Conditions: v =88m/min | ||
| c | ||||
| 0.06 | (N=2800min-1) | |||
| Up-cut | 4 |
| 0.05 | Down-cut | v =560mm/min | ||
| Down-cut | f | |||
| 0.04 | 3 | (f =0.1mm/t) |
z 0.03 Up-cut Down-cut a =15mm Up-cut p
0.02 2 ae=0.5mm 0.01 1 Side Milling
0 50 100 150 200 250 Dry,Air
Cutting Length (m) 0
Side Milling Slotting
Work: Pre-hardened steel Work: Pre-hardened steel
Endmill
(40HRC) (40HRC)
Specifications
Cutting Conditions: v =25m/min Cutting Conditions: v =25m/min
c c
a =12mm a =8mm
p p
| a =0.8mm | a =8mm | Up-cut | Down-cut |
| e | e |
| Feed rate | Feed rate | Feed rate | Feed rate | |||||||
| Cat. | Number | Helix | 0.16mm/rev | 0.11mm/rev | 0.05mm/rev | 0.03mm/rev | ||||
| No. | of Teeth | Angle | Style | Style | Style | Style |
Up-cut Down-cut Up-cut Down-cut Up-cut Down-cut Up-cut Down-cut
2 30°
4 30°
Cutting surface · The tool tip tends to back off with the down-cut. · The side of the slot tends to cut into the up-cut side toward the bottom of the slot.
Results
Reference surface · 4 teeth offers more rigidity and less backing off. · 4 teeth offers higher rigidity and less deflection.