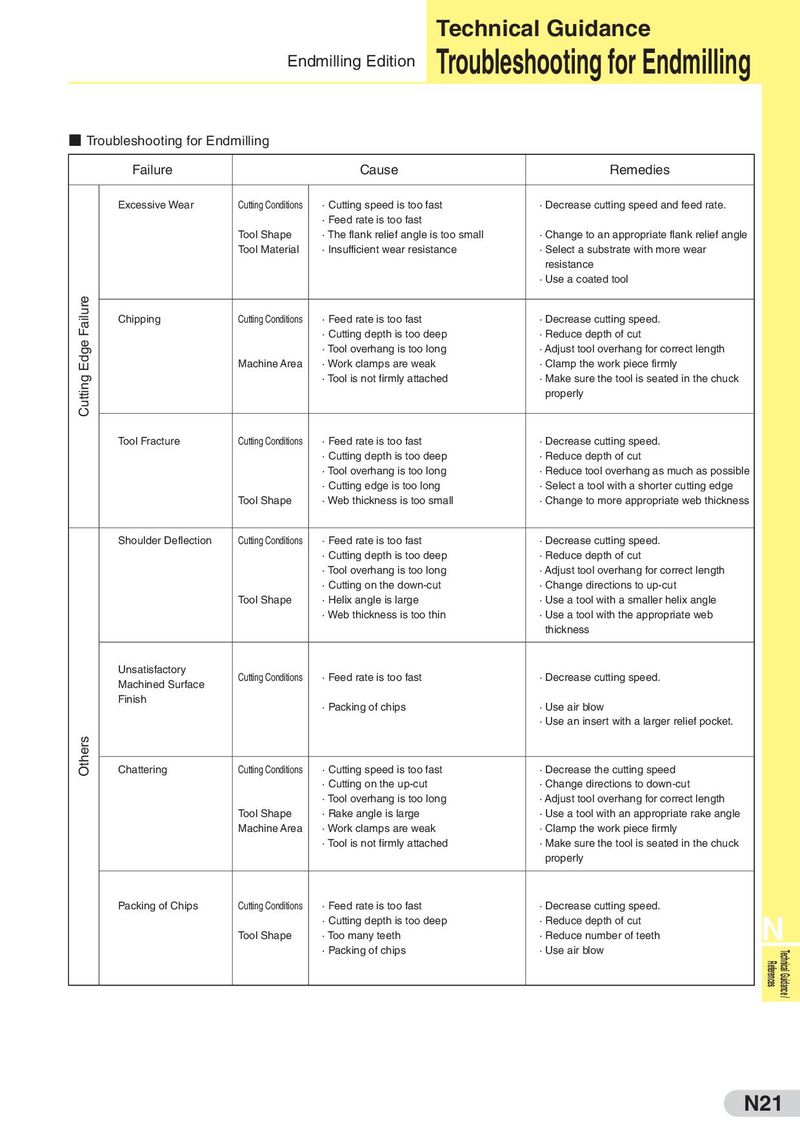
| Failure | | Cause | Remedies |
| Excessive Wear | Cutting Conditions Tool Shape Tool Material | · Cutting speed is too fast · Feed rate is too fast · The flank relief angle is too small · Insufficient wear resistance | · Decrease cutting speed and feed rate. · Change to an appropriate flank relief angle · Select a substrate with more wear resistance · Use a coated tool |
| Cutting Edge Failure | Chipping | Cutting Conditions Machine Area | · Feed rate is too fast · Cutting depth is too deep · Tool overhang is too long · Work clamps are weak · Tool is not firmly attached | · Decrease cutting speed. · Reduce depth of cut · Adjust tool overhang for correct length · Clamp the work piece firmly · Make sure the tool is seated in the chuck properly |
| Tool Fracture | Cutting Conditions Tool Shape | · Feed rate is too fast · Cutting depth is too deep · Tool overhang is too long · Cutting edge is too long · Web thickness is too small | · Decrease cutting speed. · Reduce depth of cut · Reduce tool overhang as much as possible · Select a tool with a shorter cutting edge · Change to more appropriate web thickness |
| Shoulder Deflection | Cutting Conditions Tool Shape | · Feed rate is too fast · Cutting depth is too deep · Tool overhang is too long · Cutting on the down-cut · Helix angle is large · Web thickness is too thin | · Decrease cutting speed. · Reduce depth of cut · Adjust tool overhang for correct length · Change directions to up-cut · Use a tool with a smaller helix angle · Use a tool with the appropriate web thickness |
| Unsatisfactory Machined Surface Finish | Cutting Conditions | · Feed rate is too fast · Packing of chips | · Decrease cutting speed. · Use air blow · Use an insert with a larger relief pocket. |
| rs | | | | |
| Othe | Chattering | Cutting Conditions Tool Shape Machine Area | · Cutting speed is too fast · Cutting on the up-cut · Tool overhang is too long · Rake angle is large · Work clamps are weak · Tool is not firmly attached | · Decrease the cutting speed · Change directions to down-cut · Adjust tool overhang for correct length · Use a tool with an appropriate rake angle · Clamp the work piece firmly · Make sure the tool is seated in the chuck properly |
| Packing of Chips | Cutting Conditions Tool Shape | · Feed rate is too fast · Cutting depth is too deep · Too many teeth · Packing of chips | · Decrease cutting speed. · Reduce depth of cut · Reduce number of teeth · Use air blow |
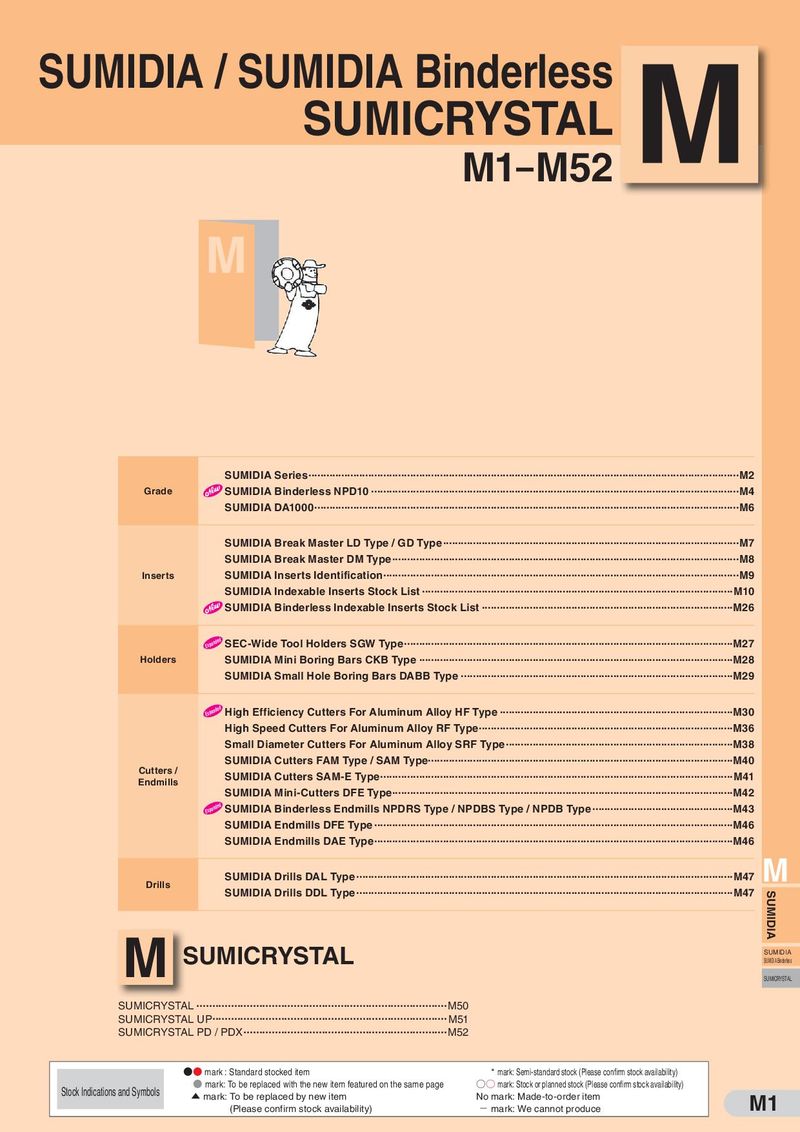 Каталог Sumitomo пластины с алмазными вставками Sumidia
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo токарные резцы (державки) для наружного точения
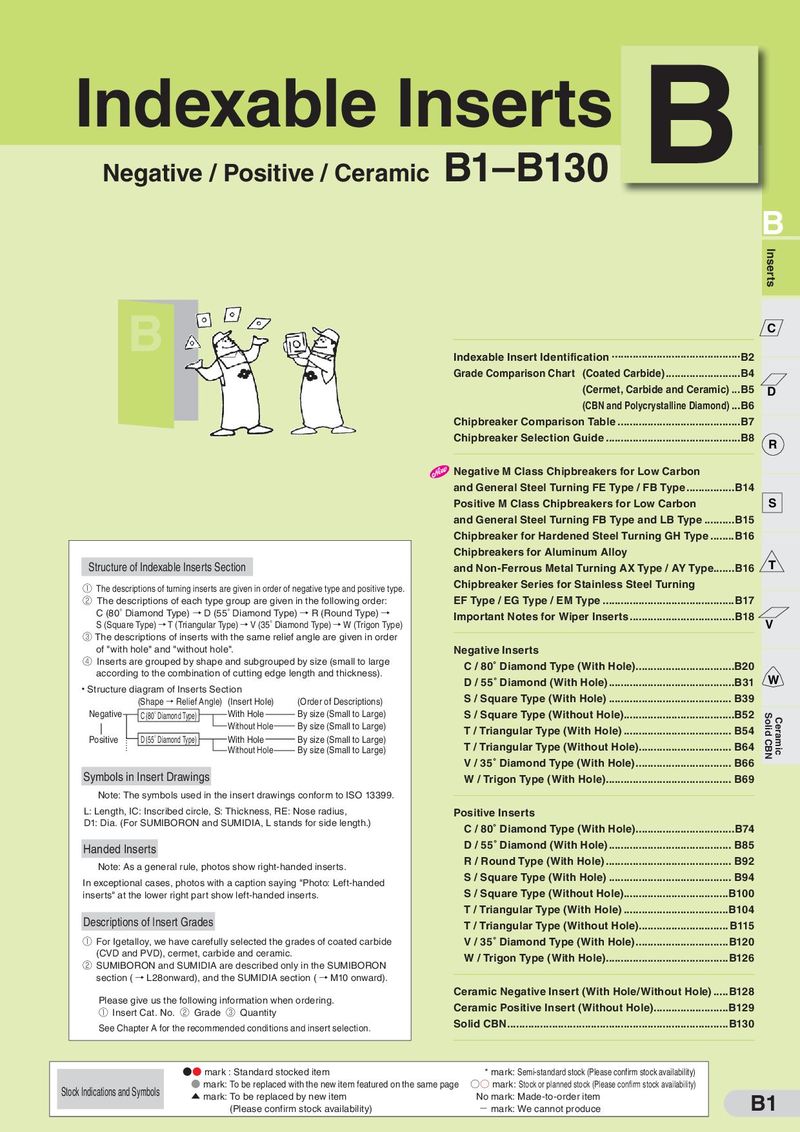 Каталог Sumitomo твердосплавные пластины
 Каталог Sumitomo фрезы со сменными пластинами
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal