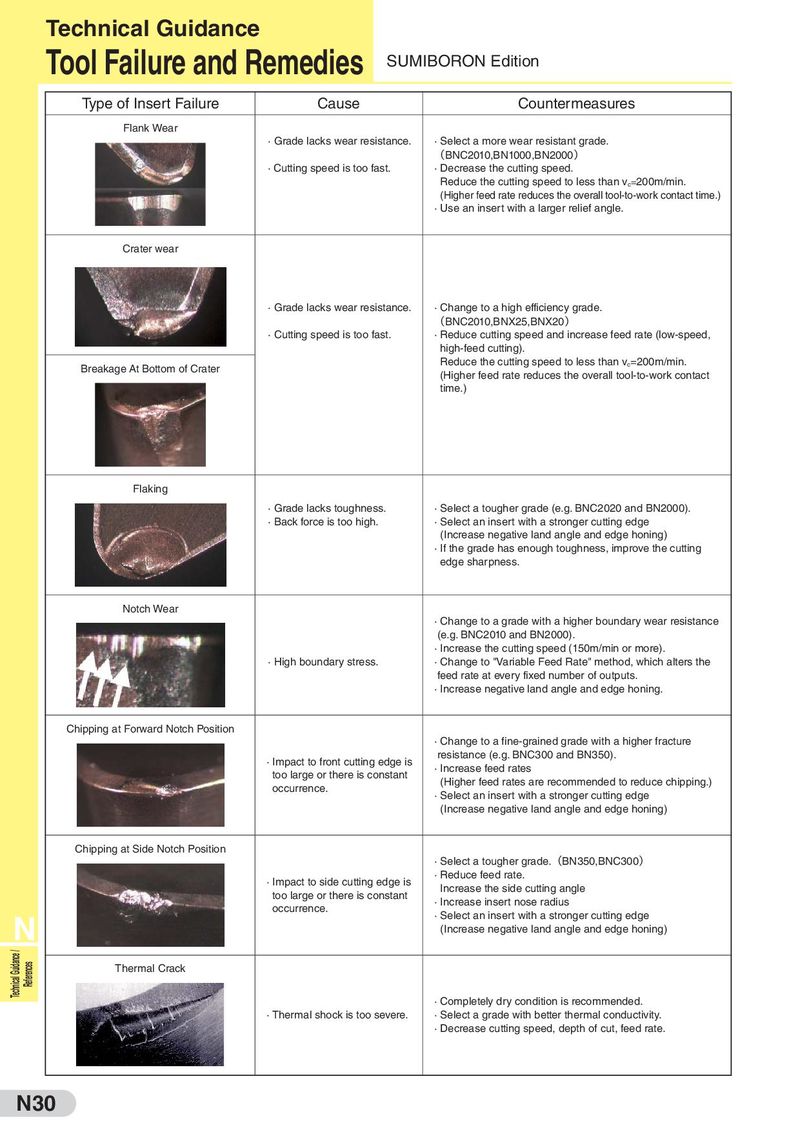
| Type of Insert Failure Flank Wear | Cause · Grade lacks wear resistance. · Cutting speed is too fast. | Countermeasures · Select a more wear resistant grade. `(`BNC2010,BN1000,BN2000`)` · Decrease the cutting speed. Reduce the cutting speed to less than vc=200m/min. (Higher feed rate reduces the overall tool-to-work contact time.) · Use an insert with a larger relief angle. |
| Crater wear Breakage At Bottom of Crater Flaking | · Grade lacks wear resistance. · Cutting speed is too fast. · Grade lacks toughness. · Back force is too high. | · Change to a high efficiency grade. `(`BNC2010,BNX25,BNX20`)` · Reduce cutting speed and increase feed rate (low-speed, high-feed cutting). Reduce the cutting speed to less than vc=200m/min. (Higher feed rate reduces the overall tool-to-work contact time.) · Select a tougher grade (e.g. BNC2020 and BN2000). · Select an insert with a stronger cutting edge (Increase negative land angle and edge honing) · If the grade has enough toughness, improve the cutting edge sharpness. |
| Notch Wear | · High boundary stress. | · Change to a grade with a higher boundary wear resistance (e.g. BNC2010 and BN2000). · Increase the cutting speed (150m/min or more). · Change to "Variable Feed Rate" method, which alters the feed rate at every fixed number of outputs. · Increase negative land angle and edge honing. |
| Chipping at Forward Notch Position | · Impact to front cutting edge is too large or there is constant occurrence. | · Change to a fine-grained grade with a higher fracture resistance (e.g. BNC300 and BN350). · Increase feed rates (Higher feed rates are recommended to reduce chipping.) · Select an insert with a stronger cutting edge (Increase negative land angle and edge honing) |
| Chipping at Side Notch Position | · Impact to side cutting edge is too large or there is constant occurrence. | · Select a tougher grade.`(`BN350,BNC300`)` · Reduce feed rate. Increase the side cutting angle · Increase insert nose radius · Select an insert with a stronger cutting edge (Increase negative land angle and edge honing) |
| Thermal Crack | · Thermal shock is too severe. | · Completely dry condition is recommended. · Select a grade with better thermal conductivity. · Decrease cutting speed, depth of cut, feed rate. |
 Каталог Sumitomo пластины с алмазными вставками Sumidia
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo токарные резцы (державки) для наружного точения
 Каталог Sumitomo твердосплавные пластины
 Каталог Sumitomo фрезы со сменными пластинами
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal