Техническая информация Sumitomo - страница 14
Навигация
 Каталог Sumitomo пластины с алмазными вставками Sumidia
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo токарные резцы (державки) для наружного точения
 Каталог Sumitomo твердосплавные пластины
 Каталог Sumitomo фрезы со сменными пластинами
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal
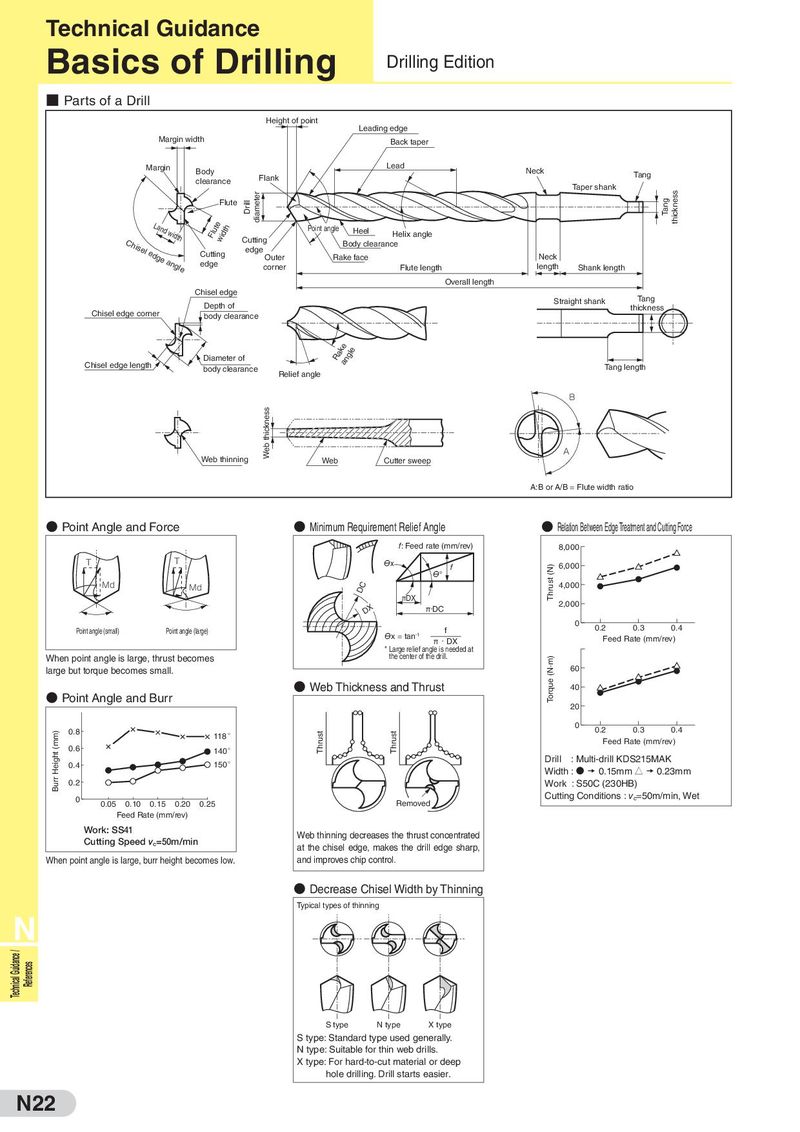
Basics of Drilling Drilling Edition
■ Parts of a Drill
Height of point Leading edge Margin width Back taper
Margin Lead
| Body | Neck | Tang | |||
| clearance | Flank | ||||
| Taper shank | |||||
| Flute |
| Land width | e | 先端角先端角 | ||
| Point angle | Heel | |||
| Flut | Helix angle |
| Chisel edge angle | width | Cutting | Body clearance |
| edge |
| Cutting | Outer | Rake face | Neck | ||
| edge | corner | Flute length | length | Shank length |
Overall length Chisel edge Straight shank Tang Depth of thickness
Chisel edge corner body clearance
ke Diameter of Ra Chisel edge length angle body clearance Tang length Relief angle B
A
Web thinning Web Cutter sweep
A:B or A/B = Flute width ratio
- Point Angle and Force
- Minimum Requirement Relief Angle
- Relation Between Edge Treatment and Cutting Force
f: Feed rate (mm/rev) 8,000 T T
| Ѳx | f | 6,000 | |
| Ѳ° |
Md Md 4,000
DC πDX ・ 2,000 DX π DC
0
| Point angle (small) | Point angle (large) | f | 0.2 | 0.3 | 0.4 | |
| Ѳx = tan -1 | ・ | Feed Rate (mm/rev) |
π DX * Large relief angle is needed at When point angle is large, thrust becomes the center of the drill. large but torque becomes small. 60
- Web Thickness and Thrust
- 40
Point Angle and Burr
20 0
| 0.8 | ° | 0.2 | 0.4 0.3 | |
| 118 | ||||
| Feed Rate (mm/rev) | ||||
| 0.6 | 140° | |||
| ° | Drill : Multi-drill KDS215MAK | |||
| 0.4 | 150 | D | J |
| Width : | 0.15mm | 0.23mm | ||
| 0.2 | Work : S50C (230HB) | |||
| Cutting Conditions : v =50m/min, Wet | ||||
| 0 | c |
0.05 0.10 0.15 0.20 0.25 Removed
Feed Rate (mm/rev) Work: SS41 Web thinning decreases the thrust concentrated Cutting Speed v =50m/min
c at the chisel edge, makes the drill edge sharp, When point angle is large, burr height becomes low. and improves chip control.
- Decrease Chisel Width by Thinning Typical types of thinning
N
S type N type X type
S type: Standard type used generally. N type: Suitable for thin web drills. X type: For hard-to-cut material or deep hole drilling. Drill starts easier.