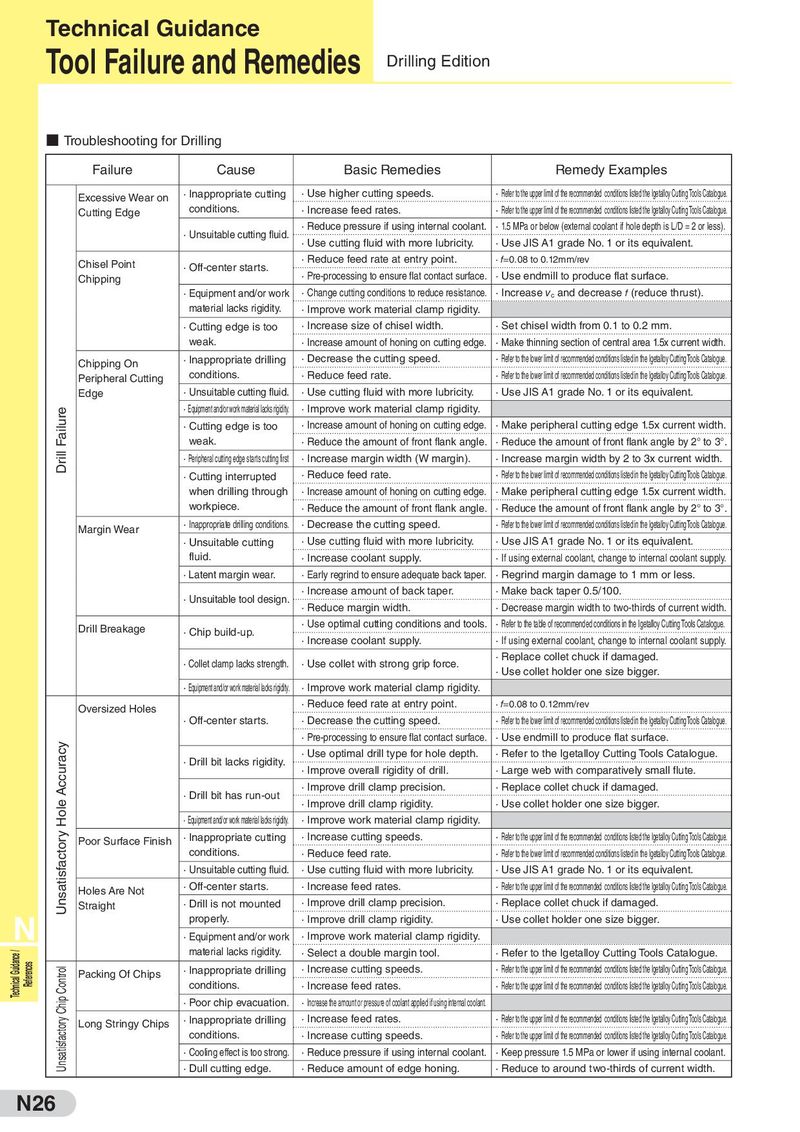
| Failure | Cause | Basic Remedies | Remedy Examples |
| Excessive Wear on | · Inappropriate cutting | · Use higher cuttingspeeds. | ·Refer to the upper limit of the recommended conditions listed the Igetalloy Cutting Tools Catalogue. |
| Cutting Edge | conditions. | · Increase feed rates. | ·Refer to the upper limit of the recommended conditions listed the Igetalloy CuttingTools Catalogue. |
| | | ·Reduce ressure if usininternal coolant | ·15 MPa or below (external coolant if hole deth is L/D = 2 or less) |
| | ·Unsuitable cutting fluid. | pg. · Use cuttingfluid with more lubricity. | . p . · Use JIS A1grade No. 1 or its equivalent. |
| Chisel Point | · Off-center starts. | · Reduce feed rate at entry point. | ·f=0.08 to 0.12mm/rev |
| Chipping | | ·Pre-processingto ensure flat contact surface. | · Use endmill toproduce flat surface. |
| | · Equipment and/or work | ·Change cutting conditions to reduce resistance. | · Increasevcand decreasef (reduce thrust). |
| | material lacks rigidity. | · Improve work material clamprigidity. | |
| | · Cutting edge is too | · Increase size of chisel width. | · Set chisel width from 0.1 to 0.2 mm. |
| | weak. | ·Increase amount of honingon cuttingedge. | ·Make thinningsection of central area 1.5x current width. |
| Chipping On | · Inappropriate drilling | · Decrease the cuttingspeed. | ·Refer to the lower limit of recommended conditions listed in the Igetalloy Cutting Tools Catalogue. |
| Peripheral Cutting | conditions. | · Reduce feed rate. | ·Refer to the lower limit of recommended conditions listed in the Igetalloy CuttingTools Catalogue. |
| Edge | ·Unsuitable cuttingfluid. | · Use cuttingfluid with more lubricity. | · Use JIS A1grade No. 1 or its equivalent. |
| re | | ·Equipment and/or work material lacks rigidity. | · Improve work material clamprigidity. | |
| ilu | | · Cutting edge is too | ·Increase amount of honingon cuttingedge. | ·Makeperipheral cuttingedge 1.5x current width. |
| Fa | | weak. | ·Reduce the amount of front flank angle. | ·Reduce the amount of front flank angle by2° to 3°. |
| rill | | ·Peripheral cutting edge starts cutting first | · Increase margin width(W margin). | · Increase margin width by2 to 3x current width. |
| D | | · Cutting interrupted | · Reduce feed rate. | ·Refer to the lower limit of recommended conditions listed in the Igetalloy Cutting Tools Catalogue. |
| | when drilling through | ·Increase amount of honingon cuttingedge. | ·Makeperipheral cuttingedge 1.5x current width. |
| | workpiece. | ·Reduce the amount of front flank angle. | ·Reduce the amount of front flank angle by2° to 3°. |
| Marin Wear | ·Inappropriate drilling conditions. | · Decrease the cuttingspeed. | ·Refer to the lower limit of recommended conditions listed in the Igetalloy Cutting Tools Catalogue. |
| g | · Unsuitable cutting | · Use cuttingfluid with more lubricity. | · Use JIS A1grade No. 1 or its equivalent. |
| | fluid. | · Increase coolant supply. | ·If usingexternal coolant, change to internal coolant supply. |
| | · Latent margin wear. | ·Earlyregrind to ensure adequate back taper. | · Regrind margin damage to 1 mm or less. |
| | | · Increase amount of back taper. | · Make back taper 0.5/100. |
| | ·Unsuitable tool design. | · Reduce margin width. | ·Decrease margin width to two-thirds of current width. |
| Drill Breakage | Chi bild- | ·Use optimal cuttingconditions and tools. | ·Refer to the table of recommended conditions in the Igetalloy Cutting Tools Catalogue. |
| | · p uup. | · Increase coolant supply. | ·If usingexternal coolant, change to internal coolant supply. |
| | ·Collet clamp lacks strength. | · Use collet with strong grip force. | · Replace collet chuck if damaged. · Use collet holder one size bigger. |
| | · Equipment and/or work material lacks rigidity. | · Improve work material clamprigidity. | |
| | | · Reduce feed rate at entrypoint | ·f=008 to 012mm/rev |
| Oversized Holes | · Off-center starts. | . · Decrease the cuttingspeed. | . . · Refer to the lower limit of recommended conditions listed in the Igetalloy Cutting Tools Catalogue. |
| | | ·Pre-processingto ensure flat contact surface. | · Use endmill toproduce flat surface. |
| curacy | | · Drill bit lacks rigidity. | · Use optimal drill type for hole depth. · Improve overall rigidityof drill. | · Refer to the IgetalloyCuttingTools Catalogue. · Large web with comparativelysmall flute. |
| Ac | | · Drill bit has run-out | · Improve drill clamp precision. | · Replace collet chuck if damaged. |
| le | | | · Improve drill clamprigidity. | · Use collet holder one size bigger. |
| Ho | | ·Equipment and/or work material lacks rigidity. | · Improve work material clamprigidity. | |
| ry | Poor Surface Finish | · Inappropriate cutting | · Increase cuttingspeeds. | ·Refer to the upper limit of the recommended conditions listed the Igetalloy Cutting Tools Catalogue. |
| cto | | conditions. | · Reduce feed rate. | · Refer to the lower limit of recommended conditions listed in the Igetalloy CuttingTools Catalogue. |
| isfa | | ·Unsuitable cuttingfluid. | · Use cuttingfluid with more lubricity. | · Use JIS A1grade No. 1 or its equivalent. |
| at | | · Off-center starts. | · Increase feed rates. | · Refer to the upper limit of the recommended conditions listed the Igetalloy Cutting Tools Catalogue. |
| ns | Holes Are Not Straight | · Drill is not mounted | · Improve drill clamp precision. | · Replace collet chuck if damaged. |
| U | | properly. | · Improve drill clamprigidity. | · Use collet holder one size bigger. |
| N | | · Equipment and/or work | · Improve work material clamprigidity. | |
| e / | | material lacks rigidity. | · Select a double margin tool. | · Refer to the IgetalloyCuttingTools Catalogue. |
| Guidanc ences rol | Pki Of Chi | · Inappropriate drilling | · Increase cuttingspeeds. | ·Refer to the upper limit of the recommended conditions listed the Igetalloy Cutting Tools Catalogue. |
| chnical Refer Cont | acng ps | conditions. | · Increase feed rates. | ·Refer to the upper limit of the recommended conditions listed the Igetalloy CuttingTools Catalogue. |
| Te hip | | ·Poor chipevacuation. | ·Increase the amount or pressure of coolant applied if using internal coolant. | |
| ory C | Long Stringy Chips | · Inappropriate drilling | · Increase feed rates. | ·Refer to the upper limit of the recommended conditions listed the Igetalloy Cutting Tools Catalogue. |
| fact | | conditions. | · Increase cuttingspeeds. | ·Refer to the upper limit of the recommended conditions listed the Igetalloy CuttingTools Catalogue. |
| atis | | ·Coolingeffect is too strong. | ·Reducepressure if usinginternal coolant. | ·Keep pressure 1.5 MPa or lower if usinginternal coolant. |
| Uns | | · Dull cuttingedge. | · Reduce amount of edge honing. | · Reduce to around two-thirds of current width. |
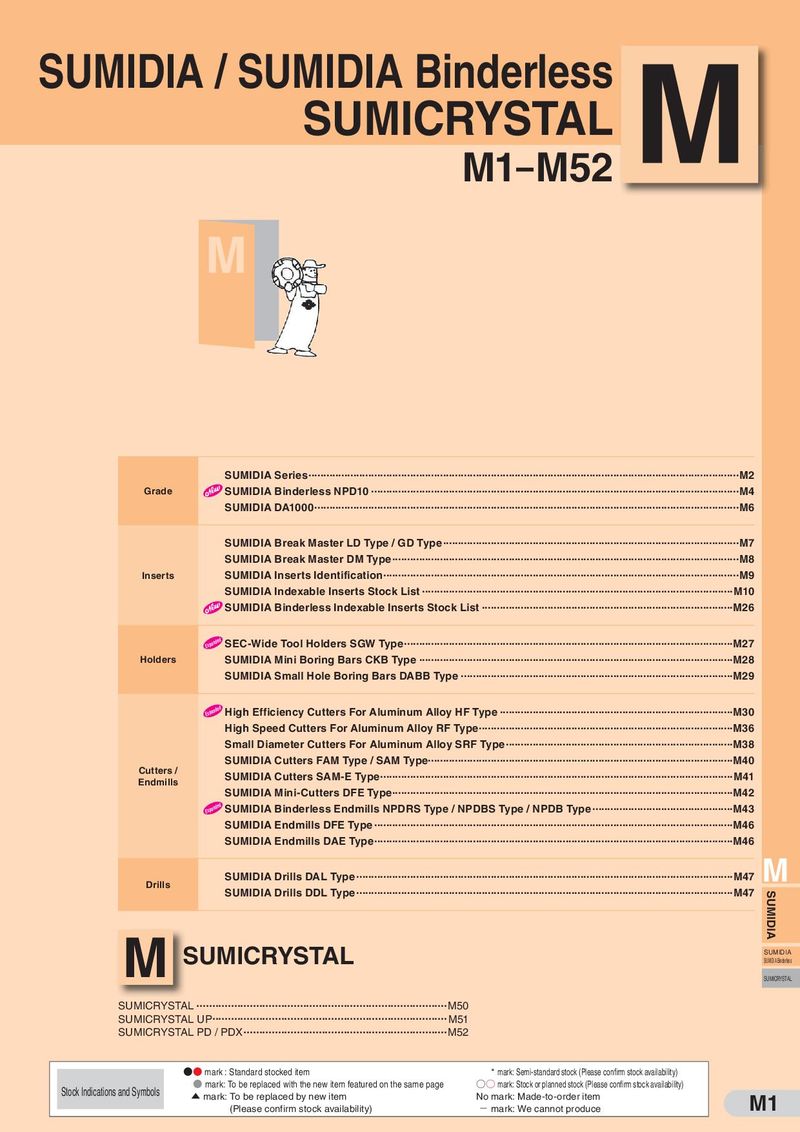 Каталог Sumitomo пластины с алмазными вставками Sumidia
 Общий каталог Sumitomo 2019 - 2020
 Каталог Sumitomo токарные резцы (державки) для наружного точения
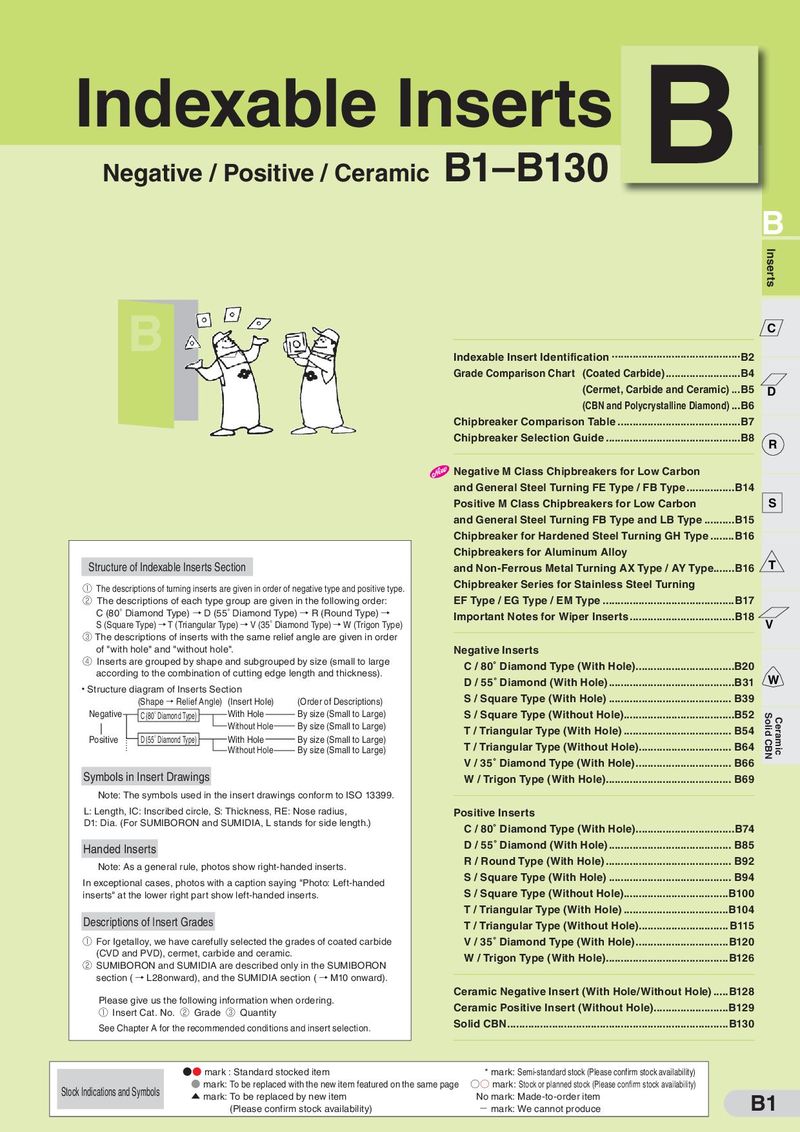 Каталог Sumitomo твердосплавные пластины
 Каталог Sumitomo фрезы со сменными пластинами
 Каталог Sumitomo пластины с режущей кромкой-моноалмаз Sumicristal