Каталог Sumitomo сплавы и режимы - страница 32
Навигация
 Каталог Sumitomo токарные резцы (державки) для наружного точения
 Каталог Sumitomo сверла и развертки
 Каталог Sumitomo запасные части
 Каталог Sumitomo микроинструмент
 Каталог Sumitomo фрезы со сменными пластинами
Polycrystalline Diamond
SUMIDIA Binderless Series
SUMIDIA Binderless Series uses nano-polycrystalline diamond for the cutting edge and demonstrates
excellent wear and fracture resistance compared to conventional sintered diamond tools.
In particular, SUMIDIA Binderless Series allows for improvements in tool life and machining precision
A that go far beyond conventional diamond tools in the machining of hard brittle materials, such as carbide.
- Excellent for High Precision Machining of Carbide Nano-polycrystalline diamond with excellent wear resistance achieves high precision machining of carbide.
- Maintains Superior Dimensional Tolerances Over Many Hours Greatly reduces the number of tool replacements compared to conventional diamond tools, and increases work efficiency while reducing total costs.
- Suitable for Hard Brittle Material Machining Hard brittle materials (such as ceramics) that could only be ground before can now be cut.
Characteristics
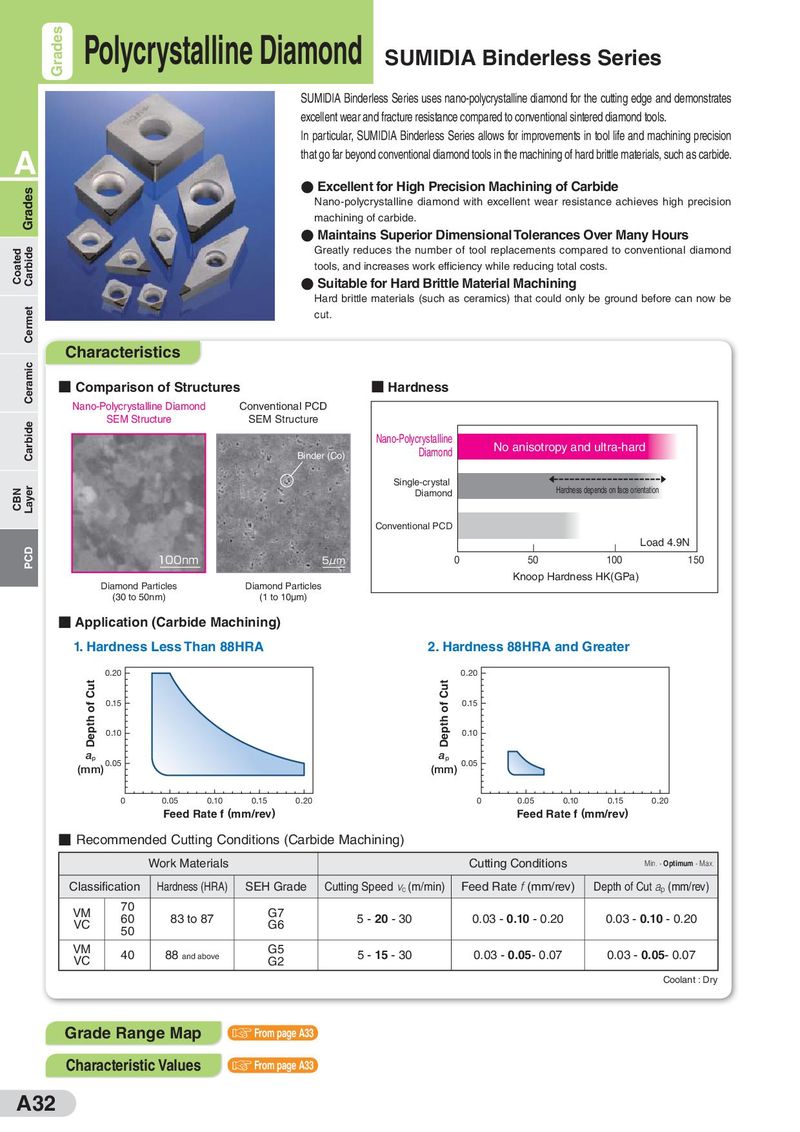
- Comparison of Structures
- Hardness
Nano-Polycrystalline Diamond Conventional PCD SEM Structure SEM Structure Nano-Polycrystalline No anisotropy and ultra-hard Diamond Binder (Co)
Single-crystal Diamond Hardness depends on face orientation
Conventional PCD Load 4.9N
100nm 5μm 0 50 100 150
Knoop Hardness HK(GPa) Diamond Particles Diamond Particles (30 to 50nm) (1 to 10μm)
- Application (Carbide Machining) 1. Hardness Less Than 88HRA 2. Hardness 88HRA and Greater
0.20 0.20
0.15 0.15
0.10 0.10
a p ap 0.05 0.05 (mm) (mm)
0 0.05 0.10 0.15 0.20 0 0.05 0.10 0.15 0.20
Feed Rate f (mm/rev) Feed Rate f (mm/rev)
- Recommended Cutting Conditions (Carbide Machining)
| Work Materials | Cutting Conditions | Min. -Optimum- Max. | ||||
| Classifi | cation | Hardness (HRA) | SEH Grade | Cutting Speed vc(m/min) | Feed Ratef(mm/rev) | Depth of Cutap(mm/rev) |
| VM VC | 70 60 50 | 83 to 87 | G7 G6 | 5 -20- 30 | 0.03 -0.10- 0.20 | 0.03 -0.10- 0.20 |
| VM VC | 40 | 88and above | G5 G2 | 5 -15- 30 | 0.03 -0.05- 0.07 | 0.03 -0.05- 0.07 |
| Coolant : Dry |