Каталог Sumitomo сплавы и режимы - страница 11
Навигация
 Каталог Sumitomo токарные резцы (державки) для наружного точения
 Каталог Sumitomo сверла и развертки
 Каталог Sumitomo запасные части
 Каталог Sumitomo микроинструмент
 Каталог Sumitomo фрезы со сменными пластинами
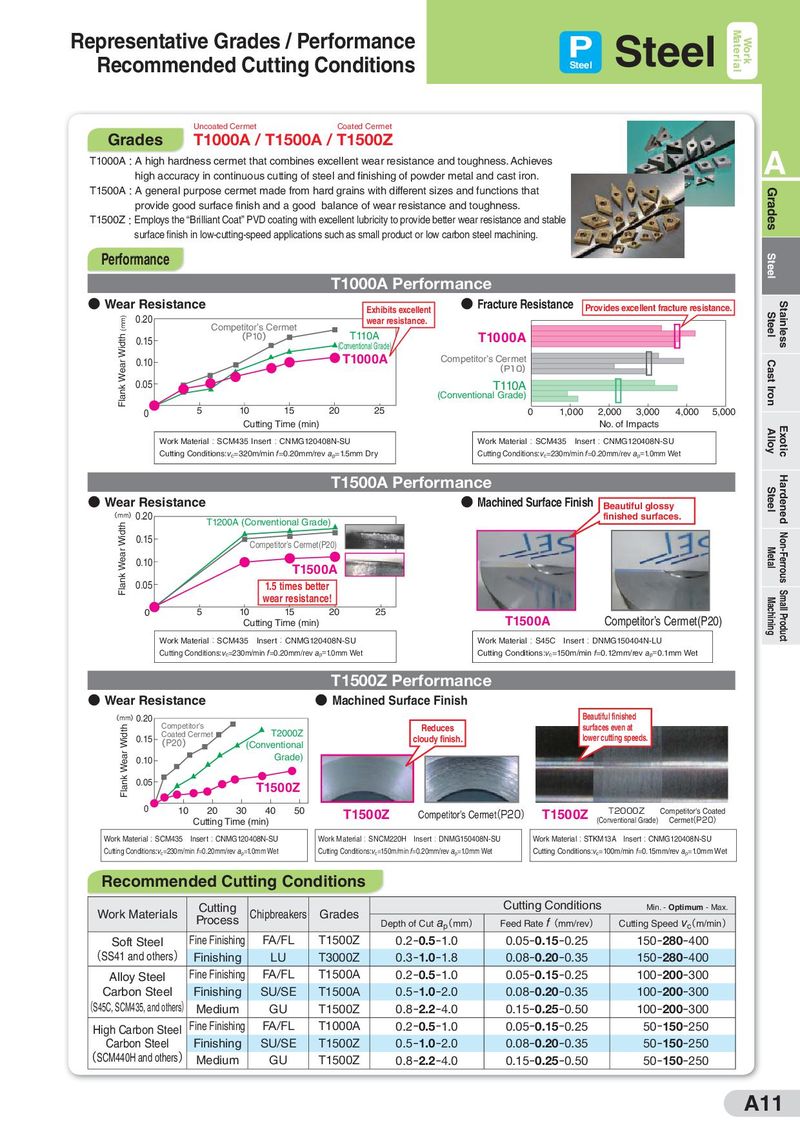
Representative Grades / Performance P Steel
Uncoated Cermet Coated Cermet
Grades T1000A / T1500A / T1500Z
: A T1000A A high hardness cermet that combines excellent wear resistance and toughness. Achieves high accuracy in continuous cutting of steel and finishing of powder metal and cast iron. T1500A : A general purpose cermet made from hard grains with different sizes and functions that provide good surface finish and a good balance of wear resistance and toughness. T1500Z : Employs the “Brilliant Coat” PVD coating with excellent lubricity to provide better wear resistance and stable surface finish in low-cutting-speed applications such as small product or low carbon steel machining.
Performance
T1000A Performance
- Wear Resistance
- Fracture Resistance
Exhibits excellent Provides excellent fracture resistance. 0.20 wear resistance. Competitor’s Cermet
| (P10) | T110A | T1000A | |||
| 0.15 | |||||
| (Conventional Grade) | |||||
| T1000A | Competitor’s Cermet |
| 0.10 | ( | ) | |
| P10 | |||
| 0.05 | T110A | ||
| (Conventional Grade) |
| 0 | 5 | 10 | 15 | 20 | 25 | 0 | 1,000 | 2,000 | 3,000 | 4,000 | 5,000 |
| Cutting Time (min) | No. of Impacts |
| Work Material:SCM435 Insert:CNMG120408N-SU | Work Material:SCM435 | Insert:CNMG120408N-SU |
| Cutting Conditions:v =320m/min f=0.20mm/rev a =1.5mm Dry | Cutting Conditions:v =230m/min f=0.20mm/rev a =1.0mm Wet |
c p c p
T1500A Performance
- Wear Resistance
- Machined Surface Finish
Beautiful glossy (mm )0.20 finished surfaces. T1200A (Conventional Grade) 0.15 Competitor’s Cermet(P20) 0.10
T1500A
0.05 1.5 times better wear resistance!
0 5 10 15 20 25
Cutting Time (min) T1500A Competitor’s Cermet(P20)
| Work Material:SCM435 | Insert:CNMG120408N-SU | Work Material:S45C | Insert:DNMG150404N-LU |
| Cutting Conditions:v =230m/min f=0.20mm/rev a =1.0mm Wet | Cutting Conditions:v =150m/min f=0.12mm/rev a =0.1mm Wet |
c p c p
T1500Z Performance
- Wear Resistance
- Machined Surface Finish
(mm )0.20 Beautiful finished
| Competitor's | Reduces | surfaces even at | |||
| Coated Cermet | T2000Z | ||||
| 0.15 ( | ) | cloudy finish. | lower cutting speeds. | ||
| P20 | (Conventional | ||||
| 0.10 | Grade) | ||||
| 0.05 | T1500Z |
| 0 | 10 | 20 | 30 | 40 | 50 | T1500Z | (P20) | T1500Z | T2000Z | Competitor's Coated | |
| Competitor’s Cermet |
Cutting Time (min) (Conventional Grade) Cermet(P20)
| Work Material:SCM435 | Insert:CNMG120408N-SU | Work Material:SNCM220H | Insert:DNMG150408N-SU | Work Material:STKM13A | Insert:CNMG120408N-SU |
| Cutting Conditions:v =230m/min f=0.20mm/rev a =1.0mm Wet | Cutting Conditions:v =150m/min f=0.20mm/rev a =1.0mm Wet | Cutting Conditions:v =100m/min f=0.15mm/rev a =1.0mm Wet |
c p c p c p
Recommended Cutting Conditions
| Work Materials | Cutting P | Chipbreakers | Grades | CuttingConditions | Min. -Optimum- Max. | |
| rocess | Depth of Cut ap(mm) | Feed Rate f (mm/rev) | Cutting Speed vc(m/min) | |||
| Soft Steel | Fine Finishing | FA/FL | T1500Z | 0.2-0.5-1.0 | 0.05-0.15-0.25 | 150-280-400 |
| (SS41 and others) | Finishing | LU | T3000Z | 0.3-1.0-1.8 | 0.08-0.20-0.35 | 150-280-400 |
| Alloy Steel | Fine Finishing | FA/FL | T1500A | 0.2-0.5-1.0 | 0.05-0.15-0.25 | 100-200-300 |
| Carbon Steel | Finishing | SU/SE | T1500A | 0.5-1.0-2.0 | 0.08-0.20-0.35 | 100-200-300 |
| (S45C, SCM435, and others) | Medium | GU | T1500Z | 0.8-2.2-4.0 | 0.15-0.25-0.50 | 100-200-300 |
| High Carbon Steel | Fine Finishing | FA/FL | T1000A | 0.2-0.5-1.0 | 0.05-0.15-0.25 | 50-150-250 |
| Carbon Steel | Finishing | SU/SE | T1500Z | 0.5-1.0-2.0 | 0.08-0.20-0.35 | 50-150-250 |
| (SCM440H and others) | Medium | GU | T1500Z | 0.8-2.2-4.0 | 0.15-0.25-0.50 | 50-150-250 |