| Work Materials | Grades | Binder | CBN Content (%) G | rain Size (μm) | Hardness HV (GPa) | TRS (GPa) | Main Coating Components C | oating Thickness (μ | m) Characteristics |
| BNC2010 | TiCN | 50 to 55 | 2 | 30 to 32 | 1.10 to 1.20 | TiCN multi- layered | 1.5 | Improves the wear resistance of coating and substrate and stably achieves excellent surface roughness. |
| BNC2020 | TiN | 70 to 75 | 5 | 34 to 36 | 1.20 to 1.30 | TiAlN multi- layered | 1.5 | Provides long tool life in general and high-efficiency cutting thanks to tough substrate coated with a highly wear-resistant and highly adhesive layer. |
| BNC300 | TiN | 60 to 65 | 1 | 33 to 35 | 1.15 to 1.25 | TiAIN | 1 | Suited for finishing when there is a combination of continuous and interrupted cutting. |
| BNC100 | TiN | 40 to 45 | 1 | 29 to 32 | 1.05 to 1.15 | TiAIN/TiCN | 2 | Highly wear resistant coating makes this grade suited for high speed finishing. |
| BNC160 | TiN | 60 to 65 | 3 | 31 to 33 | 1.10 to 1.20 | TiAIN/TiCN | 2 | Stable, high precision finishing of hardened steel. |
| H | BNC200 | TiN | 65 to 70 | 4 | 33 to 35 | 1.15 to 1.25 | TiAIN | 2 | Tough substrate with high wear resistant coating provide longer tool life. |
| Hardened Steel | BN1000 | TiCN | 40 to 45 | 1 | 27 to 31 | 0.90 to 1.00 | | | Ultimate wear and fracture resistance. Suited to high-speed cutting. |
| BN2000 | TiN | 50 to 55 | 2 | 31 to 34 | 1.05 to 1.15 | | | A general purpose grade for hardened steel that provides a high degree of fracture and wear resistance. |
| BNX20 | TiN | 55 to 60 | 3 | 31 to 33 | 0.95 to 1.10 | | | Crater resistant grade, suitable for high efficiency cutting under high temperature conditions. |
| BN350 | TiN | 60 to 65 | 1 | 33 to 35 | 1.20 to 1.30 | | | High cutting edge strength, suited to heavy interrupted cutting. |
| BNX10 | TiCN | 40 to 45 | 3 | 27 to 31 | 0.80 to 0.90 | | | Optimum wear resistance. Suited to continuous, high-speed cutting. |
| BNX25 | TiN | 65 to 70 | 4 | 29 to 31 | 1.00 to 1.10 | | | Excellent fracture resistance during high speed cutting. Suited to high speed interrupted cutting of hardened steel. |
| Sintered | BN7500 | Co Compound | 90 to 95 | 1 | 41 to 44 | 1.40 to 1.50 | | | Maintains optimum cutting edge sharpness. Suited for finishing of sintered alloy. |
| alloy | BN7000 | Co Compound | 90 to 95 | 2 | 41 to 44 | 1.30 to 1.40 | | | Improved wear and fracture resistance in rough cutting of sintered components. |
| BNS800 | Al Alloy | 85 to 90 | 8 | 39 to 42 | 0.95 to 1.10 | | | 100% solid CBN structure with good thermal impact resistance. |
| K | BN7000 | Co Compound | 90 to 95 | 2 | 41 to 44 | 1.30 to 1.40 | | | Improved wear and fracture resistance in rough cutting of cast iron and exotic alloy. |
| Cast Iron | BN500 | TiC | 65 to 70 | 6 | 32 to 34 | 1.00 to 1.10 | | | Optimized for cast iron cutting. Maintains good wear and fracture resistance. |
| BNC500 `(`For Ductile Cast Iron`)` | TiC | 60 to 65 | 4 | 32 to 34 | 1.00 to 1.10 | TiAIN | 2 | Substrate with excellent wear resistance and coating makes this grade suited for hard-to-cut cast iron. |
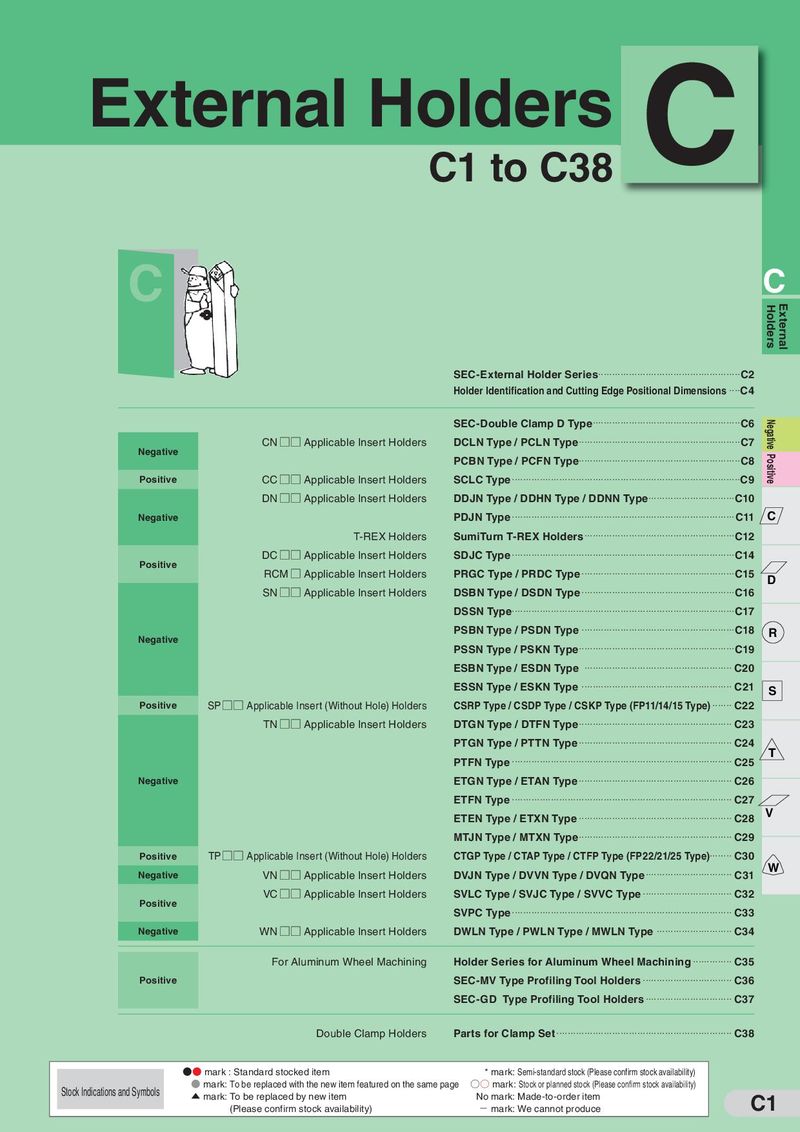 Каталог Sumitomo токарные резцы (державки) для наружного точения
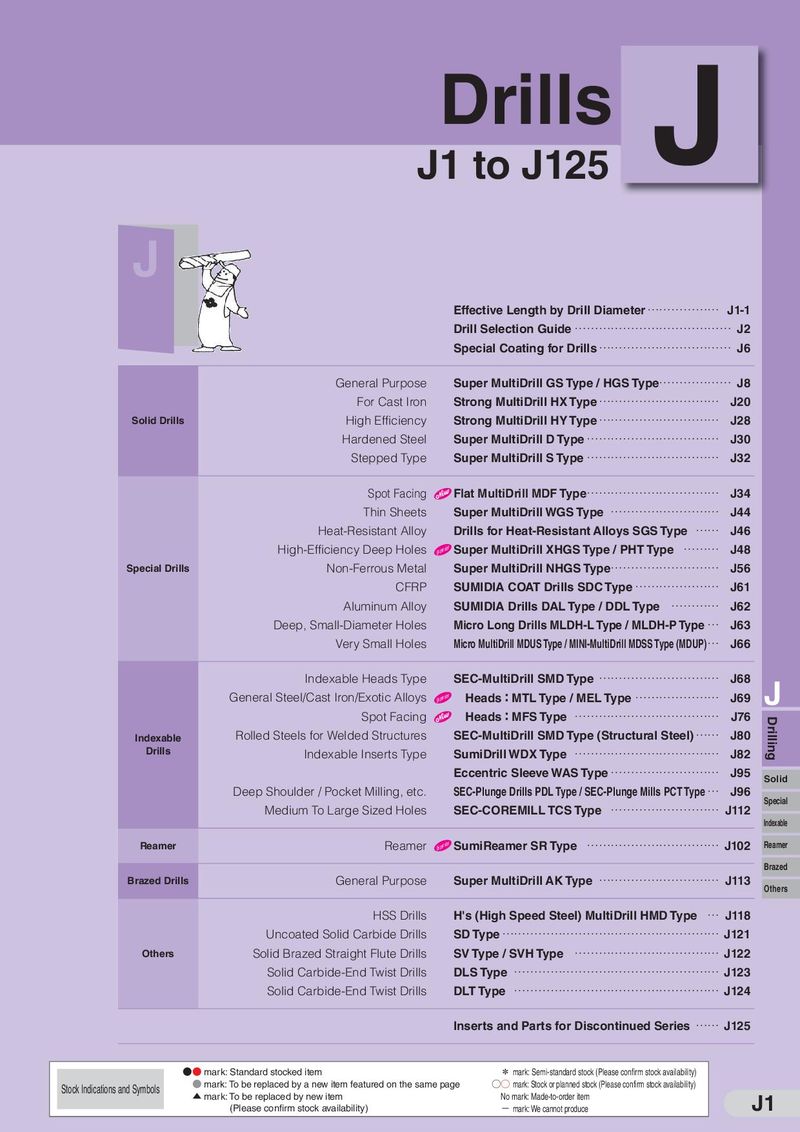 Каталог Sumitomo сверла и развертки
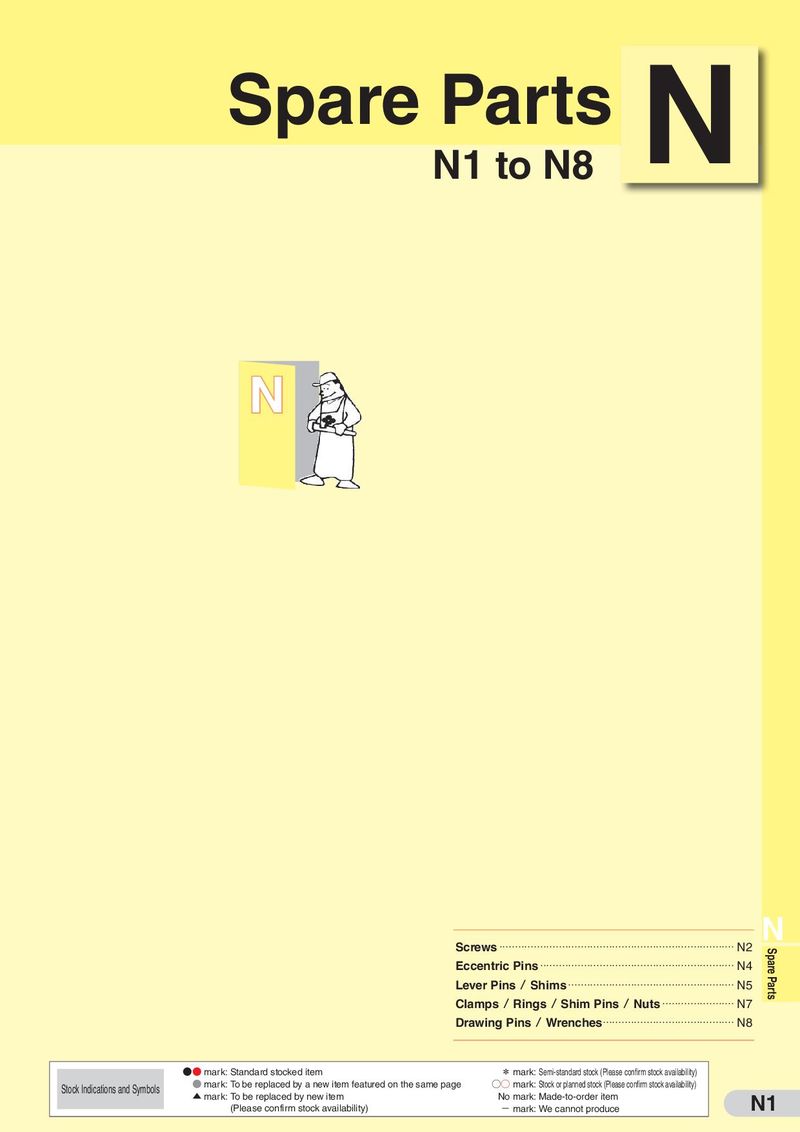 Каталог Sumitomo запасные части
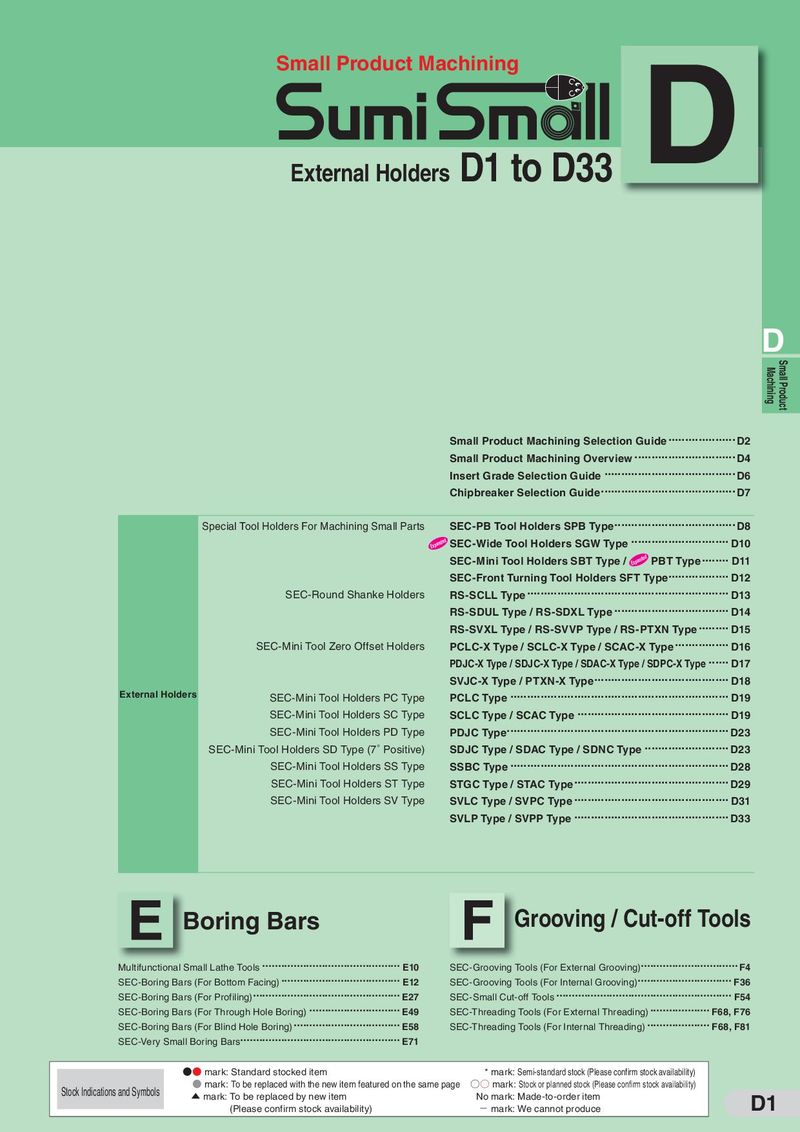 Каталог Sumitomo микроинструмент
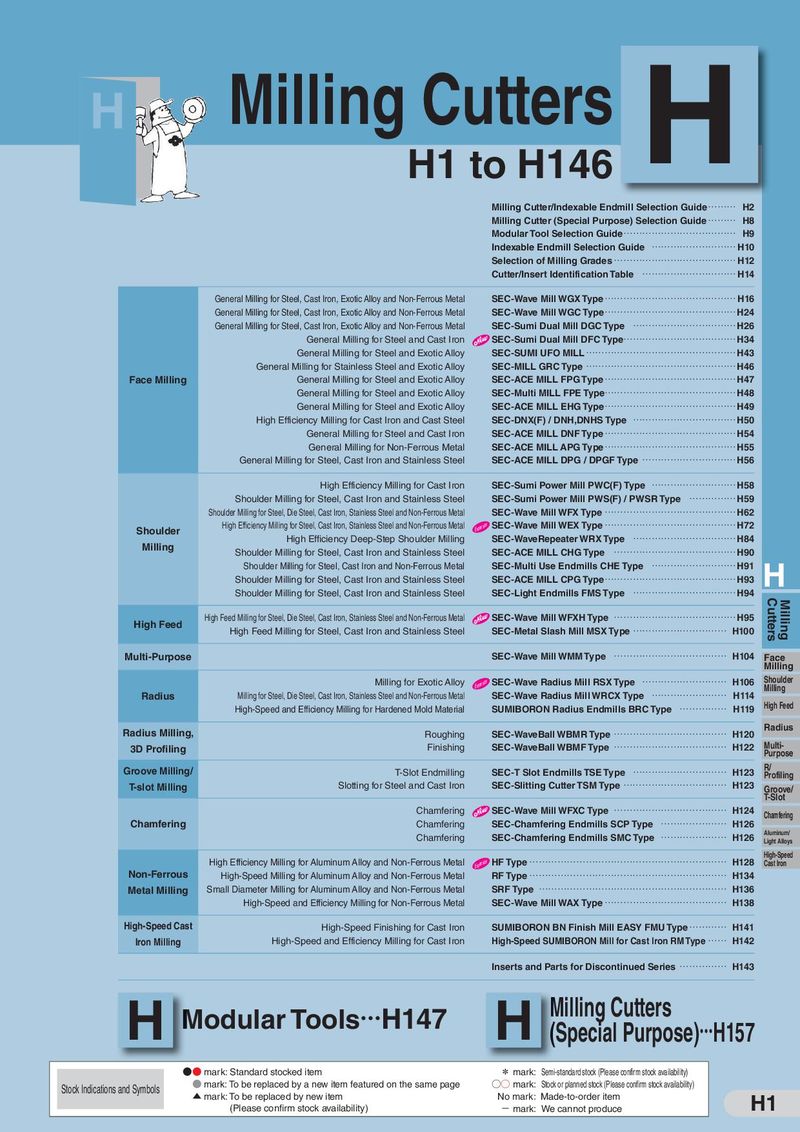 Каталог Sumitomo фрезы со сменными пластинами
