Каталог Sumitomo сплавы и режимы - страница 10
Навигация
 Каталог Sumitomo токарные резцы (державки) для наружного точения
 Каталог Sumitomo сверла и развертки
 Каталог Sumitomo запасные части
 Каталог Sumitomo микроинструмент
 Каталог Sumitomo фрезы со сменными пластинами
Steel P Representative Grades /
Performance
| High Speed Cutting | General Purpose Cutting | Interrupted Cutting | Small Product Machining | ||
| A | Grades | AC810P / | AC8025P / AC830P / | AC1030U |
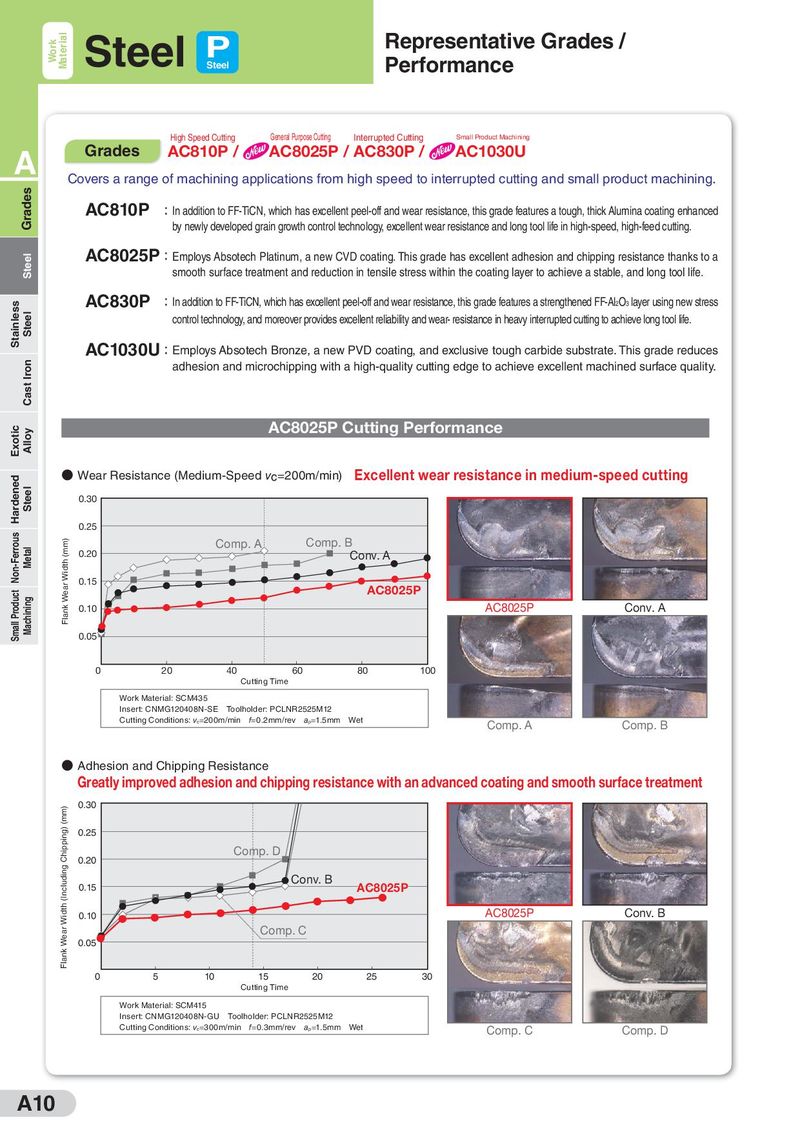
Covers a range of machining applications from high speed to interrupted cutting and small product machining. AC810P : In addition to FF-TiCN, which has excellent peel-off and wear resistance, this grade features a tough, thick Alumina coating enhanced by newly developed grain growth control technology, excellent wear resistance and long tool life in high-speed, high-feed cutting. AC8025P: Employs Absotech Platinum, a new CVD coating. This grade has excellent adhesion and chipping resistance thanks to a
smooth surface treatment and reduction in tensile stress within the coating layer to achieve a stable, and long tool life. AC830P : In addition to FF-TiCN, which has excellent peel-off and wear resistance, this grade features a strengthened FF-Al O layer using new stress 2 3 control technology, and moreover provides excellent reliability and wear- resistance in heavy interrupted cutting to achieve long tool life.
AC1030U: Employs Absotech Bronze, a new PVD coating, and exclusive tough carbide substrate. This grade reduces
adhesion and microchipping with a high-quality cutting edge to achieve excellent machined surface quality.
AC8025P Cutting Performance
- Wear Resistance (Medium-Speed vc=200m/min) Excellent wear resistance in medium-speed cutting 0.30
0.25
Comp. A Comp. B
| 0.20 | ◆ | ◆ | ◆ | Conv. A | ● | |
| 0.15 | ◆ | ● | ● | ● | ● |
- AC8025P
| 0.10 | ● ● | ● | ● | AC8025P | Conv. A |
| 0.05 |
| 0 | 20 | 40 | 60 | 80 | 100 | ||
| Cutting Time | |||||||
| Work Material: SCM435 | |||||||
| Insert: CNMG120408N-SE | Toolholder: PCLNR2525M12 |
Cutting Conditions: vc=200m/min f=0.2mm/rev ap=1.5mm Wet Comp. A Comp. B
- Adhesion and Chipping Resistance Greatly improved adhesion and chipping resistance with an advanced coating and smooth surface treatment 0.30
0.25
Comp. D
0.20 ■ ■ Conv. B
0.15 ■● ◆ AC8025PAC8025P
- AC8025P Conv. B
| 0.10 | ●◆ | ● | ||
| ◆ | Comp. C | |||
| 0.05 |
| 0 | 5 | 10 | 15 | 20 | 25 | 30 | |||
| Cutting Time | |||||||||
| Work Material: SCM415 | |||||||||
| Insert: CNMG120408N-GU | Toolholder: PCLNR2525M12 |
Cutting Conditions: v =300m/min f=0.3mm/rev a =1.5mm Wet Comp. C Comp. D
c p