Каталог Sumitomo сплавы и режимы - страница 16
Навигация
 Каталог Sumitomo токарные резцы (державки) для наружного точения
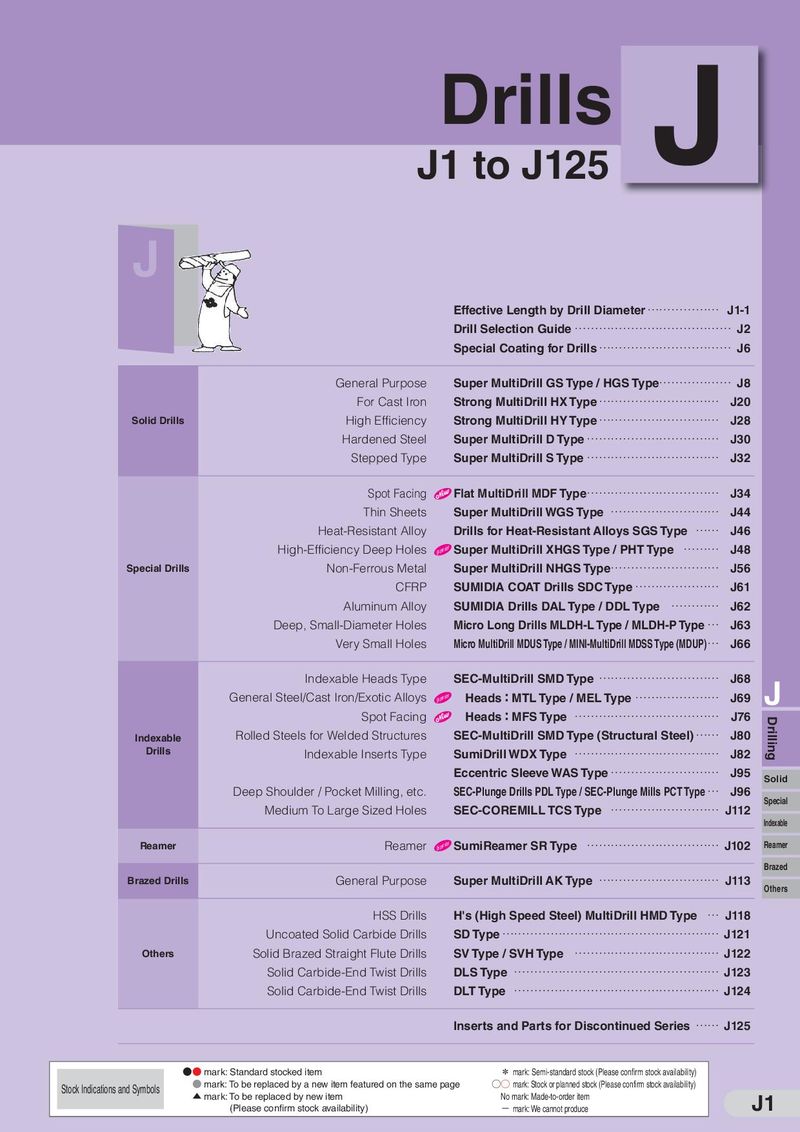 Каталог Sumitomo сверла и развертки
 Каталог Sumitomo запасные части
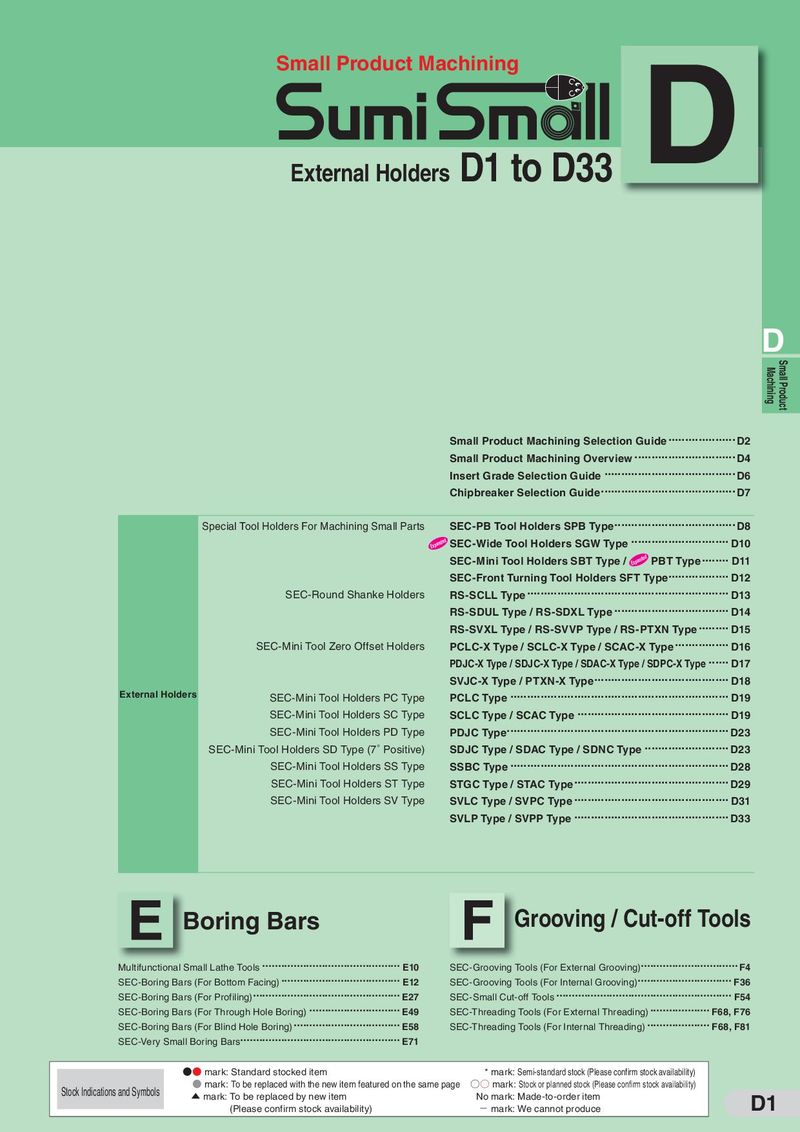 Каталог Sumitomo микроинструмент
 Каталог Sumitomo фрезы со сменными пластинами
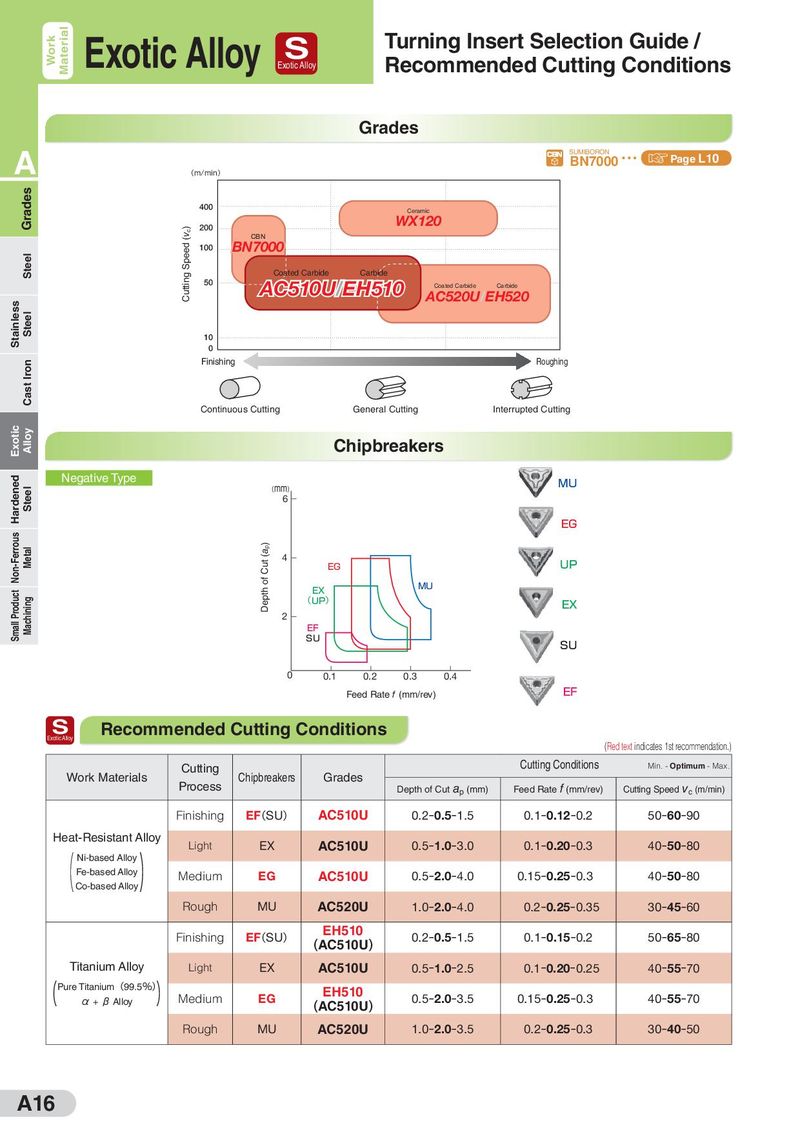
Exotic Alloy S Turning Insert Selection Guide /
Exotic Alloy
| Finishin 400 200 100 50 10 0 (m/min) Cutting Speed (vc) | g BN7000 Coated CBN AC5 | Gr Carbide Carbi 10U/EH5 | ades WX120 Ceramic AC520U/E Coated Carbide de 10 | SUMIBORON BN700 Roughing H520 Carbide | 0 PageL10 | |
| Continu | ous Cutting | Gener | al Cutting I | nterrupted Cutting | ||
| Chipb | reakers | |||||
| Negative Type | 6 4 2 0 (mm) Depth of Cut (ap) | Feed Ra EG EX (UP) EF SU 0.2 0.1 | tef(mm/rev) MU 0.3 0.4 | MU EX SU UP EG EF | ||
| S Exotic Alloy Recomm | ended | Cutting | Condition | s | (R | ed textindicates 1st recommendation.) |
| Cutting Conditions | Min -Optimum- Max | |||||
| Wk Mtil | Cutting | Chibk | Gd | .. | ||
| or aeras | Process | preaers | raes | Depth of Cut ap(mm) | Feed Rate f(mm/rev) | Cutting Speed vc(m/min) |
| Finishing | EF(SU) | AC510U | 0.2-0.5-1.5 | 0.1-0.12-0.2 | 50-60-90 | |
| Heat-Resistant Alloy Ni-based Alloy | Light | EX | AC510U | 0.5-1.0-3.0 | 0.1-0.20-0.3 | 40-50-80 |
| `(` ) Fe-based Alloy Co-based Alloy | Medium | EG | AC510U | 0.5-2.0-4.0 | 0.15-0.25-0.3 | 40-50-80 |
| Rough | MU | AC520U | 1.0-2.0-4.0 | 0.2-0.25-0.35 | 30-45-60 | |
| Finishing | EF(SU) | EH510 (AC510U) | 0.2-0.5-1.5 | 0.1-0.15-0.2 | 50-65-80 | |
| Titanium Alloy | Light | EX | AC510U | 0.5-1.0-2.5 | 0.1-0.20-0.25 | 40-55-70 |
| ( Pure Titanium(99.5%)) α+βAlloy | Medium | EG | EH510 (AC510U) | 0.5-2.0-3.5 | 0.15-0.25-0.3 | 40-55-70 |
| Rough | MU | AC520U | 1.0-2.0-3.5 | 0.2-0.25-0.3 | 30-40-50 |