Общий каталог TooTool - страница 51
Навигация
 Каталог TooTool техническая информация 1
 Каталог TooTool монолитные фрезы
 Каталог TooTool техническая информация 2
- 页 1
- 页 2
- 页 3
- 页 4
- 页 5
- 页 6
- 页 7
- 页 8
- 页 9
- 页 10
- 页 11
- 页 12
- 页 13
- 页 14
- 页 15
- 页 16
- 页 17
- 页 18
- 页 19
- 页 20
- 页 21
- 页 22
- 页 23
- 页 24
- 页 25
- 页 26
- 页 27
- 页 28
- 页 29
- 页 30
- 页 31
- 页 32
- 页 33
- 页 34
- 页 35
- 页 36
- 页 37
- 页 38
- 页 39
- 页 40
- 页 41
- 页 42
- 页 43
- 页 44
- 页 45
- 页 46
- 页 47
- 页 48
- 页 49
- 页 50
- 页 51
- 页 52
- 页 53
- 页 54
- 页 55
- 页 56
- 页 57
- 页 58
- 页 59
- 页 60
- 页 61
- 页 62
- 页 63
- 页 64
- 页 65
- 页 66
- 页 67
- 页 68
- 页 69
- 页 70
- 页 71
- 页 72
- 页 73
- 页 74
- 页 75
- 页 76
- 页 77
- 页 78
- 页 79
- 页 80
- 页 81
- 82: 新增页码2
- 页 83
- 页 84
- 页 85
- 页 86
- 页 87
- 页 88
- 页 89
- 页 90
- 页 91
- 页 92
- 页 93
- 页 94
- 页 95
- 页 96
- 页 97
- 页 98
- 页 99
- 页 100
- 页 101
- 页 102
- 页 103
- 页 104
- 页 105
- 页 106
- 页 107
- 页 108
- 页 109
- 页 110
- 页 111
- 页 112
- 页 113
- 页 114
- 页 115
- 页 116
- 页 117
- 页 118
- 页 119
- 页 120
- 页 121
- 页 122
- 页 123
- 页 124
- 页 125
- 页 126
- 页 127
- 页 128
- 页 129
- 页 130
- 页 131
- 页 132
- 页 133
- 页 134
- 页 135
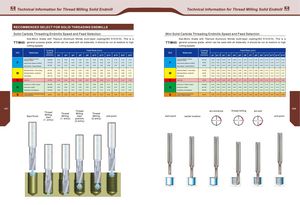
Technical Information for Thread Milling Solid Endmill Technical Information for Thread Milling Solid Endmill
RECOMMENDED SELECT FOR SOLID THREADING ENDMILLS
Solid Carbide Threading Endmills Speed and Feed Selection Mini Solid Carbide Threading Endmills Speed and Feed Selection
Sub - Micro Grade with Titanium Aluminum Nitride multi - layer coating ( ISO K 10 - K 10 ) . This is a Sub - Micro Grade with Titanium Aluminum Nitride multi - layer coating ( ISO K 10 - K 10 ) . This is a
TTIM 45 general purpose grade , which can be used with all materials ; It should be run at medium to high TTIM 45 general purpose grade , which can be used with all materials ; It should be run at medium to high
cutting speeds . cutting speeds .
Cutting Feed Rate ( mm ) Feed Rate ( mm )
ISO Materials Speed ISO Materials
( m / min ) cp 2 cp 3 cp4 cp 6 cp8 cp 10 cp12 cp 14 cp16 cp 20 cp25 cp 5 cp 6 cp7 cp8 cp9 cp10 cp12 (p14 cp16
Low and Medium Carbon Low and Medium Carbon
100 - 250 0.03 0.04 0.04 0.06 0.07 0.08 0.09 0.11 0.12 0.15 0.18 60- 120 0.04 0.05 0.05 0.07 0.09 0.11 0.13 0.14 0.15 0.16 0.16 0.17 0.18 0.18
Steels < 0.55 %C Steels < 0.55 %C
P High Carbon Steels >0.55 % C
110- 180 0.02 0.03 0.03 0.05 0.06 0.07 0.08 0.09 0.10 0.12 0.15 P High Carbon Steels > 0.55 % C
60 - 90 0.03 0.04 0.05 0.06 0.08 0.09 0.10 0.12 0.13 0.14 0.14 0.16 0.17 0.18
Alloy Steels , Treated Steelss -
90 160 0.02 0.02 0.03 0.03 0.04 0.05 0.05 0.06 0.07 0.08 0.10
Alloy Steels, Treated Steelss
50 - 80 0.03 0.04 0.04 0.05 0.05 0.06 0.07 0.07 0.08 0.09 0.10 0.12 0.13 0.14
Stainless Steels - Free cutting -
60 160 0.02 0.03 0.03 0.04 0.05 0.06 0.06 0.07 0.08 0.09 0.11 -
Stainless Steels Free cutting 70- 100 0.02 0.03 0.03 0.04 0.05 0.06 0.06 0.07 0.08 0.09 0.10 0.11 0.12 0.13
M Stainless Steels - Austenitic 60 -120 0.02 0.02 0.03 0.03 0.04 0.05 0.05 0.06 0.07 0.08 0.10 M Stainless Steels - Austenitic 60 - 90 0.02 0.03 0.03 0.04 0.05 0.06 0.06 0.07 0.08 0.09 0.10 0.11 0.12 0.13
Cast Steels -
130 170 0.02 0.02 0.03 0.03 0.04 0.05 0.05 0.06 0.07 0.08 0.10 Cast Steels 70 - 90 0.03 0.04 0.04 0.05 0.05 0.06 0.07 0.07 0.08 0.09 0.10 0.12 0.13 0.14
Cast Iron 70 - 150 0.03 0.04 0.04 0.06 0.07 0.08 0.09 0.11 0.12 0.15 0.18 Cast Iron 40 - 80 0.04 0.05 0.05 0.07 0.09 0.11 0.13 0.14 0.15 0.16 0.16 0.17 0.18 0.18
Aluminum«12% Si, Copper -
150 350 0.03 0.04 0.04 0.06 0.07 0.08 0.09 0.11 0.12 0.15 0.18 Aluminum« 12% Si , Copper 100 - 200 0.04 0.05 0.05 0.07 0.09 0.11 0.13 0.14 0.15 0.16 0.16 0.17 0.18 0.16
N Aluminum >12 % Si 100 -250 0.02 0.02 0.03 0.03 0.04 0.05 0.05 0.06 0.07 0.08 0.10 N Aluminum> 12% Si 60- 140 0.03 0.03 0.03 0.04 0.05 0.06 0.06 0.07 0.08 0.09 0.10 0.11 0.13 0.10
Synthetics , Duroplastics 100 - 400 0.05 0.06 0.07 0.08 0.10 0.11 0.12 0.13 0.15 0.18 0.22 Synthetics , Duroplastics -
50 200 0.09 0.10 0.11 0.12 0.14 0.16 0.18 0.19 0.19 0.19 0.19 0.19 0.20 0.20
Thermoplastics and Nickel Alloys . Thermoplastics and Nickel
S Titanium Alloys
20 -80 0.02 0.02 0.02 0.03 0.03 0.03 0.03 0.04 0.04 0.04 0.05 S Alloys , Titanium Alloys
20 - 40 0.03 0.03 0.03 0.04 0.04 0.05 0.06 0.06 0.06 0.07 0.07 0.07 0.08 0.08
097 098
Thread arc entrance thread milling arc exit
Thread
Thread Milling Thread
Milling
Start Point Milling start Milling end point start point center location end point
start
( 1 . entry ) position ( 2 . entry )
( 1 . entry )
( 2 . entry )
fLl f
fLl
fl \ J ans
at
Hil
Eli
1
k
rt
M I&
' in /
M
h
\J
P
'w
RECOMMENDED SELECT FOR SOLID THREADING ENDMILLS
Solid Carbide Threading Endmills Speed and Feed Selection Mini Solid Carbide Threading Endmills Speed and Feed Selection
Sub - Micro Grade with Titanium Aluminum Nitride multi - layer coating ( ISO K 10 - K 10 ) . This is a Sub - Micro Grade with Titanium Aluminum Nitride multi - layer coating ( ISO K 10 - K 10 ) . This is a
TTIM 45 general purpose grade , which can be used with all materials ; It should be run at medium to high TTIM 45 general purpose grade , which can be used with all materials ; It should be run at medium to high
cutting speeds . cutting speeds .
Cutting Feed Rate ( mm ) Feed Rate ( mm )
ISO Materials Speed ISO Materials
( m / min ) cp 2 cp 3 cp4 cp 6 cp8 cp 10 cp12 cp 14 cp16 cp 20 cp25 cp 5 cp 6 cp7 cp8 cp9 cp10 cp12 (p14 cp16
Low and Medium Carbon Low and Medium Carbon
100 - 250 0.03 0.04 0.04 0.06 0.07 0.08 0.09 0.11 0.12 0.15 0.18 60- 120 0.04 0.05 0.05 0.07 0.09 0.11 0.13 0.14 0.15 0.16 0.16 0.17 0.18 0.18
Steels < 0.55 %C Steels < 0.55 %C
P High Carbon Steels >0.55 % C
110- 180 0.02 0.03 0.03 0.05 0.06 0.07 0.08 0.09 0.10 0.12 0.15 P High Carbon Steels > 0.55 % C
60 - 90 0.03 0.04 0.05 0.06 0.08 0.09 0.10 0.12 0.13 0.14 0.14 0.16 0.17 0.18
Alloy Steels , Treated Steelss -
90 160 0.02 0.02 0.03 0.03 0.04 0.05 0.05 0.06 0.07 0.08 0.10
Alloy Steels, Treated Steelss
50 - 80 0.03 0.04 0.04 0.05 0.05 0.06 0.07 0.07 0.08 0.09 0.10 0.12 0.13 0.14
Stainless Steels - Free cutting -
60 160 0.02 0.03 0.03 0.04 0.05 0.06 0.06 0.07 0.08 0.09 0.11 -
Stainless Steels Free cutting 70- 100 0.02 0.03 0.03 0.04 0.05 0.06 0.06 0.07 0.08 0.09 0.10 0.11 0.12 0.13
M Stainless Steels - Austenitic 60 -120 0.02 0.02 0.03 0.03 0.04 0.05 0.05 0.06 0.07 0.08 0.10 M Stainless Steels - Austenitic 60 - 90 0.02 0.03 0.03 0.04 0.05 0.06 0.06 0.07 0.08 0.09 0.10 0.11 0.12 0.13
Cast Steels -
130 170 0.02 0.02 0.03 0.03 0.04 0.05 0.05 0.06 0.07 0.08 0.10 Cast Steels 70 - 90 0.03 0.04 0.04 0.05 0.05 0.06 0.07 0.07 0.08 0.09 0.10 0.12 0.13 0.14
Cast Iron 70 - 150 0.03 0.04 0.04 0.06 0.07 0.08 0.09 0.11 0.12 0.15 0.18 Cast Iron 40 - 80 0.04 0.05 0.05 0.07 0.09 0.11 0.13 0.14 0.15 0.16 0.16 0.17 0.18 0.18
Aluminum«12% Si, Copper -
150 350 0.03 0.04 0.04 0.06 0.07 0.08 0.09 0.11 0.12 0.15 0.18 Aluminum« 12% Si , Copper 100 - 200 0.04 0.05 0.05 0.07 0.09 0.11 0.13 0.14 0.15 0.16 0.16 0.17 0.18 0.16
N Aluminum >12 % Si 100 -250 0.02 0.02 0.03 0.03 0.04 0.05 0.05 0.06 0.07 0.08 0.10 N Aluminum> 12% Si 60- 140 0.03 0.03 0.03 0.04 0.05 0.06 0.06 0.07 0.08 0.09 0.10 0.11 0.13 0.10
Synthetics , Duroplastics 100 - 400 0.05 0.06 0.07 0.08 0.10 0.11 0.12 0.13 0.15 0.18 0.22 Synthetics , Duroplastics -
50 200 0.09 0.10 0.11 0.12 0.14 0.16 0.18 0.19 0.19 0.19 0.19 0.19 0.20 0.20
Thermoplastics and Nickel Alloys . Thermoplastics and Nickel
S Titanium Alloys
20 -80 0.02 0.02 0.02 0.03 0.03 0.03 0.03 0.04 0.04 0.04 0.05 S Alloys , Titanium Alloys
20 - 40 0.03 0.03 0.03 0.04 0.04 0.05 0.06 0.06 0.06 0.07 0.07 0.07 0.08 0.08
097 098
Thread arc entrance thread milling arc exit
Thread
Thread Milling Thread
Milling
Start Point Milling start Milling end point start point center location end point
start
( 1 . entry ) position ( 2 . entry )
( 1 . entry )
( 2 . entry )
fLl f
fLl
fl \ J ans
at
Hil
Eli
1
k
rt
M I&
' in /
M
h
\J
P
'w