Общий каталог TooTool - страница 119
Навигация
 Каталог TooTool техническая информация 1
 Каталог TooTool монолитные фрезы
 Каталог TooTool техническая информация 2
- 页 1
- 页 2
- 页 3
- 页 4
- 页 5
- 页 6
- 页 7
- 页 8
- 页 9
- 页 10
- 页 11
- 页 12
- 页 13
- 页 14
- 页 15
- 页 16
- 页 17
- 页 18
- 页 19
- 页 20
- 页 21
- 页 22
- 页 23
- 页 24
- 页 25
- 页 26
- 页 27
- 页 28
- 页 29
- 页 30
- 页 31
- 页 32
- 页 33
- 页 34
- 页 35
- 页 36
- 页 37
- 页 38
- 页 39
- 页 40
- 页 41
- 页 42
- 页 43
- 页 44
- 页 45
- 页 46
- 页 47
- 页 48
- 页 49
- 页 50
- 页 51
- 页 52
- 页 53
- 页 54
- 页 55
- 页 56
- 页 57
- 页 58
- 页 59
- 页 60
- 页 61
- 页 62
- 页 63
- 页 64
- 页 65
- 页 66
- 页 67
- 页 68
- 页 69
- 页 70
- 页 71
- 页 72
- 页 73
- 页 74
- 页 75
- 页 76
- 页 77
- 页 78
- 页 79
- 页 80
- 页 81
- 82: 新增页码2
- 页 83
- 页 84
- 页 85
- 页 86
- 页 87
- 页 88
- 页 89
- 页 90
- 页 91
- 页 92
- 页 93
- 页 94
- 页 95
- 页 96
- 页 97
- 页 98
- 页 99
- 页 100
- 页 101
- 页 102
- 页 103
- 页 104
- 页 105
- 页 106
- 页 107
- 页 108
- 页 109
- 页 110
- 页 111
- 页 112
- 页 113
- 页 114
- 页 115
- 页 116
- 页 117
- 页 118
- 页 119
- 页 120
- 页 121
- 页 122
- 页 123
- 页 124
- 页 125
- 页 126
- 页 127
- 页 128
- 页 129
- 页 130
- 页 131
- 页 132
- 页 133
- 页 134
- 页 135
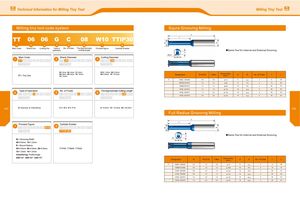
Technical Information for Milling Tiny Tool Milling Tiny Tool
Milling tiny tool code system Squre Grooving Milling
L
| Main code | Shank Dia | Cutting Dia | Type of | No. of flutes | The Approximate | Process figure | Carbide Grades | • | |
| operation | cutting length | Same Tool for Internal and External Grooving |
Main Code Shank Diameter Cutting Diameter
| 03: 3mm | 04: 4mm 05: 5mm | 015: 1 5mm | 05: 5.0mm | ||
| , | Groove Dia. |
06: 6mm 08: 8mm 10: 10mm 06: 6.0mm 10: 10.0mm Designation W ±0.02 T Max d D No of Flutes I L
| TT = Tiny Tool | . | (min.) | . | |
| 12: 12mm |
| TT | 0606G C08 W 08 | 0.8 | 0.8 | cp > 6 | 6 | 6 . 0 | 3 | 8 | 58 |
| 08078G D10 W10 | 1.0 | 1.2 | q> > 8 | 8 | 7.8 | 4 | 10 | 64 | |
| 10098G D20 W12 | 1.2 | 1.4 | cp > 10 | 10 | 9.8 | 4 | 20 | 73 | |
| 1616G E30 W14 | 1.4 | 1.8 | cp > 16 | 16 | 16.0 | 5 | 30 | 101 |
Type of Operation No. of Flutes The Approximate Cutting Lengthm
| 1616G E40 W17 | 1.7 | 2.0 | cp > 16 | 16 | 16.0 | 5 | 40 | 101 |
| 1616G E45 W19 | 2.0 | 2.2 | cp > 16 | 16 | 16.0 | 5 | 45 | 101 |
233 G: Grooving C: Chamfering
Process Figure
W = Grooving Width
08=0.8mm 10= 1.0mm
R = Round Radius
05=0.5mm 06= 0.6mm 09=0.9mm
10=1.0mm 15=1.5mm
Chamfering: Profile Angle
A90=90° A60=60° A45=45°
C=3 D=4 E=5 F=6
Carbide Grades
iiiacm
TTIP30 TTIM45 TTIS30
8 = 8.0mm 10 = 10.0mm 40 = 40.0mm
234
Full Radius Grooving Milling
L
Same Tool for Internal and External Grooving
| Designation TT 0606G C08R05 | R 0.5 | W ±0.02 1.0 | TMax. 0.8 | GrooveDia. (min.) cp>6 | d 6 | D 6.0 | No.ofFlutes 3 | I 8 | L 58 |
| 10088GD16R05 | 0.5 | 1.0 | 1.0 | cp >8.8 | 10 | 8.8 | 4 | 16 | 73 |
| 1010G D20 R06 | 0.6 | 1.2 | 1.0 | cp >10 | 10 | 10.0 | 4 | 20 | 73 |
| 1212G D30 R09 | 0.9 | 1.8 | 1.4 | cp >12 | 12 | 12.0 | 4 | 30 | 84 |
| 1616G E40R10 | 1.0 | 2.0 | 1.6 | cp>16 | 16 | 16.0 | 5 | 40 | 101 |
| 1616G E40R15 | 1.5 | 3.0 | 2.2 | cp>16 | 16 | 16.0 | 5 | 40 | 101 |