Общий каталог TooTool - страница 123
Навигация
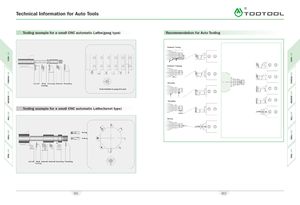 Каталог TooTool техническая информация 1
 Каталог TooTool монолитные фрезы
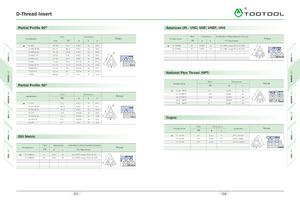 Каталог TooTool техническая информация 2
- 页 1
- 页 2
- 页 3
- 页 4
- 页 5
- 页 6
- 页 7
- 页 8
- 页 9
- 页 10
- 页 11
- 页 12
- 页 13
- 页 14
- 页 15
- 页 16
- 页 17
- 页 18
- 页 19
- 页 20
- 页 21
- 页 22
- 页 23
- 页 24
- 页 25
- 页 26
- 页 27
- 页 28
- 页 29
- 页 30
- 页 31
- 页 32
- 页 33
- 页 34
- 页 35
- 页 36
- 页 37
- 页 38
- 页 39
- 页 40
- 页 41
- 页 42
- 页 43
- 页 44
- 页 45
- 页 46
- 页 47
- 页 48
- 页 49
- 页 50
- 页 51
- 页 52
- 页 53
- 页 54
- 页 55
- 页 56
- 页 57
- 页 58
- 页 59
- 页 60
- 页 61
- 页 62
- 页 63
- 页 64
- 页 65
- 页 66
- 页 67
- 页 68
- 页 69
- 页 70
- 页 71
- 页 72
- 页 73
- 页 74
- 页 75
- 页 76
- 页 77
- 页 78
- 页 79
- 页 80
- 页 81
- 82: 新增页码2
- 页 83
- 页 84
- 页 85
- 页 86
- 页 87
- 页 88
- 页 89
- 页 90
- 页 91
- 页 92
- 页 93
- 页 94
- 页 95
- 页 96
- 页 97
- 页 98
- 页 99
- 页 100
- 页 101
- 页 102
- 页 103
- 页 104
- 页 105
- 页 106
- 页 107
- 页 108
- 页 109
- 页 110
- 页 111
- 页 112
- 页 113
- 页 114
- 页 115
- 页 116
- 页 117
- 页 118
- 页 119
- 页 120
- 页 121
- 页 122
- 页 123
- 页 124
- 页 125
- 页 126
- 页 127
- 页 128
- 页 129
- 页 130
- 页 131
- 页 132
- 页 133
- 页 134
- 页 135
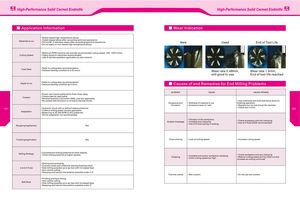
High-Performance Solid Cermet Endmills High-Performance Solid Cermet Endmills
Application Information HI Wear Indication
• Nickel - based high - temperature alloys .
• Cobalt - based alloys after consulting technical assistance .
Materials to cut
• P 6 and M 1 - 3 stainless steels after consulting technical assistance. New Used End of Tool Life
• Do not apply on iron - based high - temperature alloys .
Cutting Speed
• Maximum RPM machine can provide recommended cutting speed : 250-1000 m / min .
• Highly dynamic machines recommended .
\ /
• Use of spindle speeders applicable ( no wet coolant ) .
• Referto cutting data recommendation .
/ \
Feed Rate
• General starting condition fz 0 , 03 mm / z. Wear rate 0.48 mm Wear rate 1 4 mm ,,
still good to use End of tool life reached
• Referto cutting data recommendation .
Depth of cut
• General starting condition ap 0 , 5 mm . Causes of and Remedies for End Milling Problems
problem cause cause remedy
•Power cool nozzle preferred to flush chips away.
• Pressurised air applicable .
Coolant
• Minimal Quantity Lubrication ( MQL ) and dry applicable .
• No coolant with emulsion or oil due to thermal shock . • Use undersize end mills that leave stock for
Excessive burr • Softness of material to cut . finishing operation .
formation • Excessive wear on radii . • Replace tool as end of tool life reached .
•Hydraulic chuck with or without sleeve preferred . • Check tool runout .
241 242
• Collet or milling power chucks applicable .
Adaptation
• Balancing at 25 , 000 RPM ( 2 , 5 G ) preferred .
• Shrink adaptation not recommended.
• Vibration of the workpiece .
Sudden breakage • Unstable tool clamping .
• Check workpiece and tool clamping.
• Use of 4 - flute EADE recommended .
• Use of 6 - flute tooling in slotting .
Roughing Appliaction Yes
Finishing Application Yes Chips sticking • Lack of cutting speed . • Increase cutting speed .
• Conventional milling preferred at lower speeds .
Milling Strategy • Check workpiece and tool clamping .
• Climb milling preferred at higher speeds . • Unstable tool and / or workpiece clamping .
Chipping • Reduce cutting speed during initial cut and
• Initial cutting speed too high . increase as cutting continues .
• Slotting and pocketing .
• Common sizes and undersize leaving finishing stock .
2 and 4 - Flute • Side milling possible up to ap max with increased feed .
• Non - centre cutting .
• Ramping and helical interpolation possible under 2.5 ° .
Thermal cracks • Wet coolant . • Do not use wet coolant .
• Profiling and face milling .
• Non - centre cutting .
Ball Nose
• Side milling possible up to a p max with increased feed .
• Ramping and helical interpolation possible under 2 ° .
Application Information HI Wear Indication
• Nickel - based high - temperature alloys .
• Cobalt - based alloys after consulting technical assistance .
Materials to cut
• P 6 and M 1 - 3 stainless steels after consulting technical assistance. New Used End of Tool Life
• Do not apply on iron - based high - temperature alloys .
Cutting Speed
• Maximum RPM machine can provide recommended cutting speed : 250-1000 m / min .
• Highly dynamic machines recommended .
\ /
• Use of spindle speeders applicable ( no wet coolant ) .
• Referto cutting data recommendation .
/ \
Feed Rate
• General starting condition fz 0 , 03 mm / z. Wear rate 0.48 mm Wear rate 1 4 mm ,,
still good to use End of tool life reached
• Referto cutting data recommendation .
Depth of cut
• General starting condition ap 0 , 5 mm . Causes of and Remedies for End Milling Problems
problem cause cause remedy
•Power cool nozzle preferred to flush chips away.
• Pressurised air applicable .
Coolant
• Minimal Quantity Lubrication ( MQL ) and dry applicable .
• No coolant with emulsion or oil due to thermal shock . • Use undersize end mills that leave stock for
Excessive burr • Softness of material to cut . finishing operation .
formation • Excessive wear on radii . • Replace tool as end of tool life reached .
•Hydraulic chuck with or without sleeve preferred . • Check tool runout .
241 242
• Collet or milling power chucks applicable .
Adaptation
• Balancing at 25 , 000 RPM ( 2 , 5 G ) preferred .
• Shrink adaptation not recommended.
• Vibration of the workpiece .
Sudden breakage • Unstable tool clamping .
• Check workpiece and tool clamping.
• Use of 4 - flute EADE recommended .
• Use of 6 - flute tooling in slotting .
Roughing Appliaction Yes
Finishing Application Yes Chips sticking • Lack of cutting speed . • Increase cutting speed .
• Conventional milling preferred at lower speeds .
Milling Strategy • Check workpiece and tool clamping .
• Climb milling preferred at higher speeds . • Unstable tool and / or workpiece clamping .
Chipping • Reduce cutting speed during initial cut and
• Initial cutting speed too high . increase as cutting continues .
• Slotting and pocketing .
• Common sizes and undersize leaving finishing stock .
2 and 4 - Flute • Side milling possible up to ap max with increased feed .
• Non - centre cutting .
• Ramping and helical interpolation possible under 2.5 ° .
Thermal cracks • Wet coolant . • Do not use wet coolant .
• Profiling and face milling .
• Non - centre cutting .
Ball Nose
• Side milling possible up to a p max with increased feed .
• Ramping and helical interpolation possible under 2 ° .