Общий каталог TooTool - страница 48
Навигация
 Каталог TooTool техническая информация 1
 Каталог TooTool монолитные фрезы
 Каталог TooTool техническая информация 2
- 页 1
- 页 2
- 页 3
- 页 4
- 页 5
- 页 6
- 页 7
- 页 8
- 页 9
- 页 10
- 页 11
- 页 12
- 页 13
- 页 14
- 页 15
- 页 16
- 页 17
- 页 18
- 页 19
- 页 20
- 页 21
- 页 22
- 页 23
- 页 24
- 页 25
- 页 26
- 页 27
- 页 28
- 页 29
- 页 30
- 页 31
- 页 32
- 页 33
- 页 34
- 页 35
- 页 36
- 页 37
- 页 38
- 页 39
- 页 40
- 页 41
- 页 42
- 页 43
- 页 44
- 页 45
- 页 46
- 页 47
- 页 48
- 页 49
- 页 50
- 页 51
- 页 52
- 页 53
- 页 54
- 页 55
- 页 56
- 页 57
- 页 58
- 页 59
- 页 60
- 页 61
- 页 62
- 页 63
- 页 64
- 页 65
- 页 66
- 页 67
- 页 68
- 页 69
- 页 70
- 页 71
- 页 72
- 页 73
- 页 74
- 页 75
- 页 76
- 页 77
- 页 78
- 页 79
- 页 80
- 页 81
- 82: 新增页码2
- 页 83
- 页 84
- 页 85
- 页 86
- 页 87
- 页 88
- 页 89
- 页 90
- 页 91
- 页 92
- 页 93
- 页 94
- 页 95
- 页 96
- 页 97
- 页 98
- 页 99
- 页 100
- 页 101
- 页 102
- 页 103
- 页 104
- 页 105
- 页 106
- 页 107
- 页 108
- 页 109
- 页 110
- 页 111
- 页 112
- 页 113
- 页 114
- 页 115
- 页 116
- 页 117
- 页 118
- 页 119
- 页 120
- 页 121
- 页 122
- 页 123
- 页 124
- 页 125
- 页 126
- 页 127
- 页 128
- 页 129
- 页 130
- 页 131
- 页 132
- 页 133
- 页 134
- 页 135
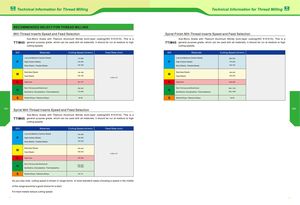
Technical Information for Thread Milling Technical Information for Thread Milling
RECOMMENDED SELECT FORTHREAD MILLING
Mill - Thread Inserts Speed and Feed Selection Spiral Finish Mill - Thread Inserts Speed and Feed Selection
Sub - Micro Grade with Titanium Aluminum Nitride multi - layer coating ( ISO K 10 - K 10 ) . This is a Sub - Micro Grade with Titanium Aluminum Nitride multi - layer coating ( ISO K 10 - K 10 ) . This is a
TTIM 45 general purpose grade , which can be used with all materials ; It should be run at medium to high TTIM 45 general purpose grade , which can be used with all materials ; It should be run at medium to high
cutting speeds . cutting speeds .
ISO Materials Cutting Speed ( m / min ) Feed Rate ( mm ) ISO Materials Cutting Speed ( m / min )
Low and Medium Carbon Steels 115 - 280 Low and Medium Carbon Steels 200 - 330
P High Carbon Steels 130 -200 P High Carbon Steels 170 - 235
Alloy Steels , Treated Steels 105 - 180 Alloy Steels , Treated Steels 100 - 195
Stainless Steels 130 -190 Stainless Steels 180 - 230
M 150 -190
M 180 - 230
Cast Steels Cast Steels
0.05 - 0.15
Cast Iron 80 -170 Cast Iron 200 - 350
Non - Ferrous and Aluminum 180 - 340 Non - Ferrous and Aluminum 500 -1100
N Synthetics , Duroplastics , Thermoplastics 115 - 460
N Synthetics , Duroplastics , Thermoplastics 400 -1500
s Nickel Alloys , Titanium Alloys 25 - 90 s Nickel Alloys , Titanium Alloys 30 - 55
091 092
Spiral Mill - Thread Inserts Speed and Feed Selection
Sub - Micro Grade with Titanium Aluminum Nitride multi - layer coating ( ISO K 10 - K 10 ) . This is a
TTIM 45 general purpose grade , which can be used with all materials ; It should be run at medium to high
cutting speeds .
ISO Materials Cutting Speed ( m / min ) Feed Rate ( mm )
Low and Medium Carbon Steels 145 - 360
P High Carbon Steels 165 -255
Alloy Steels , Treated Steels 135 - 230
Stainless Steels 165 - 245
M 190 - 245
Cast Steels
0.05 - 0.15
Cast Iron 100 - 220
Non - Ferrous and Aluminum
230 - 440
N Synthetics , Duroplastics , Thermoplastics
145 - 590
s Nickel Alloys , Titanium Alloys 30 - 115
As you may note , cutting speed is shown in range terms . In most standard cases choosing a speed in the middle
of the range would be a good choice for a start.
For hard metals reduce cutting speed .
RECOMMENDED SELECT FORTHREAD MILLING
Mill - Thread Inserts Speed and Feed Selection Spiral Finish Mill - Thread Inserts Speed and Feed Selection
Sub - Micro Grade with Titanium Aluminum Nitride multi - layer coating ( ISO K 10 - K 10 ) . This is a Sub - Micro Grade with Titanium Aluminum Nitride multi - layer coating ( ISO K 10 - K 10 ) . This is a
TTIM 45 general purpose grade , which can be used with all materials ; It should be run at medium to high TTIM 45 general purpose grade , which can be used with all materials ; It should be run at medium to high
cutting speeds . cutting speeds .
ISO Materials Cutting Speed ( m / min ) Feed Rate ( mm ) ISO Materials Cutting Speed ( m / min )
Low and Medium Carbon Steels 115 - 280 Low and Medium Carbon Steels 200 - 330
P High Carbon Steels 130 -200 P High Carbon Steels 170 - 235
Alloy Steels , Treated Steels 105 - 180 Alloy Steels , Treated Steels 100 - 195
Stainless Steels 130 -190 Stainless Steels 180 - 230
M 150 -190
M 180 - 230
Cast Steels Cast Steels
0.05 - 0.15
Cast Iron 80 -170 Cast Iron 200 - 350
Non - Ferrous and Aluminum 180 - 340 Non - Ferrous and Aluminum 500 -1100
N Synthetics , Duroplastics , Thermoplastics 115 - 460
N Synthetics , Duroplastics , Thermoplastics 400 -1500
s Nickel Alloys , Titanium Alloys 25 - 90 s Nickel Alloys , Titanium Alloys 30 - 55
091 092
Spiral Mill - Thread Inserts Speed and Feed Selection
Sub - Micro Grade with Titanium Aluminum Nitride multi - layer coating ( ISO K 10 - K 10 ) . This is a
TTIM 45 general purpose grade , which can be used with all materials ; It should be run at medium to high
cutting speeds .
ISO Materials Cutting Speed ( m / min ) Feed Rate ( mm )
Low and Medium Carbon Steels 145 - 360
P High Carbon Steels 165 -255
Alloy Steels , Treated Steels 135 - 230
Stainless Steels 165 - 245
M 190 - 245
Cast Steels
0.05 - 0.15
Cast Iron 100 - 220
Non - Ferrous and Aluminum
230 - 440
N Synthetics , Duroplastics , Thermoplastics
145 - 590
s Nickel Alloys , Titanium Alloys 30 - 115
As you may note , cutting speed is shown in range terms . In most standard cases choosing a speed in the middle
of the range would be a good choice for a start.
For hard metals reduce cutting speed .