Каталог Sumitomo пластины с алмазными вставками Sumidia - страница 6
Навигация
 Каталог Sumitomo токарные резцы (державки) для внутреннего точения
 Каталог Sumitomo микроинструмент
 Техническая информация Sumitomo
 Каталог Sumitomo модульные системы для револьверных головок токарных станков
 Каталог Sumitomo твердосплавные заготовки
 Каталог Sumitomo фрезы со сменными пластинами
DA1000
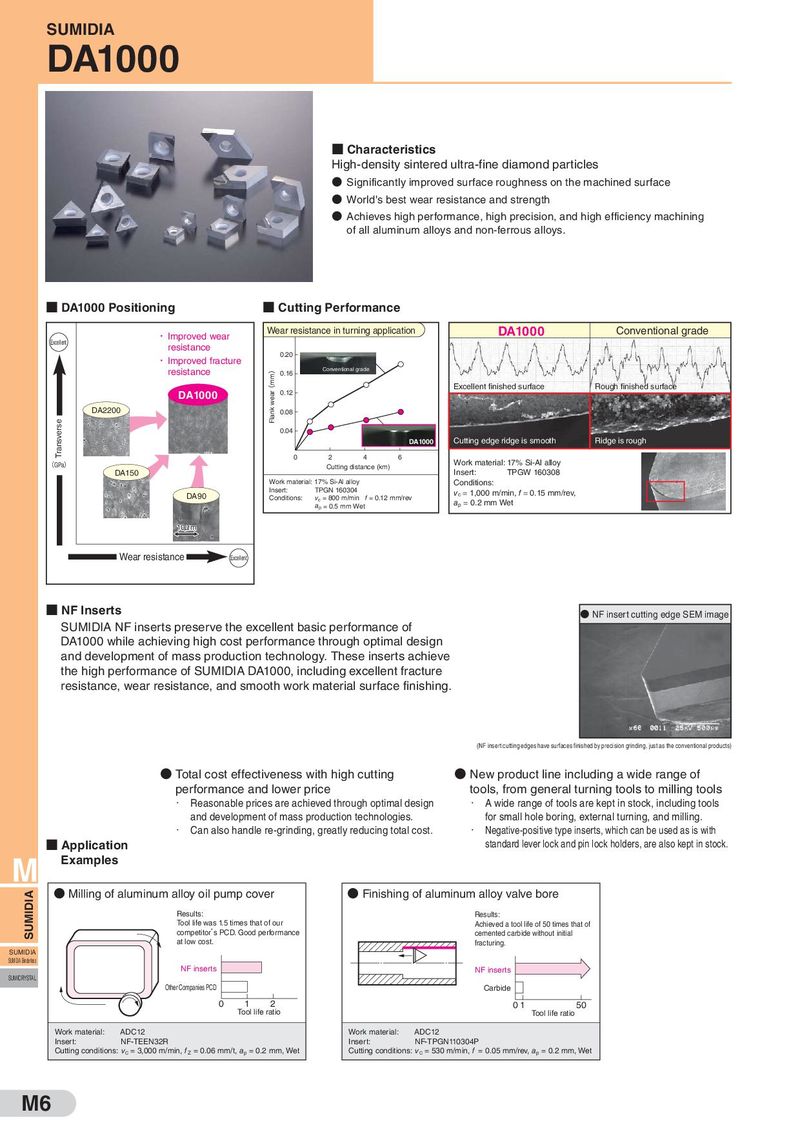
- Characteristics
High-density sintered ultra-fine diamond particles
- Significantly improved surface roughness on the machined surface
- World's best wear resistance and strength
- Achieves high performance, high precision, and high efficiency machining of all aluminum alloys and non-ferrous alloys.
- DA1000 Positioning
- Cutting Performance
Wear resistance in turning application DA1000 Conventional grade
Improved wear Excellent resistance
- 0.20
Improved fracture resistance Conventional grade 0.16 Excellent finished surface Rough finished surface DA1000 0.12 DA2200 0.08
0.04
DA1000 Cutting edge ridge is smooth Ridge is rough
0 2 4 6
| ( | ) | Work material: 17% Si-Al alloy | |||
| GPa | Cutting distance (km) | ||||
| DA150 | Insert: TPGW 160308 | ||||
| Work material: 17% Si-Al alloy | Conditions: |
| Insert: | TPGN 160304 | v = 1,000 m/min, f = 0.15 mm/rev, | |
| DA90 | Conditions: v = 800 m/min f = 0.12 mm/rev | c |
c a = 0.2 mm Wet a = 0.5 mm Wet p p 1010μμmm
Wear resistance Excellent
- NF Inserts
- NF insert cutting edge SEM image
SUMIDIA NF inserts preserve the excellent basic performance of
DA1000 while achieving high cost performance through optimal design
and development of mass production technology. These inserts achieve
the high performance of SUMIDIA DA1000, including excellent fracture
resistance, wear resistance, and smooth work material surface finishing.
(NF insert cutting edges have surfaces finished by precision grinding, just as the conventional products)
- Total cost effectiveness with high cutting
- New product line including a wide range of
performance and lower price tools, from general turning tools to milling tools
- Reasonable prices are achieved through optimal design
- A wide range of tools are kept in stock, including tools
and development of mass production technologies. for small hole boring, external turning, and milling.
- Can also handle re-grinding, greatly reducing total cost.
- Negative-positive type inserts, which can be used as is with
- Application standard lever lock and pin lock holders, are also kept in stock.
M Examples
- Milling of aluminum alloy oil pump cover
- Finishing of aluminum alloy valve bore
| Results: | Results: | |
| Tool life was 1.5 times that of our | Achieved a tool life of 50 times that of | |
| competitor s PCD. Good performance | cemented carbide without initial | |
| at low cost. | fracturing. | |
| SUMIDIA | ||
| SUMIDIA Binderless | ||
| NF inserts | NF inserts | |
| SUMICRYSTAL | ||
| Other Companies PCD | Carbide | |
| 50 0 1 2 1 0 | ||
| Tool life ratio Tool life ratio | ||
| Work material: ADC12 | Work material: ADC12 |
Insert: NF-TEEN32R Insert: NF-TPGN110304P
Cutting conditions: v = 3,000 m/min, f Z = 0.06 mm/t, ap = 0.2 mm, Wet Cutting conditions: v = 530 m/min, f = 0.05 mm/rev, a p = 0.2 mm, Wet C C