Каталог Sumitomo пластины с алмазными вставками Sumidia - страница 31
Навигация
 Каталог Sumitomo токарные резцы (державки) для внутреннего точения
 Каталог Sumitomo микроинструмент
 Техническая информация Sumitomo
 Каталог Sumitomo модульные системы для револьверных головок токарных станков
 Каталог Sumitomo твердосплавные заготовки
 Каталог Sumitomo фрезы со сменными пластинами
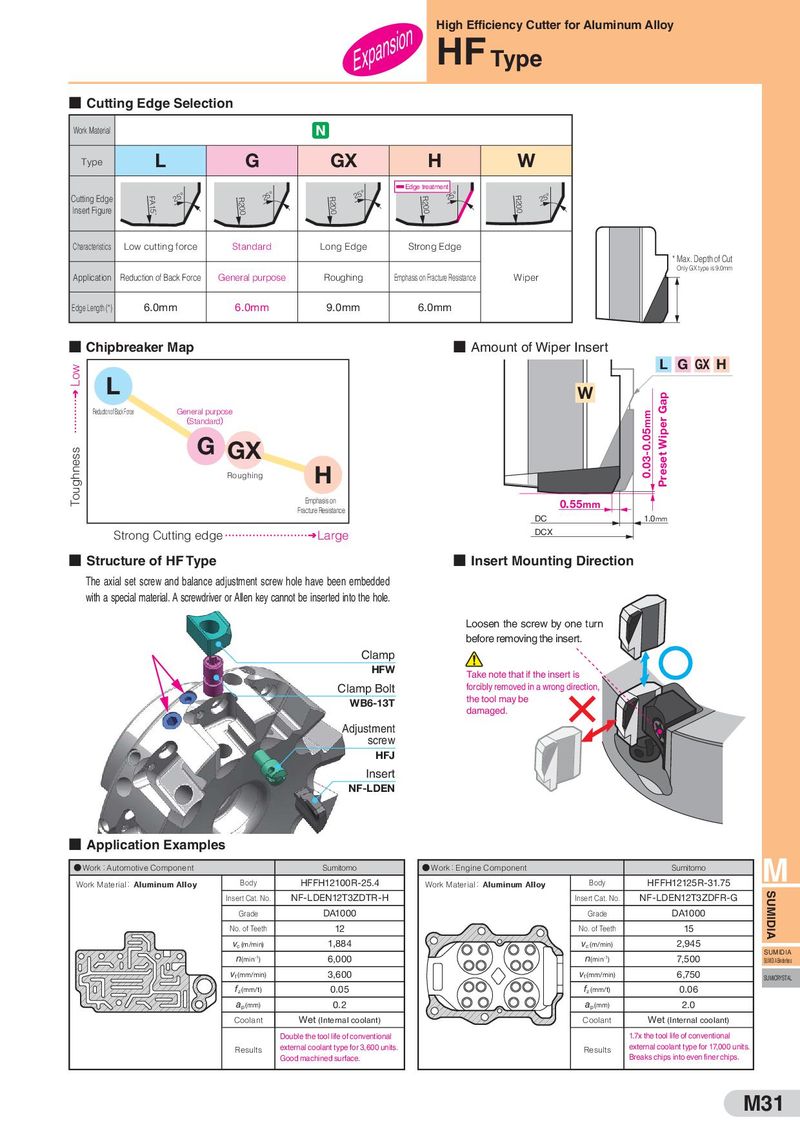
- Cutting Edge Selection Work Material
L G
Type
FA15’ R200
Cutting Edge 25° 25°
Insert Figure
HF
Expansion Type
| GX | H | W | |
| Edge treatment | |||
| R200 | R200 | R200 |
25° 25° 25°
| Characteristics | Low cutting force | Standard | Long Edge | Strong Edge | |||||
| * Max. Depth of Cut | |||||||||
| Only GX type is 9.0mm | |||||||||
| Application | Reduction of Back Force | General purpose | Roughing | Emphasis on Fracture Resistance | Wiper | ||||
| Edge Length (*) | 6.0mm | 6.0mm | 9.0mm | 6.0mm |
- Chipbreaker Map
- Amount of Wiper Insert
LGGXH
L
W
Reduction of Back Force General purpose (Standard)
G GX
H
Roughing Emphasis on 0.55mm Fracture Resistance DC 1.0mm
Strong Cutting edge Large DCX
- Structure of HF Type
- Insert Mounting Direction
The axial set screw and balance adjustment screw hole have been embedded
with a special material. A screwdriver or Allen key cannot be inserted into the hole.
Loosen the screw by one turn
before removing the insert.
Clamp
HFW Take note that if the insert is Clamp Bolt forcibly removed in a wrong direction, the tool may be WB6-13T damaged.
Adjustment
screw
HFJ
Insert
NF-LDEN
- Application Examples
M
●Work:Automotive Component Sumitomo ●Work:Engine Component Sumitomo
| Work Material:Aluminum Alloy Body | HFFH12100R-25.4 | Work Material:Aluminum Alloy Body | HFFH12125R-31.75 |
| Insert Cat. No. | NF-LDEN12T3ZDTR-H | Insert Cat. No. | NF-LDEN12T3ZDFR-G |
| Grade | DA1000 | Grade | DA1000 |
| No. of Teeth | 12 | No. of Teeth | 15 |
| v (m/min) | 1,884 | v (m/min) | 2,945 |
| c | c | ||
| SUMIDIA | |||
| n(min-1) | 6,000 | n(min -1) | SUMIDIA Binderless 7,500 |
| v (mm/min) | 3,600 | v (mm/min) | 6,750 |
| f | f | SUMICRYSTAL | |
| f (mm/t) | 0.05 | f (mm/t) | 0.06 |
| z | z | ||
| a (mm) | 0.2 | a (mm) | 2.0 |
| p | p | ||
| Coolant | Wet (Internal coolant) | Coolant | Wet (Internal coolant) |
| Double the tool life of conventional | 1.7x the tool life of conventional | ||
| Results | external coolant type for 3,600 units. | Results | external coolant type for 17,000 units. |
Good machined surface. Breaks chips into even finer chips.