Каталог Sumitomo пластины с алмазными вставками Sumidia - страница 41
Навигация
 Каталог Sumitomo токарные резцы (державки) для внутреннего точения
 Каталог Sumitomo микроинструмент
 Техническая информация Sumitomo
 Каталог Sumitomo модульные системы для револьверных головок токарных станков
 Каталог Sumitomo твердосплавные заготовки
 Каталог Sumitomo фрезы со сменными пластинами
| Radial direction | 0°〜2° | 5.7 | P M K N N S H | |||||
| Axial direction | +10° | Steel | Stainless steel | Cast iron | Non-ferrous Aluminum Exotic alloy Hardened steel | |||
| H | H | H | S | S | H |
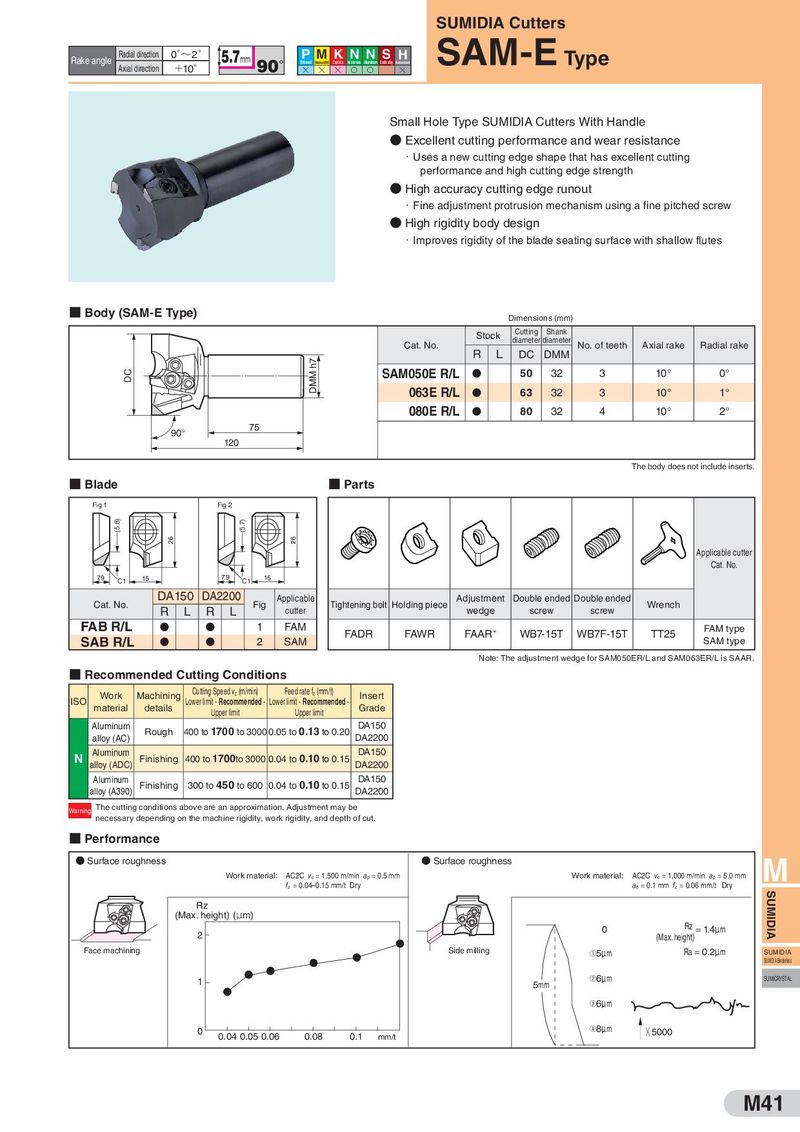
SUMIDIA Cutters
SAM-E
Type
Small Hole Type SUMIDIA Cutters With Handle
- Excellent cutting performance and wear resistance
- Uses a new cutting edge shape that has excellent cutting performance and high cutting edge strength
- High accuracy cutting edge runout
- Fine adjustment protrusion mechanism using a fine pitched screw
- High rigidity body design
- Improves rigidity of the blade seating surface with shallow flutes
- Body (SAM-E Type)
75 90° 120
- Blade Fig 1 Fig 2
Dimensions (mm)
| Stock | Cutting | Shank |
| diameter diameter |
| Cat. No. | R | L | No. of teeth | Axial rake | Radial rake | |
| DC DMM |
| SAM050E R/L | D | 50 | 32 | 3 | 10° | 0° | |
| 063E R/L | D | 63 | 32 | 3 | 10° | 1° | |
| 080E R/L | D | 80 | 32 | 4 | 10° | 2° |
The body does not include inserts.
- Parts
Applicable cutter Cat. No.
| 7.9 | 15 | 7.9 | 15 | ||
| C1 | C1 |
DA150 DA2200 Applicable Adjustment Double ended Double ended
Cat. No. Fig Tightening bolt Holding piece Wrench
| R | L | R | L | cutter | wedge | screw | screw | ||||||||
| FAB R/L | D | D | 1 | FAM | |||||||||||
| * | FAM type | ||||||||||||||
| D | D | FADR | FAWR | FAAR | WB7-15T | WB7F-15T | TT25 | ||||||||
| SAB R/L | 2 | SAM | SAM type |
Note: The adjustment wedge for SAM050ER/L and SAM063ER/L is SAAR.
- Recommended Cutting Conditions
Cutting Speed v (m/min) Feed rate f (mm/t)
| Work | Machining | c | z | Insert | ||
| ISO | Lower limit - Recommended - Lower limit - Recommended - | |||||
| material | details | Grade |
Upper limit Upper limit Aluminum DA150 Rough 400 to 1700 to 3000 0.05 to 0.13 to 0.20 alloy (AC) DA2200
Aluminum DA150
N Finishing 400 to 1700to 3000 0.04 to 0.10 to 0.15
alloy (ADC) DA2200 Aluminum DA150 Finishing 300 to 450 to 600 0.04 to 0.10 to 0.15 alloy (A390) DA2200 The cutting conditions above are an approximation. Adjustment may be Warning necessary depending on the machine rigidity, work rigidity, and depth of cut.
- Performance
- Surface roughness
- Surface roughness M
Work material: AC2C v = 1,500 m/min a = 0.5 mm Work material: AC2C v = 1,000 m/min a = 5.0 mm
c p c p
fz = 0.04–0.15 mm/t Dry ae = 0.1 mm fz = 0.06 mm/t Dry Rz (Max. height) (µm) 0 Rz = 1.4µm
2 (Max. height) D
Face machining Side milling ① µ Ra = 0.2µm
D 5 m SUMIDIA
D SUMIDIA Binderless D D ②6µm 1 SUMICRYSTAL
5mm D ③6µm ④8µm
0.04 0.05 0.06 0.08 0.1 mm/t