Каталог Sumitomo пластины с алмазными вставками Sumidia - страница 36
Навигация
 Каталог Sumitomo токарные резцы (державки) для внутреннего точения
 Каталог Sumitomo микроинструмент
 Техническая информация Sumitomo
 Каталог Sumitomo модульные системы для револьверных головок токарных станков
 Каталог Sumitomo твердосплавные заготовки
 Каталог Sumitomo фрезы со сменными пластинами
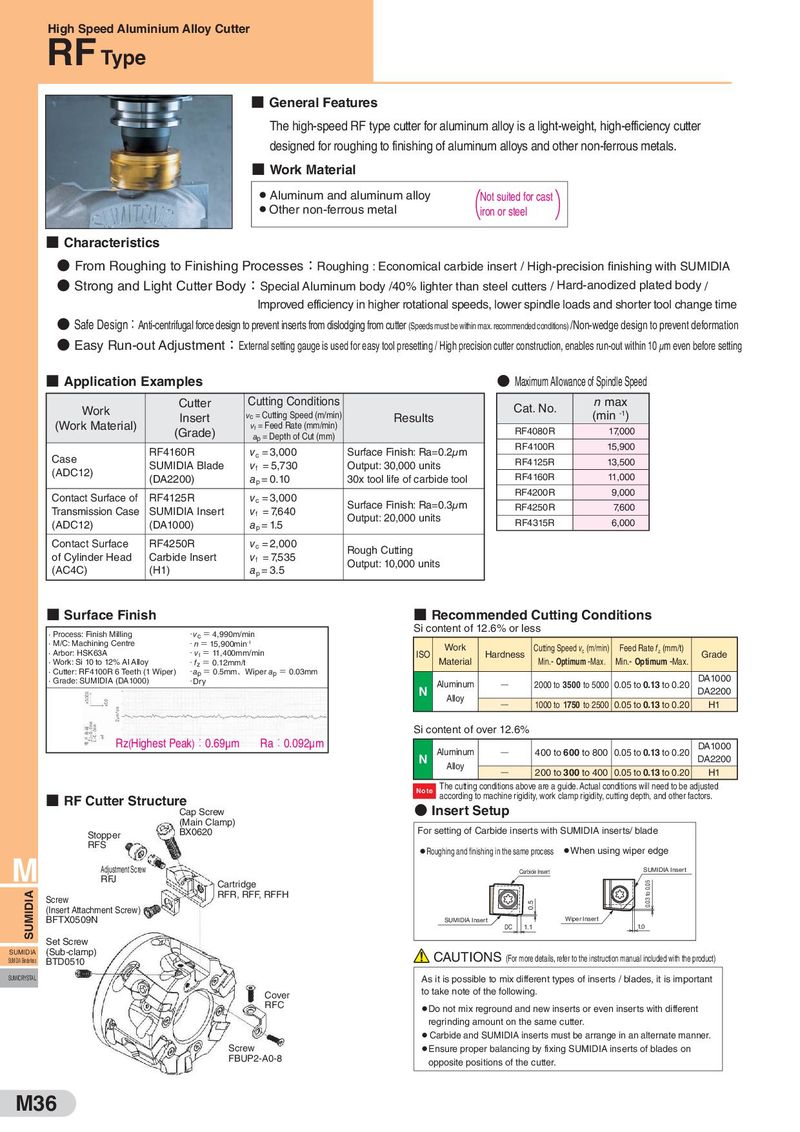
RFHigh Speed Aluminium Alloy Cutter
- General Features The high-speed RF type cutter for aluminum alloy is a light-weight, high-efficiency cutter designed for roughing to finishing of aluminum alloys and other non-ferrous metals.
- Work Material
- Aluminum and aluminum alloy Not suited for cast
- Other non-ferrous metal iron or steel
- Characteristics
- From Roughing to Finishing Processes:
Roughing : Economical carbide insert / High-precision finishing with SUMIDIA
- Strong and Light Cutter Body:
Special Aluminum body /40% lighter than steel cutters / Hard-anodized plated body /
Improved efficiency in higher rotational speeds, lower spindle loads and shorter tool change time
- Safe Design:
Anti-centrifugal force design to prevent inserts from dislodging from cutter (Speeds must be within max. recommended conditions) /Non-wedge design to prevent deformation
- Easy Run-out Adjustment:
External setting gauge is used for easy tool presetting / High precision cutter construction, enables run-out within 10 μm even before setting
- Application Examples Maximum Allowance of Spindle Speed
| Cutter | Cutting Conditions | n max | ||
| Work | Cat. No. | |||
| Insert | v = Cutting Speed (m/min) | Results | (min -1) | |
| c | ||||
| (Work Material) | v = Feed Rate (mm/min) | |||
| (Grade) | f | RF4080R | 17,000 | |
| ap = Depth of Cut (mm) | ||||
| RF4100R | 15,900 |
| RF4160R | v = 3,000 | Surface Finish: Ra=0.2μm | |||
| Case | c | ||||
| SUMIDIA Blade | v = 5,730 | Output: 30,000 units | RF4125R | 13,500 | |
| (ADC12) | f | ||||
| (DA2200) | a = 0.10 | 30x tool life of carbide tool | RF4160R | 11,000 | |
| p | |||||
| RF4200R | 9,000 | ||||
| Contact Surface of | RF4125R | v = 3,000 | |||
| c | Surface Finish: Ra=0.3μm | ||||
| Transmission Case | SUMIDIA Insert | v = 7,640 | RF4250R | 7,600 | |
| f | Output: 20,000 units | ||||
| (ADC12) | (DA1000) | a = 1.5 | RF4315R | 6,000 | |
| p | |||||
| Contact Surface | RF4250R | v = 2,000 | |||
| c | Rough Cutting | ||||
| of Cylinder Head | Carbide Insert | v = 7,535 | |||
| f | Output: 10,000 units | ||||
| (AC4C) | (H1) | a = 3.5 |
p
- Surface Finish
- Recommended Cutting Conditions Si content of 12.6% or less
Process: Finish Milling ・v = 4,990m/min
c
- M/C: Machining Centre ・n= 15,900min-1
= Work Cutting Speed v (m/min) Feed Rate f (mm/t)
| · Arbor: HSK63A | v 11,400mm/min | Hardness ISO | c | z | Grade | ||
| ・ | f = | - | - | - - | |||
| · Work: Si 10 to 12% Al Alloy | f 0.12mm/t | Min. Material Optimum | Max. | Min. Optimum Max. | |||
| z | |||||||
| · Cutter: RF4100R 6 Teeth (1 Wiper) | ・a | = 0.5mm、Wiper a | = 0.03mm | ||||
| p | p | DA1000 | |||||
| · Grade: SUMIDIA (DA1000) | ・Dry | Q |
Aluminum 2000 to 3500 to 5000 0.05 to 0.13 to 0.20 N DA2200 Alloy Q 1000 to 1750 to 2500 0.05 to 0.13 to 0.20 H1
Si content of over 12.6%
Rz Highest Peak :0.69μm Ra:0.092μm
( ) DA1000
| Aluminum | Q | 400 to 600 to 800 0.05 to 0.13 to 0.20 | ||
| N | DA2200 | |||
| Alloy | Q | |||
| 200 to 300 to 400 0.05 to 0.13 to 0.20 | H1 | |||
| The cutting conditions above are a guide. Actual conditions will need to be adjusted |
| ■ | Note | according to machine rigidity, work clamp rigidity, cutting depth, and other factors. | ||
| RF Cutter Structure | ● | |||
| Cap Screw | Insert Setup | |||
| (Main Clamp) |
| Stopper | BX0620 | For setting of Carbide inserts with SUMIDIA inserts/ blade |
| RFS |
M Roughing and finishing in the same process When using wiper edge
Adjustment Screw SUMIDIA Insert Carbide Insert RFJ Cartridge
RFR, RFF, RFFH Screw (Insert Attachment Screw)
BFTX0509N SUMIDIA Insert Wiper Insert
| DC | 1.1 | 1.0 | |
| Set Screw |
| SUMIDIA | (Sub-clamp) | CAUTIONS | |||
| (For more details, refer to the instruction manual included with the product) | |||||
| SUMIDIA Binderless | BTD0510 | ||||
| SUMICRYSTAL | As it is possible to mix different types of inserts / blades, it is important | ||||
| Cover | to take note of the following. |
RFC
- Do not mix reground and new inserts or even inserts with different regrinding amount on the same cutter.
- Carbide and SUMIDIA inserts must be arrange in an alternate manner.
| Screw | ● Ensure proper balancing by fixing SUMIDIA inserts of blades on |
| FBUP2-A0-8 | opposite positions of the cutter. |