Каталог Sumitomo пластины с алмазными вставками Sumidia - страница 38
Навигация
 Каталог Sumitomo токарные резцы (державки) для внутреннего точения
 Каталог Sumitomo микроинструмент
 Техническая информация Sumitomo
 Каталог Sumitomo модульные системы для револьверных головок токарных станков
 Каталог Sumitomo твердосплавные заготовки
 Каталог Sumitomo фрезы со сменными пластинами
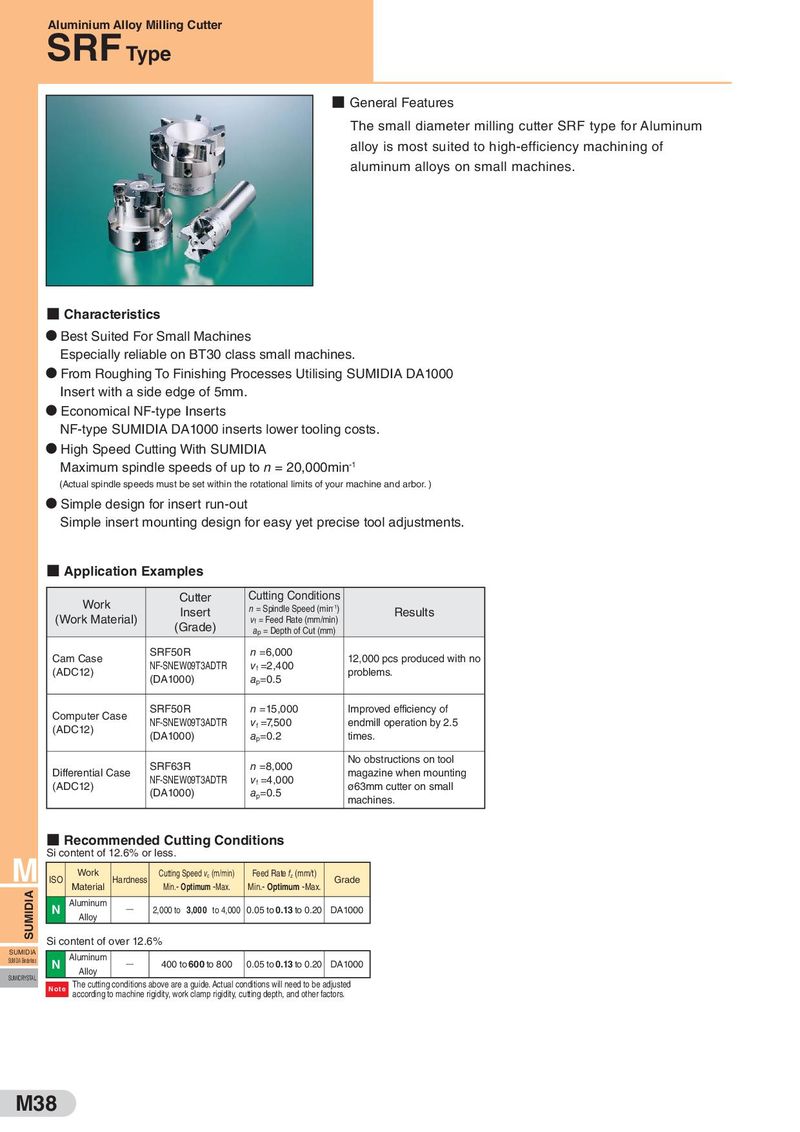
SRFAluminium Alloy Milling Cutter
- General Features The small diameter milling cutter SRF type for Aluminum alloy is most suited to high-efficiency machining of aluminum alloys on small machines.
- Characteristics
D Best Suited For Small Machines
Especially reliable on BT30 class small machines.
D From Roughing To Finishing Processes Utilising SUMIDIA DA1000
Insert with a side edge of 5mm.
D Economical NF-type Inserts
NF-type SUMIDIA DA1000 inserts lower tooling costs.
D High Speed Cutting With SUMIDIA
Maximum spindle speeds of up to n = 20,000min-1
(Actual spindle speeds must be set within the rotational limits of your machine and arbor. )
D Simple design for insert run-out
Simple insert mounting design for easy yet precise tool adjustments.
- Application Examples
| Work (Work Material) | Cutter Insert (Grade) | Cutting Conditions n= Spindle Speed (min-1) vf= Feed Rate (mm/min) ap= Depth of Cut(mm) | Results |
| Cam Case (ADC12) | SRF50R NF-SNEW09T3ADTR (DA1000) | n=6,000 vf=2,400 ap=0.5 | 12,000 pcs produced with no problems. |
| Computer Case (ADC12) | SRF50R NF-SNEW09T3ADTR (DA1000) | n=15,000 vf=7,500 ap=0.2 | Improved efficiency of endmill operation by 2.5 times. |
| Differential Case (ADC12) | SRF63R NF-SNEW09T3ADTR (DA1000) | n=8,000 vf=4,000 ap=0.5 | No obstructions on tool magazine when mounting ø63mm cutter on small machines. |
- Recommended Cutting Conditions
M Si content of 12.6% or less.
Work Cutting Speed v (m/min) Feed Rate f (mm/t)
ISO Hardness c z Grade
| Material | Min.- Optimum -Max. | Min.- Optimum -Max. | |
| Aluminum | Q |
| N | 2,000 to | 3,000 | to 4,000 0.05 to 0.13 to 0.20 DA1000 | ||||
| Alloy | |||||||
| Si content of over 12.6% | |||||||
| SUMIDIA | Aluminum | ||||||
| SUMIDIA Binderless | N | Q | 400 to600 to 800 | 0.05 to 0.13 to 0.20 DA1000 |
Alloy SUMICRYSTAL The cutting conditions above are a guide. Actual conditions will need to be adjusted Note according to machine rigidity, work clamp rigidity, cutting depth, and other factors.