Обший каталог Yamawa 2016 - 2017 - страница 703
Навигация
 Каталоги Yamawa твердосплавные метчики для закаленной стали
 Краткое руководство Yamawa по каталогам
 Общий каталог Yamawa 2021
 Общий каталог Yamawa 2022 - 2023
- CONTENTS
- Basic concept of new product system for various steels
- System chart of taps for blind holes on ISO P - steel ~ 45HRC
- System chart of taps for through holes on ISO P - steel ~ 45HRC
- System chart of taps for blind holes on ISO M - stainless steel
- System chart of taps for through holes on ISO M - stainless steel
- System chart of taps for blind holes on ISO K - cast iron
- System chart of taps for through holes on ISO K - cast iron
- System chart of taps for blind holes on ISO N - non ferrous materials
- System chart of taps for through holes on ISO N - non ferrous materials
- System chart of forming taps for ISO P steel and ISO M stainless steel
- System chart of forming taps for ISO N non ferrous materials
- System chart of taps for blind holes on ISO S-heat resistant alloys
- System chart of taps for through holes on ISO S-heat resistant alloys
- System chart of taps for blind and through holes on ISO H - hardened steel 45 ~ 63HRC
- ISO Code
- List of work materials
- Selection chart of taps
- YAMAWA PRODUCT LINE-UPS
- Spiral Fluted Tap Series for blind hole
- Spiral Fluted Tap Series for through hole
- Spiral Pointed Tap Series
- Straight Fluted Tap Series
- Cemented Carbide Tap Series
- Roll Tap Series
- Dies
- Center Drills
- Spiral Fluted Tap Series for blind hole
- Spiral Fluted Tap Series for through hole
- Spiral Pointed Tap Series
- Hand Tap Series
- Cemented Carbide Tap Series
- Roll Tap Series
- Check Pin Series
- Pipe Tap Series
- Dies
- Spiral Fluted Tap Series for blind hole
- Spiral Fluted Tap Series for through hole
- Spiral Pointed Tap Series
- Hand Tap Series
- Cemented Carbide Tap Series
- Roll Tap Series
- Special Thread Taps / Simple Inspection Tools
- Pipe Tap Series
- Thread Mills
- Dies
- Center Drills/Centering Tools
- Explanation of icons
- DIN LINE UP
- SPIRAL FLUTED TAP SERIES FOR BLIND HOLE
- SP Spiral Fluted Taps
- SP(Coating) Spiral Fluted Taps, Coated
- SP OX Spiral Fluted Taps, Oxided
- SP(LH) Spiral Fluted Taps for Left Hand Threads
- AU+SP Plus Series Spiral Fluted Taps, Coated
- AUXSP X Series Spiral Fluted Taps, Coated
- AL+SP/AL-SP Spiral Fluted Taps for Aluminum
- LO-SP Low Spiral Fluted Taps
- LO-SP OX Low Spiral Fluted Taps, Oxided
- PH-SP Spiral Fluted Taps for Hard-to-Machine Materials
- E-SP Spiral Fluted Taps for Soft Structural Steels
- SP+VA Spiral Fluted Taps for Stainless Steels
- SP-VA Spiral Fluted Taps for Stainless Steels
- SP-VA(Coating) Spiral Fluted Taps for Stainless Steels, Coated
- SP-BLF Spiral Fluted Taps, Deep Hole Use
- SP-BLF(Coating) Spiral Fluted Taps, Deep Hole Use, Coated
- SP-BLF OX Spiral Fluted Taps, Deep Hole Use, Oxided
- SU2-SP Spiral Fluted Taps for Tough Stainless Steels
- ZEN-B Spiral Fluted Taps for Nickel Base Alloys
- ZET-B Spiral Fluted Taps for Titanium Alloys
- F-SP Spiral Fluted Taps for High Speed Tapping
- HFIHS For Ultra Fast Tapping, Vertical Use. Spiral Fluted Taps for Carbon Steels
- HFISP For Ultra Fast Tapping, Horizontal Use. Low Spiral Fluted Taps for Carbon Steels
- HFAHS For Ultra Fast Tapping, Vertical Use, Spiral Fluted Taps for Aluminum
- HFASP For Ultra Fast Tapping, Horizontal Use, Low Spiral Fluted Taps for Aluminum
- HDISP For Dry Tapping, Blind Hole Use, Spiral Fluted Taps for Steels
- HDASP For Dry Tapping, Blind Hole Use, Spiral Fluted Taps for Aluminum
- SPIRAL FLUTED TAP SERIES FOR THROUGH HOLE
- SL+VA Spiral Fluted Taps for Stainless Steels, Through Hole Use(with LH spiral flutes)
- MHSL Spiral Fluted Taps for Carbon Steels of middle hardness, Through Hole Use(with LH spiral flutes)
- AU+SL Spiral Fluted Taps, Coated, Through Hole Use(with LH spiral flutes)
- AUXSL X Series Spiral Fluted Taps, Coated, Through Hole Use(with LH spiral flutes)
- ZET-P Spiral Fluted Taps for Titanium Alloys, Through Hole Use(with LH spiral flutes)
- F-SL Spiral Fluted Taps for High Speed Tapping, Through Hole Use(with LH spiral flutes)
- HDISL Spiral Fluted Taps for Steels, for Dry Tapping and for Ultra High Speed Tapping, Through Hole Use(with LH spiral flutes)
- SPIRAL POINTED TAP SERIES
- PO Spiral Pointed Taps
- PO(Coating) Spiral Pointed Taps, Coated
- PO OX Spiral Pointed Taps, Oxided
- EH-PO Spiral Pointed Taps for Hard-to-Machine Materials
- PO-VA Spiral Pointed Taps for Stainless Steels
- PO-VA(Coating) Spiral Pointed Taps for Stainless Steels, Coated
- ZEN-P Spiral Pointed Taps for Nickel Base Alloys
- Straight Fluted Tap Series
- HT Straight Fluted and Hand Tap
- EH-HT Straight Fluted Taps for Hard-to-Machine Materials
- GG-HT Straight Fluted Taps for Cast Irons
- GG-HT(Coating) Straight Fluted Taps for Cast Irons, Coated
- GG-HT-OH Straight Fluted Taps for Cast Irons with Internal Coolant Hole
- GG-HT-OH (Coating) Straight Fluted Taps for Cast Irons with Internal Coolant Hole, Coated
- LA-HT Straight Fluted Taps for Die Cast Materials
- AXE-HT AXE Straight Fluted Taps
- CEMENTED CARBIDE TAP SERIES
- CT-FC Carbide Taps for Cast Irons
- EH-CT Carbide Taps for Hard Materials
- UH-CT Carbide Taps for Ultra Hard Materials
- ROLL TAP SERIES
- R-D Thread Forming Taps for Soft Structural Steel Sheets
- R-D(Coating) Thread Forming Taps for Soft Structural Steel Sheets, Coated
- R-D(Coating) Thread Forming Taps for Soft Structural Steel Sheets, Coated
- N+RS/N-RS Thread Forming Taps for Non-Ferrous Materials
- N+RZ/N-RZ Thread Forming Taps for Steels
- OL+RZ Thread Forming Taps for Dry Tapping, Coated
- HP+RZ/HP-RZ High Performance Thread Forming Taps, Coated
- MHRZ Roll Taps for Carbon Steels of Middle Hardness
- Dies
- DPO HSS Spiral Pointed Dies
- Center Drills
- CD-A Low Helix Center Drills-Type A 60°
- CD-R Low Helix Center Drills-Type R
- ANSI LINE UP
- SPIRAL FLUTED TAP SERIES FOR BLIND HOLE
- ISP Spiral Fluted Taps for General Purpose
- SP Spiral Fluted Taps
- SP OX Spiral Fluted Taps,Oxided
- SP Spiral Fluted Taps for Alloy Steels
- LO-SP Low Spiral Fluted Taps for Alloy Steels
- AU+SP Plus Series Spiral Fluted Taps,Coated
- ZELX SS SP Spiral Fluted Taps for Stainless Steels
- ZELX SS SP 6" Long Shank Spiral Fluted Taps for Stainless Steels
- ZELX AL SP Spiral Fluted Taps for Aluminum
- ZELX ALS SP Spiral Fluted Taps for Aluminum
- SP STI Spiral Fluted Taps for Helical Coil Wire Screw Thread Inserts
- SP OX STI Spiral Fluted Taps for Helical Coil Wire Screw Thread Inserts, Oxided
- ZELX TI SP Spiral Fluted Taps for Titanium Alloys
- ZELX NI SP Spiral Fluted Taps for Nickel Base Alloys
- ZELX NI SP STI Spiral Fluted Taps for Nickel Base Alloys, for Helical Coil Wire Screw Thread Inserts
- ZELX FR Spiral Fluted Taps for High Speed Tapping
- SPIRAL FLUTED TAP SERIES FOR THROUGH HOLE
- ZELX TI LHSP Spiral Fluted Taps for Titanium Alloys, Through Hole Use(with LH spiral flutes)
- ZELX FR LHSP Spiral Fluted Taps for High Speed Tapping, Through Hole Use( with LH spiral flutes)
- MHSL Spiral Fluted Taps for Carbon Steels of middle hardness, Through Hole Use (with LH spiral flutes)
- SPIRAL POINTED TAP SERIES
- IPO Spiral Pointed Taps for General Purpose
- PO Spiral Pointed Taps
- PO OX Spiral Pointed Taps, Oxided
- ZELX SS PO Spiral Pointed Taps for Stainless Steels
- ZELX SS PO 6" Long Shank Spiral Pointed Taps for Stainless Steels
- ZELX AL PO Spiral Pointed Taps for Aluminum
- PO STI Spiral Pointed Taps for Helical Coil Wire Screw Thread Inserts
- PO OX STI Spiral Pointed Taps for Helical Coil Wire Screw Thread Inserts, Oxided
- ZELX NI PO Spiral Pointed Taps for Nickel Base Alloys
- ZELX NI PO STI Spiral Pointed Taps for Nickel Base Alloys for Helical Coil Wire Screw Thread Inserts
- HAND TAP SERIES
- IHT Hand Taps for General Purpose
- HT Hand Taps
- HT OX Hand Taps, Oxided
- HT-CI Hand Taps for Cast Irons
- AXE-HT AXE Hand Taps
- HT STI Hand Taps for Helical Coil Wire Screw Thread Inserts
- HT OX STI Hand Taps for Helical Coil Wire Screw Thread Inserts, Oxided
- ZELX MOLD Hand Taps for Hard-to-Machine Materials
- EH-HT Hand Taps for Hard-to-Machine Materials
- CEMENTED CARBIDE TAP SERIES
- ZELX CARB AL Carbide Taps for Light Alloys
- ZELX CARB CI Carbide Taps for Cast Irons
- ROLL TAP SERIES
- N-RZ Thread Forming Taps for Steels
- N-RS Thread Forming Taps for Non-Ferrous Materials
- OL-RZ Thread Forming Taps for Dry Tapping, Coated
- HP-RZ High Performance Thread Forming Taps, Coated
- MHRZ Roll Taps for Carbon Steels of Middle Hardness
- CHECK PIN
- CPC-S Check Pins for Bored Hole in thread cut tapping (Straight Type)
- CPC-T Check Pins for Bored Holes in thread cut tapping (Taper Type)
- PIPE TAP SERIES
- ZELX SS NPT Taps for American Taper Pipe Threads
- ZELX SS NPTF Taps for American Dryseal Taper Pipe Threads
- ZELX MOLD NPT Hand Taps for Hard-to-Machine Materials For American Taper Pipe Threads
- NPT Hand Taps for American Taper Pipe Threads
- INT-NPT Interrupted Taps for American Taper Pipe Threads
- NPT-CI Hand Taps for American Taper Pipe Threads for Cast Irons
- NPTF Hand Taps for American Dryseal Taper Pipe Threads
- NPTF-CI Hand Taps for American Dryseal Taper Pipe Threads, for Cast Irons
- NPS Hand Taps for American Parallel Pipe Threads
- NPSF Hand Taps for American Dryseal Parallel Pipe Threads
- Dies
- PO-D HSS Spiral Pointed Dies
- RD-DA Die Attachment (for Solid Dies)
- JIS LINE UP
- SPIRAL FLUTED TAP SERIES FOR BLIND HOLE
- ISP Spiral Fluted Taps for General Purpose
- SP Spiral Fluted Taps
- SP 1.5P Spiral Fluted Taps 1.5P
- +SP Plus Series Spiral Fluted Taps
- XSP X Series Spiral Fluted Taps
- SP OX Spiral Fluted Taps, Oxided
- +SP OX Plus Series Spiral Fluted Taps, Oxided
- SP LH Spiral Fluted Taps for Left Hand Threads
- SP V Spiral Fluted Taps, Coated
- AU+SP Plus Series Spiral Fluted Taps, Optimum Coating for the tapping
- AUXSP X Series Spiral Fluted Taps, Coated
- LS-SP Long Shank Spiral Fluted Taps
- LS-SP LH Long Shank Spiral Fluted Taps for Left Hand Threads
- LS-SP V Long Shank Spiral Fluted Taps, Coated
- SU+SP/SU-SP Spiral Fluted Taps for Stainless Steels
- SUXSP X Series Spiral Fluted Taps for Stainless Steels
- SU2-SP Spiral Fluted Taps for Tough Stainless Steels
- SU-S-SP Spiral Fluted Taps for Stainless Steels, Deep Hole Use
- S-SP Short Spiral Fluted Taps, Deep Hole Use
- E-SP Spiral Fluted Taps for Soft Structural Steels
- HC+SP/HC-SP Spiral Fluted Taps for High Carbon Steels
- HC+SP OX / HC-SP OX Spiral Fluted Taps for High Carbon Steels, Oxided
- AL+SP/AL-SP Spiral Fluted Taps for Aluminum
- AL-SP 1.5P Spiral Fluted Taps for Aluminum 1.5P
- LO-SP Low Spiral Fluted Taps
- LS-LO-SP Long Shank Low Spiral Fluted Taps
- MC-SP Spiral Fluted Taps with Internal Coolant Hole
- ZET-B Spiral Fluted Taps for Titanium Alloys
- ZEN-B Spiral Fluted Taps for Nickel Base Alloys
- F-SP Spiral Fluted Taps for High Speed Tapping
- HFIHS For Ultra Fast Tapping, Vertical Use. Spiral Fluted Taps for Carbon Steels
- HFISP For Ultra Fast Tapping, Horizontal Use. Low Spiral Fluted Taps for Carbon Steels
- HFAHS For Ultra Fast Tapping, Vertical Use. Spiral Fluted Taps for Aluminum
- HFASP For Ultra Fast Tapping, Horizontal Use. Low Spiral Fluted Taps for Aluminum
- HDISP For Dry Tapping, Blind Hole Use. Spiral Fluted Taps for Steels
- HDASP For Dry Tapping, Blind Hole Use. Spiral Fluted Taps for Aluminum
- SPIRAL FLUTED TAP SERIES FOR THROUGH HOLE
- XSL X Series Spiral Fluted Taps, Through Hole Use (with LH spiral flutes)
- AU+SL Spiral Fluted Taps, Coated, Through Hole Use(with LH spiral flutes)
- AUXSL X Series Spiral Fluted Taps, Coated, Through Hole Use (with LH spiral flutes)
- SU+SL Spiral Fluted Taps for Stainless Steels, Through Hole Use(with LH spiral flutes)
- SUXSL X Series Spiral Fluted Taps for Stainless Steels, Through Hole Use (with LH spiral flutes)
- ZET-P Spiral Fluted Taps for Titanium Alloys, Through Hole Use (with LH spiral flutes)
- F-SL Spiral Fluted Taps for High Speed Tapping, Through Hole Use (with LH spiral flutes)
- HDISL Spiral Fluted Taps for Steels, for Dry Tapping and for Ultra High Speed Tapping,Through Hole Use (with LH spiral flutes)
- MHSL Spiral Fluted Taps for Carbon Steels of middle hardness, Through Hole Use (with LH spiral flutes)
- SPIRAL POINTED TAP SERIES
- IPO Spiral Pointed Taps for General Purpose
- PO Spiral Pointed Taps
- +PO Plus Series Spiral Pointed Taps
- PO OX Spiral Pointed Taps, Oxided
- +PO OX Plus Series Spiral Pointed Taps, Oxided
- PO LH Spiral Pointed Taps for Left Hand Threads
- PO V Spiral Pointed Taps, Coated
- LS-PO Long Shank Spiral Pointed Taps
- LS-PO V Long Shank Spiral Pointed Taps, Coated
- SU+PO/SU-PO Spiral Pointed Taps for Stainless Steels
- S-PO Short Spiral Pointed Taps for Deep Hole Use
- HC+PO/HC-PO Spiral Pointed Taps for High Carbon Steels
- MC-PO Spiral Pointed Taps with Internal Coolant
- EH-PO Spiral Pointed Taps for Hard-to-Machine Materials
- ZEN-P Spiral Pointed Taps for Nickel Base Alloys
- HAND TAP SERIES
- IHT Hand Taps for General Purpose
- HT Hand Taps
- HT LH Hand Taps for Left Hand Threads
- LS-HT Long Shank Hand Taps
- LS-HT LH Long Shank Hand Taps for Left Hand Threads
- LS-HT V Long Shank Hand Taps, Coated
- SU-HT Hand Taps for Stainless Steels
- FC-HT Hand Taps for Cast Irons
- LA-HT Hand Taps for Die Cast Materials
- AXE-HT AXE Hand Taps
- MG-HT Hand Taps with Short Chamfer for Magnesium Alloy Castings
- AL-HT Hand Taps for Helical Coil Wire Screw Thread Inserts
- PL1 Hand Taps for Plastics
- MC-HT Hand Taps with Internal Coolant Hole
- EH-HT Hand Taps for Hard-to-Machine Materials
- CEMENTED CARBIDE TAP SERIES
- N-CT LA Carbide Taps for Light Alloys
- N-CT FC Carbide Taps for Cast Irons
- N-CT-PO Spiral Pointed Carbide Taps
- MC-AD-CT Carbide Taps with Oil Hole
- EH-CT Carbide Taps for Hard Materials
- UH-CT Carbide Taps for Ultra Hard Materials
- HFACT-P Carbide Taps for Ultra Fast Tappings, Through Hole Use, for Aluminum
- HFACT-B Carbide Taps for Ultra Fast Tappings, Blind Hole Use, for Aluminum
- HFICT-P Carbide Taps for Ultra Fast Tappings, Through Hole Use, for Cast Irons
- HFICT-B Carbide Taps for Ultra Fast Tappings, Blind Hole Use, for Cast Irons
- ROLL TAP SERIES
- N+RZ/N-RZ Thread Forming Taps for Steels
- LS-N-RZ Long Shank Thread Forming Taps for Steels
- N+RS/N-RS Thread Forming Taps for Non-Ferrous Materials
- LS-N-RS Long Shank Thread Forming Taps for Non-Ferrous Materials
- R+V Thread Forming Taps, Coated
- OL+RZ/OL-RZ Thread Forming Taps for Dry Tapping, Coated
- HP+RZ/HP-RZ High Performance Thread Forming Taps, Coated
- SC-TL-RZ Torqueless Thread Forming Taps with short chamfer
- SURZ SU Thread Forming Taps
- MHRZ Roll Taps for Carbon Steels of Middle Hardness
- SPECIAL THREAD TAPS / SIMPLE INSPECTION TOOLS
- MS+RS Roll Taps for Miniature Threads
- HPsRZ High Performance Roll Taps for Miniature Threads
- SIT Simple Thread Inspection Tools
- SITD(Tandem Type) Simple Thread Inspection Tools, Tandem Type
- CHECK PINS
- CPC-S Check Pins for Bored Hole in thread cut tapping (Straight Type)
- CPC-T Check Pins for Bored Holes in thread cut tapping (Taper Type)
- CPR-S Check Pins for Bored Hole in thread form tapping (Straight Type)
- CPR-T Check Pins for Bored Holes in thread form tapping (Taper Type)
- SA Shank Adjusters
- TA Tap Adapter
- PIPE TAP SERIES
- Rc Hand Taps for Taper Pipe Threads
- PT Hand Taps for Taper Pipe Threads, Long (ℓg) Type
- PT LH Hand Taps for Taper Pipe Threads, Long (ℓg) Type, for LH Threads
- PT-X X Series Hand Taps for Taper Pipe Threads, Short (ℓg) Type
- S-PT Hand Taps for Taper Pipe Threads, Short (ℓg) Type
- S-PT LH Hand Taps for Taper Pipe Threads, Short (ℓg) Type, for LH Threads
- LS-PT Long Shank Hand Taps for Taper Pipe Threads, Long (ℓg) Type
- LS-S-PT Long Shank Hand Taps for Taper Pipe Threads, Short (ℓg) Type
- SP-PT Spiral Fluted Taps for Taper Pipe Threads, Long (ℓg) Type
- SP-S-PT Spiral Fluted Taps for Taper Pipe Threads, Short (ℓg) Type
- SP-PT-X X Series Spiral Fluted Taps for Taper Pipe Threads, Short (ℓg) Type
- LS-SP-PT Long Shank Spiral Fluted Taps for Taper Pipe Threads, Long (ℓg) Type
- LS-SP-S-PT Long Shank Spiral Fluted Taps for Taper Pipe Threads, Short (ℓg) Type
- INT-PT Interrupted Taps for Taper Pipe Threads, Long (ℓg) Type
- INT-S-PT Interrupted Taps for Taper Pipe Threads, Short (ℓg) Type
- LS-INT-PT Long Shank Interrupted Taps for Taper Pipe Threads, Long (ℓg) Type
- LS-INT-S-PT Long Shank Interrupted Taps for Taper Pipe Threads, Short (ℓg) Type
- LC-PT Hand Taps for Taper Pipe Threads, Long (ℓg) Type, for Low Carbon Steels
- LC-S-PT Hand Taps for Taper Pipe Threads, Short (ℓg) Type, for Low Carbon Steels
- SU-PT Hand Taps for Taper Pipe Threads, Long (ℓg) Type, for Stainless Steels
- SU-S-PT Hand Taps for Taper Pipe Threads, Short (ℓg) Type, for Stainless Steels
- FC-PT Hand Taps for Taper Pipe Threads, Long (ℓg) Type, for Cast Irons
- FC-S-PT Hand Taps for Taper Pipe Threads, Short (ℓg) Type, for Cast Irons
- CT-PT Carbide Taps for Taper Pipe Threads, Long (ℓg) Type, for Cast Irons
- CT-S-PT Carbide Taps for Taper Pipe Threads, Short (ℓg) Type, for Cast Irons
- Rp Hand Taps for Parallel Pipe Threads
- PS Hand Taps for Parallel Pipe Threads
- PS LH Hand Taps for Parallel Pipe Threads, for LH Threads
- LS-PS Long Shank Hand Taps for Parallel Pipe Threads
- SP-PS Spiral Fluted Taps for Parallel Pipe Threads
- LS-SP-PS Long Shank Spiral Fluted Taps for Parallel Pipe Threads
- CT-PS Carbide Taps for Parallel Pipe Threads
- G Hand Taps for Parallel Pipe Threads
- PF Hand Taps for Parallel Pipe Threads
- PF LH Hand Taps for Parallel Pipe Threads, for LH Threads
- LS-PF Long Shank Hand Taps for Parallel Pipe Threads
- SP-PF Spiral Fluted Taps for Parallel Pipe Threads
- LS-SP-PF Long Shank Spiral Fluted Taps for Parallel Pipe Threads
- SU-PF Hand Taps for Parallel Pipe Threads, for Stainless Steels
- FC-PF Hand Taps for Parallel Pipe Threads, for Cast Irons
- CT-PF Carbide Taps for Parallel Pipe Threads
- NPT Hand Taps for American Taper Pipe Threads
- S-NPT Hand Taps for American Taper Pipe Threads, Short (ℓg) Type
- LS-NPT Long Shank Hand Taps for American Taper Pipe Threads
- SP-NPT Spiral Fluted Taps for American Taper Pipe Threads
- LS-SP-S-NPT Long Shank Spiral Fluted Taps for American Taper Pipe Threads, Short (ℓg) Type
- INT-NPT Interrupted Taps for American Taper Pipe Threads
- INT-S-NPT Interrupted Taps for American Taper Pipe Threads, Short (ℓg) Type
- NPTF Hand Taps for American Dryseal Taper Pipe Threads
- LS-NPTF Long Shank Hand Taps for American Dryseal Taper Pipe Threads
- NPS Hand Taps for American Parallel Pipe Threads
- NPSF Hand Taps for American Dryseal Parallel Pipe Threads
- THREAD MILLS
- MC-CSLC Carbide Thread Mills for Metric Internal Threads
- MC-CSLC Carbide Thread Mills for Taper Pipe Threads
- MC-CSLC Carbide Thread Mills for Parallel Pipe Threads
- MC-HLC Thread Mills for Metric Internal Threads
- MC-HLC Thread Mills for Taper Pipe Threads
- MC-HLC Thread Mills for Parallel Pipe Threads
- Dies
- D Solid Round Dies
- D LH Solid Round Dies for Left Hand Threads
- D PF Solid Round Dies for Parallel Pipe Threads
- D PF LH Solid Round Dies for Parallel Pipe Threads, for Left Hand Threads
- D NPSM Solid Round Dies for American Parallel Pipe Threads
- D PT Solid Round Dies for Taper Pipe Threads
- D PT LH Solid Round Dies for Taper Pipe Threads, for Left Hand Threads
- D NPT Solid Round Dies for American Taper Pipe Threads
- D NPTF Solid Round Dies for American Dryseal Taper Pipe Threads
- MS-RS-D/RS-D Rolling Dies
- N-RSD New Rolling Dies
- RD-DH Die Holders for Solid Dies
- RD-DC Die Collets for Die Holders
- RD-DA Die attachment (Designed Specially for Solid Round Dies)
- Center Drills/Centering Tools
- CESA High Helix Center Drills-JIS Type A 60°
- CE-S High Helix Center Drills-Type A 60°
- CD-S Low Helix Center Drills-Type A 60°
- CD-S LH Low Helix Center Drills-Type A 60°, Left Hand Cut
- CE-S V High Helix Center Drills-Type A 60°, Coated
- C-CD-S Carbide Center Drills-Type A 60°
- CE-SL Long Shank High Helix Center Drills-Type A 60°
- CD-SL Long Shank Low Helix Center Drills-Type A 60°
- CE-SL V Long Shank High Helix Center Drills-Type A 60°, Coated
- CD-SL V Long Shank Low Helix Center Drills-Type A 60°, Coated
- C-CD-SL Long Shank Carbide Center Drills-Type A 60°
- CEQA High Helix Center Drills-JIS Type A 90°
- CE-Q High Helix Center Drills-Type A 90°
- CD-Q Low Helix Center Drills-Type A 90°
- CD-Q LH Low Helix Center Drills - Type A 90°, Left Hand Cut
- CE-Q V High Helix Center Drills-Type A 90°, Coated
- CD-Q V Low Helix Center Drills-Type A 90°, Coated
- C-CD-Q Low Helix Carbide Center Drills-Type A 90°
- CE-QL Long Shank High Helix Center Drills-Type A 90°
- CE-QL V Long Shank High Helix Center Drills-Type A 90°, Coated
- C-CD-QL Long Shank Carbide Center Drills-Type A 90°
- CEIR High Helix Center Drills-JIS Type R
- CD-R Low Helix Center Drills-Type R
- CESB High Helix Center Drills-JIS Type B 60°
- CESC High Helix Center Drills-JIS Type C 60°
- MHCDS Center Drills for Carbon Steels of Middle Hardness for running at High Speed
- JOINT TOOLS
- JO-CES Joint- High Helix Center Drills-Type A 60°
- JO-CES V Joint- High Helix Center Drills-Type A 60°, Coated
- JO-CDS Joint- Low Helix Center Drills-Type A 60°
- JO-CDS V Joint- Low Helix Center Drills-Type A 60°, Coated
- JO-C-CDS Joint- Low Helix Carbide Center Drills-Type A 60°
- JO-PEQ Joint- Point Drills 90°
- JO-PEQ V Joint- Point Drills 90°, Coated
- JO-C-PEQ V Joint- Carbide Point Drills 90°, Coated
- JO-NCSD V Joint- NC Starting Drills for Beveling, Coated
- JO-CSQM Joint- Countersinks 90°, Drilling Machine Use
- JO-HOLDER Holders for Joint Tools, for 150mm and for 200mm
- POINT DRILLS
- PE-Q Point Drills 90°
- PE-Q V Point Drills 90°, Coated
- C-PE-Q V Carbide Point Drills 90°, Coated
- PE-QL V Long Shank Point Drills 90°, Coated
- PE-S Point Drills 60°
- PE-S V Point Drills 60°, Coated
- C-PE-S V Carbide Point Drills 60°,Coated
- PE-SL V Long Shank Point Drills 60°, Coated
- NC-SD V NC Starting Drills for Bevelling (90°), Coated
- NC-SD NC Starting Drills for Center Positioning (125°)
- CS-Q Countersinks 90°, Machining Center Use
- CS-QM Countersinks 90°and 60°, Drilling Machine Use
- CS-G Submarine Gate Cutter, 20°, 30°
- YAMAWA LINE-UPS ARRANGED ON SIZES
- Explanation of catalogue contents
- Flowchart : M2 tapping
- M2 Taps
- M2 Dies
- Flowchart : M3 tapping
- M3 Taps
- M3 Dies
- Flowchart : M4 tapping
- M4 Taps
- M4 Dies
- Flowchart : M5 tapping
- M5 Taps
- M5 Dies
- Flowchart : M6 tapping
- M6 Taps
- M6 Dies
- Flowchart : M8 tapping
- M8 Taps
- M8 Dies
- Flowchart : M10 tapping
- M10 Taps
- M10 Dies
- Flowchart : M12 tapping
- M12 Taps
- M12 Dies
- Explanation of catalogue contents
- M1.4-M7 Taps
- M1-M7 Dies
- M9-M24 Taps
- M9-M24 Dies
- M25-M48 Taps
- M26-M36 Dies
- Taps For Unified threads
- Dies For Unified threads
- Taps For Whitworth threads
- Dies For Pipe threads
- Taps For Pg threads
- Dies For American pipe threads
- PRAD system Solution tool
- Specification of corresponding standard blanks (for European market)
- Specification of corresponding standard blanks (for European market)
- Specification of corresponding standard blanks (for European market)
- Specification of corresponding standard blanks (for European market)
- YAMAWA Standard blank Line UP
- TECHNICAL INFORMATION
- 1.Terminology of Taps
- 2.Flutes
- 3.Edge angle and Cutting allowance of taps
- 4.Recommended Tapping Speeds
- 5.Tapping speed and Revolution
- 6.Tapping Torque
- 7.Metric Thread and Gauge Profile
- 8.Length of engagement
- 9.Classes of Internal Threads and Classes of Cutting Taps
- 10.About UNJ Threads
- 11.Accuracy of external threads and accuracy of Dies
- 12.Guide to Thread Forming Taps (Roll Taps)
- 13.How to set the tap's oversize to meet with the coating margin of internal threads
- 14.Tap, Thread Limits
- 15.Bored hole size before tapping ( for thread cutting )
- 16.Bored hole size before tapping ( for thread forming )
- 17.Bar diameter for external threads ( for cutting type dies )
- 18.Bar diameter of external threads (for thread rolling dies)
- 19.Surface Treatment
- 20.Carbide Taps
- 21.Taps for Pipe Threads
- 22.Features of MC-Helical Thread Mills
- 23.Selecting different tap holder combinations by machine feed system
- 24.The mechanism for a tap to cut oversize on an internal thread
- 25.Trouble Shooting
- 26.Center Drills
- 27.Table of recommend centering condition
- 28.Thread Series
- 29.Basic profile of threads
- 30.Symbols for Standard Threads
- 31.Cross chart of thread cutting tool standard
- 32.Hardness conversion table
- 33.Conversion table from inch to millimeter
- 34.Materials used for Cutting Tools
- Searching table by product name
- Alphabet of product name
- Overseas agency
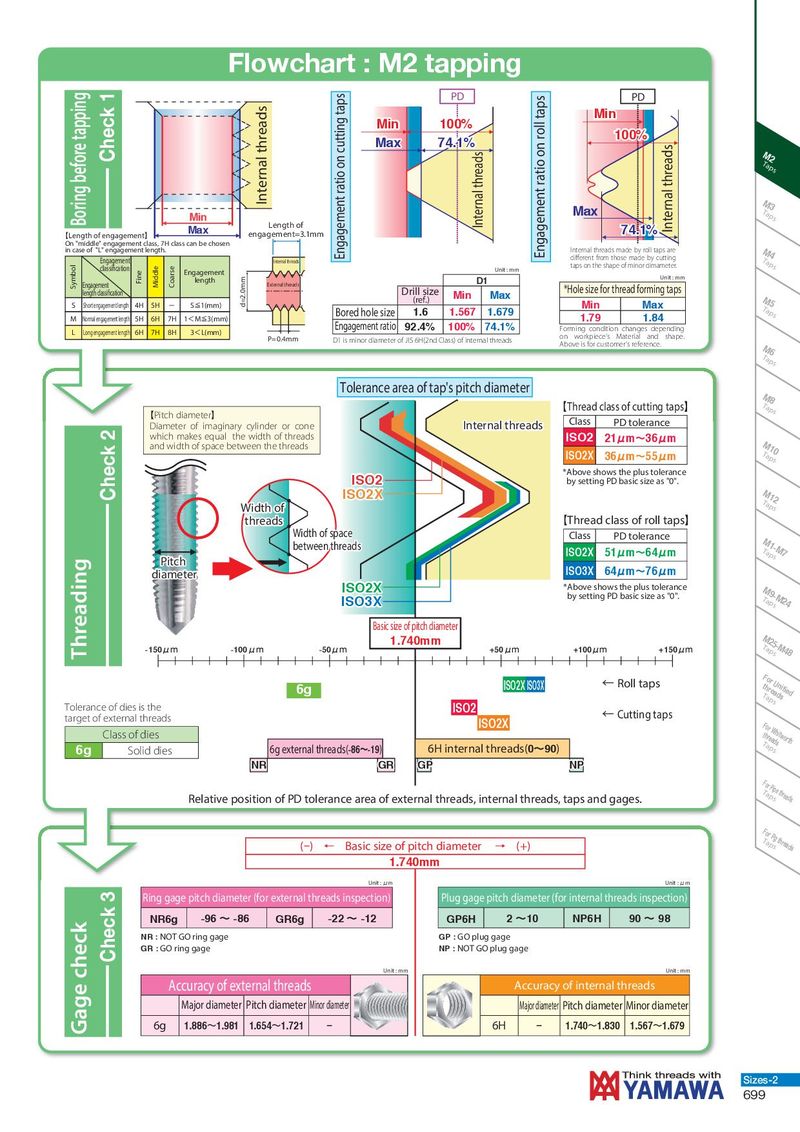
PD PD
MinMin
ℓ MinMin 100%
100%100% MaxMax 74.1% M2 Taps
P2 M3 MaxMax Taps Min
| Max | Length of | 74.1%74.1% | |||||
| P2 | engagement=3.1mm | ||||||
| Length of engagement | |||||||
| On "middle" engagement class, 7H class can be chosen | M4 | ||||||
| in case of "L" engagement length. | Internal threads made by roll taps are |
| Engagement | different from those made by cutting | Taps | |||
| Internal threads | taps on the shape of minor dimameter. | ||||
| classification | Unit : mm | ||||
| Engagement |
length D1 Unit : mm
Engagement External threads *Hole size for thread forming taps
| length classification | Drill size | Min | |||
| Max | M5 | ||||
| (ref.) |
P1 P2 S Short engagement length 4H 5H — S 1(mm) Min Max
Bored hole size 1.6 1.567 1.679 Taps
M Normal engagement length 5H 6H 7H 1 M 3(mm) 1.79 1.84
| Engagement ratio | 92.4% | 100% | 74.1% | |
| Forming condition changes depending |
| L | Long engagement length | 6H | 7H | 8H | 3 L(mm) | ||||
| P=0.4mm | on workpiece's Material and shape. | ||||||||
| D1 is minor diameter of JIS 6H(2nd Class) of internal threads | M6 | ||||||||
| Above is for customer's reference. | |||||||||
| Taps |
| 1 | Tolerance area of tap's pitch diameter | M8 | |||
| 2 | Thread class of cutting taps | Taps | |||
| 【Pitch diameter】 | |||||
| 3 | Internal threads Class | PD tolerance | |||
| Diameter of imaginary cylinder or cone | |||||
| 4 | which makes equal the width of threads | ISO2 | 21μm〜36μm | M10 | |
| H | and width of space between the threads | ||||
| ISO2X | 36μm〜55μm | Taps | |||
| H | |||||
| ISO2ISO2 | *Above shows the plus tolerance | ||||
| M5 | by setting PD basic size as "0". | M12 | |||
| ISO2XISO2X | |||||
| M4 | Taps | ||||
| Width of Width of | |||||
| M3 | threadsthreads | Thread class of roll taps |
| M1-M2 | width of space Width of space | Class | ||
| PD tolerance | M1-M |
| P6 | between threadsbetween threads | 7 μ 〜 μ |
| ISO2X | m m 64 51 Taps | |
| P5 | Pitch Pitch | |
| ISO3X | 64μm〜76μm | |
| diameterdiameter | ||
| P4 | ISO2XISO2X | M9-M |
| *Above shows the plus tolerance | ||
| P3 | ISO3XISO3X by setting PD basic size as "0". | 24 Taps |
| P2 | ||
| P1 | Basic size of pitch diameter | M25-M |
| 1.740mm | ||
| +50μm -50μm -100μm -150μm +100μm | 48 +150μm Taps | |
| S5 | ||
| S3 | For Unified | |
| ISO2X ISO3X | ← Roll taps threads | |
| S1-S2 | 6g | |
| N1 | < | Taps |
Tolerance of dies is the ISO2 ←
N2 > Cutting taps
target of external threads ISO2X For Whitworth
N3 Class of dies threads
| 6g | 6g external threads( | 〜 | ) | 6H internal threads( | 〜 | ) | Taps | ||||||
| N4 | Solid dies | -86 | -19 | 0 | 90 | ||||||||
| NR | GRGR | GP | NPNP |
For Pipe threads Taps Relative position of PD tolerance area of external threads, internal threads, taps and gages. For Pg threads
(–) ← Basic size of pitch diameter → (+) Taps 1.740mm
Unit : m Unit : m Ring gage pitch diameter (for external threads inspection) Plug gage pitch diameter (for internal threads inspection)
NR6g -96 〜 -86 GR6g -22 〜 -12 GP6H 2 〜10 NP6H 90 〜 98
NR : NOT GO ring gage GP : GO plug gage GR : GO ring gage NP : NOT GO plug gage Unit : mm Unit : mm Accuracy of external threads Accuracy of internal threads
Major diameter Pitch diameter Minor diameter Major diameter Pitch diameter Minor diameter
6g 〜 〜 − 6H − 〜 〜