Общий каталог Yamawa 2022 - 2023 - страница 1232
Навигация
 Краткое руководство Yamawa по каталогам
 Общий каталог Yamawa 2021
 Каталоги Yamawa твердосплавные метчики для закаленной стали
 Обший каталог Yamawa 2016 - 2017
- How to Read the General Catalog
- Z-PRO Product System
- New System table of taps for steels, blind hole use(low and middle speed range)
- New System table of taps for steels, blind hole use(Middle and High speed range)
- New System table of taps for steels, blind hole use(low and middle speed range)
- New System table of taps for steels, blind hole use(Middle and High speed range)
- New System table of taps for stainless steels, blind hole use
- New System table of taps for stainless steels, through hole use
- New System table of taps for non-ferrous materials, blind hole use
- New System table of taps for non-ferrous materials, through hole use
- New System table of roll taps for steels
- New System table of roll taps for non-ferrous materials
- YAMAWAPRODUCT LINE-UPS
- ①Spiral Fluted Tap Series for blind hole
- ②Spiral Fluted Tap Series for through hole
- ③Spiral Pointed Tap Series for through hole
- ④Hand Tap Series
- ⑤Cemented Carbide Tap Serie
- ⑥Roll Tap Series
- ⑦Special Thread Taps / Simple Inspection Tools
- ⑧Pipe Tap Series
- ⑨Thread Mills / Premium Thread Mills
- ⑩Dies
- ⑪Center Drills/Centering Tools
- ①Spiral Fluted Tap Series for blind hole
- ②Spiral Fluted Tap Series for through hole
- ③Spiral Pointed Tap Series for through hole
- ④Hand Tap Series
- ⑤Cemented Carbide Tap Series
- ⑥Roll Tap Series
- ⑦Special Thread Taps / Simple Inspection Tools
- ⑧Pipe Tap Series
- ⑩Dies
- ①Spiral Fluted Tap Series for blind hole
- ②Spiral Fluted Tap Series for through hole
- ③Spiral Fluted Tap Series for through hole
- ④Hand Tap Series
- ⑤Cemented Carbide Tap Series
- ⑥Roll Tap Series
- ⑦Special Thread Taps / Simple Inspection Tools
- ⑧Pipe Tap Series
- ⑩Dies
- ① SPIRAL FLUTED TAPSERIES FOR BLIND HOLE
- Selection chart of taps
- VUSP Z-PRO Coated Spiral Fluted Taps
- VUSP Z-PRO Coated Spiral Fluted Taps
- VUSP Z-PRO Coated Spiral Fluted Taps
- VUSP 1.5P Z-PRO Coated Spiral Fluted Taps 1.5P
- VUSP 1.5P Z-PRO Coated Spiral Fluted Taps 1.5P
- VUSP E Z-PRO Coated Spiral Fluted Taps E(1.5P)
- VUSP CH Z-PRO Coated Spiral Fluted Taps with Coolant Through Hole
- VUSP CH Z-PRO Coated Spiral Fluted Taps with Coolant Through Hole
- VUSP CH Z-PRO Coated Spiral Fluted Taps with Coolant Through Hole
- HVSP Z-PRO Spiral fluted Taps for Forged Parts in the Heavy Metalworking Industry
- HVSP Z-PRO Heavy Industry Spiral Fluted Tap for Large Parts Processing
- HVSP Z-PRO Heavy Industry Spiral Fluted Tap for Large Parts Processing
- MHSP Z-PRO Spiral Taps for Medium Hard Carbon Steels
- MHSP Z-PRO Spiral Taps for Medium Hard Carbon Steels
- SP Spiral Fluted Taps
- SP Spiral Fluted Taps
- SP Spiral Fluted Taps
- +SP Plus Series Spiral Fluted Taps
- SP 1.5P Spiral Fluted Taps 1.5P
- IS PSpiral Fluted Taps for General Purpose
- IS PSpiral Fluted Taps for General Purpose
- SP OX Spiral Fluted Taps,Oxidized
- SP OX Spiral Fluted Taps,Oxidized
- SP OX Spiral Fluted Taps, Oxidized
- SP Spiral Fluted Taps for Alloy Steels
- SP LH Spiral Fluted Taps for Left Hand Threads
- SP LH Spiral Fluted Taps for Left Hand Threads
- SP V Spiral Fluted Taps, Coated
- AU+SP Plus Series Spiral Fluted Taps,Optimum Coating for the Tapping
- AU+SP Plus Series Spiral Fluted Taps,Coated
- AU+SP Plus Series Spiral Fluted Taps, Coated
- LS-SP Long Shank Spiral Fluted Taps
- LS-SP OX Long Shank Oxidized Spiral Tap
- LS-SP LH Long Shank Spiral Fluted Taps for Left Hand Threads
- LS-SP V Long Shank Spiral Fluted Taps, Coated
- LS-SP-K Long Shank Spiral Fluted Taps with Long Neck
- SU+SP SU-SP Spiral Fluted Taps for Stainless Steels
- ZELX SS SP Spiral Fluted Taps for Stainless Steels
- SP-VA Spiral Fluted Taps for Stainless Steels
- SP+VA Spiral Fluted Taps for Stainless Steels
- SP-VA Spiral Fluted Taps for Stainless Steels, Coated
- SU2-SP Spiral Fluted Taps for Tough Stainless Steels
- SU2-SP Spiral Fluted Taps for Tough Stainless Steels
- SU-S-SP Spiral Fluted Taps for Stainless Steels, Deep Hole Use
- LS-SU-S-SP Long Shank Spiral Fluted Taps for Stainless Steels, Deep Hole Use
- ZELX SS SP 6" Long Shank Spiral Fluted Taps for Stainless Steels
- S-SP Short Spiral Fluted Taps, Deep Hole Use
- SP-BLF Spiral Fluted Taps, Deep Hole Use
- SP-BLF OX Spiral Fluted Taps, Deep Hole Use, Oxidized
- SP-BLF Spiral Fluted Taps, Deep Hole Use(Coated)
- E-SP Spiral Fluted Taps for Soft Structural Steels
- HC+SP HC-SP Spiral Fluted Taps for High Carbon Steels
- HC+SP OX HC-SP OX Spiral Fluted Taps for High Carbon Steels, Oxidized
- AL+SP AL-SP Spiral Fluted Taps for Aluminum
- AL-SP 1.5P Spiral Fluted Taps for Aluminum 1.5P
- AL-SP Spiral Fluted Taps for Aluminum
- AL+SP AL-SP Spiral Fluted Taps for Aluminum
- ALS-SP Spiral Fluted Taps for Aluminum
- LO-SP Low Spiral Fluted Taps
- LO-SP Low Spiral Fluted Taps for Alloy Steels
- LO-SP Low Spiral Fluted Taps
- LO-SP OX Low Spiral Fluted Taps, OxidizedDIN
- LS-LO-SP Long Shank Low Spiral Fluted Taps
- ZET-B Spiral Fluted Taps for Titanium Alloys
- ZELX TI SP Spiral Fluted Taps for Titanium Alloys
- ZET-B Spiral Fluted Taps for Titanium Alloys
- ZEN-B Spiral Fluted Taps for Nickel Base Alloys
- ZELX NI SP Spiral Fluted Taps for Nickel Base Alloys
- ZEN-B Spiral Fluted Taps for Nickel Base Alloys
- PM-SP Spiral Fluted Taps for Hard-to-Machine Materials
- PM-SP Spiral Fluted Taps for Hard-to-Machine Materials
- PH-SP Spiral Fluted Taps for Hard-to-Machine Materials
- LS-PM-SP Long Shank Spiral Fluted Taps for Hard-to-Machine Materials
- F-SP Spiral Fluted Taps for High Speed Tapping
- ZELX FR Spiral Fluted Taps for High Speed Tapping
- F-SP Spiral Fluted Taps for High Speed Tapping
- LS-F-SP Long Shank Spiral Fluted Taps for High Speed Tapping
- HFIHS For Ultra Fast Tapping, Vertical Use. Spiral Fluted Taps for Steels
- HFIHS For Ultra Fast Tapping, Vertical Use. Spiral Fluted Taps for Steels
- HFISP For Ultra Fast Tapping, Horizontal Use. Low Spiral Fluted Taps for Steels
- HFISP For Ultra Fast Tapping, Horizontal Use. Low Spiral Fluted Taps for Steels
- HFAHS For Ultra Fast Tapping, Vertical Use. Spiral Fluted Taps for Aluminum
- HFAHS For Ultra Fast Tapping, Vertical Use, Spiral Fluted Taps for Aluminum
- HFASP For Ultra Fast Tapping, Horizontal Use. Low Spiral Fluted Taps for Alum
- HFASP For Ultra Fast Tapping, Horizontal Use, Low Spiral Fluted Taps for Aluminum
- HDISP For Dry Tapping, Blind Hole Use. Spiral Fluted Taps for Steels
- HDISP For Dry Tapping, Blind Hole Use, Spiral Fluted Taps for Steels
- HDASP For Dry Tapping, Blind Hole Use. Spiral Fluted Taps for Aluminum
- HDASP For Dry Tapping, Blind Hole Use, Spiral Fluted Taps for Aluminum
- MC-SP Spiral Fluted Taps with Internal Coolant Hole
- XSP X Series Spiral Fluted Taps
- AUXSP X Series Spiral Fluted Taps, Coated
- AUXSP X SeriesSpiral Fluted Taps, Coated
- SUXSP X Series Spiral Fluted Taps for Stainless Steels
- ② SPIRAL FLUTED TAP SERIESFOR THROUGH HOLE
- Selection chart of taps
- MHSL Z-PROSpiral Fluted Taps for Carbon Steels of Medium Hardness,Through Hole Use (with LH Spiral Flutes)
- MHSL Spiral Fluted Taps for Carbon Steels of Medium Hardness,Through Hole Use (with LH Spiral Flutes)
- MHSL Z-PRO Spiral Fluted Taps for Carbon Steels of MediumHardness, Through Hole Use (with LH Spiral Flutes)
- MHSL Z-PRO Spiral Fluted Taps for Carbon Steels of MediumHardness, Through Hole Use( with LH Spiral Flutes)
- LKSL Z-PRO Long Neck Spiral Fluted Tap for Through Hole
- LKSL XL Z-PRO Extra-Long Neck Spiral Fluted Tap for Through Hole
- AU+SL Spiral Fluted Taps, Coated, Through Hole Use(with LH Spiral Flutes)
- AU+SL Spiral Fluted Taps, Coated, Through Hole Use( with LH Spiral Flutes
- SU+SL Spiral Fluted Taps for Stainless Steels, Through Hole Use(with LH Spiral Flutes)
- SL+VA Spiral Fluted Taps for Stainless Steels, Through Hole Use(with LH Spiral Flutes)
- ZET-P Spiral Fluted Taps for Titanium Alloys, Through Hole Use (with LH Spiral Flutes)
- ZELX TI LHSP Spiral Fluted Taps for Titanium Alloys, Through Hole Use(with LH Spiral Flutes)
- ZET-P Spiral Fluted Taps for Titanium Alloys, Through Hole Use( with LH Spiral Flutes)
- F-SL Spiral Fluted Taps for High Speed Tapping, Through Hole Use (with LH Spiral Flutes)
- ZELX FR LHSP Spiral Fluted Taps for High Speed Tapping, Through Hole Use( with LH Spiral Flutes)
- F-SL Spiral Fluted Taps for High Speed Tapping, Through Hole Use( with LH Spiral Flutes)
- LS-F-SL Long Shank Spiral Fluted Taps for High Speed Tapping, Through Hole Use (with LH Spiral Flutes)
- HDISL Spiral Fluted Taps for Steels, for Dry Tapping and for UltraHigh Speed Tapping, Through Hole Use (with LH Spiral Fluted)
- HDISL Spiral Fluted Taps for Steels, for Dry Tapping and for UltraHigh Speed Tapping, Through Hole Use( with LH Spiral Flutes)
- XSL X Series Spiral Fluted Taps, Through Hole Use (with LH Spiral Flutes)
- AUXSL X Series Spiral Fluted Taps, Coated, Through Hole Use (with LH Spiral Flutes)
- AUXSL X Series Spiral Fluted Taps, Coated, Through Hole Use( with LH Spiral Flutes
- SUXSL X Series Spiral Fluted Taps for Stainless Steels, Through Hole Use (with LH Spiral Flutes)
- ③ SPIRAL POINTEDTAP SERIESFOR THROUGH HOLE
- Selection chart of taps
- VUPO Z-PRO Coated Spiral Pointed T
- VUPO Z-PRO Coated Spiral Pointed Taps
- VUPO Z-PRO Coated Spiral Pointed Taps
- PO Spiral Pointed Taps
- PO Spiral Pointed Taps
- PO Spiral Pointed Taps
- +PO Plus Series Spiral Pointed Taps
- IPO Spiral Pointed Taps for General Purpose
- IPO Spiral Pointed Taps for General Purpose
- PO OX Spiral Pointed Taps, Oxidized
- PO OX Spiral Pointed Taps, Oxidized
- PO OX Spiral Pointed Taps, Oxidized
- PO LH Spiral Pointed Taps for Left Hand Threads
- PO V Spiral Pointed Taps, Coated
- PO VSpiral Pointed Taps, Coated
- LS-PO Long Shank Spiral Pointed Taps
- LS-PO V Long Shank Spiral Pointed Taps, Coated
- LS-PO-K Long Shank Spiral Pointed Taps with Long Neck
- SU+PO SU-PO Spiral Pointed Taps for Stainless Steels
- ZELX SS PO Spiral Pointed Taps for Stainless Steels
- PO-VA Spiral Pointed Taps for Stainless Steels
- PO-VA Spiral Pointed Taps for Stainless Steels, Coated
- LS-SU-S-PO Long Shank Short Spiral Pointed Taps for Stainless Steels
- ZELX SS PO 6" Long Shank Spiral Pointed Taps for Stainless Steels
- S-PO Short Spiral Pointed Taps for Deep Hole Use
- HC+PO HC-PO Spiral Pointed Taps for High Carbon Steels
- HC-PO OX Oxidized Spiral Pointed Taps for High Carbon Steels
- AL-PO Spiral Pointed Taps for Aluminum
- EH-PO Spiral Pointed Taps for Hard-to-Machine Materials
- EH-PO Spiral Pointed Taps for Hard-to-Machine Materials
- ZEN-P Spiral Pointed Taps for Nickel Base Alloys
- ZELX NI PO Spiral Pointed Taps for Nickel Base Alloys
- ZEN-P Spiral Pointed Taps for Nickel Base Alloys
- PM-PO Spiral Pointed Taps for Hard-to-Machine Materials
- PM-PO Spiral Pointed Taps for Hard-to-Machine Materials
- LS-PM-PO Long Shank Spiral Pointed Taps for Hard-to-Machine Materials
- MC-PO Spiral Pointed Taps with Internal Coolant
- ④ HAND TAP SERIES
- Selection chart of taps
- HT Hand Taps
- HT Hand Taps
- HT Hand Taps
- IHT Hand Taps for General Purpose
- IHT Hand Taps for General Purpose
- HT OX Hand Taps, Oxidized
- HT LH Hand Taps for Left Hand Threads
- LS-HT Long Shank Hand Taps
- LS-HT LH Long Shank Hand Taps for Left Hand Threads
- LS-HT V Long Shank Hand Taps, Coated
- SU-HT Hand Taps for Stainless Steels
- FC-HT Hand Taps for Cast Irons
- HT-CI Hand Taps for Cast Irons
- GG-HT Hand Taps for Cast Irons
- GG-HT Hand Taps for Cast Irons, Coated
- GGST Z-PRO Straight Fluted Taps for Cast Irons
- GGST CH Z-PRO Straight Fluted Taps for Cast Irons with Coolant Through Hole,Blind Hole Use
- GG-HT-OH Hand Taps for Cast Irons with Internal Coolant Hole
- GG-HT-OH Hand Taps for Cast Irons with Internal Coolant Hole, Coated
- LA-HT Hand Taps for Die Cast Materials
- LA-HT Hand Taps for Die Cast Materials
- AXE-HT AXE Hand Taps
- AXE-HT AXE Hand Taps
- AXE-HT AXE Hand Taps
- MG-HT Hand Taps with Short Chamfer for Magnesium Alloy Castings
- PL1 Hand Taps for Plastics
- EH-HT Hand Taps for Hard-to-Machine Materials
- EH-HT Hand Taps for Hard-to-Machine Materials
- ZELX MOLD Hand Taps for Hard-to-Machine Materials
- EH-HT Hand Taps for Hard-to-Machine Materials
- RE-HT Hand Tap for Thread Repair
- MS+TR Hand Tap for Miniature Threads
- MC-HT Hand Taps with Internal Coolant Hole
- ⑤ CEMENTED CARBIDETAP SERIES
- Selection chart of taps
- N-CT LA Carbide Taps for Light Alloys
- ZELX CARB AL Carbide Taps for Light Alloys
- CT LA Carbide Taps for Light Alloys
- N-CT FC Carbide Taps for Cast Irons
- ZELX CARB CI Carbide Taps for Cast Irons
- LS-N-CT Long Shank Carbide Taps
- N-CT-SP Spiral Fluted Carbide Taps
- N-CT-PO Spiral Pointed Carbide Taps
- EH-CT Carbide Taps for Hard Materials
- EH-CT Carbide Taps for Hard Materials
- UH-CT Carbide taps for ultra hard materials
- UH-CT Carbide taps for ultra hard materials
- HFACT-P Carbide Taps for Ultra Fast Tappings, Through Hole Use, for Aluminum
- HFACT-B Carbide Taps for Ultra Fast Tappings, Blind Hole Use, for Aluminum
- HFICT-P Carbide Taps for Ultra Fast Tappings, Through Hole Use, for Cast Irons
- HFICT-B Carbide Taps for Ultra Fast Tappings, Blind Hole Use, for Cast Irons
- ACHSP Spiral Fluted Tap for Aluminum Casting
- MC-AD-CT Carbide Taps with Oil Hole
- ⑥ ROLL TAP SERIES
- Selection chart of taps
- MHRZ Z-PRO Roll Taps for Medium Hardness Carbon Steels
- MHRZ Roll Taps for Medium Hardness Carbon Steels
- MHRZ Z-PRO Roll Taps for Medium Hardness Carbon Steels
- MHRZ Z-PRO Roll Taps for Medium Hardness Carbon Steels
- N+RZ N-RZ Roll Taps for Steels
- N-RZ Roll Taps for Steels
- N+RZ N-RZ Roll Taps for Steels
- LS-N-RZ Long Shank Roll Taps for Steels
- N+RS N-RS Roll Taps for Non-Ferrous Materials
- N-RS Roll Taps for Non-Ferrous Materials
- N+RS N-RS Roll Taps for Non-Ferrous Materials
- LS-N-RS Long Shank Roll Taps for Non-Ferrous Materials
- R+V Roll Taps, Coated
- OL+RZ OL-RZ Roll Taps for Dry Tapping, Coated
- OL-RZ Roll Taps for Dry Tapping, Coated
- OL+RZ Roll Taps for Dry Tapping, Coated
- HP+RZ HP-RZ High Performance Roll Taps, Coated
- HP-RZ High Performance Roll Taps, Coated
- HP+RZ HP-RZ High Performance Roll Taps, Coated
- SC-TL-RZ Torqueless Roll Taps with Short Chamfer
- SURZ SU Roll Taps
- MS+RS Roll Taps for Miniature Threads
- HPsRZ High Performance Roll Taps for Miniature Threads
- R-Y Roll Taps for Thin Soft Structural Steel Sheets
- R-D Roll Taps for General Purpose
- R-D Roll Taps for General Purpose, Coated
- R-D Roll Taps for General Purpose, Coated
- ⑦ SPECIAL THREAD TAPS /SIMPLE INSPECTION TOOLS
- Selection chart of taps
- AL-HT STI Hand Taps for Aluminum Materials (for Helical Coil Wire Screw Thread Inserts)
- HT STI Hand Taps for Helical Coil Wire Screw Thread Inserts
- HT OX STI Hand Taps for Helical Coil Wire Screw Thread Inserts, Oxided
- AL-SP STI Spiral Fluted Taps for Aluminum Materials (for Helical Coil Wire Screw Thread Inserts)
- SP STI Spiral Fluted Taps for Helical Coil Wire Screw Thread Inserts
- SP OX STI Spiral Fluted Taps for Helical Coil Wire Screw Thread Inserts, Oxided
- ZELX NI SP STI Spiral Fluted Taps for Helical Coil Wire Screw Thread Inserts and for Nickel Base Alloys
- AL-PO STI Spiral Pointed Taps for Aluminum Materials (for Helical Coil Wire Screw Thread Inserts)
- PO STI Spiral Pointed Taps for Helical Coil Wire Screw Thread Inserts
- PO OX STI Spiral Pointed Taps for Helical Coil Wire Screw Thread Inserts, Oxidized
- ZELX NI PO STI Spiral Pointed Taps for Helical Coil Wire Screw Thread Inserts and for Nickel Base Alloys
- N-RS STI Roll Taps for Nonferrous Materials (for Helical Coil Wire Screw Thread Inserts)
- N-CT LA STI Carbide Hand Taps for Light Alloys (for Helical Coil Wire Screw Thread Inserts)
- NT Nut Taps
- HT TRI Hand Taps for Tripod Threads
- SP TRI Spiral Fluted Taps for Tripod Threads
- RLS-HT Hand Taps for Camera Release Threads
- HT TV Hand Taps for Automobile Tire Valve Threads
- HT CTV Hand Taps for Bicycle Tire Valve Threads
- HT CTC Hand Taps for Steel Conduit Threads
- HT CTG Hand Taps for Thick Steel Conduit Threads
- HT Pg Hand Taps for Steel Conduit Threads
- HT BC Hand Taps for Bicycle Threads
- HT MST Hand Tap for Microscope Objective Lens
- SL Tr Spiral Flute Tap for Through Hole for Trapezoidal Threads
- SL LH Tr A Spiral Flute Left Hand Trapezoidal Thread Tap Spiral Tap
- SIT Simple ThreadInspection Tools
- SITD Simple Thread Inspection Tools,Tandem Type
- CHECK PINS
- CPC-S Check Pins for Bored Hole in Thread Cut Tapping (Straight Type)
- CPC-T Check Pins for Bored Holes in Thread Cut Tapping (Taper Type)
- CPR-S Check Pins for Bored Hole in Thread Form Tapping (Straight Type)
- CPR-T Check Pins for Bored Holes in Thread Form Tapping (Taper Type)
- CPR-Y Check-Pins for Bored Holes in Thread Form Tapping for R-Y Taps.
- SA Shank Adjusters
- ITRD Broken Tap Removal Tools
- ⑧ PIPE TAP SERIES
- Selection chart of taps
- AUSP Rc Z-PRO Coated Spiral Fluted Taps for Taper Pipe Threads
- AUSP Rp Z-PRO Coated Spiral Fluted Taps for Parallel Pipe Threads
- AUSP G Z-PRO Coated Spiral Fluted Taps for Parallel Pipe Threads
- Rc Hand Taps for Taper Pipe Threads
- PT Hand Taps for Taper Pipe Threads, Long (ℓg) Type
- PT LH Hand Taps for Taper Pipe Threads Long (ℓg) Type for LH Threads
- PT-X X Series Hand Taps for Taper Pipe Threads Short (ℓg) Type
- S-PT Hand Taps for Taper Pipe Threads Short (ℓg) Type
- S-PT LH Hand Taps for Taper Pipe Threads Short (ℓg) Type for LH Threads
- LS-PT Long Shank Hand Taps for Taper Pipe Threads Long (ℓg) Type
- LS-S-PT Long Shank Hand Taps for Taper Pipe Threads, Short (ℓg) Type
- SP-PT Spiral Fluted Taps for Taper Pipe Threads, Long (ℓg) Type
- SP-S-PT Spiral Fluted Taps for Taper Pipe Threads Short (ℓg) Type
- SP-PT-X X Series Spiral Fluted Taps for Taper Pipe Threads Short (ℓg) Type
- LS-SP-PT Long Shank Spiral Fluted Taps for Taper Pipe Threads, Long (ℓg) Type
- LS-SP-S-PT Long Shank Spiral Fluted Taps for Taper Pipe Threads, Short (ℓg) Type
- INT-PT Interrupted Taps for Taper Pipe Threads, Long (ℓg) Type
- INT-S-PT Interrupted Taps for Taper Pipe Threads, Short (ℓg) Type
- LS-INT-PT Long Shank Interrupted Taps for Taper Pipe Threads, Long (ℓg) Type
- LS-INT-S-PT Long Shank Interrupted Taps for Taper Pipe Threads, Short (ℓg) Type
- LC-PT Hand Taps for Taper Pipe Threads Long (ℓg) Type, for Low Carbon Steels
- LC-S-PT Hand Taps for Taper Pipe Threads Short (ℓg) Type, for Low Carbon Steels
- SU-PT Hand Taps for Taper Pipe Threads Long (ℓg) Type, for Stainless Steels
- SU-S-PT Hand Taps for Taper Pipe Threads Short (ℓg) Type, for Stainless Steels
- SU-SP-PT Spiral Fluted Taps for Taper Pipe Threads, Long (ℓg) Type for Stainless Steels
- SU-SP-S-PT Spiral Fluted Taps for Taper Pipe Threads Short (ℓg) Type for Stainless Steels
- FC-PT Hand Taps for Taper Pipe Threads, Long (ℓg) Type, for Cast Irons
- FC-S-PT Hand Taps for Taper Pipe Threads, Short (ℓg) Type, for Cast Irons
- CT-PT Carbide Taps for Taper Pipe Threads, Long (ℓg) Type, for Cast Irons
- CT-S-PT Carbide Taps for Taper Pipe Threads, Short (ℓg) Type, for Cast Irons
- Rp Hand Taps for Parallel Pipe Threads
- PS Hand Taps for Parallel Pipe Threads
- PS LH Hand Taps for Parallel Pipe Threads, for LH Threads
- LS-PS Long Shank Hand Taps for Parallel Pipe Threads
- SP-PS Spiral Fluted Taps for Parallel Pipe Threads
- LS-SP-PS Long Shank Spiral Fluted Taps for Parallel Pipe Threads
- FC-PS Hand Tap for Parallel Pipe Threads in Cast Irons
- CT-PS Carbide Taps for Parallel Pipe Threads
- G Hand Taps for Parallel Pipe Threads
- HT G Hand Taps for Parallel Pipe Threads
- GG-HT G Hand Taps for Parallel Pipe Threads, for Cast Irons
- GGST G Z-PRO Straight Fluted Taps for Parallel Pipe Threads, for Cast Irons
- GG-HT G Hand Taps for Parallel Pipe Threads, for Cast Irons (Coated)
- EH-HT G Hand Taps for Parallel Pipe Threads, for Hard-to-Machine Materials
- SP G Spiral Fluted Taps for Parallel Pipe Threads
- SP OX G Spiral Fluted Taps for Parallel Pipe Threads, Oxidized
- SP V G Spiral Fluted Taps for Parallel Pipe Threads, Coated
- SP-VA G Spiral Fluted Taps for Parallel Pipe Threads, for Stainless Steels
- SU2-SP G Spiral Fluted Taps for Parallel Pipe Threads, for Tough Stainless Steels
- LO-SP G Low Spiral Fluted Taps for Parallel Pipe Threads
- LO-SP OX G Low Spiral Fluted Taps for Parallel Pipe Threads, Oxidized
- PH-SP G Spiral Fluted Taps for Parallel Pipe Threads, for Hard-to-Machine Materials
- PO G Spiral Pointed Taps for Parallel Pipe Threads
- PO OX G Spiral Pointed Taps for Parallel Pipe Threads, Oxidized
- PO V G Spiral Pointed Taps for Parallel Pipe Threads, Coated
- PO-VA G Spiral Pointed Taps for Parallel Pipe Threads, for Stainless Steels
- R-D G Roll Taps for Parallel Pipe Threads, for General Purpose
- R-D G Roll Taps for Parallel Pipe Threads, for General Purpose, Coated
- PF Hand Taps for Parallel Pipe Threads
- PF LH Hand Taps for Parallel Pipe Threads, for LH Threads
- LS-PF Long Shank Hand Taps for Parallel Pipe Threads
- SP-PF Spiral Fluted Taps for Parallel Pipe Threads
- LS-SP-PF Long Shank Spiral Fluted Taps for Parallel Pipe Threads
- SU-PF Hand Taps for Parallel Pipe Threads, for Stainless Steels
- SU-SP-PF Spiral Fluted Taps for Parallel Pipe Threads, for Stainless Steels
- FC-PF Hand Taps for Parallel Pipe Threads, for Cast Irons
- CT-PF Carbide Taps for Parallel Pipe Threads
- NPT Hand Taps for American Taper Pipe Threads
- NPT Hand Taps for American Taper Pipe Threads
- ZELX MOLD NPT Hand Taps for Hard-to-Machine Materials For American Taper Pipe Threads
- NPT-CI Hand Taps for American Taper Pipe Threads for Cast Irons
- S-NPT Hand Taps for American Taper Pipe Threads, Short (ℓg) Type
- LS-NPT Long Shank Hand Taps for American Taper Pipe Threads
- SP-NPT Spiral Fluted Taps for American Taper Pipe Threads
- ZELX SS NPT Taps for American Taper Pipe Threads
- LS-SP-S-NPT Long Shank Spiral Fluted Taps for American Taper Pipe Threads, Short (ℓg) Type
- INT-NPT Interrupted Taps for American Taper Pipe Threads
- INT-NPT Interrupted Taps for American Taper Pipe Threads
- INT-S-NPT Interrupted Taps for American Taper Pipe Threads, Short (ℓg) Type
- NPTF Hand Taps for American Dryseal Taper Pipe Threads
- NPTF Hand Taps for American Dryseal Taper Pipe Threads
- NPTF-CI Hand Taps for American Dryseal Taper Pipe Threads, for Cast Irons
- ZELX SS NPTF Taps for American Dryseal Taper Pipe Threads
- LS-NPTF Long Shank Hand Taps for American Dryseal Taper Pipe Threads
- NPS Hand Taps for American Parallel Pipe Threads
- NPS Hand Taps for American Parallel Pipe Threads
- NPSF Hand Taps for American Dryseal Parallel Pipe Threads
- NPSFHand Taps for American Dryseal Parallel Pipe Threads
- ⑨ THREAD MILLS /PREMIUM THREAD MILLS
- Selection chart of Thread Mills
- PRML Z-PRO Premium Thread Mills
- PRML TI Z-PRO Premium Thread Mills for Heat-Resistant Alloys
- MC-CSLC Carbide Thread Mills for Metric Internal Threads
- MC-CSLC Carbide Thread Mills for Taper Pipe Threads
- MC-CSLC Carbide Thread Mills for Parallel Pipe Threads
- MC-HLC Thread Mills for Metric Internal Threads
- MC-HLC Thread Mills for Taper Pipe Threads
- MC-HLC Thread Mills for Parallel Pipe Threads
- ⑩ DIES
- D Solid Round Dies
- D LH Solid Round Dies for Left Hand Threads
- D PT Solid Round Dies for Taper Pipe Threads
- D PT LH Solid Round Dies for Taper Pipe Threads, for Left Hand Threads
- D PF Solid Round Dies for Parallel Pipe Threads
- D PF LH Solid Round Dies for Parallel Pipe Threads, for Left Hand Threads
- D NPT Solid Round Dies for American Taper Pipe Threads
- D NPTF Solid Round Dies for American Dryseal Taper Pipe Threads
- D NPSM Solid Round Dies for American Parallel Pipe Threads
- DPO Spiral Pointed HSS Round Dies
- DPO Spiral Pointed HSS Round Dies
- SP-D Spiral Fluted HSS Round Dies
- HS-D HSS Round Dies for Auto Lathe, for Stainless Steel
- MS-RS-D RS-D Rolling Dies
- N-RSD New Rolling Dies
- RD-DA Die Attachment (Designed Specially for Solid Round Dies)
- RD-DA Die Attachment (Designed Specially for Solid Round Dies)
- ⑪ CENTER DRILLS /CENTERING TOOLS
- CESA High Helix Center Drills-JIS Type A 60°
- CE-S High Helix Center Drills-Type A 60°
- CE-S(I) High Helix Center Drills-Type A 60°, (Old JIS Type 1 )
- CD-S Low Helix Center Drills-Type A 60°
- CD-S(I) Low Helix Center Drills-Type A 60°, (Old JIS Type 1 )
- CD-S LH Low Helix Center Drills-Type A 60°, Left Hand Cut
- CE-S V High Helix Center Drills-Type A 60°, Coated
- CE-S V(I) High Helix Center Drills-Type A 60°, Coated, (Old JIS Type 1 )
- CD-S V Type A Low Helix Coated 60° Center Hole Drill
- CD-S V(I) Coating Low Helix A Type 60° Center Hole Drill Former JIS Type 1
- C-CD-S Carbide Center Drills-Type A 60°
- CE-SL Long Shank High Helix Center Drills-Type A 60°
- CD-SL Long Shank Low Helix Center Drills-Type A 60°
- CE-SL V Long Shank High Helix Center Drills-Type A 60°, Coated
- CD-SL V Long Shank Low Helix Center Drills-Type A 60°, Coated
- C-CD-SL Long Shank Low Helix Carbide Center Drills-Type A 60°
- CEQA High Helix Center Drills-JIS Type A 90°
- CE-Q High Helix Center Drills-Type A 90°
- CD-Q Low Helix Center Drills-Type A 90°
- CD-Q LH Low Helix Center Drills - Type A 90°, Left Hand Cut
- CE-Q V High Helix Center Drills-Type A 90°, Coated
- CD-Q V Low Helix Center Drills-Type A 90°, Coated
- C-CD-Q Low Helix Carbide Center Drills-Type A 90°
- CE-QL Long Shank High Helix Center Drills-Type A 90°
- CE-QL V Long Shank High Helix Center Drills-Type A 90°, Coated
- C-CD-QL Long Shank Low Helix Carbide Center Drills-Type A 90°
- CESB High Helix Center Drills-JIS Type B 60°
- CE-S(II) High Helix Center Drills-Type B 60°, (Old JIS Type 2 )
- CD-S(II) Low Helix Center Drills-Type B 60°, (Old JIS Type 2 )
- CESC High Helix Center Drills-JIS Type C 60°
- CEIR High Helix Center Drills-JIS Type R
- CD-R Low Helix Center Drills-Type R
- CE-T High Helix A Type 75° Center Hole Drill
- MHCDS Center Drills for Carbon Steels of Medium Hardness forRunning at High Speed
- AUCES Coated Type A 60° High Helix Single End Center Hole Drill
- AUCDS Coated Type A 60° Low Helix Single End Center Hole Drill
- AUPEQ Coated Single End Point Drill PE-90°
- AUPES Coated Single End Point Drill PE-60°
- SHANK EXTENSION Shank Extension
- POINT DRILLS
- PE-Q Point Drills 90°
- PE-Q V Point Drills 90°, Coated
- C-PE-Q V Carbide Point Drills 90°, Coated
- PE-QL V Long Shank Point Drills 90°, Coated
- PE-S Point Drills 60°
- PE-S V Point Drills 60°, Coated
- C-PE-S V Carbide Point Drills 60°, Coated
- PE-SL V Long Shank Point Drills 60°, Coated
- NC-SD V NC Starting Drills for Chamfering (90°), Coated
- NC-SD NC Starting Drills for Center Positioning (125°
- CS-Q Countersinks 90°, Machining Center Use
- CS-QM Countersinks 90°and 60°, Drilling Machine Use
- CS-G Submarine Gate Cutter, 20°, 30°
- JOINT TOOLS
- JO-CES Joint- High Helix Center Drills-Type A 60°
- JO-CES V Joint- High Helix Center Drills-Type A 60°, Coated
- JO-CDS Joint- Low Helix Center Drills-Type A 60°
- JO-CDS V Joint- Low Helix Center Drills-Type A 60°, Coated
- JO-C-CDS Joint- Low Helix Carbide Center Drills-Type A 60°
- JO-CDS(II) Joint- Low Helix Center Drills-Type B 60°, (Old JIS Type 2 )
- JO-PEQ Joint- Point Drills 90°
- JO-PEQ V Joint- Point Drills 90°, Coated
- JO-C-PEQ V Joint- Carbide Point Drills 90°, Coated
- JO-NCSD V Joint- NC Starting Drills for Chamfering 90°, Coated
- JO-CSQM Joint- Countersinks 90°, Drilling Machine Use
- JO-HOLDERHolders for Joint Tools, for 150mm and for 200mm
- YAMAWA LINE-UPS ARRANGED ON SIZES
- Flowchart : M2 tapping
- M2 Taps
- M2 Dies
- Flowchart : M3 tapping
- M3 Taps
- M3 Dies
- Flowchart : M4 tapping
- M4 Taps
- M4 Dies
- Flowchart : M5 tapping
- M5 Taps
- M5 Dies
- Flowchart : M6 tapping
- M6 Taps
- M6 Dies
- Flowchart : M8 tapping
- M8 Taps
- M8 Dies
- Flowchart : M10 tapping
- M10 Taps
- M10 Dies
- Flowchart : M12 tapping
- M12 Taps
- M12 Dies
- M1-M8.5 Taps
- M1-M8.5 Dies
- M9-M24 Taps
- M9-M24 Dies
- M25-M48 Taps
- M25-M48 Dies
- M50-M100 Taps
- M50-M100 Dies
- For Unified threads Taps
- For Unified threads Dies
- For Whitworth threads Taps
- For Whitworth threads Dies
- For Screw threads usedon sewing machines Taps(SM)
- For Screw threads usedon sewing machines Dies(SM)
- For Pipe threads Taps
- For Pipe threads Dies
- For Americanpipe threads Taps
- For Americanpipe threads Dies
- For Miniaturethreads Taps
- For Miniaturethreads Dies
- PRAD system Solution tool
- Version of special tap manufacturing
- Version of recycling
- Specification corresponding with standard blanks(for Japanese market)
- Standard blank dimension table (for Japan)
- Specification corresponding with standard blanks(for Japanese market)
- Specification corresponding with standard blanks(DIN)
- Specification of corresponding standard blanks(for European market)
- Specification of corresponding standard blanks(for American market)Overall length : DIN, Shank dia. : ANSI
- YAMAWA Standard blank Line UP
- YAMAWA Standard Long shank blank Line UP
- Table for tap dimensions and type
- TECHNICAL INFORMATION
- 1.Terminology of Taps
- 2.Flutes
- 3.Edge angle and Cutting allowance of taps
- 4.Recommended Tapping Speeds
- 5.Tapping speed and Revolution Speed
- 6.Tapping Torque
- 7.Metric Thread and Gauge Pro le
- 8.Length of engagement
- 9.Classes of Internal Threads and Classes of Taps
- 10.About UNJ Threads
- 11.Class of external threads and class of Dies
- 12.Guide to Thread Forming Taps (Roll Taps)
- 13.How to set the tap's oversize to meet with the coatingmargin of internal threads
- 14.Tap, Thread Limits
- 15.Bored hole size before tapping ( for thread cutting )
- 16.Bored hole size before tapping ( for thread forming )
- 17.Bar diameter for external threads ( for cutting type dies )
- 18.Bar diameter of external threads (for thread rolling dies)
- 19.Surface Treatment
- 20.Carbide Taps
- 21.Taps for Pipe Threads
- 22.Features of MC-Helical Thread Mills
- 23.Selecting di erent tap holder combinations by machine feed system
- 24.The mechanism for a tap to cut oversize on an internal thread
- 25.Trouble Shooting
- 26.Center Drills
- 27.Table of recommend centering condition
- 28.Thread Series
- 29.Basic pro le of threads
- 30.List of Thread Standards and Nominal Diameter Ranges of YAMAWA Taps
- 31.Cross chart of thread cutting tool standard
- 32.Hardness conversion table
- 33.Conversion table from inch to millimeter
- 34.Chemical Component table of work materials
- 35.Materials used for Cutting Tools
- Searching table by product code
- Index of product symbols
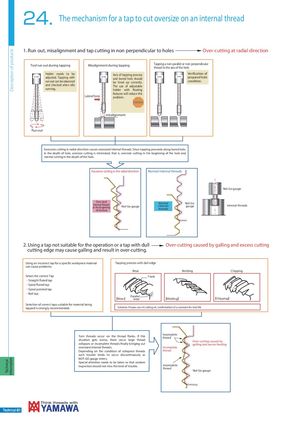
The mechanism for a tap to cut oversize on an internal thread 24. The mechanism for a tap to cut over size on an internal thread
1. Run out, misalignment and tap cutting in non perpendicular to holes Over-cutting at radial direction 3. Tapping with an improper feed condition over-cutting at axial direction
Tapping a non-parallel or non-perpendicular Process of over-cutting due to excessive feed Tool run out during tapping Misalignment during tapping thread to the axis of the hole.
| Holder needs to be | Verification of | With cutting edge b1, cutting starts. | |
| Axis of tapping process |
| holder | adjusted. Tapping with | holder | and bored hole should | holder | holder | prepared hole |
| run out can be observed | be lined up correctly. | condition. | ||||
| and checked when idle | The use of adjustable |
running. Workpiece Cutting part by b1
holder with floating features will reduce this Lateral force problem. Solutions
Not Go gauge Excessive-cutting of the thread
misalignment Tap with excessive feeding
Run out Position between workpiece and tap after the tap rotates 1 turn. Excessive cutting in radial direction causes oversized internal threads. Since tapping proceeds along bored hole, Distance of in the depth of hole, oversize cutting is minimized, that is, oversize cutting in the beginning of the hole and excess feeding normal cutting in the depth of the hole. Workpiece
Excessive-cutting in the radial direction Normal internal threads
Cutting trace by b1 Not Go gauge Tap Over sized Normal internal threads Not Go
Not Go gauge internal gauge internal threads
at the beginning threads of the bore Position between workpiece and tap after the tap rotates 2 turns.
Workpiece Distance of excess feeding
2. Using a tap not suitable for the operation or a tap with dull Over-cutting caused by galling and excess cutting
cutting edge may cause galling and result in over-cutting. Tap Using an incorrect tap for a specific workpiece material Tapping process with dull edge can cause problems
Wear Welding Chipping
Select the correct Tap Flank ・Straight fluted tap The position between workpiece and tap after 3 rotations of tap. ・Spiral fluted tap Over-cutting of the thread by ・Spiral pointed tap too slow feeding
・Roll tap Not Go gauge Parallel Process Opposite of excessive
【Wear】 wear 【Welding】 【Chipping】 Workpiece Distance of
excess feeding feeding Factors in fluencing extra Selection of correct taps suitable for material being material is cut at back frank. tapped is strongly recommended. Solution: Proper use of cutting oil, confirmation of a constant for tool life
over-cutting during tapping Tap Incomplete The tap mounting condition in the holder. Torn threads occur on the thread flanks. If this thread
| situation gets worse, there occur large thread | Over-cutting caused by | The condition of bored hole. |
| collapses or incomplete threads finally bringing out | galling and excess feeding | The cutting oil selection. |
| oversized internal threads. | Incomplete | Solutions | |
| Depending on the condition of collapsed threads | thread | Feed adjustment is strongly recommanded. | Incorrect adjustment of feed balance. |
| such trouble tends to occur discontinuously as | Selection of the tap depending on material | ||
| *(Use fully synchronous feed system and fixing holder) | |||
| NOT-GO gouge enters. | |||
| Special attention needs to be taken so that random | When using machines that do not have the | being cut. |
inspection should not miss this kind of trouble. Incomplete thread synchronous feed system, such as drilling machine. Technical Inf Not Go gauge *Adjust the correct weight balance of main spindle
properly. *Use an axial/radial floating holder for adjustment.