Общий каталог Palbit 2022 - страница 9
Навигация
 Общий каталог Palbit
- MILLING
- Milling tool selection
- Tools Overview
- Inserts Codification
- New grade PHH - PHP
- Inserts Overview
- Face Milling
- PLUS 28088
- PLUS 90260
- PLUS 90845
- PLUS 90945
- PLUS 91245
- LINEPRO 06045
- LINEPRO 09945
- LINEPRO 00036
- Hifeed Milling
- TETRAFEED 16320
- PENTA HIFEED 06320
- HIFEED 06410
- HIFEED 06690
- HIFEED 06815
- HIFEED 50560
- HIFEED 50060
- HIFEED 06590
- Shoulder Milling
- HEXAPLUS 49590
- PLUS 49090
- PLUS 17190
- PLUS 17590
- PLUS 18190
- LINEPRO 20090
- LINEPRO 20190
- LINEPRO 20290
- TGPLUS 90090
- TGPLUS 90190
- TGPLUS 90390
- ALUPRO 76090
- ALUPRO 77090
- ALUPRO 08390
- LINEPRO 06290
- LINEPRO 17090
- LINEPRO 18090
- Profile Milling
- W-PRO 62090
- BALLPRO 63090
- PLUS 49095
- PLUS 45095
- TOROMILL 33590 | 33690 | 33890 | 33990
- TOROMILL 33890|33990
- TURBOMILL 34190 | 34290
- TOROMILL X2 35190
- TOROMILL 24590|25090|25190
- TOROMILL 25290|25390
- LINEPRO 40095|40595|41095
- HARDMILL 72090
- CENTER & CHAMFER
- Spot face
- Spare Parts
- Procedures for clamping screws
- Technical Data
- Milling Grades
- Comparative Grades Chart
- Formulas & calculations
- Troubleshooting
- PCD Tipped End Mills
- Straight Flutes PCD
- Solide Carbide End Mills
- Selection Guide for Solid Carbide
- Troubleshooting
- DRILLING
- Drills Code Key
- Nomenclature
- Overview
- Jet Drills
- Integrex Drills
- Trepanning Drills
- Solid Carbide Drills
- ISO Driling inserts code key
- Inserts
- Spare Parts
- Technical Data
- TURNING
- New turning grades
- ISO Turning Code key
- Inserts Recomendation
- Negative Inserts Overview
- Positive Inserts Overview
- DOMX
- Negative inserts
- Positive inserts
- PCBN & PCD Inserts
- PCBN turning inserts
- PCD Inserts selection
- ISO PCD Inserts code key
- Single Tip
- Negative Inserts
- CNGA Z1
- DNGA Z1
- SNGA Z1
- TNGA Z1
- VNGA Z1
- Positive Inserts
- OVERVIEW
- CCGT Z1
- CCGW Z1
- CPGT Z1
- CPGW Z1
- DCGT Z1
- DCGW Z1
- SCGT Z1
- SCGW Z1
- VCGT Z1
- VCGW Z1
- TCGT Z1
- TCGW Z1
- TPGT Z1
- TPGW Z1
- Full Edge - Positive Inserts
- CCGT FR/FL
- CCGW FR/FL
- TCGT FL
- TCGW FL
- PCD recommended cutting data
- Heavy turning
- Bar Peeling
- Inserts code key
- Negative Inserts
- INGR-MP
- JNGF-MP
- LNGF-MP
- UNGF-MP
- TNMJ-MP
- TNGM-MP
- TNMM-LH
- XNMJ-MP
- XNMJ-MH
- XNGJ-RP
- Railway Turning
- Inserts code key
- Negative Inserts
- CNMM-HY
- CNMM-HZ
- SNMM-HY
- SNMM-HZ
- LNUX-RMM
- LNUX-RRM
- LNUX-RHR
- LNUX-RMM-T
- LNUX-RRM-T
- LNUX-RHR-T
- Positive Inserts
- RCMR-RR
- RCMX-ST
- RCMX-RM
- RCMX-RR
- Scarfing
- External Toolholders
- External toolholder code key
- Clamping System
- (C) Top Clamping Toolholders
- CKJN 93º
- CKNN 63º
- CSBP 75º
- CSDP 45º
- CSKP 75º
- CSSP 45º
- CSTP 60º
- CTBP 75º
- CTCP N 90º
- CTCP 90º
- CTDP 45º
- CTFP 90º
- CTGP 90º
- CTTP 60º
- (D) Dimple Lock Toolholders
- DCLN 95º
- DDJN 93º
- DSSN 45º
- DTGN 90º
- DWLN 95º
- (M) Wedge Clamp Toolholders
- MCLN 95º
- MSSN 45º
- MTEN 60º
- MTJN 93º
- MTNN 63º
- MWLN 95º
- (M-K) Double Lock Toolholders
- MCLN-K 95º
- MDJN-K 93º
- MSSN-K 45º
- MTJN-K 93º
- MVJN-K 93º
- MVQN-K 117º30’
- MVVN-K 72º30’
- MWLN-K 95º
- (P) Lever LockToolholders
- PCBN 75º
- PCFN 90º
- PCKN 75º
- PCLN 95º
- PCMN 50º
- PCSN 45º
- PDJN 93º
- PDNN 63º
- PRDC
- PRSC
- PRSN
- PSBN 75º
- PSDN 45º
- PSKN 75º
- PSSN 45º
- PTDN 45º
- PTFN 90º
- PTGN 90º
- PTTN 60º
- PWLN 95º
- (S) Center Screw Toolholders
- SCAC 90º
- SCLC 95º
- SDJC 93º
- SDNC 62º30’
- SRDC
- SSBC 75º
- SSDC 45º
- SSSC 45º
- STAC 90º
- STDC 45º
- STFC 90º
- STGC 90º
- STJC 93º
- STTC 60º
- SVHC 107º30’
- SVJB 93º
- SVJC 93º
- SVLC 95º
- SVVB 72º30’
- SVVC 72º30’
- SVXC 113º
- SVZC 100º
- Internal Toolholders
- Clamping System
- (C) Top Clamp Toolholders
- CKUN 93º
- CSKP 75º
- CTFP 90º
- CTUP 93º
- (D) Dimple Lock Toolholders
- DCLN 95º
- DDUN 93º
- (M) Wedge Clamp Toolholders
- MTUN 93º
- MWLN 95º
- (M-K) Double Lock Toolholders
- MCLN-K 95º
- MDUN-K 93º
- MSKN-K 75º
- MTFN 90º
- MTFN-K 90º
- MVUN-K 93º
- MWLN-K 95º
- (P) Lever Lock Toolholders
- PCKN 75º
- PCLN 95º
- A-PCLN 95º
- PDUN 93º
- A-PDUN 93º
- PDUN 93º-BT
- PSKN 75º
- A-PSKN 75º
- A-PSSN 45º
- PTFN 90º
- A-PTFN 90º
- PWLN 95º
- A-PWLN 95º
- (S) Center Screw Toolholders
- SCLC 95º
- A-SCLC 95º
- E-SCLC 95º
- SCLC N 95º
- SDQC 107º30’
- A-SDQC 107º30’
- SDUC 93º
- A-SDUC 93º
- E-SDUC 93º
- SDUC 93º-BT
- A-SDUC 93º-BT
- SSKC 75º
- A-SSSC 45º
- STFC 90º
- A-STFC 90º
- E-STFC 90º
- STUC 93º
- SVQC 107º30’
- A-SVQC 107º30’
- SVUB 93º
- SVUC 93º
- A-SVUC 93º
- A-SVJC 93
- Anti-vibrations Toolholders
- Internal Toolholders Set
- PK SCLC 95º
- PK SDQC 107º30’
- PK SDUC 93º
- PK STFC 90º
- Automatic Lathes
- Automatic Lathes code key
- Overview
- Center Screw System (S)
- SCAC 90º
- SCLC 95º
- SDAC 90º
- SDJC 93º
- SDNC 62º30’
- STJC 93º
- SVAC 90º
- SVJC 93º
- SVVC 72º30’
- Spare Parts
- CHIP BREAKERS
- CLAMPS (C HOLDERS)
- DIFFERENTIALS SCREWS
- LEVERS
- LEVER SCREWS
- LOCK PINS
- SCREWS (ALLEN)
- SCREWS (TORX)
- SHIM PIN PUNCHES
- SHIMS (T SHAPES)
- SHIMS (V SHAPES)
- SHIMS (W SHAPES)
- SHIMS (KNUX SHAPES)
- SPRINGS
- WEDGE CLAMPS (M HOLDERS)
- WEDGE CLAMPS (M-K HOLDERS)
- WRENCHES (ALLEN)
- WRENCHES (TORKS)
- Technical Data
- Turning Grades
- Comparative Grades Chart
- Comparative Chip-breaker Chart
- Chip-breaker Specifications
- Cutting Speed
- Selection Guide
- Troubleshooting
- Wiper Concept
- GROOVING & PARTING OFF
- Inserts Overview
- Grooving Plus
- Inserts code key
- GP Inserts
- Blades & Toolholders code key
- Grooving & Parting Off
- Inserts code key
- Inserts Overview
- Inserts GCMX
- Inserts SANCAR
- Blades code key
- Trigon inserts code key
- Flat grooving inserts
- Full radius grooving inserts
- External toolholder code key
- External toolholder
- Internal toolholder code key
- Internal toolholder
- SAL
- Inserts code key
- Toolholders code key
- Toolholders
- Inserts
- Technical data
- Light Grooving
- Forming Grooving
- Spare Parts
- Technical Data
- THREADING
- THREAD MILLING
- Inserts code key
- Inserts program
- iso
- un unc, unf, unef, uns
- whit bsw, bsf, bsp
- bspt
- npt
- nptf
- nps
- npsf
- pg din 40430
- unj
- american buttress
- acme
- Tooholders code key
- Multi insert toolholders
- Single insert toolholders
- wssn-1
- wssn-1 | Long shank
- ecsn-1 | Long carbide shank
- Double insert toolholders
- wssn-2
- Toolholders technical data
- Technical Data
- THREAD TURNING
- Threading - Step by Step Example
- Inserts Overview
- Partial Profile inserts
- Partial Profile code key
- Partial Profile 60º
- Partial profile 55º
- Full Profile inserts
- full profile inserts code key
- AMERICAN UN (UNC, UNF, UNEF) | ANSI B1.1-1982
- WITHWORTH FOR BSW, BSF, BSP, B.S.84: 1956, DIN 259, ISO 228-1:1994
- BSPT | B.S.21: 1985
- NPT | ANSI/ASME B 1.20.1-1983
- ROUND (DIN 405) | DIN 405:1997
- ROUND (DIN 20400) | DIN 20400:1990
- TRAPEZ | DIN 103:1977 | ISO 2901:1993
- AMERICAN ACME | ANSI/ASME: 1.5-1988
- UNJ | MIL-S-8879A
- UNJ | MIL-S-8879A
- AMERICAN BUTTRESS | ANSI B1.9-1973
- METRIC BUTTRESS SAGENGEWINDE (DIN 513:1985) SAW THREAD
- API | API SPEC 7:2001 (0.040 | 0.038r | 0.050)
- API | buttress casing | api spec 5b:2008 | oil threads
- API Round Casing & Tubing | API SPEC 5B:2008
- EXTREME LINE CASING | API SPEC 5B:2008 - OIL THREADS
- Tangencial profile inserts
- Tangencial profile code key
- TNMC (Tangencial Inserts)
- TPMC (Tangencial Inserts)
- External Toolholders
- External toolholders code key
- SXAN
- Internal Toolholders
- Internal toolholders code key
- STGN 90º
- SXFN
- Spare Parts
- Technical Data
- GENERAL TECHNICAL DATA
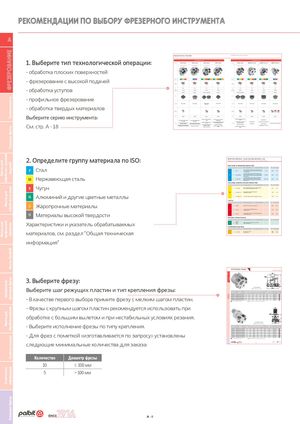
Рекомендации по выбору фрезерного инструмента
AA
milling tools overview Guia de ferramentas | Guía de herramientas
1. Выберите тип технологической операции: A FACE MILLING CUTTERS FACE MILLING CUTTERS A
| Program | plus 28088 | plus 90260 | plus 90845 | plus 90945 | Program | plus 91245 | linepro 06045 | linepro 09945 | linepro 00036 | ||
| Proprietary milling line | Proprietary milling line | Proprietary milling line | Proprietary milling line | Proprietary milling line | |||||||
| - обработка плоских поверхностей | |||||||||||
| - фрезерование с высокой подачей | Material | P M K | P K | P M K | N S P M | K N | S Material | P M K | P M K | N P M K | N P K |
| OperationMain | OperationMain | ||||||||||
| - обработка уступов | Facing | Shouldering Plunging Facing SlottingShouldering | CopyingPlungingFacing Side millingSlottingShouldering | InterpolationCopyingHelicalPlunging FacingSlanted Shoulder & ChamferSide millingSlottingShoulderingRamp downInterpolationCopyingHelicalPlunging Plunging &RecessingSlanted Shoulder & ChamferSide millingSlotting ProfilingRamp downInterpolationHelicalCopyingFacingPlunging &RecessingSlanted Shoulder & ChamferSide millingShouldering ProfilingRamp downInterpolationPlungingHelicalFacingPlunging &RecessingSlanted Shoulder & ChamferSlottingShouldering ProfilingRamp downCopyingPlungingFacingPlunging &RecessingSide millingSlottingShouldering ProfilingInterpolationCopyingHelicalPlunging FacingSlanted Shoulder & ChamferSide millingSlottingShoulderingRamp downInterpolationHelicalCopyingPlunging Plunging &RecessingSlanted Shoulder & ChamferSide millingSlotting | Profiling Plunging &Recessing ProfilingRamp down ProfilingRamp downInterpolationHelical Plunging &RecessingSlanted Shoulder & Chamfer ProfilingRamp downInterpolationHelicalCopying Plunging &RecessingSlanted Shoulder & ChamferSide milling | ||||||
| Krº | 88º | 60º | 45º | 45º | Krº | 45º | 45º | 45º | 36º | ||
| (ØDc - mm)Range | 50 - 200 | 50 - 160 | 32 - 250 | 50 - 250 | (ØDc - mm)Range | 63 - 250 | 50 - 160 | 50 - 250 | 66 - 160 | ||
| SN...1206... | PN…1105… | SN…1206… & ON…0505… | SN…1206… | SN…1606… & ON…0606… | SE…1204… | SE…13T3… | PD…1204… | ||||
| - профильное фрезерование | Insert | Insert | |||||||||
| - обработка твердых материалов | Couplings | Arbor mounting | Arbor mounting | Arbor mountingWeldon shank | Arbor mounting | Couplings | Arbor mounting | Arbor mounting | Arbor mounting | Arbour mounting | |
| OperationsOther | OperationsOther | ||||||||||
| Выберите серию инструмента: | Facing FacingShouldering ShoulderingPlunging PlungingSlotting Slotting CopyingFacing CopyingShoulderingSide milling Side millingPlungingInterpolationHelical InterpolationHelicalSlottingSlanted Shoulder & ChamferSlanted Shoulder & ChamferCopyingRamp down Ramp downSide millingPlunging &Recessing Plunging &RecessingInterpolationProfilingHelicalFacing ProfilingSlanted Shoulder & ChamferShouldering Ramp downPlunging | Plunging &RecessingSlotting Facing ProfilingCopyingShouldering Side millingPlunging | InterpolationHelicalSlotting FacingSlanted Shoulder & ChamferCopyingShoulderingRamp downSide millingPlunging Plunging &RecessingFacingFacingInterpolationHelicalSlottingShoulderingShoulderingProfilingSlanted Shoulder & ChamferCopyingPlungingPlungingRamp downSide millingSlottingFacingSlottingPlunging &RecessingShoulderingInterpolationHelicalCopyingCopying ProfilingSlanted Shoulder Plunging& ChamferSide millingSide millingRamp downSlottingInterpolationHelicalInterpolationHelicalPlunging &RecessingCopyingSlanted Shoulder Slanted Shoulder & Chamfer& ChamferProfilingSide millingRamp downRamp down InterpolationHelicalPlunging &RecessingPlunging &Recessing Slanted Shoulder & ChamferProfilingProfiling Ramp down | Plunging &Recessing Profiling | |||||||
| Page | PAG. 46 | PAG. 50 | PAG. 54 | PAG. 58 | Page | PAG. 62 | PAG. 66 | PAG. 68 | PAG. 72 | ||
| New line for Heavy and Soft face | Economical because double sided | Two different geometries for same pocket | Low cutting forces | ||||||||
| Indexable face mills with 8 helical cutting edges | Economical because double sided inserts applied | milling | inserts applied | ||||||||
| Two different geometries for same | Variety of insert geometries is available for all applications materials | Insert geometries available for all applications materials | Low cutting forces | Suitable for high-speed machining | |||||||
| См. стр. A - 18 | Features For rough to semi-finish with high-efficiency face milling | design for distribution of cutting forces 10 coners available improved insert | Features | Good chip flow | Excellent chip flow | High rake angle and low cutting forces | |||||
| Cutting edge angle enables performing | Insert geometries available for all applications materials | Excellent surface finishing | Excellent surface finishing | High rigidity due to carbide shim | |||||||
| face milling very close to the sidewall | Excellent solution for cast iron | Excellent surface finishing | Available in regular and fine pitch cutters | Available in regular and fine pictch |
cutters A - 12 A - 13
2. Определите группу материала по ISO:
WORKPIECE MATERIALS - PALBIT SELECTION MATERIALS, PSM
Material da peça - seleção de materiais Palbit, PSM | Material de la pieza - selección materiales Palbit, PSM
Стал Steel, Ferritic and Martensitic Stainless Steel
| P | ISO PSM Material Example | Description Rm(N/mm²) | (N/mm²)kcX | mc | |
| 1 Ck50 | Structural steels; ordinary carbon steels with low to medium carbon content(<0,5%C); soft carbon steel; | <500 | 1500 | 0.25 | |
| free cutting steel. | |||||
| P | Normal tool steels; harder steels for toughening; Martensitic stainless steels; Carbon steels with high | ||||
| Нержавеющая сталь | 2 42CrMnNiMo 4 | carbon content (>0,5%C); Ferritic and martensitic | 550<900 | 1900 | 0.24 |
| M | stainless steels.Normal tool steels; Harder steels for toughening; | ||||
| 3 X40CrMoV51 | Martensitic stainless steels; Difficult tool steels; High-alloy steels with high hardness; Martensitic | 900<1200 | 2000 | 0.24 | |
| stainless steels. | |||||
| Easy-cutting, Austenitic and Duplex Stainless Steel | |||||
| ЧугунK | ISO PSM Material Example | Description Rm(N/mm²) | (N/mm²)kcX | mc | |
| 4 X8CrNiS189 | Easy-cutting stainless steels; Free-cutting stainless steels; Calcium-treated stainless steels. | 1750 | 0.22 | ||
| Алюминий и другие цветные металлы | M 5 X2CrNiMo17122 | Moderately to difficult stainless steels:Austenitic and duplex. | 2050 | 0.20 | |
| N | |||||
| 6 X2CrNiMoN2253 | Very difficult stainless steels: Austenitic and duplex. | 2150 | 0.20 | ||
| Cast Iron | |||||
| Жаропрочные материалыS | ISO PSM Material Example | Description Rm(N/mm²) | (N/mm²)kcX | mc | |
| 7 GJL-150 | Medium / hard cast iron; Grey cast iron. | 1150 | 0.22 | ||
| K 8 GJL-250 | Low-alloy cast iron; Malleable cast iron; Nodular cast iron. | 1225 | 0.25 | ||
| Материалы высокой твердостиH | Difficult high-alloy cast iron; Difficult malleable cast | ||||
| 9 GJL-350 | iron; Nodular cast iron | 1470 | 0.30 | ||
| Aluminium and Non-Ferrouses | |||||
| Характеристики и указатель обрабатываемых | ISO PSM Material Example | Description Rm(N/mm²) | (N/mm²)kcX | mc | |
| N 10 AW7075AISi12 | Aluminium alloys: Low Si Aluminium alloys: | ||||
| CuZn37 | High Si Copper alloys | ||||
| Heat Resistent Super Alloys | |||||
| материалов, см. раздел “Общая техническая | ISO PSM Material Example | Description Rm(N/mm²) | (N/mm²)kcX | mc | |
| S 11 Inconel 718 | Ni-based super-alloysTitanium alloys | 33001450 | 0.240.23 |
Фрезы для профильной обрабоФрезы для профильной обрабо Please note that the Rm value is only for selection of the material group and when the material has been heat treatment or other methods that increase the strength of the material. информация” 727
3. Выберите фрезу: Выберите шаг режущих пластин и тип крепления фрезы: - В качестве первого выбора примите фрезу с мелким шагом пластин.
- Фрезы с крупным шагом пластин рекомендуется использовать при
обработке с большим вылетом и при нестабильных условиях резания. - Выберите исполнение фрезы по типу крепления.
- Для фрез с пометкой «изготавливается по запросу» установлены
следующие минимальные количества для заказа:
Количество Диаметр фрезы
10 ≤ 100 мм
5 > 100 мм
Техническая информацияТехническая информация
Tetrafeed 16320 NEW
Proprietary milling line
A
Arbor Mounting =20º | p=-7º | Rp=1,8
| Order code | Reference Referência | Dimensions | Dimensões | Dimensiones (mm) | Kg | Stock Specifications Insert | ||
| Código | Referencia | ØDc Ød | Ødg L | Ap max(mm) | ArborType | |
| 181152300 040A16320-07-07-016040 | 7 | 40 16 | 36 40 | 0,20 | 1,00 A XNKU 06… | |
| 181157500 050A16320-06-07-022040 | 6 | 50 22 | 42 40 | 0,25 | 1,00 A XNKU 06… | |
| 181152400 050A16320-08-07-022040 | 8 | 50 22 | 42 40 | 0,29 | 1,00 A XNKU 06… | |
| 181152500 052A16320-08-07-022040 | 8 | 52 22 | 40 40 | 0,39 | 1,00 A XNKU 06… | |
| 181152600 063A16320-09-07-022040 | 9 | 63 22 | 48 40 | 0,50 | 1,00 A XNKU 06… |
Stock item | Produto de stock | Itens de stock Available under request | Disponível sobre consulta | Disponible bajo consulta
Threaded Coupling =20º | p=-7º | Rp=1,8
| Order code | ReferênciaReference | Dimensions | Dimensões | Dimensiones (mm) | Kg Specifications | Stock Insert | ||
| Código | Referencia | ØDc | ØM Ødg | L | Ap max(mm) | |
| 181151300 016R16320-02-07-M08025 | 2 | 16 M08 | 13 | 25 0,02 | 1,00 | XNKU 06… |
| 181151400 020R16320-03-07-M10028 | 3 | 20 | M10 18 | 28 0,05 | 1,00 | XNKU 06… |
| 181151500 025R16320-04-07-M12030 | 4 | 25 | M12 18 | 30 0,07 | 1,00 | XNKU 06… |
| 181148000 032R16320-05-07-M16035 | 5 | 32 | M16 29 | 35 0,16 | 1,00 | XNKU 06… |
| 181151600 035R16320-06-07-M16035 | 6 | 35 | M16 29 | 35 0,17 | 1,00 | XNKU 06… |
| 181151700 040R16320-05-07-M16045 | 5 | 40 | M16 29 | 45 0,24 | 1,00 | XNKU 06… |
| 181151800 042R16320-07-07-M16035 | 7 | 42 | M16 29 | 35 0,24 | 1,00 | XNKU 06… |
| Stock item | Produto de stock | Itens de stock | Available under request | Disponível sobre consulta | Disponible bajo consulta | |||||
| A - 84 | Technical Datapage A -238 page A-230 |
TOOLING SOLUTIONS EXPERTS