Каталог Sumitomo резьбонарезной инструмент - страница 6
Навигация
 Каталог Sumitomo фрезы со сменными пластинами
 Каталог Sumitomo пластины с кубическим нитридом бора Sumiboron
 Каталог Sumitomo инструмент для обработки канавок
 Общий каталог Sumitomo 2018 - 2019
 Каталог Sumitomo твердосплавные заготовки
 Каталог Sumitomo модульные системы для револьверных головок токарных станков
- F001
- F002
- F003
- F004
- F005
- F006
- F007
- F008
- F009
- F010
- F011
- F012
- F013
- F014
- F015
- F016
- F017
- F018
- F019
- F020
- F021
- F022
- F023
- F024
- F025
- F026
- F027
- F028
- F029
- F030
- F031
- F032
- F033
- F034
- F035
- F036
- F037
- F038
- F039
- F040
- F041
- F042
- F043
- F044
- F045
- F046
- F047
- F048
- F049
- F050
- F051
- F052
- F053
- F054
- F055
- F056
- F057
- F058
- F059
- F060
- F061
- F062
- F063
- F064
- F065
- F066
- F067
- F068
- F069
- F070
- F071
- F072
- F073
- F074
- F075
- F076
- F077
- F078
- F079
- F080
- F081
- F082
- F083
- F084
- F085
- F086
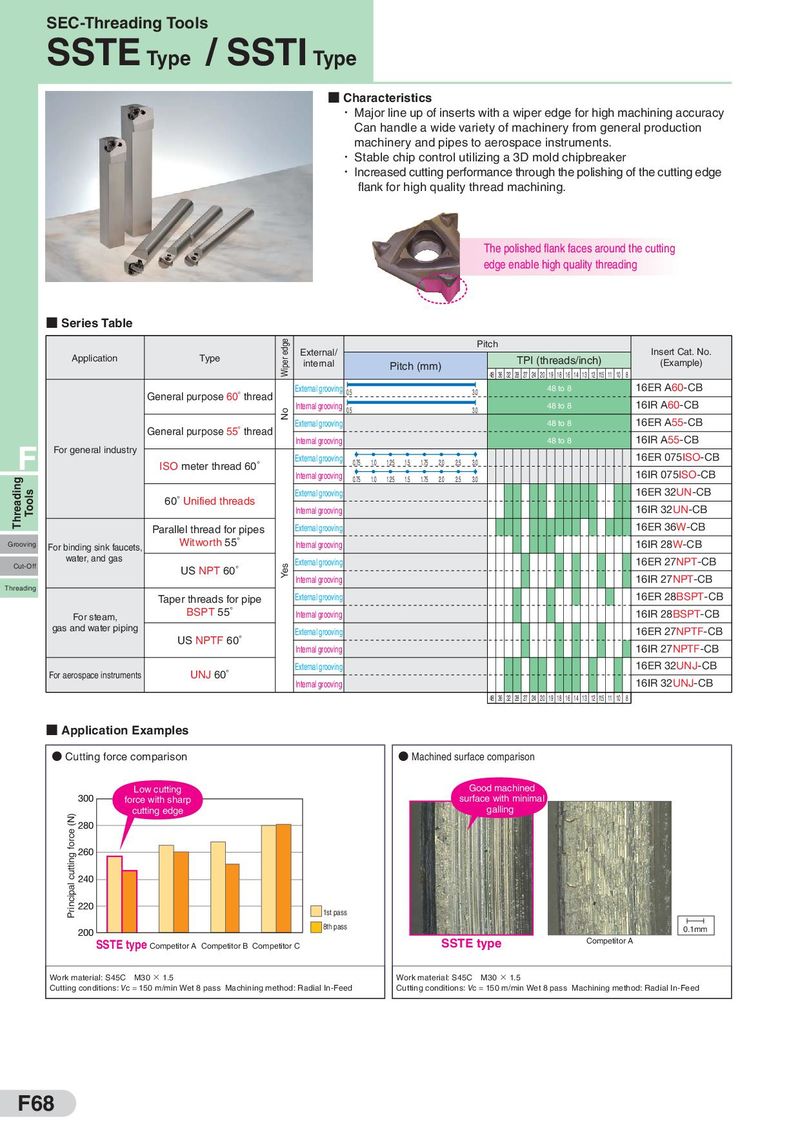
- Characteristics
- Major line up of inserts with a wiper edge for high machining accuracy
Can handle a wide variety of machinery from general production
machinery and pipes to aerospace instruments.
- Stable chip control utilizing a 3D mold chipbreaker
- Increased cutting performance through the polishing of the cutting edge flank for high quality thread machining.
The polished flank faces around the cutting
edge enable high quality threading
- Series Table
Pitch External/ Insert Cat. No.
Application Type TPI (threads/inch)
| internal | Pitch (mm) | (Example) | |
| 48 36 32 28 27 24 20 19 18 16 14 13 12 11.5 11 10 8 |
External grooving 48 to 8 16ER A60-CB
General purpose 60° thread 0.5 3.0
| Internal grooving | 48 to 8 | 16IR A60-CB |
| 3.0 0.5 | ||
| External grooving | 48 to 8 | 16ER A55-CB |
| General purpose 55° thread | ||
| F Internal grooving | 48 to 8 | 16IR A55-CB |
| For general industry | ||
| External grooving | 16ER 075ISO-CB |
| ISO meter thread 60° | 0.75 | 1.0 | 1.25 | 1.5 | 1.75 | 2.0 | 2.5 | 3.0 | ||
| Internal grooving | 16IR 075ISO-CB | |||||||||
| 0.75 | 1.0 | 1.25 | 1.5 | 1.75 | 2.0 | 2.5 | 3.0 | |||
| External grooving | 16ER 32UN-CB | |||||||||
| 60°Unified threads | ||||||||||
| Internal grooving | 16IR 32UN-CB |
| Parallel thread for pipes | External grooving | 16ER 36W-CB | |
| Witworth 55° | |||
| Grooving | For binding sink faucets, | Internal grooving | 16IR 28W-CB |
| water, and gas | External grooving | 16ER 27NPT-CB | |
| Cut-Off | US NPT 60° | ||
| Internal grooving | 16IR 27NPT-CB | ||
| Threading | |||
| Taper threads for pipe | External grooving | 16ER 28BSPT-CB | |
| BSPT 55° | |||
| For steam, | Internal grooving | 16IR 28BSPT-CB | |
| gas and water piping | External grooving | 16ER 27NPTF-CB |
US NPTF 60° Internal grooving 16IR 27NPTF-CB External grooving 16ER 32UNJ-CB For aerospace instruments UNJ 60°
Internal grooving 16IR 32UNJ-CB 48 36 32 28 27 24 20 19 18 16 14 13 12 11.5 11 10 8
- Application Examples
- Cutting force comparison
- Machined surface comparison
Low cutting Good machined
300 force with sharp surface with minimal
cutting edge galling 280
260
240
220 1st pass 8th pass 0.1mm 200
| SSTE type | SSTE type | Competitor A | |
| Competitor A Competitor B Competitor C |
Work material: S45C M30 × 1.5 Work material: S45C M30 × 1.5
Cutting conditions: Vc = 150 m/min Wet 8 pass Machining method: Radial In-Feed Cutting conditions: Vc = 150 m/min Wet 8 pass Machining method: Radial In-Feed