Общий каталог Mitsubishi 2020 - 2021 - страница 982
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
CARBIDE
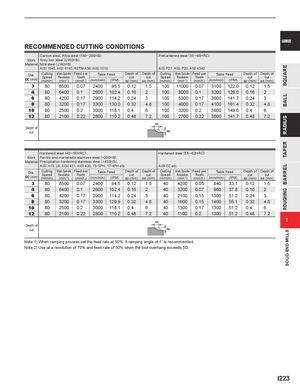
RECOMMENDED CUTTING CONDITIONS
| Work Material | Carbon s Alloy tool Mild steel AISI 1045 | teel, Alloy s steel(≤350 (≤180HB) , AISI 4140 | teel(180─ HB), , ASTM A3 | 280HB), 6, AISI 101 | 0 | Preharde AISI P21, | ned steel(3 AISI P20, A | 5─45HRC ISI 4340 | ) | |||||
| Dia. | Cutting Speed | Main Spindle Revolution | Feed per Tooth | Table | Feed | Depth of cut | Depth of cut | Cutting Speed | Main Spindle Revolution | Feed per Tooth | Table | Feed | Depth of cut | Depth of cut |
| DC(mm) | (m/min) | (min-1) | (mm/t.) | (mm/min) | (IPM) | ap (mm) | ae(mm) | (m/min) | (min-1) | (mm/t.) | (mm/min) | (IPM) | ap (mm) | ae(mm) |
| 3 | 80 | 8500 | 0.07 | 2400 | 95.5 | 0.12 | 1.5 | 100 | 11000 | 0.07 | 3100 | 122.0 | 0.12 | 1.5 |
| 4 | 80 | 6400 | 0.1 | 2600 | 102.4 | 0.16 | 2 | 100 | 8000 | 0.1 | 3200 | 126.0 | 0.16 | 2 |
| 6 | 80 | 4200 | 0.17 | 2900 | 114.2 | 0.24 | 3 | 100 | 5300 | 0.17 | 3600 | 141.7 | 0.24 | 3 |
| 8 | 80 | 3200 | 0.17 | 3300 | 130.0 | 0.32 | 4.8 | 100 | 4000 | 0.17 | 4100 | 161.4 | 0.32 | 4.8 |
| 10 | 80 | 2500 | 0.2 | 3000 | 118.1 | 0.4 | 6 | 100 | 3200 | 0.2 | 3800 | 149.6 | 0.4 | 6 |
| 12 | 80 | 2100 | 0.22 | 2800 | 110.2 | 0.48 | 7.2 | 100 | 2700 | 0.22 | 3600 | 141.7 | 0.48 | 7.2 |
| Depth of cut | a | e |
| Work Material | Hardened Ferritic a Precipitat AISI H13, | steel(40─ nd martensi ion hardeni L6, AISI 43 | 55HRC), tic stainles ng stainles 1, AISI 42 | s steel(>2 s steel( 0, 15-5PH, | 00HB), 50HB), 17-4PH et | c. | Hardene AISI D2 e | d steel(55─ tc. | 62HRC) | |||||
| Dia. | Cutting Speed | Main Spindle Revolution | Feed per Tooth | Table | Feed | Depth of cut | Depth of cut | Cutting Speed | Main Spindle Revolution | Feed per Tooth | Table | Feed | Depth of cut | Depth of cut |
| DC(mm) | (m/min) | (min-1) | (mm/t.) | (mm/min) | (IPM) | ap (mm) | ae(mm) | (m/min) | (min-1) | (mm/t.) | (mm/min) | (IPM) | ap (mm) | ae(mm) |
| 3 | 80 | 8500 | 0.07 | 2400 | 94.5 | 0.12 | 1.5 | 40 | 4200 | 0.05 | 840 | 33.1 | 0.12 | 1.5 |
| 4 | 80 | 6400 | 0.1 | 2600 | 102.4 | 0.16 | 2 | 40 | 3200 | 0.07 | 960 | 37.8 | 0.16 | 2 |
| 6 | 80 | 4200 | 0.17 | 2900 | 114.2 | 0.24 | 3 | 40 | 2100 | 0.15 | 1300 | 51.2 | 0.24 | 3 |
| 8 | 80 | 3200 | 0.17 | 3300 | 129.9 | 0.32 | 4.8 | 40 | 1600 | 0.15 | 1400 | 55.1 | 0.32 | 4.8 |
| 10 | 80 | 2500 | 0.2 | 3000 | 118.1 | 0.4 | 6 | 40 | 1300 | 0.17 | 1300 | 51.2 | 0.4 | 6 |
| 12 | 80 | 2100 | 0.22 | 2800 | 110.2 | 0.48 | 7.2 | 40 | 1100 | 0.2 | 1300 | 51.2 | 0.48 | 7.2 |
| Depth of cut | a | e |
I
Note 1) When ramping process set the feed rate at 50%. A ramping angle of 1˚ is recommended. Note 2) Use at a revolution of 70% and feed rate of 50% when the tool overhang exceeds 5D.