Общий каталог Mitsubishi 2020 - 2021 - страница 980
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
CARBIDE
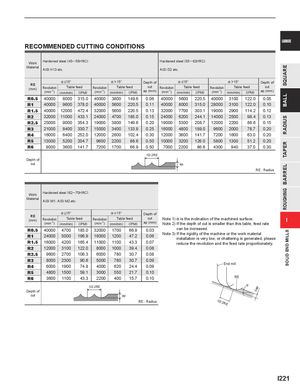
RECOMMENDED CUTTING CONDITIONS
| Work Material | Hardened AISI H13 | steel(45─ etc. | 55HRC) | Hardened AISI D2 e | steel(55─ tc. | 62HRC) | ||||||||
| RE | %≤15° | %>15° | Depth of | %≤15° | %>15° | Depth of | ||||||||
| (mm) | Revolution | Table | feed | Revolution | Table | feed | cut | Revolution | Table | feed | Revolution | Table | feed | cut |
| (min-1) | (mm/min) | (IPM) | (min-1) | (mm/min) | (IPM) | ap (mm) | (min-1) | (mm/min) | (IPM) | (min-1) | (mm/min) | (IPM) | ap (mm) | |
| R0.5 | 40000 | 8000 | 315.0 | 40000 | 3800 | 149.6 | 0.06 | 40000 | 5600 | 220.5 | 40000 | 3100 | 122.0 | 0.05 |
| R1 | 40000 | 9600 | 378.0 | 40000 | 5600 | 220.5 | 0.11 | 40000 | 8000 | 315.0 | 28000 | 3100 | 122.0 | 0.10 |
| R1.5 | 40000 | 12000 | 472.4 | 32000 | 5600 | 220.5 | 0.13 | 32000 | 7700 | 303.1 | 19000 | 2900 | 114.2 | 0.12 |
| R2 | 32000 | 11000 | 433.1 | 24000 | 4700 | 185.0 | 0.15 | 24000 | 6200 | 244.1 | 14000 | 2500 | 98.4 | 0.13 |
| R2.5 | 25000 | 9000 | 354.3 | 19000 | 3800 | 149.6 | 0.20 | 19000 | 5300 | 208.7 | 12000 | 2200 | 86.6 | 0.15 |
| R3 | 21000 | 8400 | 330.7 | 15000 | 3400 | 133.9 | 0.25 | 16000 | 4800 | 189.0 | 9600 | 2000 | 78.7 | 0.20 |
| R4 | 16000 | 6400 | 252.0 | 12000 | 2600 | 102.4 | 0.30 | 12000 | 3600 | 141.7 | 7200 | 1600 | 63.0 | 0.20 |
| R5 | 13000 | 5200 | 204.7 | 9600 | 2200 | 86.6 | 0.50 | 10000 | 3200 | 126.0 | 5800 | 1300 | 51.2 | 0.20 |
| R6 | 9000 | 3600 | 141.7 | 7200 | 1700 | 66.9 | 0.50 | 7000 | 2200 | 86.6 | 4300 | 940 | 37.0 | 0.30 |
| Depth of cut | ap |
RE : Radius
Hardened steel (62─ 70HRC) Work Material AISI W1, AISI M2 etc.
| % ≤15° | % >15° | Depth of | |
| RE |
(mm) Revolution Table feed Revolution Table feed cut Note 1) % is the inclination of the machined surface. I
| (min-1) | (mm/min) | (IPM) | (min -1) | (mm/min) | (IPM) | ap (mm) | Note 2) If the depth of cut is smaller than this table, feed rate | |
| R0.5 | 40000 | 4700 | 185.0 32000 | 1700 | 66.9 | 0.03 | can be increased. | |
| 24000 | 5000 | 196.9 16000 | 1200 | 47.2 | 0.06 | Note 3) If the rigidity of the machine or the work material | ||
| R1 | ||||||||
| installation is very low, or chattering is generated, please | ||||||||
| R1.5 | 16000 | 4200 | 165.4 11000 | 1100 | 43.3 | 0.07 | reduce the revolution and the feed rate proportionately. | |
| R2 | 12000 | 3100 | 122.0 | 8000 | 1000 | 39.4 | 0.08 | |
| R2.5 | 9600 | 2700 | 106.3 | 6000 | 780 | 30.7 | 0.08 | |
| R3 | 8000 | 2300 | 90.6 | 5000 | 780 | 30.7 | 0.09 | |
| R4 | 6000 | 1900 | 74.8 | 4000 | 620 | 24.4 | 0.09 | End mill |
| R5 | 4800 | 1500 | 59.1 | 3000 | 550 | 21.7 | 0.10 | |
| R6 | 3600 | 1100 | 43.3 | 2200 | 400 | 15.7 | 0.10 | RE |
0.2RE % < ap Depth of < cut ap
RE : Radius <0.2RE