Общий каталог Mitsubishi 2020 - 2021 - страница 961
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
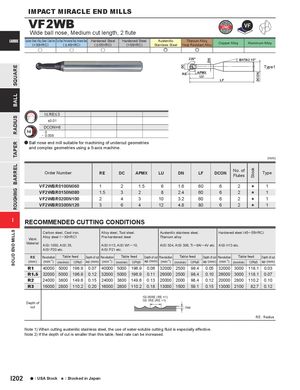
VF2WB
Wide ball nose, Medium cut length, 2 flute
CARBIDE Carbon Steel, Alloy Steel, Cast Iron Tool Steel, Pre-Hardened Steel, Hardened Steel Hardened Steel Hardened Steel Austenitic Titanium Alloy,
| (<30HRC) | ( | 45HRC) | ( | 55HRC) | (>55HRC) | Stainless Steel | Heat Resistant Alloy | Copper Alloy | Aluminum Alloy | |||
| u | u | u | e | e |
220° BHTA2 15° Type1 RE APMX LU
LF
| I ±0.01 |
| DCON=6 0 - 0.008 |
a Ball nose end mill suitable for machining of undercut geometries and complex geometries using a 5-axis machine. (mm)
| Order Number | RE | DC | APMX | LU | DN | LF | DCON | No. of Flutes | Stock | Type |
| VF2WBR0100N060 | 1 | 2 | 1.5 | 6 | 1.6 | 60 | 6 | 2 | s | 1 |
| VF2WBR0150N080 | 1.5 | 3 | 2 | 8 | 2.4 | 60 | 6 | 2 | s | 1 |
| VF2WBR0200N100 | 2 | 4 | 3 | 10 | 3.2 | 60 | 6 | 2 | s | 1 |
| VF2WBR0300N120 | 3 | 6 | 4 | 12 | 4.8 | 80 | 6 | 2 | s | 1 |
I RECOMMENDED CUTTING CONDITIONS
| Work Material | Carbon s Alloy ste AISI 105 AISI P20 | teel, Cas el (─30H 0, AISI 35 etc. | t iron, RC) , | Alloy ste Pre-hard AISI H13 AISI P21 | el, Tool st ened ste , AISI W1 etc. | eel, el ─10, | Austeniti Titanium AISI 304 | c stainless alloy , AISI 306 | steel, , Ti─6Al | ─4V etc. | Hardene AISI H13 | d steel (4 etc. | 5─55HR | C) | ||
| RE | Revolution | Table | feed | Depth of cut | Revolution | Table | feed | Depth of cut | Revolution | Table | feed | Depth of cut | Revolution | Table | feed | Depth of cut |
| (mm) | (min-1) | (mm/min) | (IPM) | ap (mm) | (min-1) | (mm/min) | (IPM) | ap (mm) | (min-1) | (mm/min) | (IPM) | ap (mm) | (min-1) | (mm/min) | (IPM) | ap (mm) |
| R1 | 40000 | 5000 | 196.9 | 0.07 | 40000 | 5000 | 196.9 | 0.06 | 32000 | 2500 | 98.4 | 0.05 | 32000 | 3000 | 118.1 | 0.03 |
| R1.5 | 32000 | 5000 | 196.9 | 0.12 | 32000 | 5000 | 196.9 | 0.11 | 26000 | 2500 | 98.4 | 0.10 | 26000 | 3000 | 118.1 | 0.07 |
| R2 | 24000 | 3800 | 149.6 | 0.15 | 24000 | 3800 | 149.6 | 0.13 | 20000 | 2000 | 98.4 | 0.12 | 20000 | 2800 | 110.2 | 0.10 |
| R3 | 16000 | 2800 | 110.2 | 0.20 | 16000 | 2800 | 110.2 | 0.18 | 13000 | 1500 | 59.1 | 0.15 | 13000 | 2100 | 82.7 | 0.12 |
| Depth of cut | RE =1) E >1) | p |
RE : Radius Note 1) When cutting austenitic stainless steel, the use of water-soluble cutting fluid is especially effective. Note 2) If the depth of cut is smaller than this table, feed rate can be increased.