Общий каталог Mitsubishi 2020 - 2021 - страница 940
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
CARBIDE
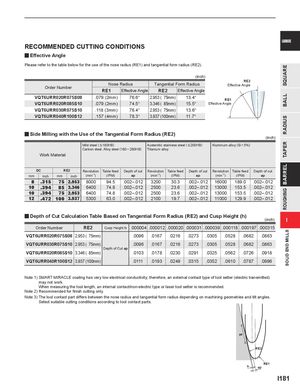
RECOMMENDED CUTTING CONDITIONS
y Effective Angle
Please refer to the table below for the use of the nose radius (RE1) and tangential form radius (RE2).
| (inch) | ||||||
| RE2 | ||||||
| Nose | Radius Tan | gential | Form Radius | Effe | fctive Angle | |
| Order Number | RE1 | R Effective Angle | E2 | Effective Angle | ||
| VQT6URR020R075S08 | .079 (2mm) | 76.6° 2.953 ( | 75mm) | 13.4° | RE1 | |
| VQT6URR020R085S10 | .079 (2mm) | 74.5° 3.346 ( | 85mm) | 15.5° | Effective Angle | |
| VQT6URR030R075S10 | .118 (3mm) | 76.4° 2.953 ( | 75mm) | 13.6° | ||
| VQT6URR040R100S12 | .157(4mm) | 78.3° 3.937( | 100mm) | 11.7° |
y Side Milling with the Use of the Tangential Form Radius (RE2)
(inch)
| Work M | aterial | Mild steel ( Carbon stee | l, Alloy steel ( | 180─280HB) | Austenitic s Titanium all | tainless steel oy | ( | Aluminum a | lloy (Si˂5%) | |||
| D mm | C inch | R mm | E2 inch | Revolution (min-1) | Table feed (IPM) | Depth of cut ap | Revolution (min-1) | Table feed (IPM) | Depth of cut ap | Revolution (min-1) | Table feed (IPM) | Depth of cut ap |
| 8 | .315 | 75 | 2.953 | 8000 | 94.5 | .002–.012 | 3200 | 30.3 | .002–.012 | 16000 | 189.0 | .002–.012 |
| 10 | .394 | 85 | 3.346 | 6400 | 74.8 | .002–.012 | 2500 | 23.6 | .002–.012 | 13000 | 153.5 | .002–.012 |
| 10 | .394 | 75 | 2.953 | 6400 | 74.8 | .002–.012 | 2500 | 23.6 | .002–.012 | 13000 | 153.5 | .002–.012 |
| 12 | .472 | 100 | 3.937 | 5300 | 63.0 | .002–.012 | 2100 | 19.7 | .002–.012 | 11000 | 129.9 | .002–.012 |
y Depth of Cut Calculation Table Based on Tangential Form Radius (RE2) and Cusp Height (h)
| (inch) | ||||||||||
| Order Number | RE2 | Cusp Heighth | .000004 | .000012 | .000020 | .000031 | .000039 | .000118 | .000197 | .000315 |
| VQT6URR020R075S08 | 2.953 ( 75mm) | .0096 | .0167 | .0216 | .0273 | .0305 | .0528 | .0682 | .0863 | |
| VQT6URR030R075S10 | 2.953 ( 75mm) | Deth of Cuta | .0096 | .0167 | .0216 | .0273 | .0305 | .0528 | .0682 | .0863 |
| VQT6URR020R085S10 | 3.346 ( 85mm) | pp | .0103 | .0178 | .0230 | .0291 | .0325 | .0562 | .0726 | .0918 |
| VQT6URR040R100S12 | 3.937 (100mm) | .0111 | .0193 | .0249 | .0315 | .0352 | .0610 | .0787 | .0996 |
Note 1) SMART MIRACLE coating has very low electrical conductivity; therefore, an external contact type of tool setter (electric transmitted) may not work. When measuring the tool length, an internal contact/non-electric type or laser tool setter is recommended. Note 2) Recommended for finish cutting only. Note 3) The tool contact part differs between the nose radius and tangential form radius depending on machining geometries and tilt angles. Select suitable cutting conditions according to tool contact parts.
ae
RE2
RE1 h ap