Общий каталог Mitsubishi 2020 - 2021 - страница 938
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
CARBIDE
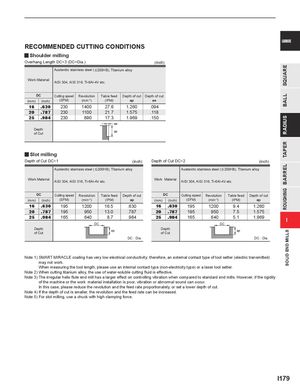
RECOMMENDED CUTTING CONDITIONS
y Shoulder milling
| Work Overha | Material ng Leng | Austenitic stai AISI 304, AISI th DC×3 (DC= | nless steel (< 316, Ti-6Al-4V Dia.) | 200HB), Titani etc. | um alloy | (inch) |
| D (mm) | C (inch) | Cutting speed (SFM) | Revolution (min-1) | Table feed (IPM) | Depth of cut ap | Depth of cut ae |
| 16 | .630 | 230 | 1400 | 27.6 | 1.260 | .094 |
| 20 | .787 | 230 | 1100 | 21.7 | 1.575 | .118 |
| 25 | .984 | 230 | 890 | 17.3 | 1.969 | .150 |
| De of | pth Cut | ae ap |
y Slot milling
| epth o | f Cut DC | ×1 | (inch) | Depth o | f Cut DC | ×2 | (inch) | ||||
| Austenitic stain | less steel ( | 200HB), Titani | um alloy | Austenitic stai | nless steel ( | 200HB), Titani | um alloy | ||||
| Work | Material | AISI 304, AISI | 316, Ti-6Al-4V | etc. | Work | Material | AISI 304, AISI | 316, Ti-6Al-4V | etc. | ||
| D (mm) | C (inch) | Cutting speed (SFM) | Revolution (min-1) | Table feed (IPM) | Depth of cut ap | D (mm) | C (inch) | Cutting speed (SFM) | Revolution (min-1) | Table feed (IPM) | Depth of cut ap |
| 16 | .630 | 195 | 1200 | 16.5 | .630 | 16 | .630 | 195 | 1200 | 9.4 | 1.260 |
| 20 | .787 | 195 | 950 | 13.0 | .787 | 20 | .787 | 195 | 950 | 7.5 | 1.575 |
| 25 | .984 | 165 | 640 | 8.7 | .984 | 25 | .984 | 165 | 640 | 5.1 | 1.969 |
| De of | pth Cut | DC | ap | DC : Dia. | De of | pth Cut | DC | ap | DC : Dia. |
Note 1) SMART MIRACLE coating has very low electrical conductivity; therefore, an external contact type of tool setter (electric transmitted) may not work. When measuring the tool length, please use an internal contact type (non-electricity type) or a laser tool setter. Note 2) When cutting titanium alloy, the use of water-soluble cutting fluid is effective. Note 3) The irregular helix flute end mill has a larger effect on controlling vibration when compared to standard end mills. However, if the rigidity of the machine or the work material installation is poor, vibration or abnormal sound can occur. In this case, please reduce the revolution and the feed rate proportionately, or set a lower depth of cut. Note 4) If the depth of cut is smaller, the revolution and the feed rate can be increased. Note 5) For slot milling, use a chuck with high clamping force.