Общий каталог Mitsubishi 2020 - 2021 - страница 936
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
VQ6MHVCH VQ6MHVRBCH
End mill, Medium cut length, 6 flute, Irregular helix flutes, With multiple thru-coolant Corner radius, Medium cut length, 6 flute, Irregular helix flutes, With multiple thru-coolant CARBIDE
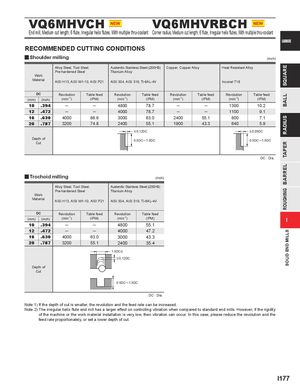
RECOMMENDED CUTTING CONDITIONS
y Shoulder milling
(inch)
| W Ma | ork terial | Alloy Steel, Tool Pre-hardened St AISI H13, AISI W | Steel, eel 1-10, AISI P21 | Austenitic Stainless Steel(≤200HB) Titanium Alloy AISI 304, AISI 316, Ti-6AL-4V | Copper, Copper | Alloy | Heat Resistant Inconel 718 | Alloy |
| D (mm) | C (inch) | Revolution (min-1) | Table feed (IPM) | Revolution (min-1) Table feed (IPM) | Revolution (min-1) | Table feed (IPM) | Revolution (min-1) | Table feed (IPM) |
| 10 | .394 | ─ | ─ | 4800 78.7 | ─ | ─ | 1300 | 10.2 |
| 12 | .472 | ─ | ─ | 4000 78.7 | ─ | ─ | 1100 | 9.1 |
| 16 | .630 | 4000 | 86.6 | 3000 63.0 | 2400 | 55.1 | 800 | 7.1 |
| 20 | .787 | 3200 | 74.8 | 2400 55.1 | 1900 | 43.3 | 640 | 5.9 |
| Dep C | th of ut | 0.5DC─1.5DC | 0.5DC─1.5DC |
DC : Dia.
| Tro | choid | milling | (inch) | ||
| W Mat | ork erial | Alloy Steel, Tool Pre-hardened St AISI H13, AISI W | Steel, eel 1-10, AISI P21 | Austenitic Stainles Titanium Alloy AISI 304, AISI 31 | s Steel(≤200HB) 6, Ti-6AL-4V |
| D (mm) | C (inch) | Revolution (min-1) | Table feed (IPM) | Revolution (min-1) | Table feed (IPM) |
| 10 | .394 | ─ | ─ | 4800 | 55.1 |
| 12 | .472 | ─ | ─ | 4000 | 47.2 |
| 16 | .630 | 4000 | 63.0 | 3000 | 43.3 |
| 20 | .787 | 3200 | 55.1 | 2400 | 35.4 |
| Dep C | th of ut | 0.5DC─1.5D 1.5DC | C |
DC : Dia. Note 1) If the depth of cut is smaller, the revolution and the feed rate can be increased. Note 2) The irregular helix flute end mill has a larger effect on controlling vibration when compared to standard end mills. However, if the rigidity of the machine or the work material installation is very low, then vibration can occur. In this case, please reduce the revolution and the feed rate proportionately, or set a lower depth of cut.