Общий каталог Mitsubishi 2020 - 2021 - страница 920
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
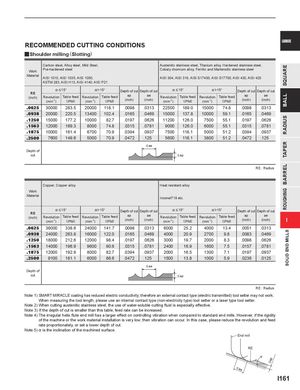
RECOMMENDED CUTTING CONDITIONS CARBIDE
y Shoulder milling (Slotting)
| Work Material | Carbon stee Pre-hardene AISI 1010, A ASTM 283, | l, Alloy steel, d steel ISI 1035, AI AISI H13, AI | Mild Steel, SI 1050, SI 4140, AISI | P21 | Austenitic s Cobaly cho AISI 304, A | teinless steel mium alloy, F ISI 316, AISI | , Titanium al erritic and M S17400, AIS | loy, Hardene artensitic sta I S17700, AI | d stainless s inless steel SI 430, AISI | teel, 420 | ||
| RE | % | 15° | %> | 15° | Depth of cut | Depth of cut | % | 15° | %> | 15° | Depth of cut | Depth of cut |
| (inch) | Revolution (min-1) | Table feed (IPM) | Revolution (min-1) | Table feed (IPM) | ap (inch) | ae (inch) | Revolution (min-1) | Table feed (IPM) | Revolution (min-1) | Table feed (IPM) | ap (inch) | ae (inch) |
| .0625 | 30000 | 283.5 | 20000 | 118.1 | .0098 | .0313 | 22500 | 189.0 | 15000 | 74.8 | .0098 | .0313 |
| .0938 | 20000 | 220.5 | 13400 | 102.4 | .0165 | .0469 | 15000 | 137.8 | 10000 | 59.1 | .0165 | .0469 |
| .1250 | 15000 | 177.2 | 10000 | 82.7 | .0197 | .0626 | 11200 | 126.0 | 7500 | 55.1 | .0197 | .0626 |
| .1563 | 12000 | 169.3 | 8000 | 74.8 | .0315 | .0781 | 9000 | 126.0 | 6000 | 55.1 | .0315 | .0781 |
| .1875 | 10000 | 161.4 | 6700 | 70.9 | .0394 | .0937 | 7500 | 118.1 | 5000 | 51.2 | .0394 | .0937 |
| .2500 | 7600 | 149.6 | 5000 | 70.9 | .0472 | .125 | 5600 | 118.1 | 3800 | 51.2 | .0472 | .125 |
| Depth of cut |
RE : Radius
| Work Material RE | Copper, Co % | pper alloy 15° | %> | 15° | Depth of cut | Depth of cut | Heat resist Inconel718 % | ant alloy etc. 15° | %> | 15° | Depth of cut | Depth of cut |
| (inch) | Revolution (min-1) | Table feed (IPM) | Revolution (min-1) | Table feed (IPM) | ap (inch) | ae (inch) | Revolution (min-1) | Table feed (IPM) | Revolution (min-1) | Table feed (IPM) | ap (inch) | ae (inch) |
| .0625 | 36000 | 338.6 | 24000 | 141.7 | .0098 | .0313 | 6000 | 25.2 | 4000 | 13.4 | .0051 | .0313 |
| .0938 | 24000 | 263.8 | 16000 | 122.0 | .0165 | .0469 | 4000 | 20.9 | 2700 | 9.8 | .0083 | .0469 |
| .1250 | 18000 | 212.6 | 12000 | 98.4 | .0197 | .0626 | 3000 | 19.7 | 2000 | 8.3 | .0098 | .0626 |
| .1563 | 14000 | 196.9 | 9600 | 90.6 | .0315 | .0781 | 2400 | 16.9 | 1600 | 7.5 | .0157 | .0781 |
| .1875 | 12000 | 192.9 | 8000 | 82.7 | .0394 | .0937 | 2000 | 16.5 | 1300 | 7.1 | .0197 | .0937 |
| .2500 | 9100 | 181.1 | 6000 | 86.6 | .0472 | .125 | 1500 | 13.8 | 1000 | 5.9 | .0236 | .0125 |
| Depth of cut |
RE : Radius Note 1) SMART MIRACLE coating has reduced electric conductivity; therefore an external contact type (electric transmitted) tool setter may not work. When measuring the tool length, please use an internal contact type (non-electricity type) tool setter or a laser type tool setter. Note 2) When cutting austenitic stainless steel, the use of water-soluble cutting fluid is especially effective. Note 3) If the depth of cut is smaller than this table, feed rate can be increased. Note 4) The irregular helix flute end mill has a larger effect on controlling vibration when compared to standard end mills. However, if the rigidity of the machine or the work material installation is very low, then vibration can occur. In this case, please reduce the revolution and feed rate proportionately, or set a lower depth of cut. Note 5) % is the inclination of the machined surface. End mill RE
< ae