Общий каталог Mitsubishi 2020 - 2021 - страница 916
Навигация
 Каталог Mitsubishi Materials запасные части
 Каталог Mitsubishi Materials резьбонарезной инструмент
 Каталог Mitsubishi Materials СНП с CBN и PCD для токарной обработки
 Каталог Mitsubishi Materials сверлильные инструменты
 Каталог Mitsubishi Materials расточной инструмент
 Каталог Mitsubishi Materials пластины для точения
CARBIDE
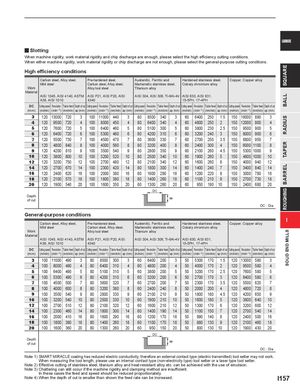
y Slotting
When machine rigidity, work material rigidity and chip discharge are enough, please select the high efficiency cutting conditions. When either machine rigidity, work material rigidity or chip discharge are not enough, please select the general-purpose cutting conditions.
High efficiency conditions
| Work Material | Carbon Mild st AISI 1 A36, A | steel, A eel 045, AIS ISI 1010 | lloy steel I 4140, | , ASTM | Pre-har Carbon Alloy to AISI P 4340 | dened s steel, Al ol steel 21, AISI | teel, loy stee P20, AI | l, SI | Auste Marte Titaniu AISI 3 | nitic, Fer nsitic sta m alloy 04, AISI | ritic and inless s 306, Ti- | teel, 6Al-4V | Harde Cobal AISI 6 15-5P | ned stai y chromi 30, AISI H, 17-4P | nless st um alloy 631, H | eel, | Coppe | r, Copp | er alloy | |
| DC (mm) | Cutting speed (m/min) | Revolution (min-1) | Table feed (mm/min) | Depth of cut ap (mm) | Cutting speed (m/min) | Revolution (min-1) | Table feed (mm/min) | Depth of cu ap (mm) | t Cutting speed (m/min) | Revolution (min-1) | Table feed (mm/min) | Depth of cut ap (mm) | Cutting speed (m/min) | Revolution (min-1) | Table feed (mm/min) | Depth of cut ap (mm) | Cutting speed (m/min) | Revolution (min-1) | Table feed (mm/min) | Depth of cut ap (mm) |
| 3 | 120 | 13000 | 720 | 3 | 100 | 11000 | 440 | 3 | 80 | 8500 | 340 | 3 | 60 | 6400 | 250 | 1.5 | 150 | 16000 | 890 | 3 |
| 4 | 120 | 9500 | 720 | 4 | 100 | 8000 | 450 | 4 | 80 | 6400 | 340 | 4 | 60 | 4800 | 250 | 2 | 150 | 12000 | 900 | 4 |
| 5 | 120 | 7600 | 720 | 5 | 100 | 6400 | 460 | 5 | 80 | 5100 | 300 | 5 | 60 | 3800 | 230 | 2.5 | 150 | 9500 | 900 | 5 |
| 6 | 120 | 6400 | 720 | 6 | 100 | 5300 | 460 | 6 | 80 | 4200 | 310 | 6 | 60 | 3200 | 240 | 3 | 150 | 8000 | 900 | 6 |
| 7 | 120 | 5500 | 730 | 7 | 100 | 4500 | 470 | 7 | 80 | 3600 | 330 | 7 | 60 | 2700 | 250 | 3.5 | 150 | 6800 | 950 | 7 |
| 8 | 120 | 4800 | 840 | 8 | 100 | 4000 | 560 | 8 | 80 | 3200 | 400 | 8 | 60 | 2400 | 300 | 4 | 150 | 6000 | 1100 | 8 |
| 9 | 120 | 4200 | 810 | 9 | 100 | 3500 | 540 | 9 | 80 | 2800 | 350 | 9 | 60 | 2100 | 260 | 4.5 | 150 | 5300 | 1000 | 9 |
| 10 | 120 | 3800 | 800 | 10 | 100 | 3200 | 520 | 10 | 80 | 2500 | 340 | 10 | 60 | 1900 | 260 | 5 | 150 | 4800 | 1000 | 10 |
| 12 | 120 | 3200 | 750 | 12 | 100 | 2700 | 480 | 12 | 80 | 2100 | 340 | 12 | 60 | 1600 | 260 | 6 | 150 | 4000 | 940 | 12 |
| 14 | 120 | 2700 | 670 | 14 | 100 | 2300 | 420 | 14 | 80 | 1800 | 300 | 14 | 60 | 1400 | 240 | 7 | 150 | 3400 | 840 | 14 |
| 16 | 120 | 2400 | 620 | 16 | 100 | 2000 | 380 | 16 | 80 | 1600 | 290 | 16 | 60 | 1200 | 220 | 8 | 150 | 3000 | 780 | 16 |
| 18 | 120 | 2100 | 570 | 18 | 100 | 1800 | 380 | 18 | 80 | 1400 | 260 | 18 | 60 | 1100 | 210 | 9 | 150 | 2700 | 730 | 18 |
| 20 | 120 | 1900 | 540 | 20 | 100 | 1600 | 350 | 20 | 80 | 1300 | 260 | 20 | 60 | 950 | 190 | 10 | 150 | 2400 | 680 | 20 |
| DC | ||||||||||||||||||||
| Depth of cut | ap | |||||||||||||||||||
| D | C : Dia. |
General-purpose conditions
I
| Work Material | Carbon Mild st AISI 1 A36, A | steel, A eel 045, AIS ISI 1010 | lloy steel I 4140, | , ASTM | Pre-ha Carbo Alloy t AISI P 4340 | rdened s n steel, A ool steel 21, AISI | teel, lloy stee P20, AI | l, SI | Auste Marte Titaniu AISI 3 | nitic, Fer nsitic sta m alloy 04, AISI | ritic and inless s 306, Ti- | teel, 6Al-4V | Harde Cobal AISI 6 15-5P | ned stai y chromi 30, AISI H, 17-4P | nless st um alloy 631, H | eel, | Coppe | r, Copp | er alloy | |
| DC (mm) | Cutting speed (m/min) | Revolution (min-1) | Table feed (mm/min) | Depth of cut ap (mm) | Cutting speed (m/min) | Revolution (min-1) | Table feed (mm/min) | Depth of cu ap (mm) | t Cutting speed (m/min) | Revolution (min-1) | Table feed (mm/min) | Depth of cut ap (mm) | Cutting speed (m/min) | Revolution (min-1) | Table feed (mm/min) | Depth of cut ap (mm) | Cutting speed (m/min) | Revolution (min-1) | Table feed (mm/min) | Depth of cut ap (mm) |
| 3 | 100 | 11000 | 490 | 3 | 80 | 8500 | 300 | 3 | 60 | 6400 | 200 | 3 | 50 | 5300 | 170 | 1.5 | 120 | 13000 | 580 | 3 |
| 4 | 100 | 8000 | 490 | 4 | 80 | 6400 | 310 | 4 | 60 | 4800 | 200 | 4 | 50 | 4000 | 170 | 2 | 120 | 9500 | 580 | 4 |
| 5 | 100 | 6400 | 490 | 5 | 80 | 5100 | 310 | 5 | 60 | 3800 | 200 | 5 | 50 | 3200 | 170 | 2.5 | 120 | 7600 | 580 | 5 |
| 6 | 100 | 5300 | 490 | 6 | 80 | 4200 | 310 | 6 | 60 | 3200 | 200 | 6 | 50 | 2700 | 170 | 3 | 120 | 6400 | 580 | 6 |
| 7 | 100 | 4500 | 500 | 7 | 80 | 3600 | 320 | 7 | 60 | 2700 | 200 | 7 | 50 | 2300 | 170 | 3.5 | 120 | 5500 | 620 | 7 |
| 8 | 100 | 4000 | 600 | 8 | 80 | 3200 | 380 | 8 | 60 | 2400 | 240 | 8 | 50 | 2000 | 200 | 4 | 120 | 4800 | 720 | 8 |
| 9 | 100 | 3500 | 540 | 9 | 80 | 2800 | 330 | 9 | 60 | 2100 | 210 | 9 | 50 | 1800 | 180 | 4.5 | 120 | 4200 | 650 | 9 |
| 10 | 100 | 3200 | 540 | 10 | 80 | 2500 | 330 | 10 | 60 | 1900 | 210 | 10 | 50 | 1600 | 180 | 5 | 120 | 3800 | 640 | 10 |
| 12 | 100 | 2700 | 510 | 12 | 80 | 2100 | 320 | 12 | 60 | 1600 | 210 | 12 | 50 | 1300 | 170 | 6 | 120 | 3200 | 600 | 12 |
| 14 | 100 | 2300 | 460 | 14 | 80 | 1800 | 300 | 14 | 60 | 1400 | 190 | 14 | 50 | 1100 | 150 | 7 | 120 | 2700 | 540 | 14 |
| 16 | 100 | 2000 | 410 | 16 | 80 | 1600 | 290 | 16 | 60 | 1200 | 170 | 16 | 50 | 990 | 140 | 8 | 120 | 2400 | 500 | 16 |
| 18 | 100 | 1800 | 390 | 18 | 80 | 1400 | 260 | 18 | 60 | 1100 | 170 | 18 | 50 | 880 | 130 | 9 | 120 | 2100 | 460 | 18 |
| 20 | 100 | 1600 | 360 | 20 | 80 | 1300 | 260 | 20 | 60 | 950 | 150 | 20 | 50 | 800 | 130 | 10 | 120 | 1900 | 430 | 20 |
| Depth of cut | DC | ap | ||||||||||||||||||
| D | C : Dia. |
In these cases the feed and speed should be reduced proportionately. I157 Note 4) When the depth of cut is smaller than shown the feed rate can be increased.